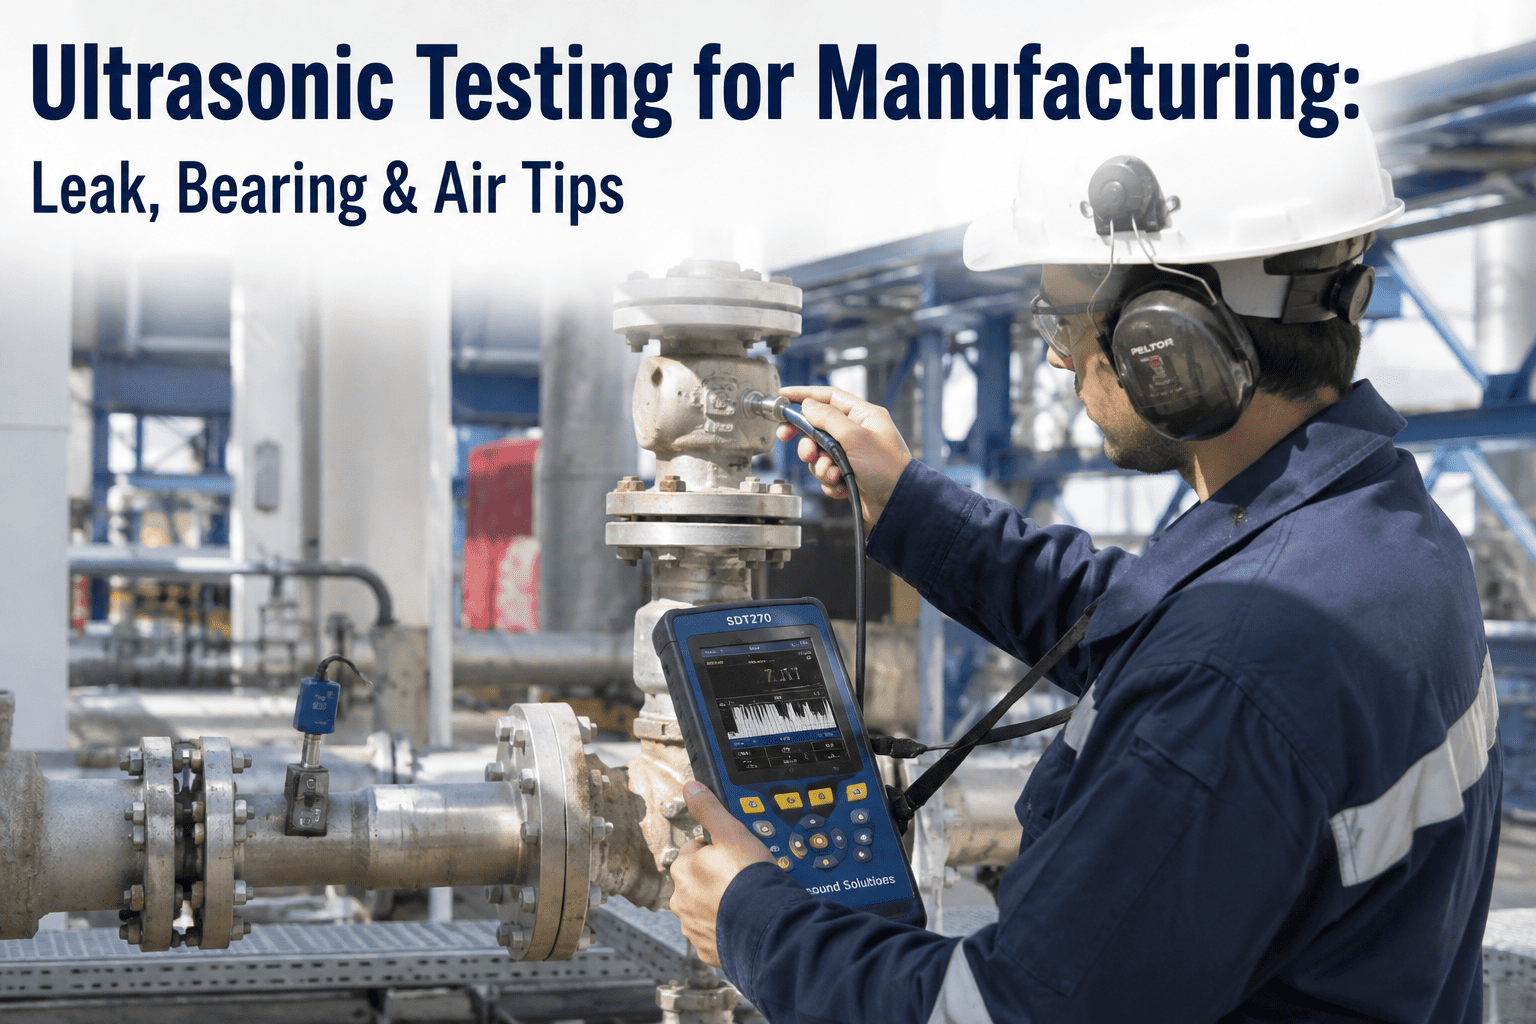
Ultrasonic Testing for Manufacturing: Leak, Bearing & Air Tips
By James Smith on August 7, 2026
Ultrasonic testing occupies an unusual position in the predictive maintenance technology stack: it is simultaneously one of the least expensive condition monitoring technologies to deploy and one of the most consistently underutilized, despite a track record spanning four decades across three of the highest-value applications in any manufacturing plant — compressed air leak detection, bearing condition assessment, and electrical discharge detection. The physics behind all three applications is the same: mechanical friction, turbulent flow, and electrical arcing all generate ultrasonic frequencies well above the range of human hearing and largely above the range of industrial background noise, making them detectable with a directional ultrasonic instrument even in a loud production environment where the same event would be completely inaudible to a technician's ear. This is a practical reference for deploying ultrasonic testing across all three applications, the equipment and methodology each requires, and the programme economics that make UT one of the highest-ROI additions to a condition monitoring programme. Book a session with the iFactory condition monitoring team to discuss ultrasonic testing programme design for your plant.
Condition Monitoring · Ultrasonic Testing
Ultrasonic Testing for Manufacturing: Leak Detection, Bearing Assessment, and Electrical Discharge in One Programme
The lowest-cost, highest-ROI condition monitoring technology in most predictive maintenance programmes — detecting compressed air leaks, bearing faults, and electrical arcing through the ultrasonic signatures each generates, well above the range of human hearing and industrial background noise.
Why the Same Detection Principle Applies to Three Very Different Failure Modes
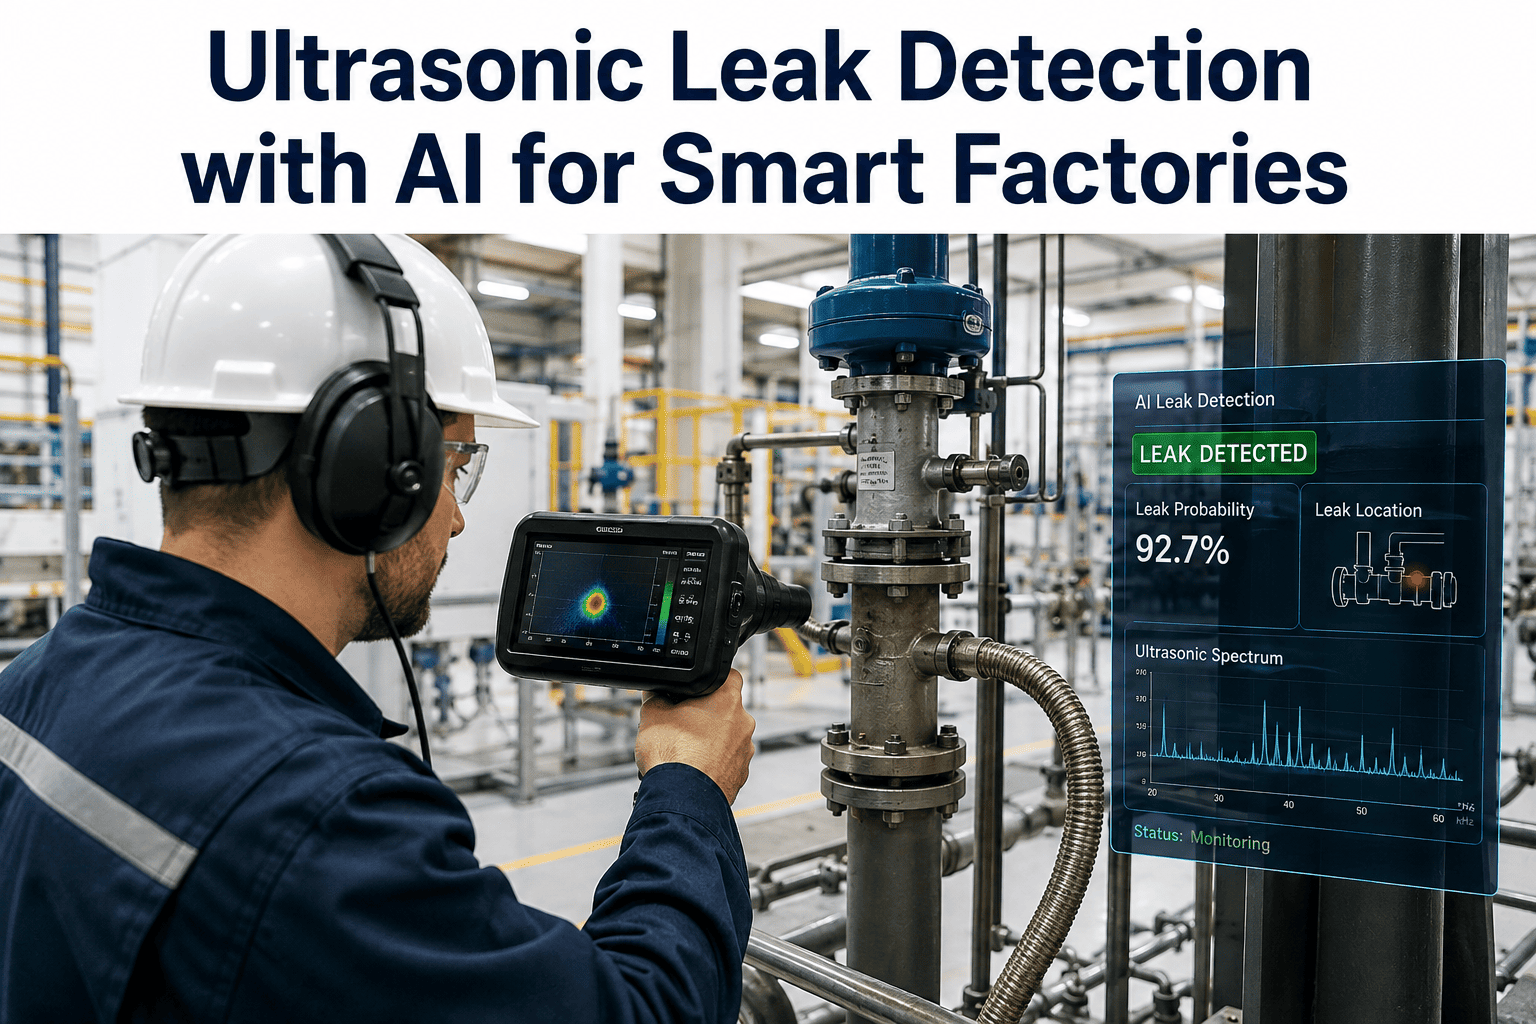
Ultrasonic testing works because turbulent flow, mechanical friction, and electrical arcing all share a common physical property: they generate broadband high-frequency acoustic emissions extending well into the 20 to 100 kHz range, far above both human hearing (roughly 20 Hz to 20 kHz) and the typical frequency content of industrial background noise (predominantly below 10 kHz from motors, fans, and mechanical operation). A directional ultrasonic instrument with a heterodyning receiver converts these otherwise inaudible high frequencies into an audible tone the technician can hear through headphones, combined with a numeric intensity reading (typically in decibels) that quantifies signal strength for trending and severity assessment.
Compressed Air & Gas Leaks
Turbulent flow through a leak orifice generates ultrasonic frequencies proportional to the pressure differential and orifice geometry — the same physical mechanism regardless of whether the escaping medium is compressed air, steam, or process gas, making UT applicable across all pressurized system leak detection.
Bearing Friction and Wear
Rolling element contact under normal lubrication produces a characteristic low-level ultrasonic signature; as lubrication degrades or surface defects develop, both the intensity and the character of the ultrasonic emission change measurably, often before vibration-based methods detect the same developing fault.
Electrical Discharge and Arcing
Corona discharge, tracking, and arcing in electrical equipment ionize the surrounding air, producing a distinctive broadband ultrasonic emission — a serious fault precursor that is completely undetectable by visual inspection or standard electrical testing until the discharge has already caused significant insulation degradation.
Application 1 — Compressed Air & Gas Leak Detection
Locating and Prioritizing Leaks Across Pressurized Systems
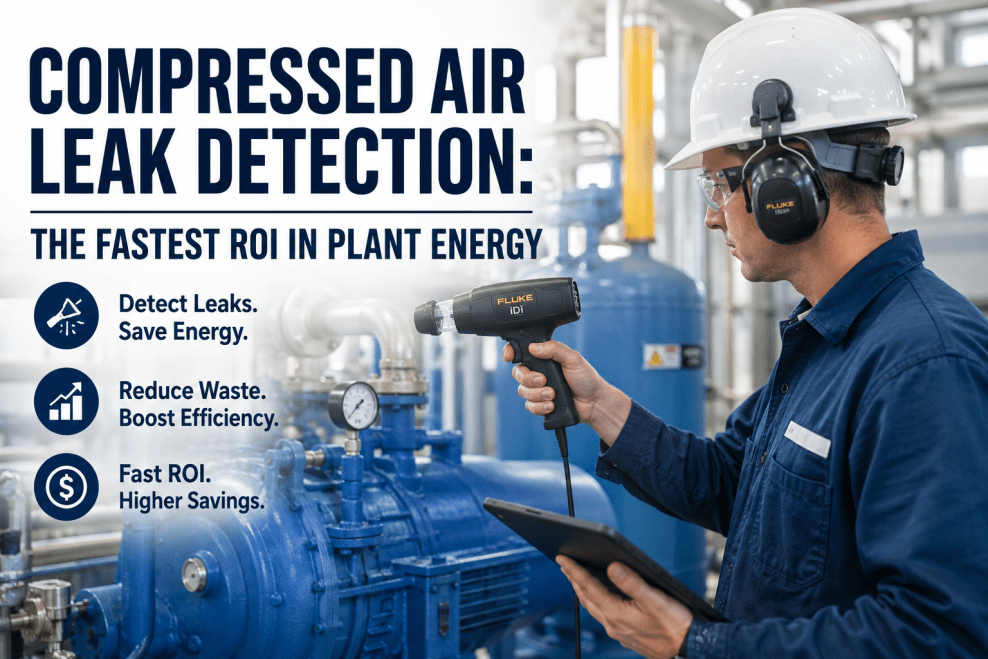
Ultrasonic leak detection is the highest-volume application of UT in most manufacturing plants and typically the fastest to demonstrate clear financial return, given that compressed air is among the most expensive utilities in a facility and leaks are almost always more numerous than facilities management expects until a systematic survey is conducted.
Survey Element
Method
Typical Finding Rate
Prioritization Basis
Compressed air distribution
Directional scan along piping, fittings, valves, quick-connects
15–30 leaks per 100,000 sq ft (first survey)
Estimated CFM loss from signal intensity → $ cost
Vacuum system leaks
Scan at joints, seals, and connection points under vacuum
Varies by system age and complexity
Process impact of vacuum loss on affected equipment
Steam trap function
Contact ultrasonic on trap body — distinguishes cycling from failed-open
15–25% of traps failed on first inspection (industry average)
Steam loss cost of failed-open traps
Refrigerant and process gas
Directional scan at fittings and seals on sealed systems
System-specific, often low-frequency but high consequence
Refrigerant cost and regulatory reporting requirements
Best practice survey timing conducts leak surveys during off-shift or low-production periods when ambient plant noise is reduced and the compressed air system is under normal operating pressure — surveys during full production still work but benefit from the improved signal-to-noise ratio of a quieter environment.
Application 2 — Bearing Condition Assessment
Ultrasonic Bearing Monitoring — Earlier Detection Than Vibration Alone
Ultrasonic bearing assessment frequently detects developing faults earlier in the failure progression than standard vibration analysis, because lubrication degradation and the earliest stages of surface fatigue produce a detectable ultrasonic signature before they generate sufficient mechanical vibration to register clearly against a vibration baseline. The two technologies are complementary rather than competing — many mature reliability programmes use ultrasonic bearing checks for early screening across a large asset population, reserving detailed vibration spectral analysis for assets flagged by ultrasonic screening or already identified as critical.
Lubrication Condition Screening
Ultrasonic intensity trending is one of the most effective methods for right-time lubrication — rather than relubricating on a fixed calendar interval regardless of actual need, ultrasonic monitoring identifies when a bearing's ultrasonic signature indicates lubricant film degradation, triggering relubrication precisely when needed. This reduces both under-lubrication failures and the equally damaging practice of over-greasing.
Early Fault Detection
Rising ultrasonic intensity trend, independent of any relubrication event, indicates developing surface fatigue or contamination — often detectable at an earlier stage than vibration analysis because the ultrasonic emission from micro-scale surface irregularities precedes the larger-amplitude vibration signature that develops as the fault progresses further.
Route-Based Screening at Scale
Ultrasonic bearing checks are fast to perform — often under a minute per measurement point — making them practical for route-based screening across hundreds of bearing locations that would be impractical to cover with detailed vibration spectral analysis on the same frequency, extending condition monitoring coverage to balance-of-plant equipment that would otherwise receive no systematic monitoring.
See What a Systematic UT Survey Finds in Your Plant
iFactory's Ultrasonic Testing Programme Covers Leak Detection, Bearing Screening, and Electrical Discharge in One Deployment
Most plants have never run a systematic ultrasonic survey across all three application areas simultaneously. iFactory's UT programme assessment identifies your leak population, screens your bearing population for early-stage faults, and checks electrical equipment for discharge activity — typically surfacing findings across all three categories in the first survey cycle.
Detecting Corona, Tracking, and Arcing Before Insulation Failure
Electrical discharge detection is the least widely deployed of the three primary UT applications despite arguably carrying the highest consequence severity — undetected arcing and tracking in switchgear, motor control centers, and high-voltage equipment can progress to catastrophic failure, arc flash events, and fire risk. Ultrasonic detection identifies discharge activity while it is still in an early, non-visible stage, well before thermal imaging or visual inspection would reveal any external sign.
Corona Discharge
Ionization of air around a high-voltage conductor at a point of sufficient electrical stress — typically detectable via ultrasonic before it becomes visible even with UV corona cameras in daylight conditions, making UT a valuable first-line screening method for high-voltage equipment.
Surface Tracking
Discharge across a contaminated or degraded insulator surface, producing a distinctive intermittent ultrasonic signature — an early indicator of insulation contamination or degradation that, left unaddressed, can progress to a surface flashover event.
Internal Arcing
Arcing within enclosed switchgear or equipment, often accompanied by a detectable ultrasonic signature transmitted through enclosure seams and openings even when the arc itself is not visible — one of the most safety-critical findings a UT programme can surface, warranting immediate de-energization and investigation protocol.
Programme Economics
Why Ultrasonic Testing Delivers Among the Fastest Payback in Condition Monitoring
Ultrasonic testing equipment cost is modest relative to most other condition monitoring technologies, and the multi-application capability of a single instrument (leak detection, bearing assessment, and electrical discharge screening all performed with the same base unit and different accessories) means the equipment investment is leveraged across three high-value use cases rather than a single dedicated purpose.
Programme Element
Typical Investment
Typical Annual Value
Typical Payback
UT instrument and accessories
$4,000–$12,000
—
One-time capital
Initial leak survey and repair
$8,000–$20,000
$60,000–$180,000
1–3 months
Ongoing bearing screening programme
$15,000–$35,000/yr (labor)
$40,000–$150,000/yr (avoided failures)
3–8 months
Electrical discharge screening
$10,000–$25,000/yr (labor)
Risk avoidance — high severity, lower frequency
Risk-adjusted — variable
The electrical discharge application carries a different economic profile than the other two — the direct financial value of a caught fault is high but the frequency of findings is typically lower, meaning the programme's value case rests more heavily on risk avoidance (preventing catastrophic failure, arc flash injury, and fire risk) than on a straightforward frequency-based cost calculation.
UT Programme KPIs
Six Metrics That Define Ultrasonic Testing Programme Maturity
Leak Load Percentage
Target: <10%
Compressed air leak volume as a percentage of total system output, tracked continuously through repeat survey cycles. The primary leak programme outcome metric — shared with the dedicated compressed air optimization discipline.
Bearing Population Coverage
Target: 100% on defined route
Percentage of the plant's bearing population included in a scheduled ultrasonic screening route. Any excluded population represents a monitoring blind spot in an otherwise low-cost-to-cover asset category.
Right-Time Lubrication Rate
Target: >80% condition-triggered
Percentage of relubrication events triggered by ultrasonic condition indication rather than fixed calendar schedule. Higher percentages indicate the programme has matured from time-based to condition-based lubrication practice.
Electrical Equipment Screening Coverage
Target: 100% of critical assets, annual minimum
Percentage of critical electrical equipment (switchgear, MCCs, high-voltage assets) receiving at least annual ultrasonic discharge screening. Given the safety severity of undetected arcing, coverage completeness matters more than survey frequency for this application.
Mean Time to Repair — Leak Findings
Target: <10 days
Time from leak identification to confirmed repair. A finding not repaired continues accumulating its full cost — tracking closure time ensures survey findings translate into realized savings rather than an unactioned report.
Technician Certification Level
Target: Level I minimum, Level II for programme lead
Formal ultrasonic testing certification level of programme personnel, following recognized certification body standards. Programme reliability and finding consistency correlate strongly with technician training level, particularly for the more nuanced bearing and electrical discharge applications.
From the Condition Monitoring Floor
“
Ultrasonic testing is the technology I recommend first to any plant building a condition monitoring programme from scratch, and it consistently surprises me how few plants have adopted it systematically given how favorable the economics are. Part of the reason is that UT sits in an awkward perception gap — it is not glamorous the way vibration analysis or thermal imaging can seem, and the instrument itself is deceptively simple, a handheld unit with headphones, which undersells how much genuine diagnostic capability it carries. I have walked plants that had invested heavily in vibration monitoring programmes for their critical rotating assets but had never run a single compressed air leak survey, despite compressed air being one of their largest utility line items — the mismatch between where the money was spent and where the money was actually being wasted was significant. The plants that get the most value from ultrasonic testing are the ones that treat it as a genuine three-application programme from the start — leak detection, bearing screening, and electrical discharge — rather than deploying it for just one use case and leaving the other two capabilities of the same instrument unused.
Casimir Njoroge-Halvorsen
Certified Ultrasound Analyst (Level III) · Condition Monitoring Specialist · 21 years in industrial predictive maintenance across manufacturing and process industries · Former Reliability Programme Manager, multi-site industrial group · UE Systems and SDT certified trainer
Condition Monitoring Team Questions
Ultrasonic Testing for Manufacturing — Frequently Asked
How does ultrasonic testing compare to vibration analysis for bearing condition monitoring — should we use one or both?
Ultrasonic testing and vibration analysis are complementary technologies detecting different aspects of bearing condition, and mature reliability programmes typically use both rather than choosing one exclusively. Ultrasonic excels at early lubrication condition screening and can detect the very earliest stages of surface fatigue, and its speed of measurement makes it practical for screening large bearing populations that would be impractical to cover with detailed vibration spectral analysis. Vibration analysis provides more detailed diagnostic information once a fault is developing — bearing frequency analysis, precise fault stage identification, and the ability to distinguish between multiple simultaneous fault modes — capability that ultrasonic alone does not fully replicate. A common and effective programme structure uses ultrasonic screening across the full bearing population on a route basis for early detection and lubrication management, reserving vibration analysis for permanently monitored critical assets and for detailed investigation once ultrasonic screening flags a bearing showing a developing trend. For guidance on structuring a combined UT and vibration programme for your asset population, book a session with the iFactory condition monitoring team.
What certification level do our technicians need to run an effective ultrasonic testing programme?
Certification requirements scale with application complexity. Basic compressed air leak detection is the most accessible application and can be performed effectively by technicians with fundamental UT training (often equivalent to Level I certification under recognized bodies such as UE Systems or SDT), given clear survey procedures and straightforward pass/fail interpretation criteria. Bearing condition assessment requires more nuanced interpretation of trending data and signature characteristics, generally benefiting from Level I certification for routine screening with Level II oversight for interpreting ambiguous or borderline findings and establishing baseline and alarm thresholds for new equipment. Electrical discharge detection carries the highest interpretation complexity and the highest consequence of a missed or misinterpreted finding, warranting Level II certification as a minimum for personnel performing this application, with Level III oversight for programme design and complex case interpretation. Investing in proper certification, rather than assuming the instrument alone provides adequate diagnostic capability, is one of the highest-leverage decisions in building a reliable UT programme. Contact our support team for certification pathway guidance.
Can ultrasonic testing be automated or continuously monitored, or does it require a technician walking a route with a handheld instrument?
Both approaches exist and serve different needs within a mature programme. Route-based handheld ultrasonic testing remains the standard approach for compressed air leak surveys (since leak locations are distributed across a large physical area not economical to instrument permanently) and for bearing screening across a large asset population where fixed sensors on every bearing would be cost-prohibitive. Permanently installed ultrasonic sensors, feeding continuous monitoring systems, are increasingly deployed for the highest-criticality assets and for electrical discharge monitoring on critical switchgear where continuous coverage justifies the additional investment given the severity consequence of a missed developing fault. The typical mature programme structure uses continuous fixed monitoring for the small population of highest-criticality assets, supplemented by route-based handheld screening covering the much larger population of standard-criticality equipment — balancing coverage completeness against instrumentation cost. AI-driven analysis of continuous ultrasonic sensor data can further improve fixed-monitoring programmes by automating trend detection and reducing the manual review burden that would otherwise limit how many continuously monitored points a team can effectively track.
How do we establish baseline and alarm thresholds for ultrasonic bearing monitoring on equipment we have no prior UT history for?
Establishing baselines on equipment without prior ultrasonic history requires a structured initial data collection period rather than assuming generic industry threshold values apply directly, since ultrasonic intensity readings are influenced by bearing size, speed, load, and even instrument-specific calibration factors that make absolute threshold values not directly transferable between different equipment or instrument setups. The recommended approach takes an initial baseline reading on each bearing under known-good operating conditions, then establishes an alarm threshold as a percentage increase relative to that specific bearing's own baseline (commonly in the range of 8 to 12 decibels above baseline as an initial alert threshold, though this should be refined based on your own programme's developing experience) rather than applying a single absolute threshold value across dissimilar equipment. As the programme matures and accumulates trend history alongside confirmed fault outcomes, threshold values can be refined and validated against your own plant's actual failure data, producing increasingly reliable and well-calibrated alarm criteria specific to your equipment population.
Is ultrasonic testing effective for detecting leaks or faults through walls, insulation, or enclosures, or does it require direct line of sight?
Airborne ultrasonic energy behaves somewhat differently from audible sound in that it does not propagate as effectively through solid barriers, generally requiring either direct line of sight to the leak or fault source, or a path through gaps, seams, or openings that allow the ultrasonic energy to reach the instrument's sensor. This means leak detection on enclosed pressurized systems may require access panels or known inspection points rather than scanning through a solid enclosure wall, and electrical discharge detection inside switchgear often relies on the discharge's ultrasonic signature transmitting through ventilation openings, seams, or gaps in the enclosure rather than through the solid enclosure material itself — which is why enclosure design and available access points matter when planning electrical discharge screening coverage. Contact ultrasonic probes, used for structure-borne applications like bearing assessment, work differently — transmitting through direct mechanical contact with the equipment rather than through air, and are not subject to the same line-of-sight limitation as airborne ultrasonic detection for leaks and electrical discharge. Understanding this distinction is important for realistic survey coverage planning, particularly for electrical discharge screening where enclosure design significantly affects detectability.
One Instrument. Three High-Value Applications. Consistently Underused.
Build a Systematic Ultrasonic Testing Programme Across Leak Detection, Bearing Health, and Electrical Safety
iFactory's condition monitoring team helps design and deploy ultrasonic testing programmes covering all three high-value applications — compressed air and gas leak surveys, bearing lubrication and early fault screening, and electrical discharge detection on critical switchgear — with the certification pathway, survey methodology, and trending framework that turns a handheld instrument into a genuine reliability programme.