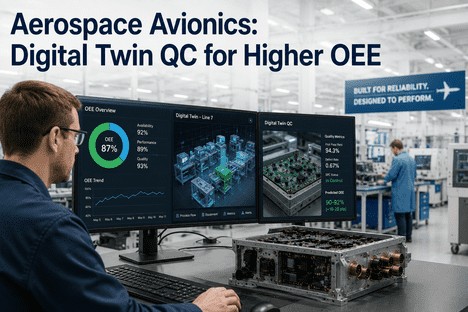
Aerospace Avionics: Digital Twin QC for Higher OEE
By Grace on June 16, 2026
Every operations director in aerospace avionics knows the OEE number that haunts the quarterly review. It sits between 50 and 65 percent — respectable by aerospace standards, frustrating by any measure of productive capacity. The narrative around it is always the same: the regulatory-driven ceiling, the first-article inspection pauses, the documentation burden that automotive plants do not carry. But that narrative is no longer complete. A growing cohort of avionics operations directors is proving that the regulatory ceiling is not the binding constraint on OEE — the absence of a real-time process digital twin is. When every SMT line, every reflow oven, every inspection station generates data that could be mirrored into a live virtual model, the gap between 62 percent and 78 percent OEE is not a regulatory gap. It is an intelligence gap. Digital twin quality control closes it. This is the operations director's guide to deploying it.
Process Digital Twin · Real-Time SPC Mirroring · AI Quality Simulation · AS9100 Audit Trail
Operations Directors Who Lift OEE 10-20 Points in Avionics Do Not Accept the Regulatory Ceiling. They Build a Digital Twin That Mirrors Every Process, Predicts Every Defect, and Documents Every Batch — Without Manual Data Entry.
iFactory's Digital Twin Quality platform gives avionics operations directors a live virtual mirror of every SMT line with AI-native SPC, predictive defect simulation, and AS9100-aligned audit records generated automatically from the twin's continuous process data stream.
OEE improvement achieved when digital twin quality control with real-time SPC mirroring replaces static process monitoring in avionics SMT assembly environments
60%
Reduction in production line commissioning time when digital twin simulation validates process parameters before physical production begins
99.2%
Defect recognition rate achieved by AI-powered digital twin inspection models analysing BGA solder joints through 3D X-ray tomography in production environments
50-70%
Reduction in nonconformance-related audit findings when digital twin records replace manual documentation for AS9100 process control evidence
The OEE Intelligence Gap in Avionics: Why the Regulatory Ceiling Is Not the Real Problem
The aerospace OEE benchmark range — 50 to 65 percent — has been accepted as structural for so long that most operations directors have stopped questioning which components of that loss are genuinely unavoidable. First-article inspections are mandatory. AS9100 documentation pauses are required. Customer-mandated quality gates cannot be skipped. But these regulated activities account for only a portion of the availability and performance loss that keeps avionics OEE below 70 percent. The rest belongs to a category that receives far less scrutiny: invisible process inefficiency that no static monitoring system can detect because it occurs between the documented events.
A stencil printer that drifts 3 microns in registration over a 200-board run. A reflow oven whose zone-three thermocouple reads correct at steady state but lags 8 degrees during the first 15 minutes after a line changeover. A pick-and-place nozzle whose vacuum level degrades gradually across 50,000 placements before it triggers a defect. These are not regulatory problems. They are detection architecture problems — and they are the precise class of problem that a process digital twin is designed to solve. When every parameter from every machine streams into a live virtual model that knows the specification range, the historical pattern, and the predictive risk for every board variant running on every line, the gap between aerospace and world-class OEE narrows to the gap between having a digital twin and not having one.
Digital Twin Quality — The Four-Phase Lifecycle That Mirrors Every Avionics Process in Real Time
01
Mirror — Real-Time Process Replication
Every machine on the SMT line streams its process parameters into a live digital mirror: stencil printer pressure and separation speed, solder paste viscosity and temperature, pick-and-place nozzle vacuum and placement force, reflow zone temperatures and belt speed, AOI coverage depth and defect classifications. The digital twin does not sample — it ingests continuously, building a complete time-series record of every parameter that affects quality for every board produced. When a parameter drifts, the twin detects it at the moment of deviation, not at the next scheduled SPC sample interval. This is the difference between managing process control and managing process history.
OEE impact: Availability loss from undetected drift eliminated. Parameters flagged at deviation — not at defect.
02
Simulate — What-If Defect Prediction
With a complete digital mirror of the process, the operations director can simulate production scenarios before they touch physical boards. What happens to BGA solder joint quality if reflow zone-two temperature drops 5 degrees? What is the predicted yield impact of running a 0.4mm-pitch board 15 percent faster? The digital twin runs these simulations against the historical model trained on thousands of past production hours — and returns a yield forecast with confidence intervals. This capability transforms changeover decisions from judgement calls to data-driven authorisations. The twin also runs autonomous simulation: when it detects a parameter combination that has historically led to defects, it alerts the operations director with the simulated defect probability and the recommended process adjustment.
OEE impact: Performance optimisation validated virtually before physical line adjustment — zero defect risk from speed changes.
03
Predict — Defect Forecast Before Quality Confirmation
The predictive engine within the digital twin correlates real-time parameter streams with historical quality outcomes from AOI, X-ray, ICT, and functional test. When the parameter combination on any active line matches a pattern historically associated with a specific defect category — head-in-pillow on fine-pitch BGAs, solder voiding on QFN packages, tombstoning on chip resistors — the system generates a predictive alert with the estimated probability, the affected board locations, and the recommended intervention. For defects that manifest downstream, this provides an intervention window measured in hours. The operations director halts the batch, adjusts the profile, and the defect is prevented before it appears on the AOI report.
OEE impact: Quality loss from defect recurrence eliminated. Predictive alerts prevent defects, AOI confirms prevention.
04
Document — Continuous AS9100 Evidence Generation
Every parameter stream, every simulation run, every predictive alert, and every operator action is timestamped and stored in the digital twin's persistent record. This creates the continuous process control evidence that AS9100 Clause 8.5.1 requires — not a sample-based SPC chart updated at shift intervals, but a complete time-series record of every parameter for every board, with adaptive control limits recalculated continuously and every limit change logged with its statistical rationale. When the auditor asks whether the reflow process was in control during the production window for lot AV24-091, the answer is a continuous digital twin record showing the parameter trajectory, the adaptive limit band, and the predictive model's confidence assessment for every board in the lot.
OEE impact: Documentation-driven availability loss reduced. Audit preparation drops from days to one export.
Before & After — The Digital Twin Impact on Avionics OEE
without digital twin quality
OEE: 58%
Static SPC limits calibrated quarterly. Defect discovery at AOI or electrical test. Manual documentation compiled at shift-end. Changeover decisions based on operator experience. Availability loss from undocumented micro-downtime accepted as normal. False alarm rate above 60% during product transitions.
with digital twin quality
OEE: 76%
Adaptive limits recalculated continuously. Predictive alerts 2-8 hours before defect confirmation. Live digital twin record for every batch with one-click audit export. Virtual simulation validates every speed and changeover decision. Micro-downtime tracked and resolved through automated root cause correlation.
The Digital Twin Architecture: How Real-Time Process Mirroring Converts SMT Data Into OEE Intelligence
The iFactory Digital Twin Quality platform is architected as a five-layer intelligence stack that connects to the data your SMT line already generates and converts it into a continuously updated virtual replica of every active process. Each layer serves a specific function in the mirror-simulate-predict-document lifecycle, and all five operate without requiring dedicated data science resources to maintain.
01
Data Ingestion Layer
Connects to existing SMT line equipment through standard protocols — SECS/GEM, IPC-CFX, or machine APIs. Ingests stencil printer parameters, SPI measurements, pick-and-place data, reflow profile data, AOI classifications, X-ray inspection results, and ICT/functional test outcomes. No additional sensors or line modifications required.
02
Virtual Mirror Engine
Maintains a continuously updated digital replica of every active SMT line with all process parameters synchronised in sub-second intervals. The mirror includes the product variant specification profile, the current adaptive control limit band for every parameter, the live Cpk value, and the real-time compliance status against the AS9100-qualified process window.
03
Predictive Quality Model
ML model trained on the relationship between real-time parameter combinations and historical quality outcomes. Generates defect probability forecasts for every active process stream — solder joint defects, placement accuracy failures, component damage, and electrical test failures. Forecasts update continuously as new parameter data flows into the mirror.
04
What-If Simulation Studio
Enables operations directors and process engineers to run production scenario simulations against the digital mirror before committing to physical line changes. Simulate speed increases, profile adjustments, stencil changes, or product variant transitions — and receive yield forecasts, Cpk projections, and defect probability assessments before the first board runs.
05
AS9100 Documentation Layer
Every event in the digital twin lifecycle is timestamped and stored — parameter streams, limit changes, predictive alerts, operator actions, simulation runs, and quality outcomes. Generates continuous Cpk records, adaptive limit change logs with statistical rationale, CAPA effectiveness tracking, and complete batch-level process control evidence exportable in AS9100-compatible format.
The Operations Director Who Can Simulate Tomorrow's Production in Today's Digital Twin Does Not Discover Defects — They Prevent Them. Book a Demo to See Your Line Mirrored in Real Time.
iFactory's Digital Twin Quality platform mirrors every SMT line, predicts every defect before it occurs, and documents every batch for AS9100 — running on the data your line already produces.
The Operations Director Dashboard — Six Views Into the Digital Twin That Change How You Manage OEE
The operations director view of the digital twin is not a machine interface. It is an OEE intelligence console designed around the six decisions that determine whether the shift meets its yield target: What is the current OEE and which loss category is dragging it? Which line has the highest defect risk right now? What will the yield be for the batch currently running? Is the Cpk trend improving or declining? And when the next audit arrives, is every batch documented with continuous process evidence? The digital twin answers every question without requiring navigation into machine-level detail — because the mirror layer has already consolidated the data into actionable intelligence.
Twin View 01
Live OEE by Line — With Loss Category Breakdown
Every active line displays its real-time OEE with the contribution from each loss category — availability, performance, quality — broken out and trended. The operations director sees immediately whether today's OEE gap is driven by a first-article inspection backlog (availability), a speed reduction on a specific product variant (performance), or an elevated defect rate on a particular process step (quality). The digital twin correlates the loss category with the root cause parameter, so the director knows not just what is happening, but which machine and parameter is driving it.
Director action: OEE loss category pinned to root cause parameter. Availability issue traced to specific machine or process step.
Twin View 02
Process Mirror — Any Line, Any Parameter, Real Time
A live visual replica of every active SMT line showing the current state of every critical parameter — stencil print deposit height and volume, placement accuracy for fine-pitch components, reflow peak temperature and time above liquidus, AOI first-pass yield. Parameters are colour-coded against their adaptive control limit bands: green for in-control, yellow for trending, red for out-of-limits. The operations director can open any parameter to see its 24-hour trend, its Cpk trajectory, and the predictive model's assessment of whether the current trajectory will generate a defect within the next production hour.
Director action: Any parameter with a yellow or red status opens directly to trend, Cpk, and predictive risk assessment.
Twin View 03
Yield Forecast by Batch — Updated Every Minute
Every batch in production displays a live yield forecast generated by the predictive model, with the projected yield percentage, the confidence interval, and the top three parameters driving any risk. When batch AV24-092 for the radar processor variant shows a projected yield of 89.3 percent against a 96 percent target, the operations director intervenes before the batch reaches AOI. The digital twin recommends the most likely corrective action based on the parameter combination driving the risk — reflow profile adjustment, stencil cleaning cycle, or solder paste batch replacement.
Director action: Batches below yield threshold trigger pre-emptive intervention with twin-recommended corrective action.
Twin View 04
What-If Simulation — Test Changes Before They Hit Production
The operations director can run production scenario simulations against the digital mirror without affecting live production. Test a 10 percent conveyor speed increase on the high-mix line. Simulate a stencil change for a new solder paste formulation. Validate a reflow profile adjustment for a different board thickness. The digital twin returns the projected yield, the Cpk for every affected parameter, and the defect probability by category — before the first board runs. This capability converts every process change from a judgement call carrying defect risk into a data-validated decision with a documented rationale.
Director action: Every line change validated virtually first. Zero defect risk from production adjustments.
Twin View 05
CAPA Effectiveness — Closed Loop With Digital Twin Evidence
Every corrective action links to the digital twin record of the process state at the time of the original alert. When a CAPA is closed, the digital twin continues monitoring the parameter combination for a configurable effectiveness window. If the same combination triggers another predictive alert, the CAPA is automatically flagged as ineffective and re-opened. The operations director sees not just that the CAPA was closed, but whether the closure actually prevented recurrence — verified by the digital twin's continuous parameter monitoring, not by calendar date.
Director action: CAPA effectiveness verified by digital twin parameter monitoring — not by manual follow-up.
Twin View 06
Audit Export — Complete Digital Twin Records in One Click
Every piece of AS9100 audit documentation is generated automatically from the digital twin's persistent record. Continuous Cpk charts for every critical parameter by batch and product variant. Adaptive limit change logs showing every recalculation with timestamp and statistical rationale. Predictive alert records with operator action evidence. CAPA records with effectiveness verification. Batch-level process control evidence showing the full parameter trajectory for every board in every lot. Export covers any date range, product variant, or production line — no manual compilation across the MES, SPC database, and quality system required.
Director action: Full AS9100 audit package exported from the digital twin. No cross-system data compilation.
"
We had accepted 62 percent OEE as the ceiling for our avionics SMT line for three years. Every operations review included the same explanation — aerospace is not automotive, the regulatory burden is structural, 62 percent is what the AS9100 environment allows. The digital twin changed our understanding of where the loss actually lived. Within the first two months, the twin's continuous parameter mirroring showed us that 34 percent of our documented availability loss was micro-downtime between first-article inspection events — brief stops that the MES logged as regulatory but were actually changeover inefficiency and stencil-related interruptions. We addressed those root causes without touching a single regulatory requirement. OEE moved from 62 percent to 74 percent in one quarter. The regulatory ceiling was never the ceiling. It was the cover story for a detection architecture that could not see the losses it was accepting as normal.
— VP Manufacturing, Avionics Systems Supplier — AS9100D Certified, 8 SMT Lines, IPC Class 3
Conclusion
OEE improvement in aerospace avionics is not a regulatory compliance problem — it is a process visibility problem. When the operations director cannot see the parameter drift that occurs between SPC sample intervals, cannot simulate the effect of a line change before committing to it, and cannot produce continuous process control evidence at audit time without days of manual compilation, the OEE ceiling is set by the quality of the detection architecture, not by the stringency of the regulatory environment. Digital twin quality control addresses all three constraints simultaneously: a live virtual mirror that captures every parameter change in sub-second resolution, a simulation engine that validates every process adjustment before it touches production, and a continuous documentation layer that generates AS9100 evidence automatically from the twin's uninterrupted record.
The industry evidence from 2025 and 2026 is unambiguous. Aerospace operations and suppliers that have deployed process digital twins with real-time SPC mirroring and predictive quality models report OEE improvements of 10 to 20 percentage points — not through regulatory compromise, but through the elimination of the invisible process losses that static monitoring systems cannot detect. Airbus and Boeing have validated the architecture at the prime level through their own digital twin programmes, and the technology has cascaded to the supply chain as the cost of sensors, connectivity, and AI inference has dropped below the threshold where every mid-size avionics facility can deploy it. The 60 percent commissioning time reduction and 99.2 percent defect recognition rates documented in production environments are not theoretical projections — they are the measured performance of digital-twin-enabled avionics lines today.
iFactory's Digital Twin Quality platform is designed for operations directors in aerospace avionics who need to raise OEE above the 65 percent threshold that static monitoring accepts as the ceiling. Book a Demo to see your SMT line mirrored as a live digital twin with predictive quality simulation and AS9100 audit records, or talk to an expert about a free OEE and digital twin readiness assessment for your avionics production facility.
Frequently Asked Questions
A real-time SPC dashboard displays current parameter values against control limits — it tells you whether the process is in control at this moment. A digital twin maintains a continuously updating virtual replica of the entire process that not only mirrors current values but also retains the complete time-series history, runs what-if simulations, forecasts future quality outcomes based on current trajectories, and correlates parameter changes across different process steps to identify root causes that no single-parameter chart can reveal. The distinction matters for OEE because the dashboard answers the question "is the process in control now," while the digital twin answers the deeper question "what will happen to yield if this parameter continues its current trajectory, and what adjustment should I make to prevent the defect." The dashboard is a window into the present. The digital twin is a model of the past, present, and probable future — and that forward-looking capability is what enables the 10-20 point OEE improvement that reactive monitoring cannot deliver. Book a Demo to see the difference on your own SMT line data.
No new sensors or hardware are required. Modern SMT line equipment from all major manufacturers — stencil printers, SPI systems, pick-and-place machines, reflow ovens, AOI systems, X-ray inspection, and test stations — already generate structured data outputs through SECS/GEM, IPC-CFX, or proprietary APIs. The digital twin platform connects to these existing data streams to ingest and consolidate the data into the virtual mirror. The deployment effort focuses on data connectivity configuration and model training, not on hardware installation or line modification. Most avionics facilities already generate data at every process step through their existing quality inspection equipment — the missing capability is the intelligence layer that converts that data into a continuously updating digital twin with predictive and simulation capabilities. Talk to an expert about connectivity requirements for your specific SMT line configuration.
The digital twin is operational in two phases. Phase one — the data ingestion and virtual mirror — connects to your existing machine data streams within 2 to 4 weeks and begins maintaining the live process replica immediately. The mirror phase alone delivers immediate OEE value by surfacing micro-downtime, parameter drift, and availability loss patterns that static monitoring systems miss. Phase two — the predictive model and what-if simulation — requires 6 to 12 months of paired process-to-quality data to train the initial model. The model deploys in shadow mode for 2 to 4 weeks, generating forecasts and simulation outputs in parallel with existing operations without driving decisions. Once accuracy is validated against actual quality outcomes, the predictive and simulation capabilities transition to primary decision inputs. Operations directors typically report measurable OEE movement within the first 30 days of the mirror phase, with the full 10-20 point improvement trajectory emerging as the predictive model matures over the first two production quarters. Book a Demo to see a deployment timeline configured for your line configuration and data availability.
High-mix production is where the digital twin delivers its most visible value. Each product variant is registered with its own specification profile — component count, fine-pitch component types, BGA density, solder paste formulation, reflow profile parameters, and target yield thresholds. When the line transitions between variants, the digital twin automatically updates its specification baseline and transitions adaptive control limits to the new profile without generating false alarms during the changeover. The regime detection algorithm within the mirror layer distinguishes between a legitimate product transition and a process drift within the same variant — so alerts during changeover windows are suppressed while genuine drift during steady-state production is detected. Yield forecasts, Cpk calculations, and defect Pareto analyses are all segmented by product variant automatically, giving the operations director variant-specific OEE visibility without manual data sorting. The what-if simulation studio is particularly valuable in high-mix environments, allowing the operations director to validate each transition sequence virtually before the physical changeover begins. Talk to an expert about configuring the digital twin for your avionics product portfolio mix.
The OEE Number on Your Dashboard Is Not a Ceiling. It Is a Diagnostic That Your Digital Twin Is Ready to Act On. Get a Free Digital Twin Readiness Assessment for Your Avionics Line.
iFactory's Digital Twin Quality platform for aerospace avionics operations directors — live process mirroring, predictive defect simulation, continuous Cpk tracking, and AS9100-aligned audit records generated automatically from the data your SMT line already produces.