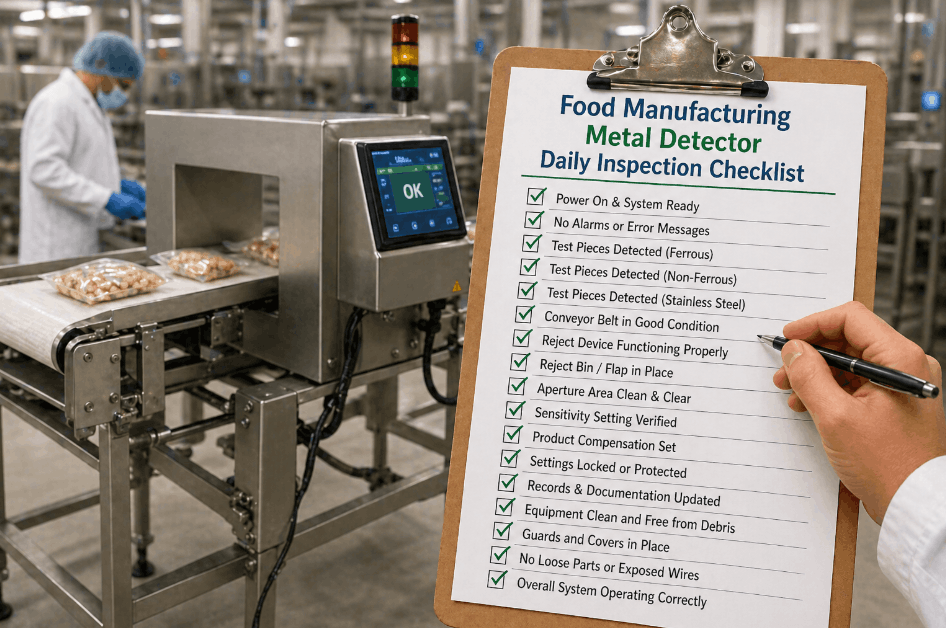
Daily testing of metal detectors and X-ray inspection equipment is a non-negotiable requirement for food safety compliance under HACCP, FSMA Preventive Controls, SQF, and BRCGS standards. When detection equipment fails to perform at validated sensitivity levels — or when test piece results go undocumented — your Critical Control Point (CCP) loses its verification backbone, exposing every product run to regulatory non-compliance and recall risk. A structured daily test checklist ensures every sensitivity check, reject mechanism test, and test piece result is captured with technician sign-off and timestamp. If your facility still relies on paper-based detection logs, book a demo to see how automated CCP compliance tracking eliminates documentation gaps across every inspection line.
1. Pre-Shift Equipment Readiness & Power-On Verification
Before any product enters the line, inspection equipment must be confirmed operational and running at validated settings. A pre-shift readiness check catches configuration drift, unauthorized setting changes, and hardware faults that would otherwise allow uninspected product to pass through the CCP undetected. Facilities managing multiple detection lines can book a demo to automate pre-shift equipment readiness verification and alert supervisors when a line is not cleared for production.
2. Test Piece Sensitivity Verification & Documentation
Sensitivity verification using certified test pieces is the core daily requirement for metal detector and X-ray CCP compliance. Every test must use the correct test piece size and type for the validated sensitivity standard, passed through the aperture in the correct orientation and position. Results must be recorded with time, test piece identity, pass/fail outcome, and technician name. Facilities running high-volume detection with multiple daily sensitivity checks can schedule a demo to digitize test result capture and automatically flag failures for immediate line hold action.
3. Reject Mechanism Function & Reject Bin Verification
Detection without effective rejection provides zero product safety protection. The reject mechanism — whether a pusher arm, air blast, diverter gate, or conveyor stop — must be tested independently of sensitivity to confirm it actuates correctly, ejects the full product, and deposits it into a secured reject bin. Reject mechanism failures are a frequent cause of contaminated product entering commerce despite a functioning detector. For facilities requiring digital reject event logging with automatic line hold triggers, book a demo to explore automated reject management workflows.
4. Product Effect Compensation & Phase Setting Verification
Product effect — the electromagnetic signal generated by conductive or high-moisture food products passing through a metal detector — is the primary cause of false rejects and inappropriate sensitivity reductions in food detection systems. Phase angle compensation settings must be validated for each product-packaging combination and confirmed daily before production. Incorrect phase settings mask true metal signals behind product effect suppression, reducing effective sensitivity below validated levels without triggering any equipment alarm. Facilities managing complex multi-SKU detection programs can book a demo to centralize product-specific detection settings and validation records in a single compliance system.
5. Mid-Shift & Product Changeover Sensitivity Re-Verification
Daily testing at shift start is the regulatory minimum — but detection equipment can drift in sensitivity during a production run due to temperature changes in the detection coil, electrical interference from nearby equipment, or mechanical vibration from the conveyor system. Mid-shift re-verification and mandatory re-testing at every product changeover are essential elements of a complete daily test program that demonstrates continuous CCP control throughout the production period.
6. End-of-Shift Test Documentation & CCP Sign-Off
End-of-shift testing closes the CCP verification loop for the production period. The final sensitivity test confirms the equipment maintained validated performance through the full shift, and the results — combined with all mid-shift tests — define the product hold scope in the event of a failure. Every daily test record must be reviewed and signed off by a designated CCP monitor before the shift record is closed. For facilities requiring supervisor-level CCP sign-off workflows with automatic escalation, book a demo to explore digital CCP compliance sign-off with timestamped authority trails.
7. X-Ray System Daily Performance & Image Quality Verification
X-ray inspection systems require additional daily checks beyond sensitivity testing — including beam intensity consistency, image quality, and detector array performance — that are not applicable to metal detectors. These checks verify the integrity of the X-ray imaging chain and confirm the system is operating within the validated image quality parameters that underpin the sensitivity claims in the CCP validation record.
8. Daily Test Record Management & Audit Readiness
Daily test records are the primary documentary evidence that your metal detector and X-ray CCPs functioned as designed throughout the production period. Under FSMA Preventive Controls, these records must be retained for a minimum of two years and must be retrievable on demand during regulatory inspections. Fragmented paper logs, incomplete entries, and missing sign-offs are among the most common documentation failures identified during FDA, USDA, and SQF inspections of food detection CCPs. Facilities transitioning from paper-based detection records to digital compliance tracking can book a demo to explore iFactory's CCP compliance tracking platform for food detection systems.