Industry surveys commonly place average OEE in pharmaceutical manufacturing at roughly 55 to 65 percent, well below the 85 percent often quoted as world class. The gap is rarely explained by slow machines. It sits in the losses that pharma plants have learned to accept: changeovers that include cleaning and line clearance, in-process checks, QA holds, material waiting for dispensing and batch records waiting for review. Most of these never appear in a headline OEE number, because the number is calculated in a way that hides them. Getting the calculation right on a tablet, capsule, blister or aseptic line is the first step to seeing where the capacity really goes. iFactory OEE Analytics applies one consistent method across every line, so the numbers can be trusted and compared.
iFactory OEE Analytics - Pharmaceutical Manufacturing
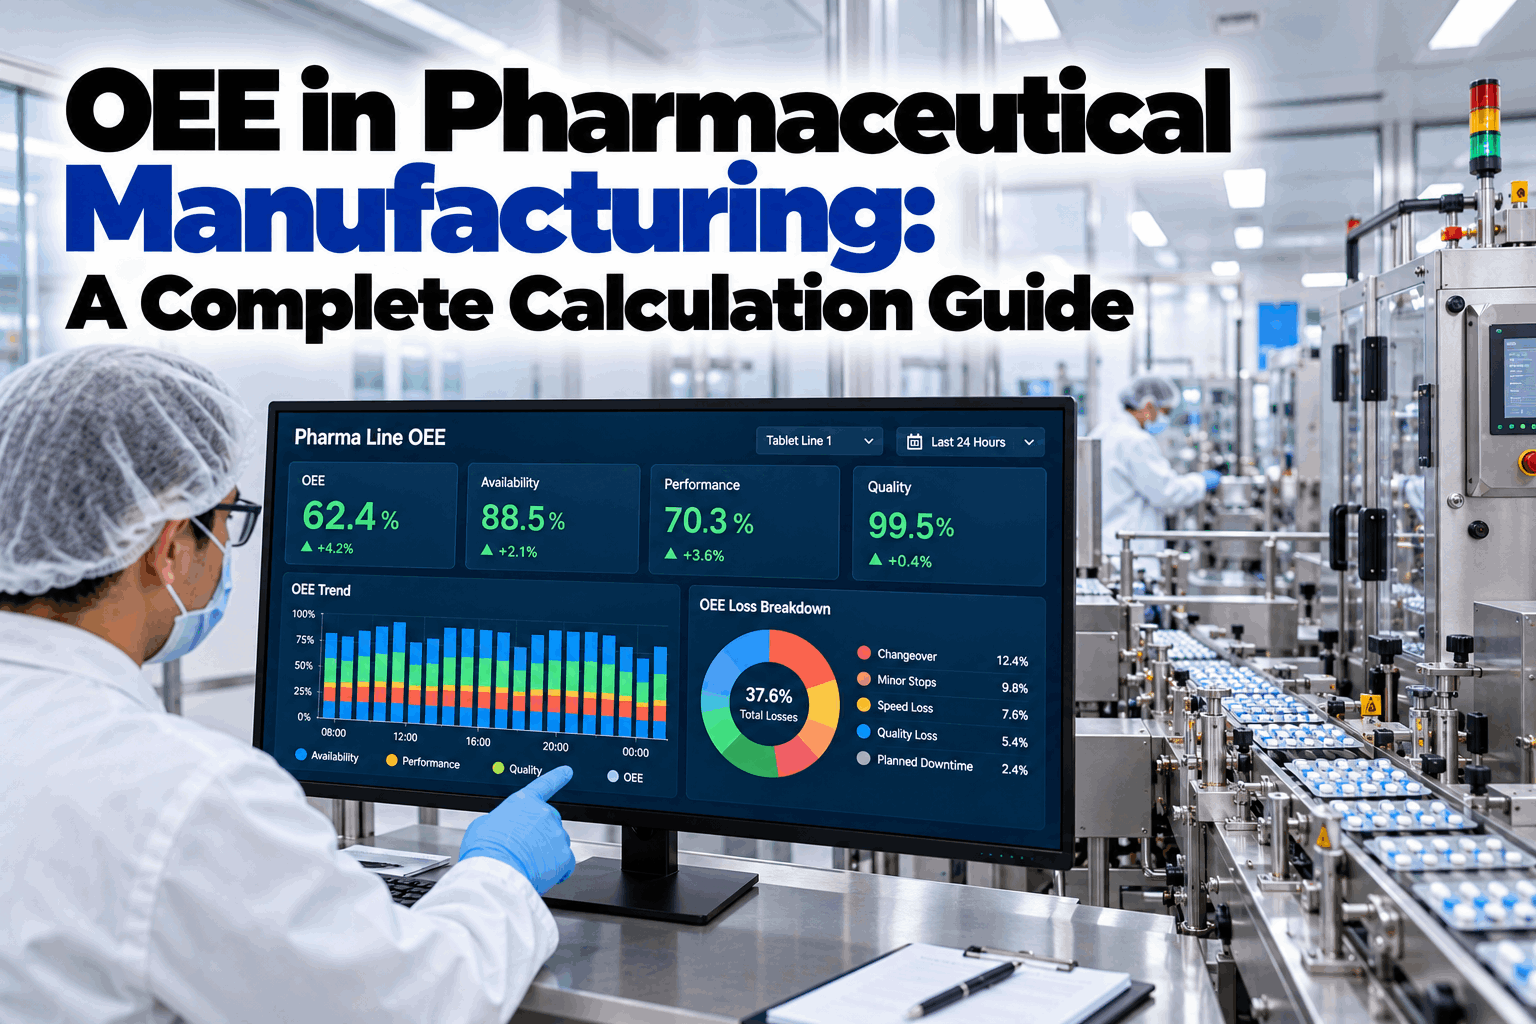
OEE in Pharmaceutical Manufacturing: A Complete Calculation Guide
How to calculate OEE on tablet, capsule, blister and aseptic lines, how to treat cleaning, line clearance and QA holds, and where the hidden losses really sit.
A x P x Q
availability, performance and quality multiplied into one figure
55-65%
commonly cited pharma OEE range; varies by source and definition
4 line types
tablet, capsule, blister and aseptic filling, each with its own losses
Hidden losses
changeover, cleaning and holds made visible instead of absorbed
Why OEE Is Harder to Calculate in Pharma
The OEE formula is the same in every industry. What differs is the set of decisions that sit behind each input. In pharma, six of them cause most of the disagreement and most of the distortion.
01
Planned or unplanned?
Cleaning, line clearance and cleaning verification are required, so many plants treat them as planned downtime. That removes the largest single loss from the OEE figure.
02
Which ideal rate?
Nameplate speed, validated speed and the speed in the batch record are often different. The choice moves the performance figure by many points.
03
What counts as good?
In-process samples, rejects, reworked units and product on QA hold are treated differently from plant to plant, which makes quality figures hard to compare.
04
Batches, not continuous runs
Production comes in batches with defined start and end points. Waiting before the batch starts and after it ends can be missed entirely.
05
Changeover is a regulated event
Changeover includes line clearance, cleaning, format parts, setup and release to run. Recorded as one block, its parts cannot be improved separately.
06
Data in separate systems
Machine signals sit in SCADA, batch data in MES or paper records and holds in the quality system. OEE built by hand from all three is slow and inconsistent.
The OEE Calculation Step by Step - A Blister Line Example
OEE equals Availability multiplied by Performance multiplied by Quality. The example below follows one 8-hour shift on a blister packing line, with illustrative numbers, so each input can be traced.
1
Set planned production time
Start with the shift length and subtract genuinely planned stops such as scheduled breaks. Be explicit about what is excluded, because every exclusion removes a loss from view.
Example: 480 min shift - 40 min breaks = 440 min
2
Calculate Availability
Run time divided by planned production time. Subtract changeover and breakdown time from planned time to get run time.
Example: 440 - 55 changeover - 25 breakdown = 360 min; 360 / 440 = 81.8%
3
Calculate Performance
Actual output divided by the output the line would produce at its ideal rate over the same run time. Slow running and minor stoppages reduce it.
Example: 60,000 made / (360 min x 200 per min = 72,000) = 83.3%
4
Calculate Quality
Good units divided by total units made. Define in advance how rejects, rework, samples and held product are counted.
Example: 57,000 good / 60,000 made = 95.0%
5
Multiply for OEE
Multiply the three results. The same figure can be checked directly by dividing good units by the output possible in planned time at the ideal rate.
Example: 81.8% x 83.3% x 95.0% = 64.8%; 57,000 / 88,000 = 64.8%
OEE Across Pharma Line Types - Where the Hidden Loss Sits
Each line type loses capacity in a different place. The table shows an illustrative result for four lines, and the biggest hidden loss on each. The values are examples for explanation and are not benchmarks.
Line type
Availability
Performance
Quality
OEE
Biggest hidden loss
Tablet compression
84%
88%
97%
72%
Cleaning between products
Capsule filling
80%
85%
98%
67%
Minor stoppages at the filling station
Blister packing
82%
83%
95%
65%
Changeover, format parts and line clearance
Aseptic vial filling
72%
80%
96%
55%
Setup, interventions and in-process holds
Plant view
-
-
-
55-72%
A single plant figure hides a 17-point range
Calculating OEE by Line Type
The method stays the same, but the ideal rate, the hidden losses and the quality count differ on each type of line. These are the points to settle before a line's OEE is trusted.
Tablet and capsule
Ideal rate
Validated machine speed for the product, such as tablets per minute for the press or capsules per minute for the filler
Hidden loss
Product changeover with full cleaning, tooling change and weight or fill adjustment
Quality count
Rejects from weight, hardness and fill checks, plus start-up product that is discarded
Blister and packaging
Ideal rate
Validated cycles per minute for the format, multiplied by pockets per cycle
Hidden loss
Format changeover, foil and PVC reel changes, and minor stoppages from feeders and cartoners
Quality count
Seal failures, missing tablets and print or code rejects found by vision or checkweighing
Aseptic filling
Ideal rate
Validated filling speed for the container, within the qualified process
Hidden loss
Setup, interventions, environmental monitoring holds and waiting for upstream steps
Quality count
Fill volume rejects, particulate and closure defects, with held product recorded separately
Want your own lines calculated this way? Book a demo - bring a week of downtime and output records for one line and we will calculate OEE and rank the losses.
How iFactory Calculates OEE Consistently - Five Stages
The platform applies one method across every line, with the definitions agreed with your team before any number is reported.
01
Capture
Machine signals, batch data and operator entries gathered per line.
02
Define
Planned time, ideal rate and quality rules agreed and applied the same way on every line.
03
Calculate
Availability, performance and quality worked out for each line and shift.
04
Attribute
Every lost minute and unit assigned to a cause, with changeover broken into its parts.
05
Improve
Losses ranked by size, so effort goes to the largest first.
What a Consistent Pharma OEE Method Delivers
The benefit is a number your teams trust, and a clear view of where capacity is lost.
One method
Every line, same rules
figures that can be compared across lines and sites
Ranked losses
Biggest first
by minutes and units, not by opinion
Visible changeover
Parts, not a block
clearance, cleaning and setup measured separately
Traceable
Back to source data
every figure linked to its records
Frequently Asked Questions
Should cleaning and line clearance count as planned downtime?
Plants make different choices, and both can be defensible. What matters is that the choice is documented and applied consistently. Because cleaning and clearance are often the largest losses in pharma, we recommend tracking them as their own category even when they are classed as planned, so they stay visible and can still be improved.
Which ideal rate should we use?
Use the speed the equipment is validated to run at for that product and format, not an unvalidated figure above it. If the batch record specifies a lower speed for a product, note the difference, because it changes how performance should be read. Whatever you choose, apply it the same way each time.
How should rework and held product be counted in Quality?
The usual approach is to count only units that are good on the first pass as good output. Reworked units, rejected units and product on hold are counted separately, so the cost of quality problems is visible. Product released after a hold can be added back, provided the rule is agreed beforehand.
Is a 55 to 65 percent OEE actually poor?
Not necessarily. Published averages depend on how each source defines planned time and which losses it includes, so comparing your figure with a headline benchmark can mislead. A more useful comparison is each line against its own baseline and against its best demonstrated performance.
Stop reporting one OEE number for the whole plant.
See Pharma OEE Calculated Line by Line on Your Own Data
Bring a week of downtime and output records for a tablet, capsule, blister or aseptic line. We will calculate OEE the consistent way and show where the hidden losses sit.