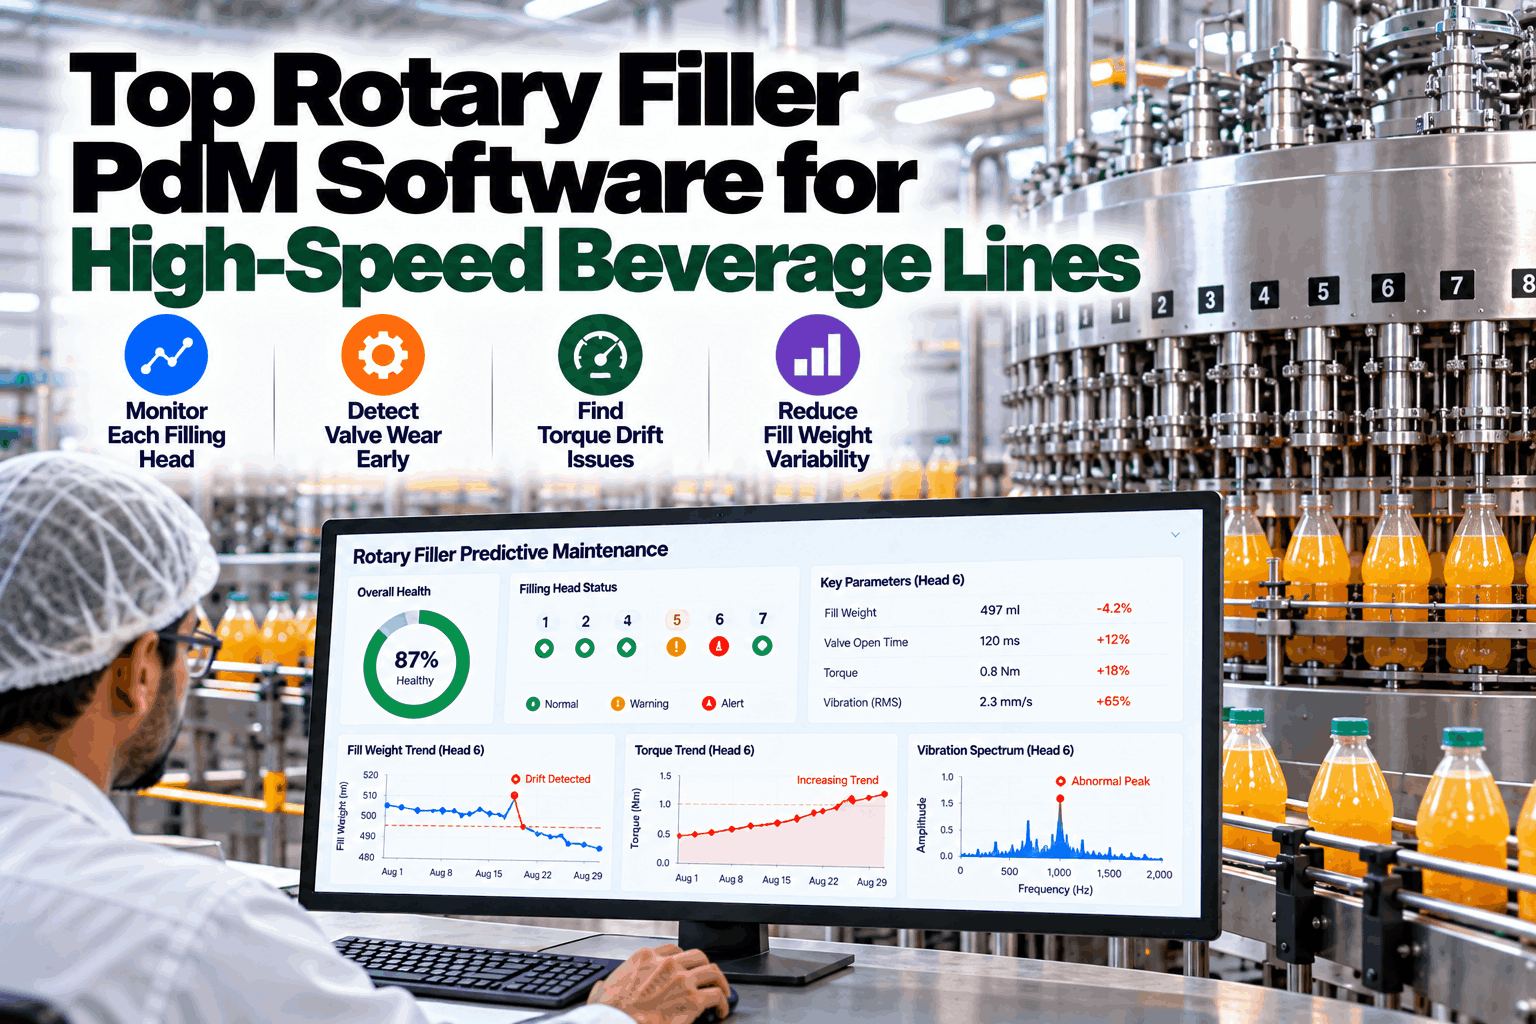
On a high-speed rotary filler, one worn valve can hide in plain sight. The line keeps running at full speed, the average fill looks fine, and yet every fortieth or eightieth container, always from the same position on the turret, is underfilled, foaming or capped at the wrong torque. By the time the checkweigher reject rate climbs, thousands of containers have gone through. Head-by-head predictive maintenance fixes that by tracking every filling valve and capping head as its own asset, so valve wear, torque drift and fill variability are caught at the first sign. This guide explains how it works on fast beverage lines, and a walkthrough shows it on real data.
Rotary Filler Predictive Maintenance for High-Speed Beverage Lines, Head by Head
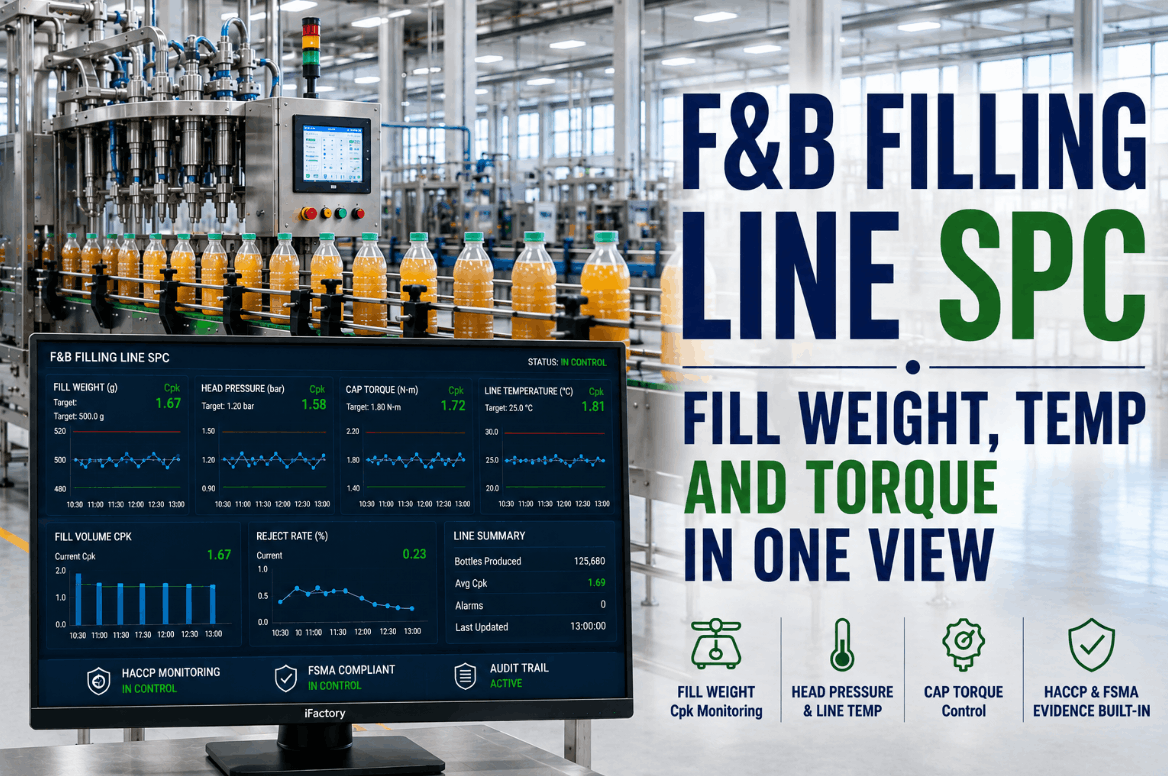
Every filling valve and capping head tracked as its own asset, so one drifting position is found in minutes, not after a shift of rejects.
Why Rotary Filler Failures Are Different
A rotary filler is not one machine; it is dozens of identical machines on one turret. Each filling valve, lift cylinder and capping head wears at its own rate. When one of them drifts, the average hides it. A single valve running slightly slow or leaking slightly will underfill or overfill one container per turret revolution, which is invisible in line-level averages but perfectly visible when the data is sorted by position.
Speed makes the stakes higher. Krones reported a line in Sydney commissioned in October 2025 filling up to 100,000 PET bottles per hour with two fillers in tandem. At that rate, a line runs through 1,667 containers every minute. A problem that takes an hour to notice has already touched 100,000 containers. Plants weighing up head-level monitoring can ask our team what data their filler already produces.
Head-by-Head Monitoring Explained
The key is to tag every container with the valve and capping head that handled it. Turret position from the machine encoder, together with the shift register the filler already uses for reject timing, makes this possible without new mechanics. Once each measurement carries a head number, the analytics can build a statistical profile for every valve and every capping head.
| Data source | Per-head metric | What a drift usually means |
|---|---|---|
| Fill level inspection or checkweigher | Mean and spread of fill per valve | Valve wear, sticking, dirty vent tube, damaged seal |
| Flowmeter or fill-time data (volumetric fillers) | Fill time and volume per valve | Valve response slowing, flowmeter drift, partial blockage |
| Capper servo or torque data | Application torque curve per head | Chuck insert wear, clutch slip, spindle bearing wear |
| Cap and closure inspection | Cocked or high caps by head | Chuck misalignment, cap feed issues at a position |
| Reject and jam logs | Rejects and jams by position | Star-wheel wear, pocket damage, timing drift |
| Drive and turret signals | Motor current, vibration, lubrication | Bearing wear, lift cam and follower wear |
Most modern fillers already log enough to start. Where they do not, a few added signals close the gap, which our engineers confirm during scoping.
The Signals That Catch a Drifting Valve Early
Per-valve fill statistics are the earliest and most useful signal. A valve whose mean fill moves a few millilitres, or whose spread widens, is telling you its seal, vent tube or actuation is changing. Fill time on volumetric fillers is similar: a valve that takes a little longer each day to deliver the same volume is slowing down mechanically.
Capping torque curves carry their own early warning. A servo capper records the torque profile for every closure. When a chuck insert wears, the peak torque drops or the curve shape changes on that head alone, long before loose caps show up in the field. Seeing these per-head views on your own line takes a short demo.
Fill Weight Variability, Giveaway and Net Contents
Fill accuracy is a financial and regulatory question at the same time. In the United States, NIST Handbook 133 sets out how inspectors check the net contents of packaged goods. The average quantity of a lot must at least equal the labelled quantity, and individual packages must not fall short by more than the maximum allowable variation. In Europe, the average quantity system behind the e-mark works on similar principles.
Plants protect themselves by overfilling a little, which is giveaway, product shipped for free. A single drifting valve forces the whole line target up to keep that position compliant. Fixing the valve lets the target come back down.
Illustrative figures; your container size, speed and product value decide the real number. We can run it with your own data.
Capping Torque Drift and Closure Integrity
Closure problems are among the most expensive quality escapes on a beverage line: leaking products, loss of carbonation, tamper-band failures and consumer complaints about caps that will not open. Most start as gradual torque drift on one or two capping heads. Magnetic clutches weaken, chuck inserts wear, and spindle bearings add friction.
A falling peak on one head points to clutch or chuck insert wear. A rising, noisy profile points to spindle friction.
Removal torque tests carry the head number, so lab results and machine data agree on which head is drifting.
High or cocked caps concentrated on one head usually mean alignment or chuck damage, not a cap supply issue.
Linking torque, inspection and lab removal results by head turns closure quality into a maintenance signal. Our support team can show how the three data sets line up.
Drives, Turrets, Cams and Star-Wheels
Beyond valves and capping heads, the mechanical backbone of the filler needs attention too. The main drive and turret bearing carry the whole rotating mass. Lift cams and followers raise and lower containers thousands of times an hour, and star-wheels and transfer pockets take the impacts of every container entering and leaving.
| Asset | Failure mode | Signal | Typical action |
|---|---|---|---|
| Main drive and gearbox | Gear and bearing wear | Vibration, motor current, oil temperature | Plan gearbox inspection at next shutdown |
| Turret slewing bearing | Wear, lubrication breakdown | Drive torque trend, vibration, grease condition | Adjust lubrication, schedule bearing inspection |
| Lift cams and followers | Follower wear, cam track damage | Vibration spikes at fixed angles | Replace followers on affected positions |
| Star-wheels and guides | Pocket wear, timing drift | Jam rate and reject position patterns | Replace worn parts, re-time transfer |
| Product and CO₂ supply | Pressure instability | Bowl level and pressure variation | Check regulators and supply valves |
These assets fail slowly, which gives weeks of warning if anyone is watching. Setting up that watch list is part of our pilot program.
From Per-Head Alert to Fixed Position
A valve or head moves outside its learned band for long enough to count, and the alert names the exact position.
Fill deviation plus fill time, or torque plus cap inspection, raises confidence before anyone stops the line.
Isolate the valve if the filler supports it, adjust the target, or plan the repair for the next changeover.
The work order lists the valve number, the likely part and the evidence.
The position returns to the line’s statistical profile, and the alert closes.
See how these alerts would look on your filler in a guided session.
How iFactory Solves Rotary Filler Reliability
Every measurement carries its valve and capping head number from encoder and shift-register data.
Fill mean, spread, fill time and torque profiles learned for each position.
Line targets and overfill cost linked to the positions that force them up.
Drive, turret, cam and star-wheel health from vibration and current.
Alerts name the position, likely part and confidence, with evidence attached.
Work orders planned into changeovers, with verification after repair.
It works across filler brands, because it reads the data the machine already produces. Ask our specialists about your model.
Find the Drifting Valves on Your Filler
Share a week of fill, torque and reject data with position numbers. We show which valves and heads are drifting, what they cost in giveaway and rejects, and when to fix them.
Fill height runs low once per turret revolution while every other valve holds target. The pattern points to one valve seal.
How Deployment Works
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the filler and capper models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensor and PLC/SCADA integration, cabling and network setup, operator and technician training, and 24×7 remote monitoring.
Server installed, sensors and controllers connected, historical work orders and failure history loaded.
Baselines learned per asset, alerts piloted on the first line with your maintenance team reviewing every finding.
Rollout to the agreed assets, technician training, CMMS hand-off and 24×7 remote monitoring in place.
The first month usually focuses on getting position numbers attached to every measurement: encoder position, shift-register data and inspection results aligned so each reading carries its valve and head. Once that mapping is proven against a few deliberate test containers, the per-position statistics build quickly, and historical data from the previous weeks can often be replayed to show which positions were already drifting before go-live.
Most beverage plants start with their fastest or most troublesome filler, then add the blower, labeller and packer on the same line. The rollout order is agreed on a scoping call.
Frequently Asked Questions
Every container is tagged with the filling valve and capping head that handled it, so fill, time, torque and reject data can be analysed per position. A single drifting valve then stands out instead of being averaged away. See it in a live demo.
Per-valve fill mean and spread, and fill time on volumetric fillers, usually move first. Capping torque profiles are the equivalent early signal for capping heads. Our engineers can check what your filler logs.
When one valve underfills, the whole line target is raised to keep that position compliant. Finding and fixing the valve lets the target return to normal, cutting overfill across every container. Ask for a giveaway estimate.
It describes how net contents are checked: a lot’s average must at least equal the labelled quantity, and individual packages must not be short by more than the maximum allowable variation. Your quality team applies the details for your products. Our team can link fill data to those checks.
Yes, in most cases. It uses encoder position, shift-register data, inspection results and servo data the filler already produces, plus vibration and current where needed. Confirm your model with a quick call.
Per-position analysis can often start from historical data in the first weeks. Typical programs go live in 6–12 weeks. Plan it with our support team.
Every Valve and Every Head, Watched Individually
iFactory finds the one drifting position on your turret before it becomes a shift of rejects, giveaway or loose caps, and plans the fix into your next changeover.
Each valve and head is scored separately, so one weak position stands out from the average.