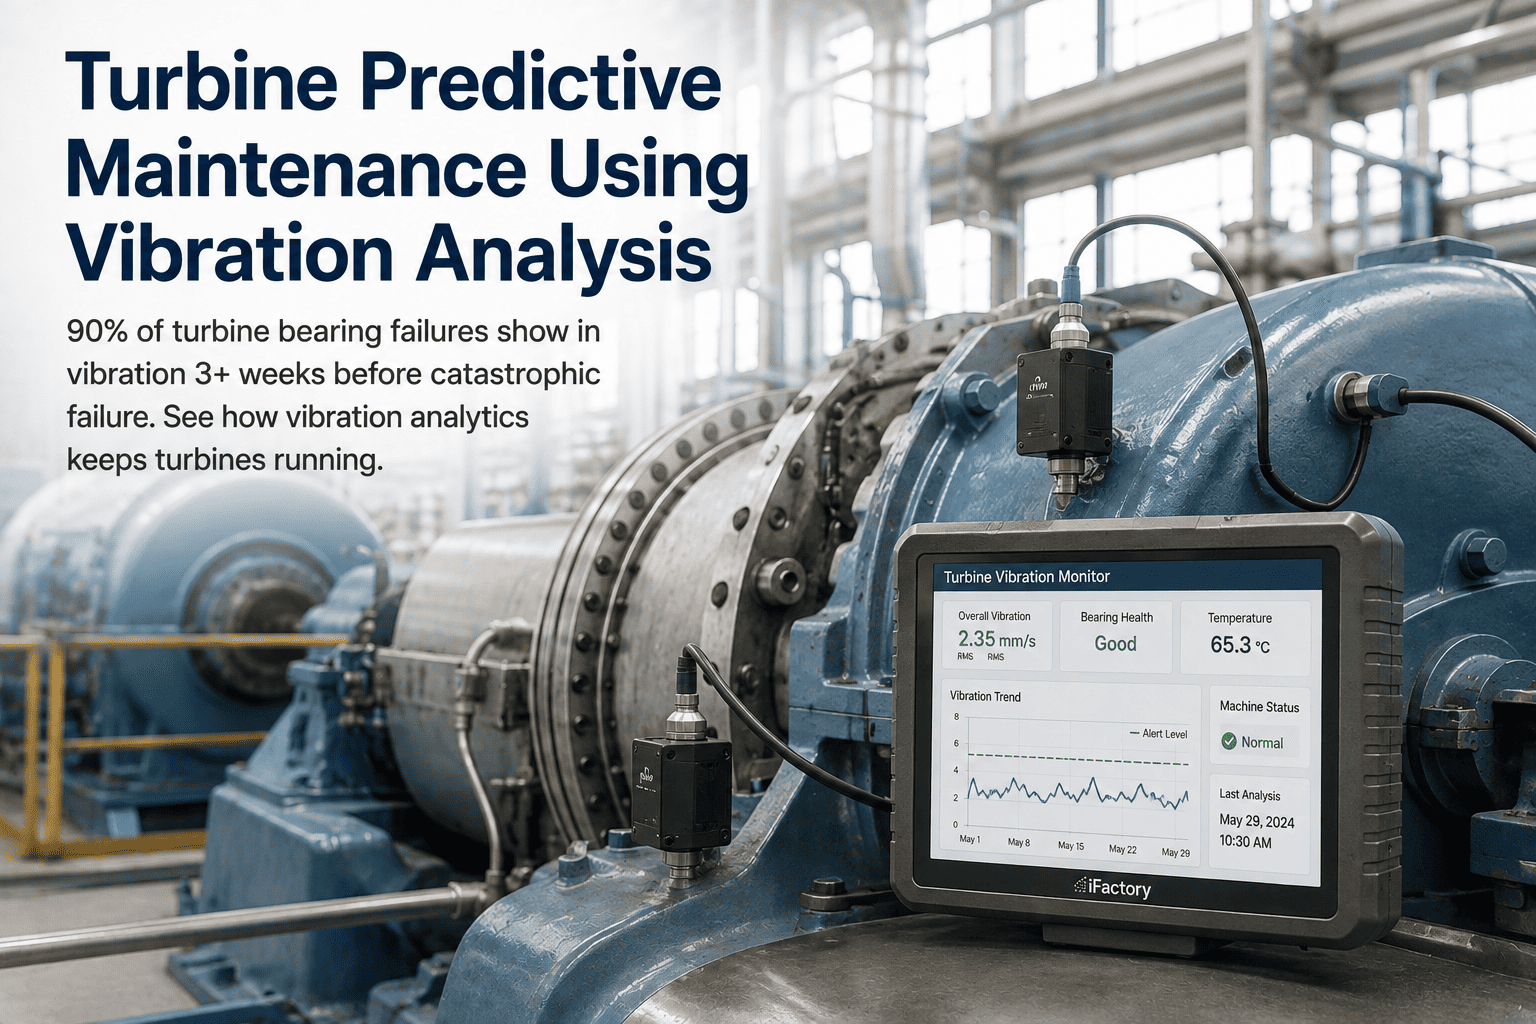
A steam turbine rarely fails without warning — it fails without anyone reading the warning. The vibration signal is almost always there, showing up as a slow creep in overall level, a shift in the 1× component, a widening cyclical pattern between overhauls. But the traditional threshold alarm is deaf to all of it: it only fires when the reading actually crosses the ISO 20816 Zone C boundary, which is often days or weeks after the bearing, rotor, or coupling started degrading. By then the options are compressed — trip the machine, or roll the dice. SPC on turbine vibration data changes that math. It puts control limits, warning bands, and pattern rules on top of the same accelerometer and proximity probe data you already collect, so a drift from Zone A into Zone B gets flagged as a signal rather than tolerated as "still within limits." iFactory vibration analytics is built around exactly that shift.
iFactory SPC for Turbine Vibration
Catch Bearing and Rotor Faults Weeks Before the Trip Level Hits
Layer control charts and pattern rules on your existing vibration monitoring — so slow drifts inside ISO 20816 Zone A/B get investigated instead of ignored.
A vibration alarm is a single number. ISO 20816 gives you Zone A (good), Zone B (acceptable long-term), Zone C (short-term only), and Zone D (damage risk) — but a threshold alarm only fires when you cross into Zone C or worse. Every problem that develops inside Zone A or Zone B is invisible to it, even when the trend is unmistakable. This is what SPC sees that the alarm doesn't.
Zone D
> 7.1 mm/s
Damage risk — trip level
Zone C
4.5 - 7.1 mm/s
Short-term operation only — alarm level
Zone B
2.8 - 4.5 mm/s
Acceptable for long-term operation
Zone A
< 2.8 mm/s
New commissioning target
A real turbine drift, 90 days
The alarm didn't fire until Day 68. SPC flagged the same drift on Day 42 — 26 days of runway to plan the outage instead of forcing it.
What the Vibration Actually Tells You
The overall vibration level is a summary. The real diagnostic value is in the frequency components — because a rising 1× tells you something completely different from a rising 2× or a broadband floor. SPC works on all of them at once.
1×
Running Speed
Imbalance
A slow rise in the 1× component is the classic signature of thermal bow, blade fouling, or lost balance weights. Steady, load-linked, and usually the first thing SPC catches.
2×
Twice Running Speed
Misalignment
A growing 2× peak — especially with an axial component — points at coupling misalignment or a shifting foundation. Often appears after an outage or a thermal cycle.
0.5×
Sub-Synchronous
Oil whirl / Rub
Sub-synchronous energy showing up is one of the most dangerous signals on a fluid-film bearing — oil whirl, whip, or an intermittent rotor rub. SPC flags it as a step change immediately.
Broadband
Bearing Frequencies
Bearing damage
A rising broadband floor — or new peaks at ball-pass frequencies — signals bearing wear, brinelling, or contamination. Weeks of warning if you're trending it.
Want SPC running on your own 1×, 2×, and broadband streams? Book a demo and we'll plot 90 days of your trend against control limits.
Threshold Monitoring vs. SPC on Vibration
Same accelerometers, same proximity probes, same DCS. What changes is what happens with the data — and that changes when you find out something is wrong.
Threshold-only
Waiting for the Trip
One alarm line — set at Zone C entry
Drift inside Zone A/B is invisible
Alarm fires days from potential damage
Forced outage — no time to plan
Root cause investigated after the fact
iFactory SPC on Vibration
Catching the Drift Weeks Earlier
UCL / LCL from the machine's own baseline
Drift inside Zone A/B triggers a signal
26+ days of warning is typical
Planned outage window instead of forced trip
Root cause investigation runs in parallel with runtime
The Pattern Rules That Do the Work
On vibration data, four pattern rules do most of the diagnostic lifting — and each one maps to a real failure mode that develops well below the alarm line.
Maps to: rising 1× on rotor, rising broadband on bearings
RuleStep Change in Mean
A sustained shift after a startup, load change, or maintenance event. New baseline, new problem.
Maps to: misalignment after outage, oil whirl onset, rotor rub
RuleWidening R-Chart
The range between highs and lows opens up. The machine is becoming less stable even if the mean hasn't moved yet.
Maps to: intermittent rub, developing crack, coupling backlash
RulePoints Hugging UCL
Two of three points inside the warning band. Not yet an alarm, but the process has clearly moved and is asking for attention.
Maps to: early bearing degradation, blade fouling building up
How iFactory Closes the Loop
SPC on vibration is only useful if the signal reaches a work order — otherwise it is another trend nobody reads. iFactory routes every fired rule to a specific inspection playbook with an owner and a deadline.
A
Baseline Learning
30–60 days of steady-state readings define the machine's real UCL, LCL, and warning band — per bearing, per speed condition.
B
Live Trending
Overall level, 1×, 2×, 0.5×, and broadband streams are trended continuously against the baseline in a single view.
C
Rule Engine
Nelson and Western Electric rules fire on drifts, shifts, trends, and warning-band clusters across every stream.
D
Playbook Routing
A rising 1× goes to balance check. A step-change in 2× goes to alignment. Sub-sync goes to bearing inspection.
E
Verify Return to Baseline
After the fix, the chart confirms the mean and R returned to Zone A — the CAPA closes with statistical proof.
What Catching Drift Early Delivers
Turbine vibration is one of the highest-consequence signals in the plant. Every week of warning bought converts directly into planned maintenance instead of forced outage, and into avoided damage that would otherwise cascade.
Weeks
Earlier warning
on bearing and rotor drifts
Planned
Outages
instead of forced trips at Zone C
Zone A
Held longer
by acting on drifts before they escalate
ISO
20816 aligned
records and thresholds match the standard
Curious how many recent trips would have been called weeks earlier? Talk to our reliability team — we'll replay your history against SPC rules.
Frequently Asked Questions
We already have ISO 20816 thresholds — why layer SPC on top?
Because ISO 20816 thresholds fire at the Zone B/C or Zone C/D boundary — by which time you're usually looking at a trip and a forced outage. SPC works on the same readings inside Zone A and B, catching a drift while the machine is still healthy on paper. The thresholds still do their job as the last line of defense; SPC gives you the early-warning layer weeks upstream.
Does this need new sensors on the turbine?
No. iFactory reads the accelerometer and proximity probe data your monitoring system already provides — Bently Nevada 3500, EMERSON CSI, ABB, or the OEM supervisory system — and adds the SPC layer on top. The physical instrumentation stays exactly as it is.
Which SPC rules make sense for turbine vibration?
The standard Nelson and Western Electric rules translate well: 7-point rising trends, sustained shifts of nine or more points on one side of the mean, widening R-chart range, and two-of-three points in the warning band. Each one maps to a specific failure mode — imbalance, misalignment, developing rub, bearing wear — and that mapping is what turns a chart pattern into a work order.
How does this handle load changes and speed variation?
By computing the baseline per operating condition, not as one global number. The UCL and LCL for full-load, 3000 rpm, steady-state are different from those for a load ramp — and iFactory treats them separately. That prevents the very common trap of a "normal" load-change transient triggering false alarms while a real drift at steady state gets missed.
Can we see this running on our own data?
Yes. Bring one turbine, one bearing, and 60–90 days of trend history. We'll compute your real baseline, run the SPC rules against the data, and show exactly which drifts would have been flagged and how many days ahead of the actual alarm. Book a demo and we'll walk it through.
Stop reacting at the trip level.
See SPC Running on Your Own Turbine Data
Bring one machine and one 90-day trend. We'll build your baseline, plot the ISO 20816 zones, run the pattern rules on your actual readings, and show every drift SPC would have flagged before threshold monitoring caught it.