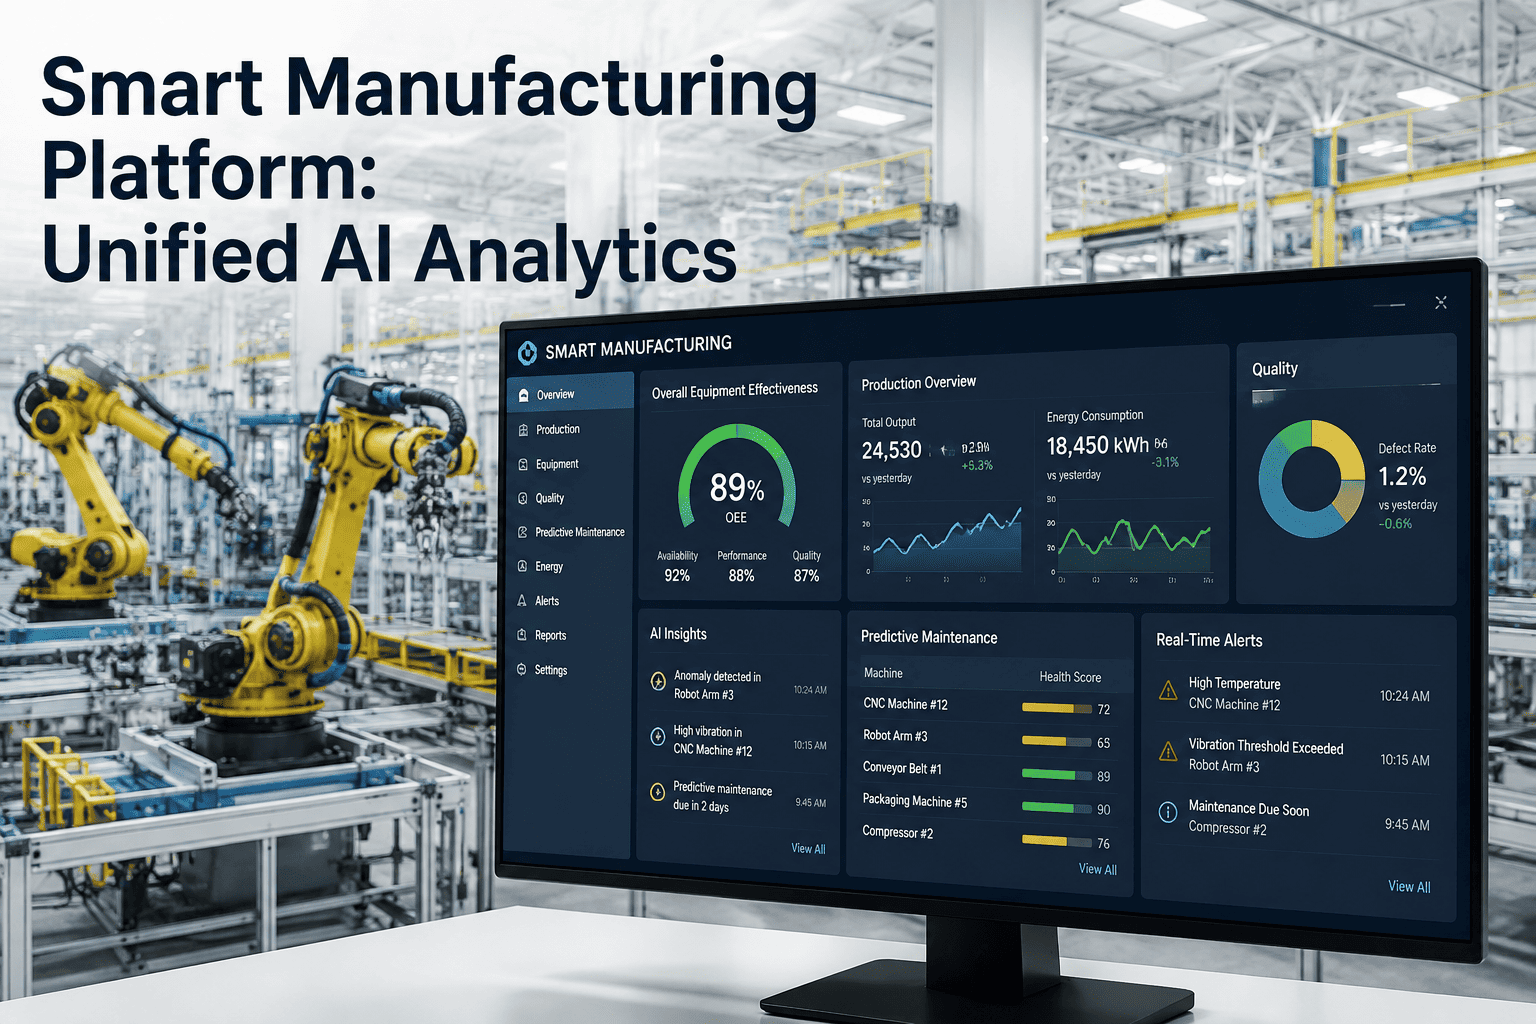
Energy waste in a manufacturing plant rarely comes from one single source, it accumulates across machine-level inefficiency, peak demand spikes, compressed-air leaks, motor degradation, fuel consumption and process inefficiencies that each quietly add a little to the total bill. Without a structured way to check all of these areas together, plants tend to focus on whichever one is most visible, while the others continue unaddressed. A checklist that puts every area on the table at once is what actually reveals where the biggest opportunity sits, and our team can help you work through this checklist against your own plant.
Manufacturing energy optimization
Put Every Source of Energy Waste on the Same Table at Once
iFactory AI helps you work through machine-level waste, peak demand, motor efficiency, compressed air, fuel and process inefficiencies side by side.
Why checklists help
The Most Visible Energy Problem Is Not Always the Biggest One
A plant tends to focus energy improvement effort on whatever problem was most recently discussed or most visible on a bill, which means quieter sources of waste, like a slow compressed air leak or a motor running inefficiently, can go unaddressed indefinitely.
One area gets attention
The most recently discussed issue gets the focus
Other areas go unchecked
Quieter sources of waste continue unnoticed
No comprehensive view
Nobody has looked at every area together
Biggest opportunity missed
The largest saving potential may sit in an area nobody reviewed
The checklist
Six Areas Every Energy Review Should Cover
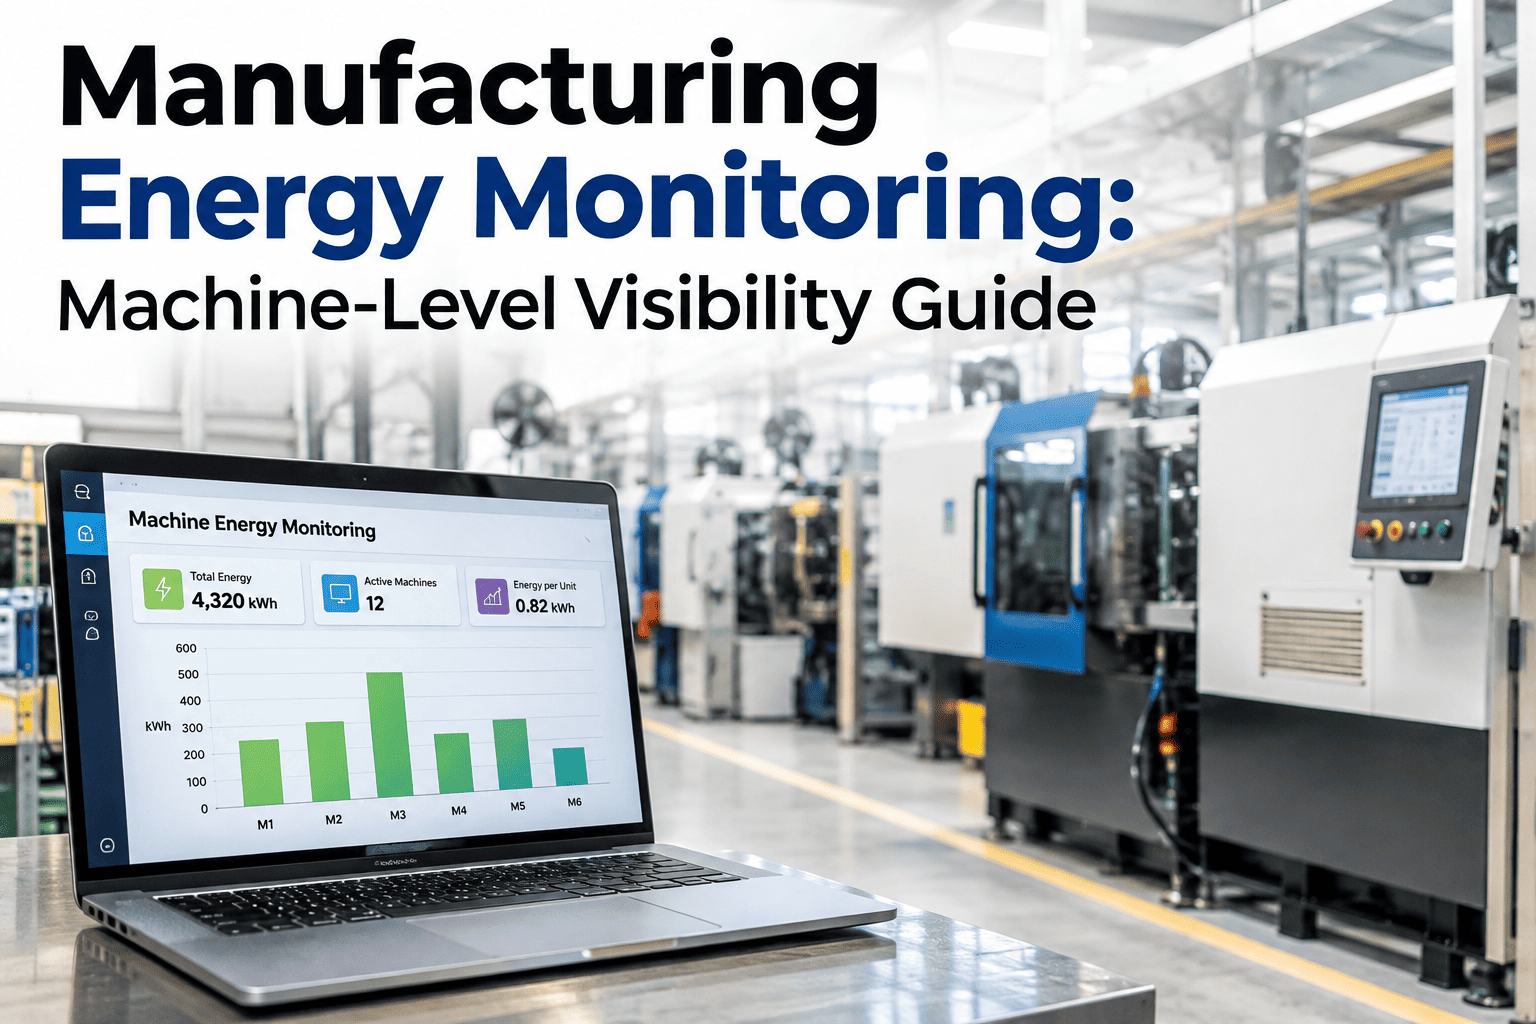
Machine-level energy consumption mapped across the plant
Peak demand pattern reviewed against your utility rate structure
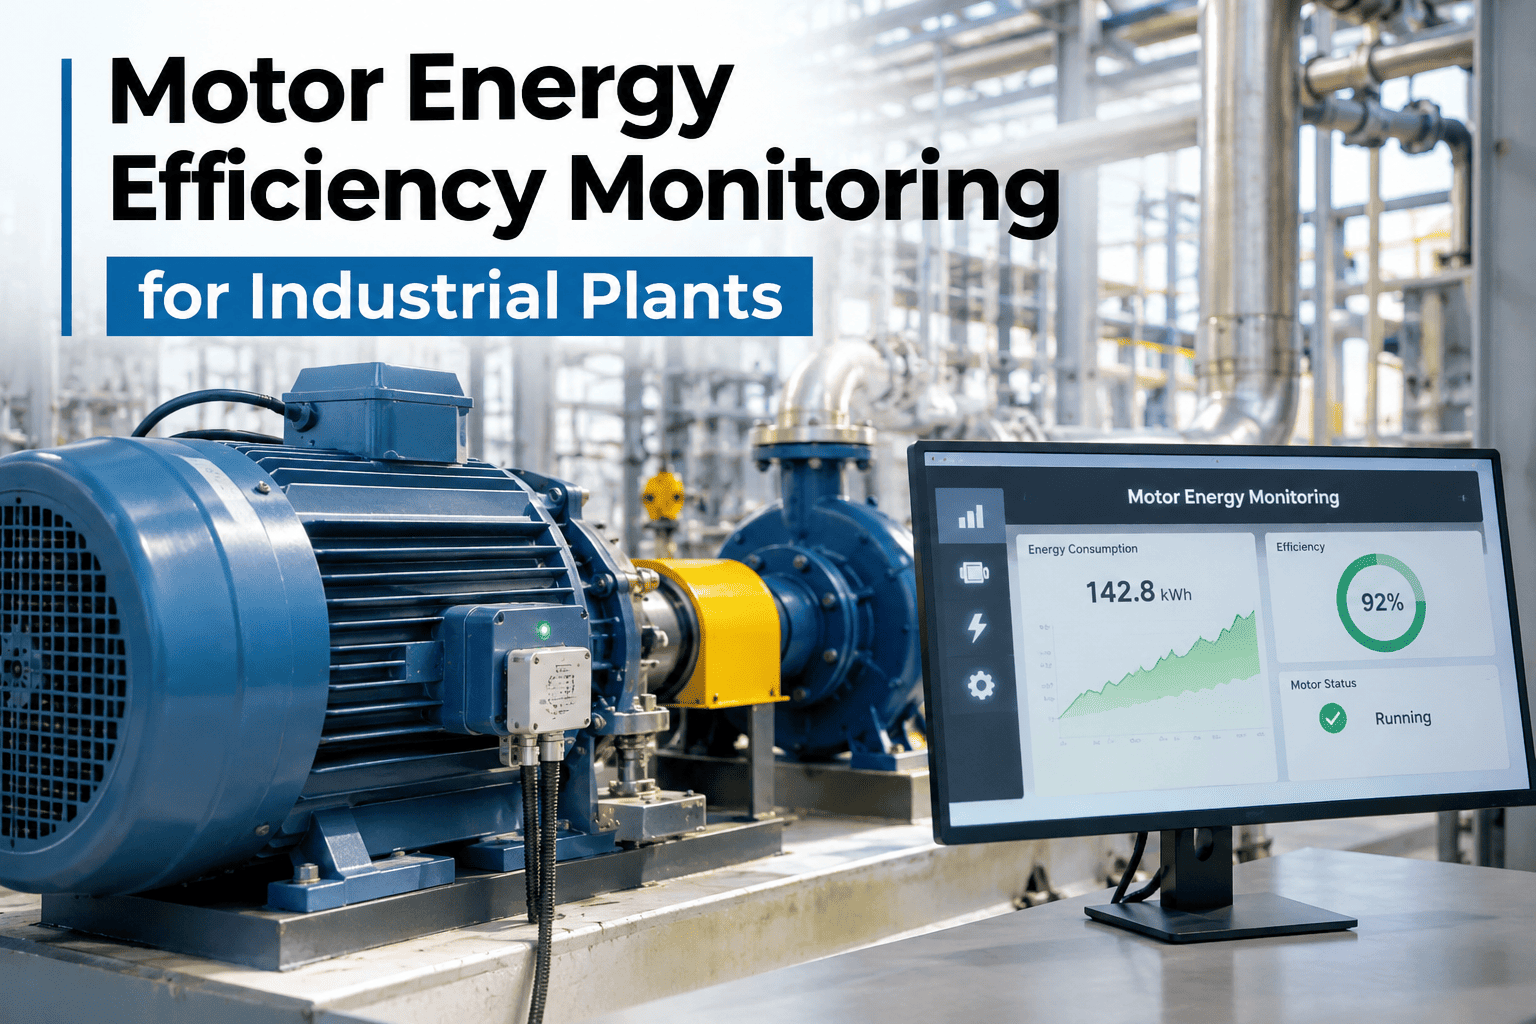
Motor current monitored against expected baselines
Compressed air system checked for leaks, including off-hours usage
Fuel consumption tracked against production output
Process-level inefficiencies identified by production step
Work Through This Checklist on a Call
Share where your plant currently stands on each area and get a prioritized view of where to focus first.
Prioritization table
Matching Each Area to a Starting Signal
| Area | Sign it needs attention | Typical first step |
|---|
| Machine-level consumption | No breakdown exists below the plant meter | Sub-meter your highest-consumption equipment |
| Peak demand | Demand charges make up a large share of the bill | Identify the timing of recent peak events |
| Motor efficiency | No baseline current data for key motors | Establish baselines for highest-horsepower motors |
| Compressed air | No off-hours usage data reviewed | Check compressor activity during a planned shutdown |
| Process inefficiency | Energy per unit has never been tracked by process | Set up energy-per-unit tracking for your most energy-intensive step |
Common pitfalls
Three Mistakes With Energy Optimization Checklists
1
Reviewing the checklist once and never again
Energy patterns shift as equipment ages and production changes, so a one-time review goes stale.
2
Focusing only on areas with existing data
Areas without current monitoring get skipped simply because they are harder to assess.
3
No clear owner for each area
A checklist without assigned follow-up rarely leads to actual change.
Expert review
The areas with no existing data are often exactly where the checklist matters most, since the absence of data is itself a sign nobody has checked. A thorough review treats a blank answer as a priority, not a reason to skip that line.
Watch for
A checklist review that skips areas simply because no monitoring currently exists there.
Do next
Treat every blank or "not sure" answer on the checklist as a candidate for the next investigation, not a low priority.
— iFactory energy specialists
Frequently asked questions
What Plants Ask About This Energy Checklist
Do we need monitoring in place before we can use this checklist?
No, the checklist itself is meant to reveal where monitoring is missing, so a plant with no monitoring at all can still use it to identify which area to instrument first.
Ask about starting from scratch.
How often should this checklist be revisited?
A quarterly or semi-annual review keeps the checklist aligned with changes in equipment, production mix and utility rates, rather than relying on a single assessment that can go stale within months.
Discuss a review cadence.
Who should be involved in going through the checklist?
Input from facilities, maintenance and production teams gives a more complete picture than any one department alone, since each sees a different part of the plant's energy use.
Talk through who to involve.
What if several areas all look like they need attention?
Prioritizing based on which area is easiest to get data on quickly, combined with where the likely cost impact seems largest, is a reasonable way to sequence investigation when multiple areas are candidates.
Ask about sequencing your priorities.
Can this checklist apply across multiple plants in the same company?
Yes, running the same checklist at each site often reveals that different plants have different priority areas, even within the same company, which helps target investment where it is actually needed.
Discuss a multi-plant rollout.
From scattered attention to a complete picture
Find Your Plant's Biggest Energy Opportunity, Not Just the Loudest One
Book a session with iFactory AI to work through this checklist and build a prioritized energy improvement plan.