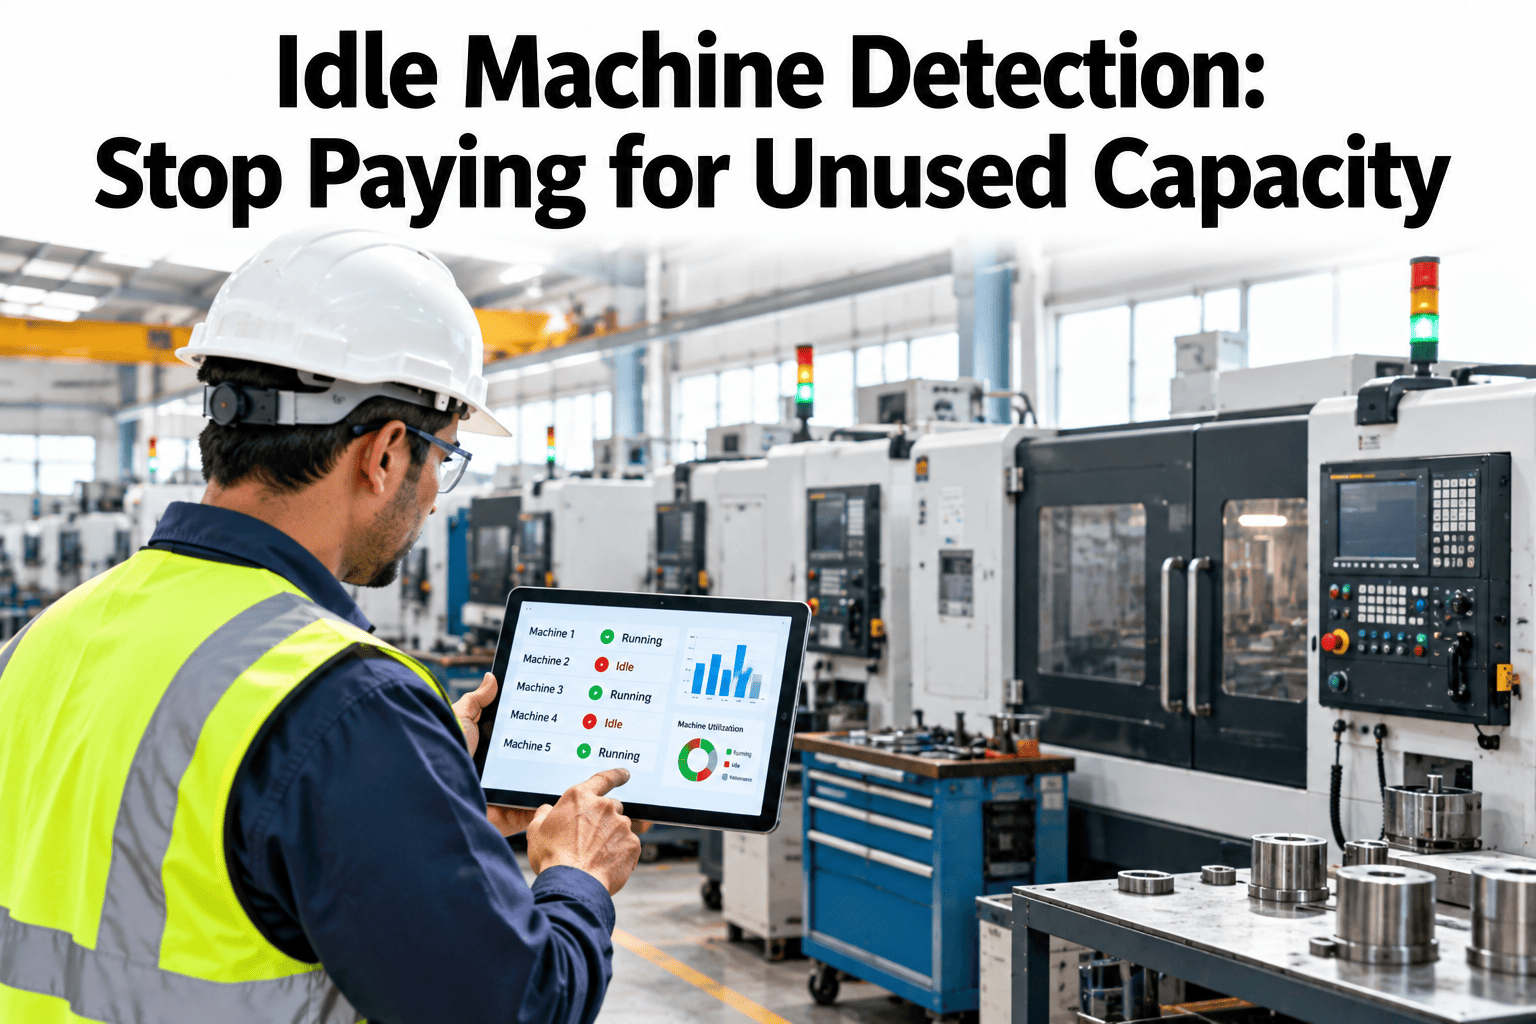
Every machine in the plant has a fixed cost that runs by the hour, whether it is making parts or standing still. Idle time is the gap between the hours you pay for and the hours the machine produces. Most plants know their downtime but not their idle time, because a machine waiting for material looks busy from the doorway. Teams that want that gap measured can ask iFactory AI how machine states are captured automatically.
Idle Machine Detection: Stop Paying for Unused Capacity
Separate running, planned stops, idle waiting and breakdowns on every machine. iFactory AI turns signals from the floor into idle hours you can name, cost and recover.
Where Idle Time Hides in a Week
Start with the whole calendar. A machine has 168 hours a week, but only part of that is scheduled, and only part of the scheduled time is spent running. The bar below shows one illustrative machine.
Teeptrak defines utilization as scheduled time divided by calendar time, and TEEP as OEE multiplied by utilization. If this machine has an OEE of 78 percent on its planned time, its TEEP is 78 percent times 57.1 percent, about 44.6 percent. The same machine can look strong on OEE and weak on TEEP.
Four States, One Clear Rule for Each
Idle detection fails when states are vague. Give every minute of scheduled time exactly one state, and write the rule that decides it.
| State | Typical Signal | Who Owns It | Fix Comes From |
|---|---|---|---|
| Running | Cycle counter advancing, power at working level | Production | Speed and quality work |
| Planned stop | Calendar entry or work order | Planner | Better planning of windows |
| Idle | Power on, no cycle for a set time | Production and logistics | Flow, staffing and scheduling |
| Down | Fault code or stop with alarm | Maintenance | Repair and reliability work |
How to Detect Idle Without Asking Operators
Manual logs miss idle time because operators are busy and stops are short. Machine signals do the job better. Choose the simplest signal that tells running from not running on each machine.
| Signal | What It Shows | Strength | Weak Spot |
|---|---|---|---|
| Controller state or cycle counter | Whether a program is cycling | Most direct and accurate | Older machines may not expose it |
| Electrical current or power | Whether the machine is working or idling | Works on almost any machine | Needs thresholds per machine |
| Vibration or sound | Cutting or moving activity | Fits manual machines | Harder to tune |
| Part presence sensor or vision | Parts arriving and leaving | Shows flow on conveyors and stations | Needs camera or sensor placement |
| Operator log-in or scan | Who is at the station | Links idle to staffing | Depends on people to scan |
Set a minimum time
Count idle only after a short wait, such as two or three minutes, so normal pauses between cycles are not flagged.
Tune per machine
A press and a lathe idle at different power levels. Calibrate each machine against a few days of known behaviour.
Check against reality
Walk the floor with the data for a shift and confirm the states match what you see. Fix mismatches before trusting reports.
Find Out How Many Hours Sit Idle
Book a 30-minute session and iFactory AI will show how machine signals turn into idle hours, reasons and costs on a realistic plant example.
Why Machines Sit Idle: Rank the Reasons
Once idle is measured, ask why. The bars show the 26 idle hours of the sample machine, split by cause. A short, fixed list of reasons makes the ranking possible.
Material and flow
Parts not staged, late deliveries and empty feed points. The largest cause here and often the cheapest to fix.
People and skills
Gaps in cover for breaks and absence, or a machine that only one person can run.
Planning
Orders not released, missing programs and schedules that leave a machine with nothing to do.
A reason code should take a few seconds. Prompt the operator on a simple screen once idle passes a set time, and offer five to eight clear choices. Free text produces long lists that nobody can rank.
Short Gaps and Long Gaps Need Different Fixes
Idle events vary widely in length. Many short gaps add up, while a few long ones can dominate the total. The bars show the share of idle hours by gap length in an illustrative month.
Fix with routine
Kitting, tool carts, standard work at changeover and clear hand-offs between steps trim minutes from each cycle.
Fix with decisions
Release orders earlier, rebalance work between machines, adjust shifts or plan the machine out of the schedule.
When During the Week Does Idle Happen
Patterns by shift and day often point to the cause. The grid shows idle share of scheduled time for one illustrative cell. Darker cells mean more idle.
Night shifts
Less support, thinner staffing and material left unstaged often explain high idle. Fix hand-offs before blaming people.
End of week
Running out of released orders on Friday leaves machines waiting. Look at when work is released.
Start of shift
Slow starts point to set-up and material readiness, not machine faults.
Putting a Price on Idle Hours
Idle hours become real when they have a cost. Each machine hour carries costs that do not stop when production does, such as depreciation or lease, floor space, insurance and fixed labour. The figures below are illustrative.
The fixed cost per hour is an assumption. Use your own figure from finance. Recovering just a quarter of those idle hours gives back 325 hours per machine, which is time the plant has already paid for.
Cost view
Idle hours times the fixed cost per hour. It shows what the unused capacity costs today.
Capacity view
Idle hours as extra output you could sell. It shows what recovery could earn.
Avoided spend
Hours that remove the need to buy another machine or add overtime.
Before You Buy Another Machine
A request for new equipment is a good moment to look at idle time. If existing machines have recoverable hours, the same output may be possible without capital spend.
| Question | What to Check | If the Answer Is Yes | If the Answer Is No |
|---|---|---|---|
| Is utilization low? | Scheduled over calendar time | Consider adding shifts first | Capacity is truly tight |
| Is idle high within the schedule? | Idle share of scheduled time | Fix flow and staffing first | Machines are well loaded |
| Are the idle hours on the right machines? | Idle by machine type | Rebalance work across machines | Bottleneck is real |
| Is the bottleneck down often? | Downtime share on the constraint | Improve reliability | Look at speed and quality |
| Is demand stable? | Order trend over the year | Purchase may be justified | Avoid fixed cost for short peaks |
Alerts That Prompt Action, Not Noise
Detection only helps if someone acts. Alert on idle that matters, to the person who can fix it, at the time it can still be fixed.
The limits above are examples. Set them from your own gap data, and apply stricter limits to bottleneck machines where an hour of idle time costs the whole line.
Common Mistakes in Idle Detection
Most programmes stumble on the same few habits.
A 90-Day Path to Visible Idle Time
iFactory AI is built as a turnkey server that racks in, plugs in and goes live in roughly 6 to 12 weeks, so a first idle-time programme fits inside a quarter.
What iFactory AI Adds
iFactory AI is smart manufacturing and industrial software. It brings machine signals, reasons and costs into one view.
Recovering Idle Hours: Fixes That Work
Each cause has a proven kind of fix. Match the fix to the ranked reason, and start with the largest bar and the lowest effort.
| Idle Cause | Typical Fix | Effort | First Step |
|---|---|---|---|
| Waiting for material | Kit and stage parts before the job starts | Low to medium | Trace the last five waits to their source |
| Changeover and set-up | Standard work, prepared tools and parallel set-up | Medium | Time and film one changeover |
| No operator available | Cross-training and break cover | Medium | Map who can run which machine |
| Waiting for quality or maintenance | Quick-response rules and scheduled checks | Low | Agree a target response time |
| No order scheduled | Release work earlier and level the load | Low | Review the release time of orders |
In the sample machine, kitting alone could remove most of the 8 hours lost to material waits. Even recovering half would add 4 hours a week, or about 200 hours a year, to one machine.
Scheduling Around Idle: Plan the Machine Out
Sometimes the right answer is not to fill idle hours but to remove them from the schedule. A machine that is only needed four days a week does not have to be staffed on the fifth.
When demand exists
Release more orders, move work from busier machines or add products that suit the idle capacity.
When demand is thin
Shorten shifts, combine runs on fewer days or shut a machine for planned maintenance in the quiet period.
Use idle for maintenance
Long, predictable idle gaps are the best windows for preventive work, which then costs no production.
Share the load
Where two machines can do the same job, balance orders so neither sits idle while the other queues.
Review each quarter
Demand shifts, so revisit which machines are staffed and when, using the latest utilization data.
Who Should See What
Idle data is useful at every level, but each group needs a different view. Give people the smallest view that lets them act.
Questions to Settle Before You Start
Answer these with production, finance and maintenance together. Each one removes an argument later, and together they take less than an hour to agree. Write the answers on one page and keep it beside the dashboard so new team members can see how the numbers are defined.
Plain-Language Glossary
Shared words keep production, finance and maintenance aligned.
Frequently Asked Questions
What is idle machine detection?
It is the automatic recognition of times when a healthy, scheduled machine is not producing. Signals from the machine or sensors set the state, so no manual log is needed.
How is idle time different from downtime?
Downtime means the machine cannot run because of a fault. Idle time means it could run but is waiting, often for material, people or orders.
Which metric should we track, OEE or TEEP?
Track both. OEE judges how well you use planned time, while TEEP judges how well you use all calendar time. Ask support how both are calculated for each machine.
Do we need new sensors?
Often not at first. Many machines expose a cycle signal, and power monitoring works on most. Add sensors only where those are not enough.
How long before we see results?
Idle hours usually appear within the first weeks of monitoring. Gains depend on fixing the top causes, which takes ownership and a weekly review.
Put Idle Hours Back to Work
iFactory AI detects idle time, ranks its causes and prices the unused capacity, so you act before buying more equipment. Book a walkthrough on your own machine data.