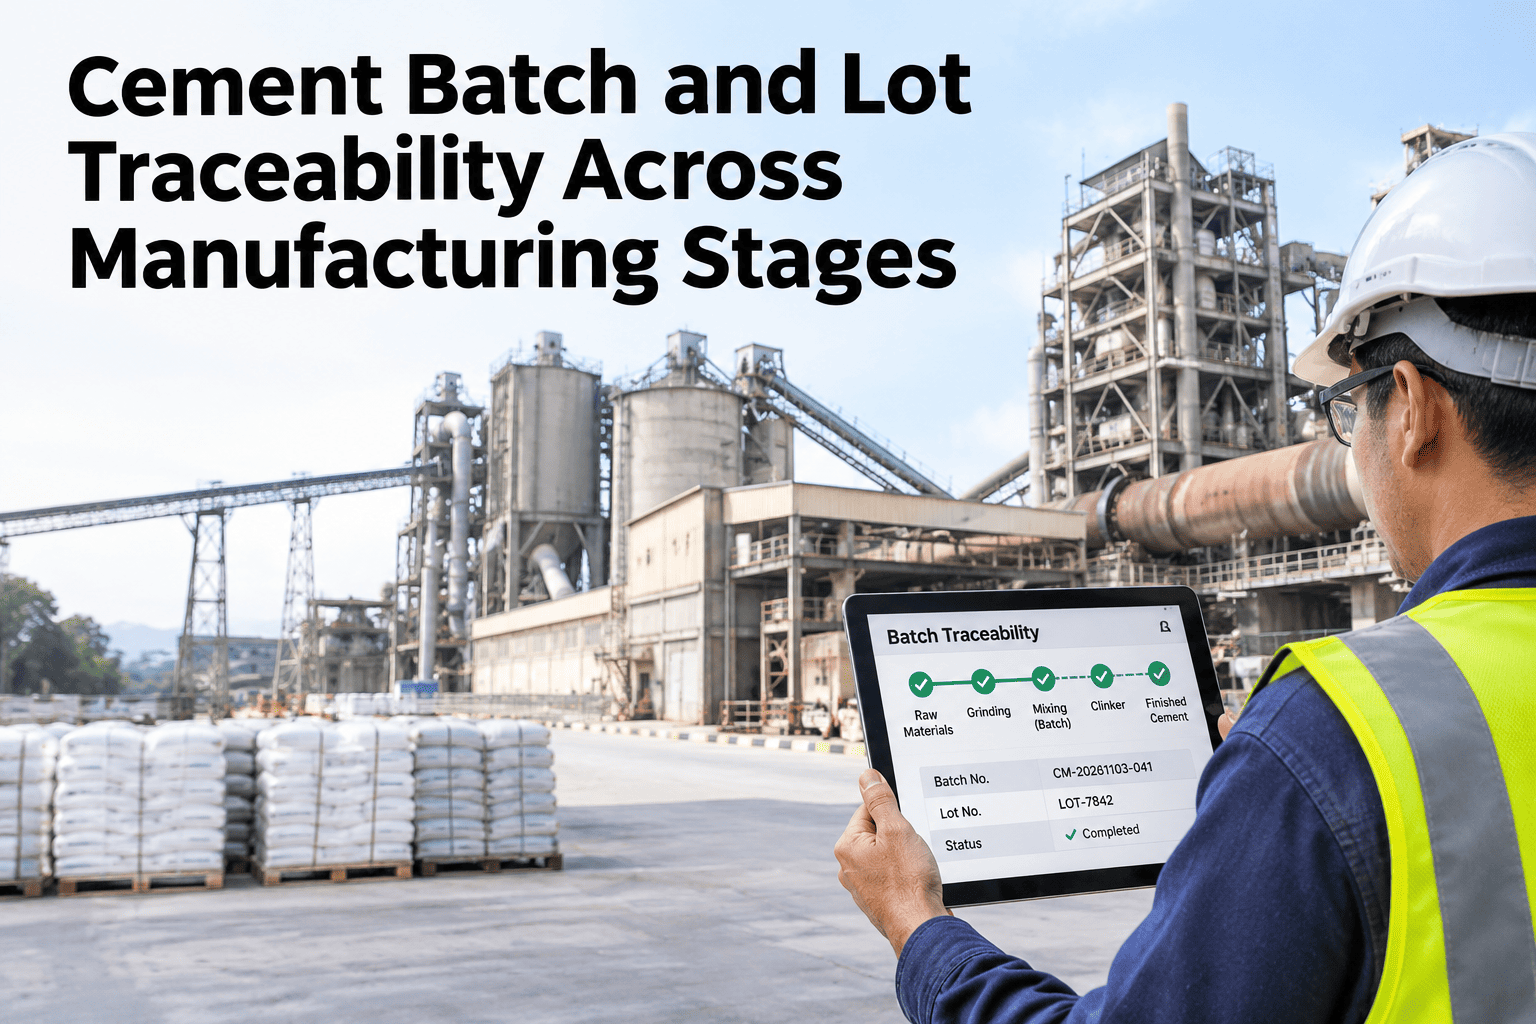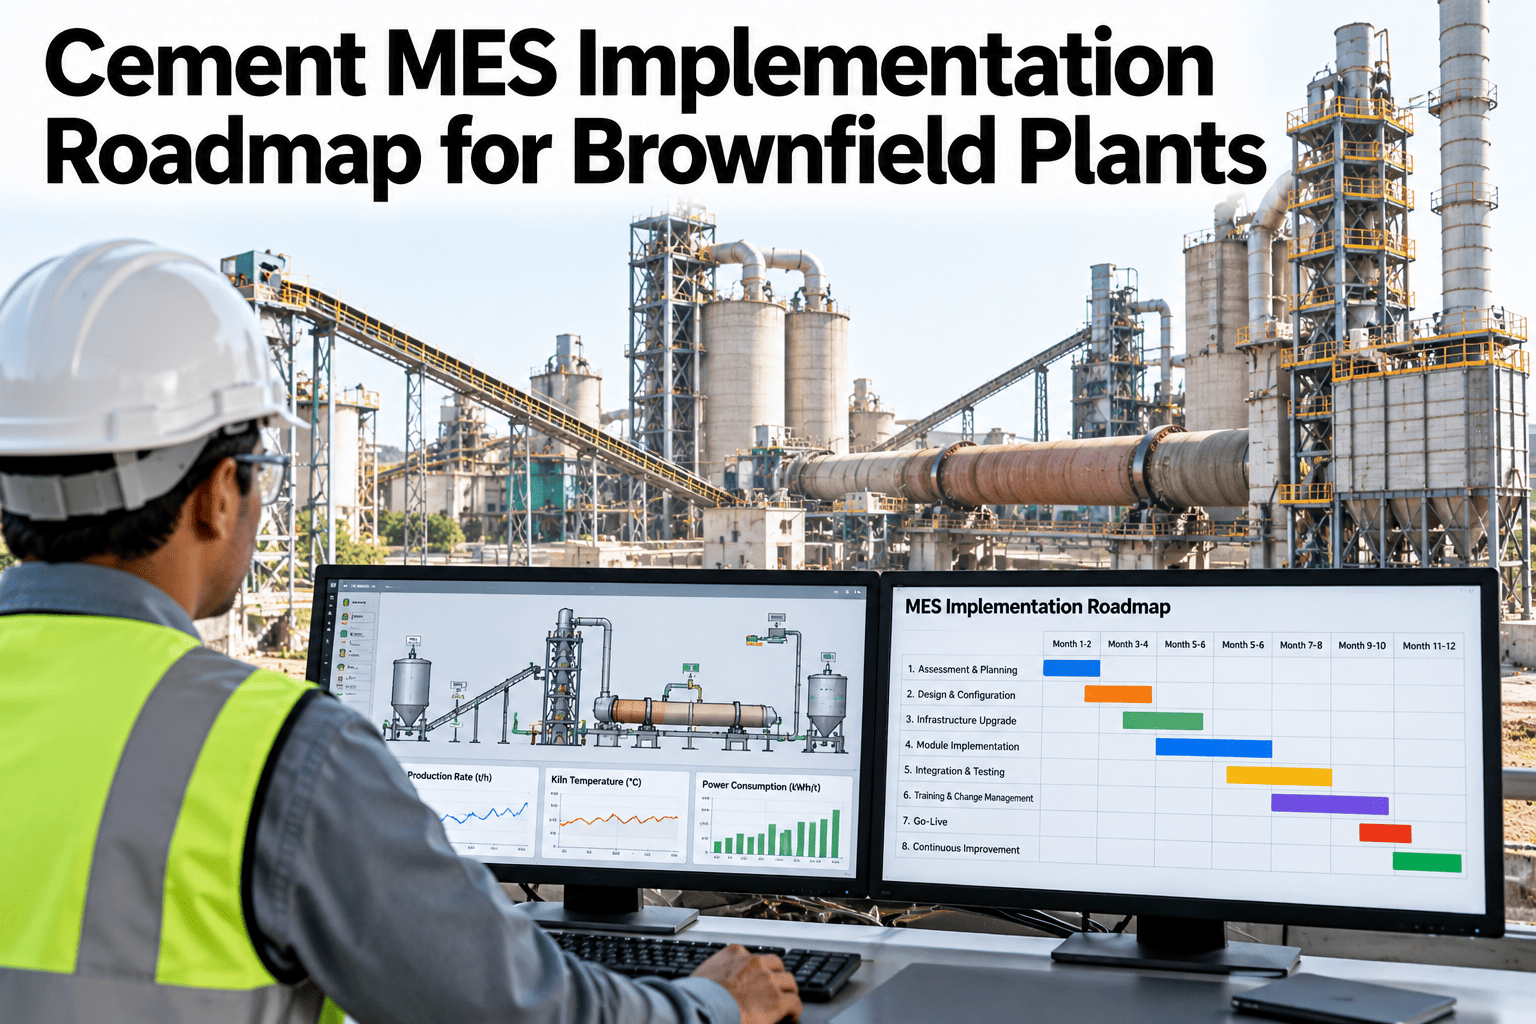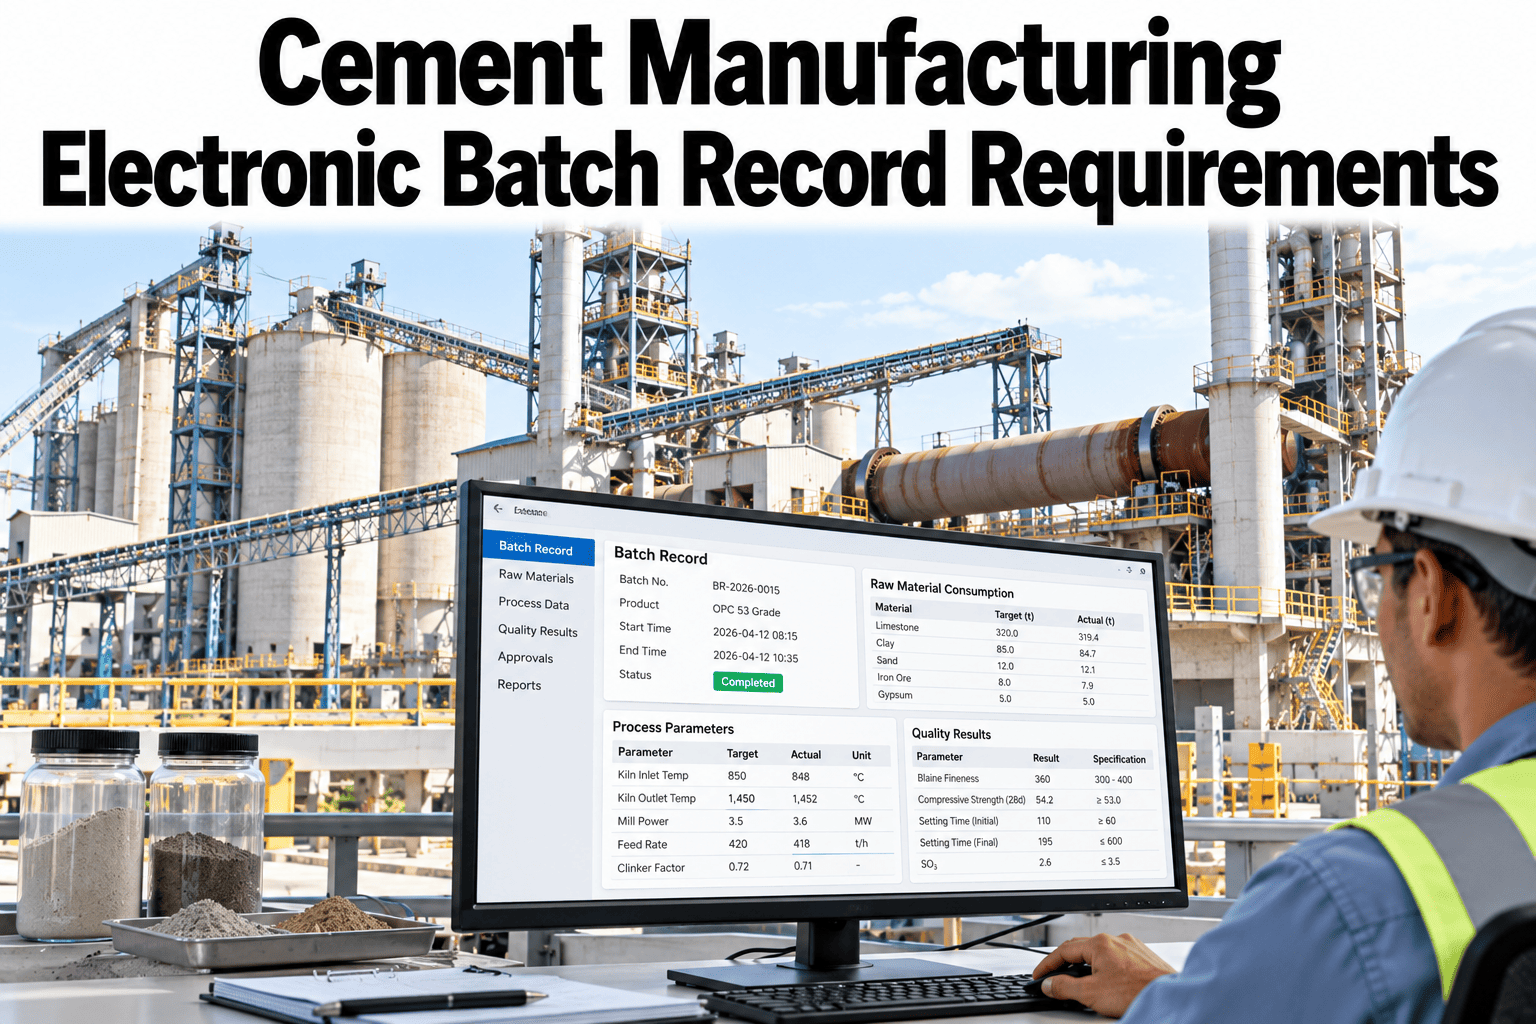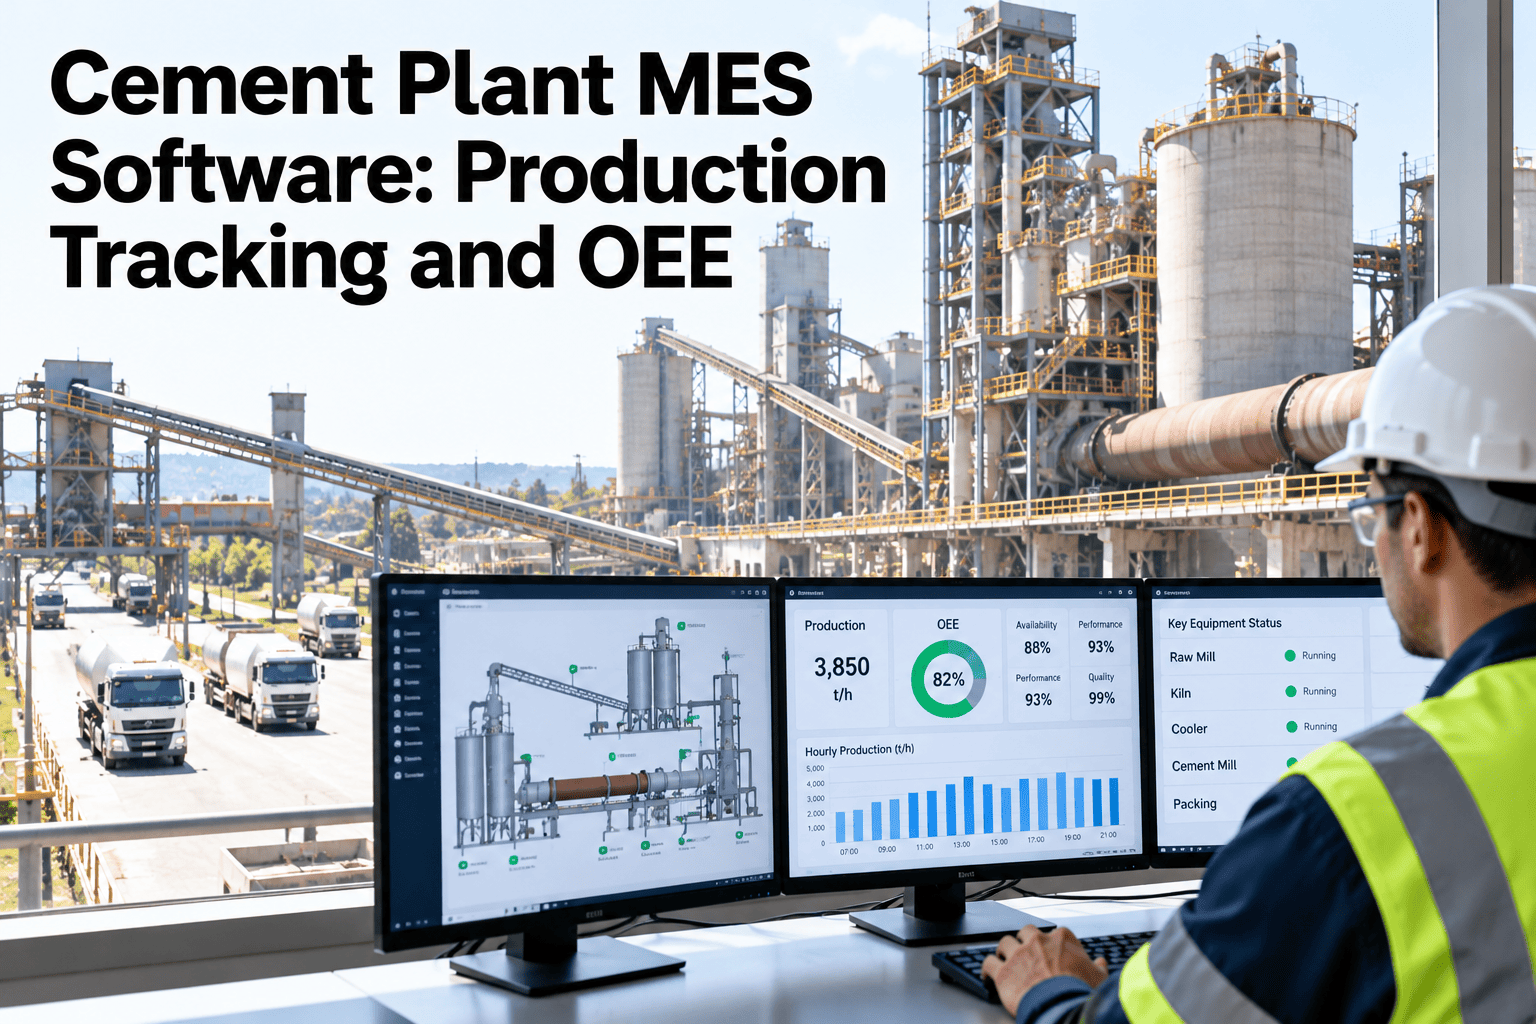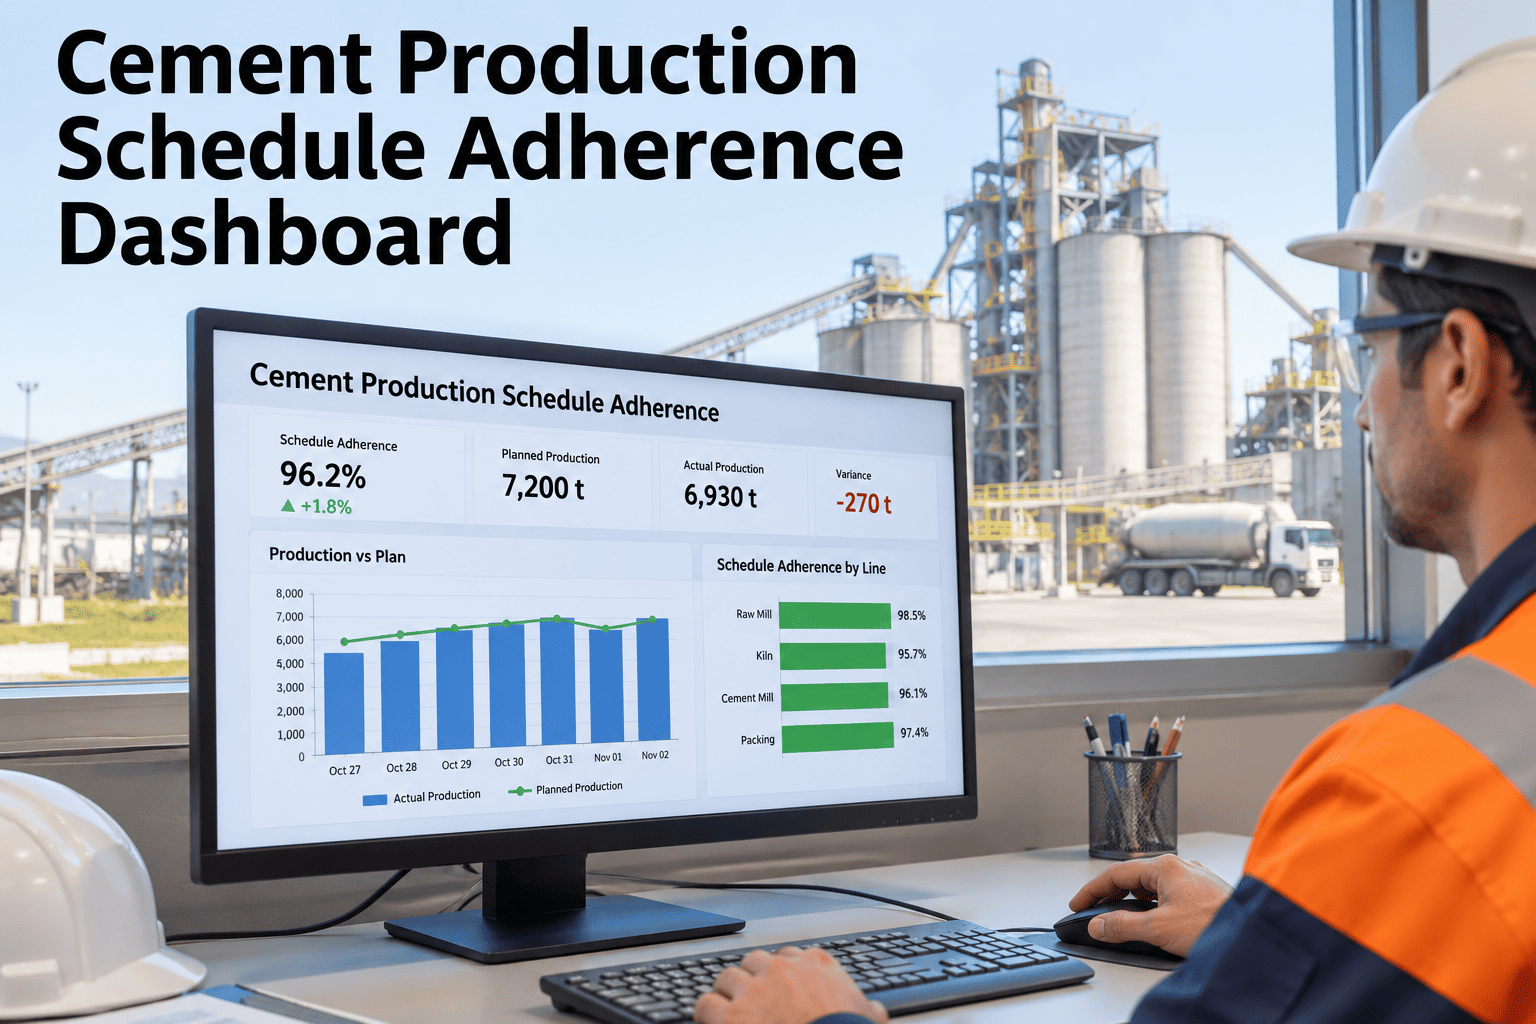
A cement plant's daily schedule is a plan for what the kiln, mills and packing lines are supposed to produce — and the gap between that plan and what actually comes off the line is where most improvement opportunity hides. World-class plants run close to 85 percent overall equipment effectiveness; most cement operations sit closer to 65 to 75 percent, and the difference is rarely one dramatic failure. It is usually a pattern of smaller variances nobody is tracking against the baseline, shift after shift. Plant managers who want to see their own schedule adherence broken down by shift and reason can walk through a schedule adherence review with our team.
See the Gap Between Planned and Actual Before It Becomes Normal
iFactory, an on-premise AI platform for cement MES and production tracking, compares actual output against the schedule baseline by shift and product, with variance reasons attached automatically.
What Does Schedule Adherence Actually Measure?
Schedule adherence compares what a line was planned to produce, by shift and product, against what it actually produced — and attaches a reason to every gap large enough to matter. A plant can be busy all shift and still fall well short of schedule if the actual rate ran below plan the whole time, which is exactly the pattern a simple uptime report never catches. The schedule itself has to be realistic for the comparison to mean anything, which is why the baseline is worth revisiting whenever equipment or product mix changes meaningfully. Ask our team how your current schedule baseline is set before comparing against it.
Where the Gap Shows Up First
See Your Own Shift-by-Shift Adherence Pattern
Share a month of production logs and we will show which shifts and products carry the biggest variance.
Variance Reason Categories, Mapped to the Six Big Losses
| Reason category | Cement example | OEE factor affected |
|---|---|---|
| Equipment failure | Unplanned kiln or mill stop | Availability |
| Setup and changeover | Grade or format changeover on packing | Availability |
| Idling and minor stops | Short feed interruptions, material blockages | Performance |
| Reduced speed | Mill or kiln running derated, below ideal rate | Performance |
| Process defects | Off-spec clinker or cement requiring rework | Quality |
| Startup loss | Ramp-up time after a planned or unplanned stop | Quality / Performance |
Which Asset Is the Current Constraint?
The constraint can also shift during a single shift — a kiln stop early on can hand the limiting role to the mill once the kiln restarts and its own backlog has to be worked through. A dashboard that only shows yesterday's average misses this movement entirely, while one checked against the schedule in near real time can show exactly which asset is setting the pace right now.
From Yesterday's Gap to Today's Action
Actual output against schedule, by shift and product.
Variance reasons ranked by lost time or lost tonnage.
Top reasons discussed at the daily production meeting.
An owner and a next step are assigned to the top variance.
The cycle repeats the next day, and over a few weeks the pattern of what consistently makes the top of the list becomes a far more reliable guide to where to invest than any single bad shift ever could be.
Comparing Adherence Across Shifts, Not Just Against the Plan
A plant that only compares actual output to the schedule misses a second, equally useful comparison — one shift against another, running the same product on the same line. When one shift consistently closes the gap that another shift consistently leaves open, the difference is rarely about the equipment. It usually points to a practice worth spreading from the better-performing shift to the rest of the rotation.
Schedule Adherence, Tracked the Same Way Every Shift
Live Planned-vs-Actual Tracking
Output is compared against schedule continuously, not only at shift-end review.
ISO 22400-2 Aligned Losses
Variance reasons follow the Six Big Losses framework, consistent across kiln, mill and packing.
Constraint Identification
The asset currently limiting the schedule is flagged, not assumed.
Turnkey On-Premise Deployment
Schedule and production data stay on your own server, with no outside cloud dependency.
What Plant Managers Ask About Schedule Adherence
What is a reasonable schedule adherence target for a cement plant?
World-class plants run close to 85 percent OEE, while most cement operations sit around 65 to 75 percent, so the right target depends on where your plant currently stands and how fast you want to close that gap. Discuss a realistic target for your own plant.
Why does performance loss get missed so often?
A mill or kiln that is technically running but at a reduced rate still shows as active on most SCADA overviews, so the loss only becomes visible once actual output is compared against the ideal rate, not just uptime. Ask support how performance loss is captured.
How is the schedule baseline itself set?
The baseline usually comes from planned production time and the line's established ideal rate, adjusted for known planned events like maintenance windows or scheduled changeovers. Review how your baseline is currently set.
Does this replace our existing OEE reporting?
It depends on what you already have — many plants use this to make existing OEE reporting live and reason-coded rather than replacing the underlying calculation method. Ask how this fits your current OEE setup.
How often should schedule variance actually be reviewed?
Most plants review it daily at a short production meeting, with a weekly roll-up to spot patterns that a single day's variance would not reveal on its own. Discuss a review cadence for your plant.
Stop Letting a Small Daily Gap Become the New Normal
See planned versus actual output, by shift and reason, on your own kiln, mill and packing lines.