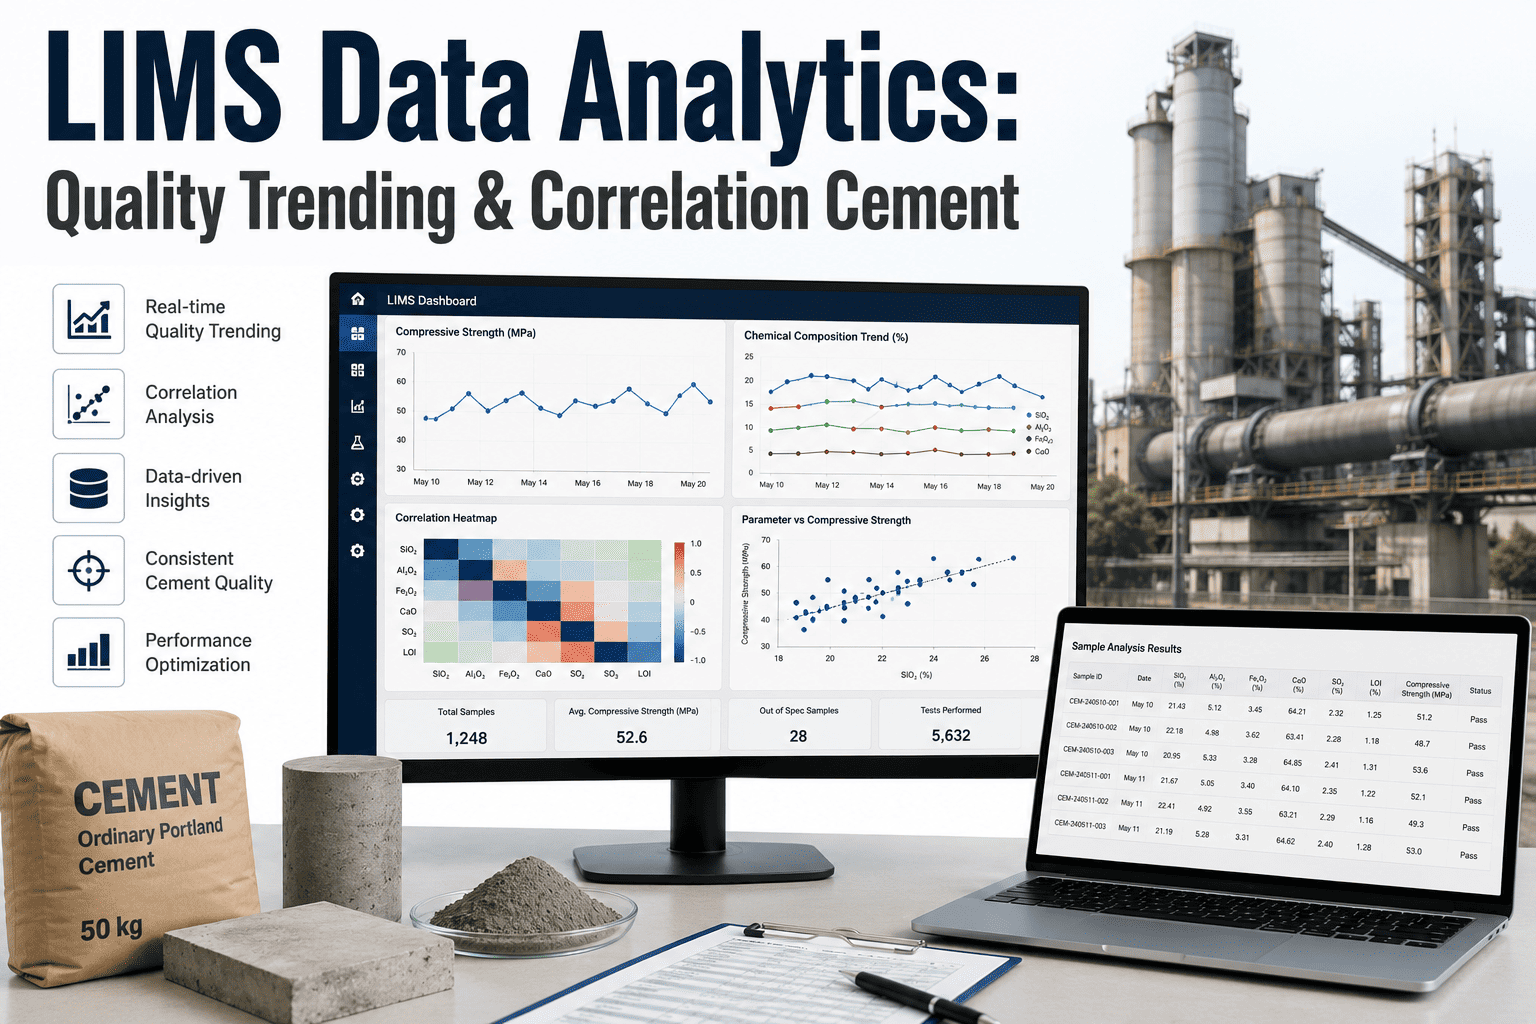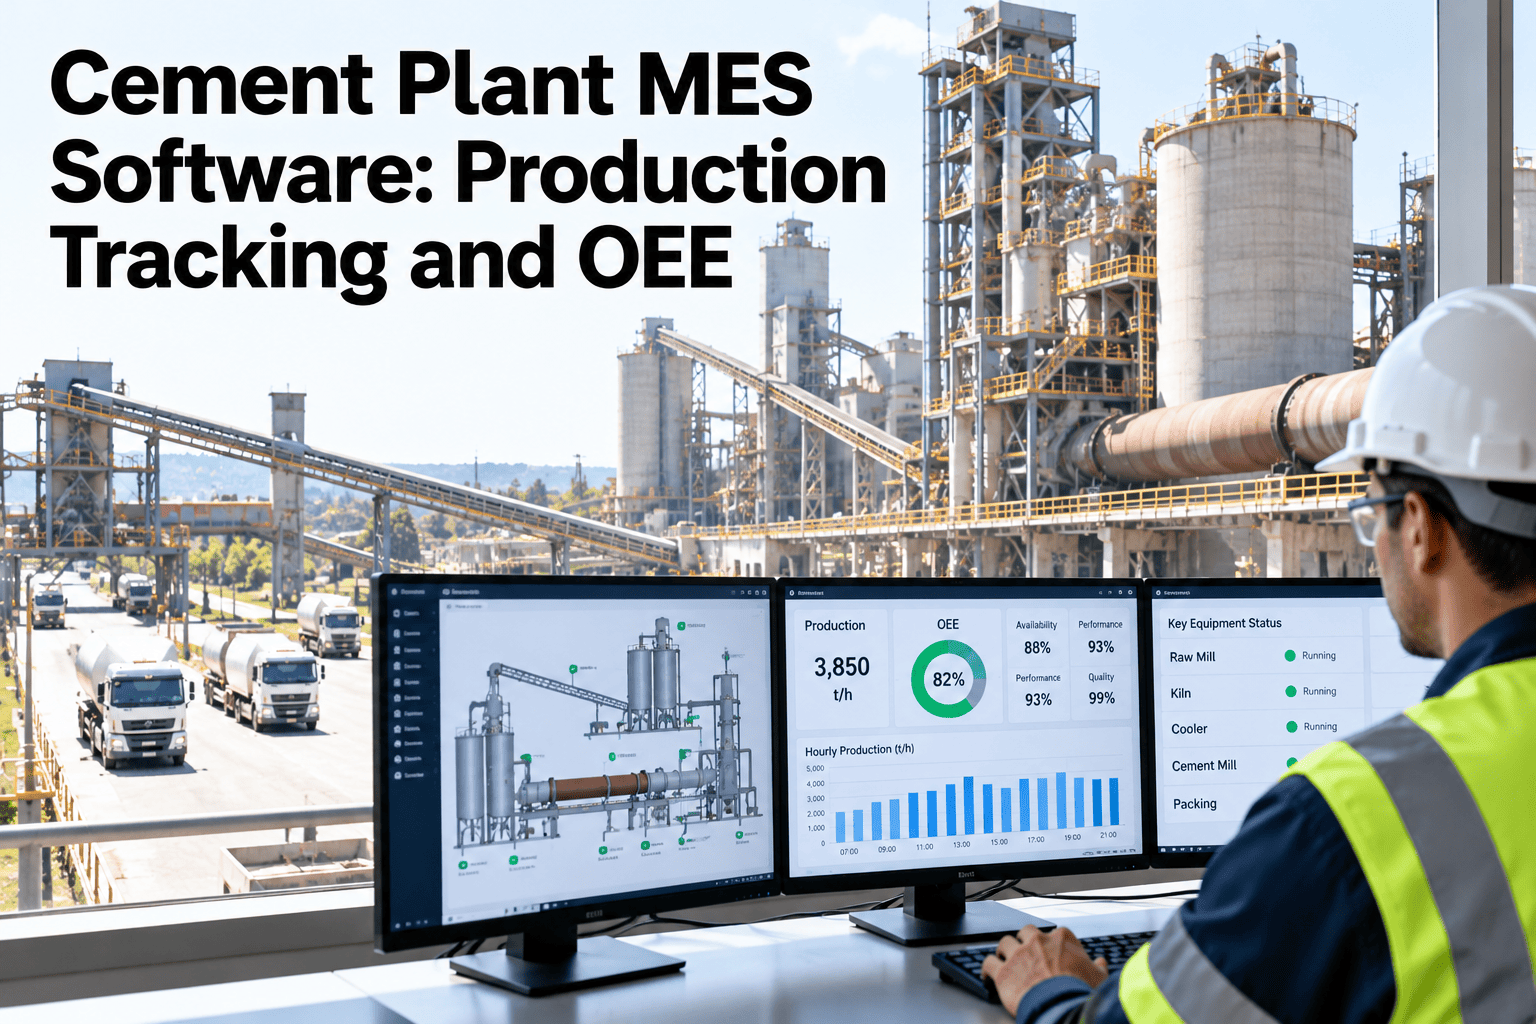
A cement plant running on shift-end spreadsheets and separate downtime logs can usually tell you yesterday's tonnage. It has a harder time telling you, in the moment, which stop reason is eating the most of today's shift, or whether a quality hold upstream is about to starve the next process step. MES software for cement production brings orders, output, downtime and quality records into one tracked system, with OEE calculated from the same consistent data rather than reconstructed after the fact. Plant operations and IT leaders can see production, downtime and OEE tracked together on iFactory AI against their own cement plant's structure.
Know This Shift's Biggest Loss While the Shift Is Still Running
iFactory AI tracks production orders, output, downtime reasons and quality records in one system, with OEE calculated from the same connected data.
What MES Tracks Across a Cement Plant Shift
| Area | What's Tracked | Why It Matters |
|---|---|---|
| Production orders and shifts | What was scheduled against what was actually run | Shows planning accuracy and shift-to-shift variation |
| Output tracking | Tonnage by line, product and time period | The core number every other metric builds from |
| Downtime reasons | Stop duration tagged to a specific cause | Points directly to the next improvement target |
| Quality records | Test results linked to the production batch | Connects the quality bucket of OEE to real batches |
OEE, Calculated From Data That Already Agrees
Built from the same downtime log every team already references.
Compared against rated output, using the same production records.
Drawn from linked lab results, not a separately reconciled figure.
See OEE Calculated From Your Own Plant's Structure
Bring your current downtime codes and production structure to a 30-minute session and map how MES would track them.
Spreadsheet Tracking vs MES Tracking
ERP and Plant Data, Connected Rather Than Duplicated
Production and quality data captured at the MES level can feed ERP for cost accounting and planning, instead of being re-entered or reconciled by hand after the fact. The specific connection depends on your plant's existing ERP setup.
A Composite Scenario: The Downtime Report Three Teams Disagreed On
Picture a weekly review where operations, maintenance and the plant manager each bring their own downtime total for the same week, pulled from three different tracking methods, none of which quite match.
With one MES system logging downtime against a shared reason code set as it happens, the three teams would be looking at the same number in the same review, freeing the meeting to discuss what to fix instead of whose number is right.
Where iFactory AI Fits
Tracks orders and output
Captures production against plan by line, shift and product.
Standardizes downtime reasons
Applies a consistent reason code set across the plant.
Links quality to production
Connects lab results to the batches that generated them.
Calculates OEE consistently
Uses one set of definitions across every line and shift.
Expert Review
A cement plant operations consultant's perspective, reviewed for accuracy before publication: a plant that has never had three different OEE numbers in the same meeting is unusual. The fix is rarely a smarter formula, it's a shared, consistently applied definition and a system that calculates it the same way every time. Mapping your own downtime codes into one shared structure is where that starts. Confirm specific integration and calculation capabilities against your plant's systems before publication of any commitments.
Frequently Asked Questions
How is OEE calculated for a cement plant specifically?
The general availability, performance and quality framework applies, but the specific definitions, such as what counts as planned downtime or rated output, need to match your plant's own operating reality, since cement production has different rhythms than discrete manufacturing. Confirming these definitions upfront avoids disputes later. See how OEE definitions would be set for your specific plant in a short session.
Can this connect to our existing ERP system?
Connecting MES-level production and quality data to an existing ERP for cost accounting and planning purposes is generally the goal, though the specific integration path depends on which ERP system your plant uses. This is worth scoping directly against your actual ERP setup. Ask for a review of how your specific ERP system would connect.
How are downtime reason codes defined for a cement plant?
Reason codes are typically defined collaboratively between operations, maintenance and quality, reflecting the actual stop causes relevant to your specific equipment and process, such as kiln-related, mill-related or material handling stops. A well-structured code set is what makes a loss ranking meaningful rather than a generic catch-all. Explore building a reason code structure for your own equipment.
Does this require replacing our existing plant systems?
Not necessarily. Many MES implementations connect to and read from existing SCADA, historian and lab systems rather than replacing them, adding the execution tracking and reporting layer those systems don't provide on their own. Whether replacement or connection is the right path depends on what you currently have. Try an assessment of how this would fit your current system landscape.
How long does implementation typically take for a cement plant?
Timelines depend on how many lines and systems are in scope, how clean your existing downtime and quality data already is, and how much reason code standardization work is needed upfront. A phased rollout, starting with one line or one data type, is a common way to show value before a full plant rollout. Join a scoping session that estimates a timeline for your plant.
Give Every Team the Same OEE Number
iFactory AI tracks production, downtime and quality in one system, calculating OEE the same way every shift. Request a demo for your own plant.