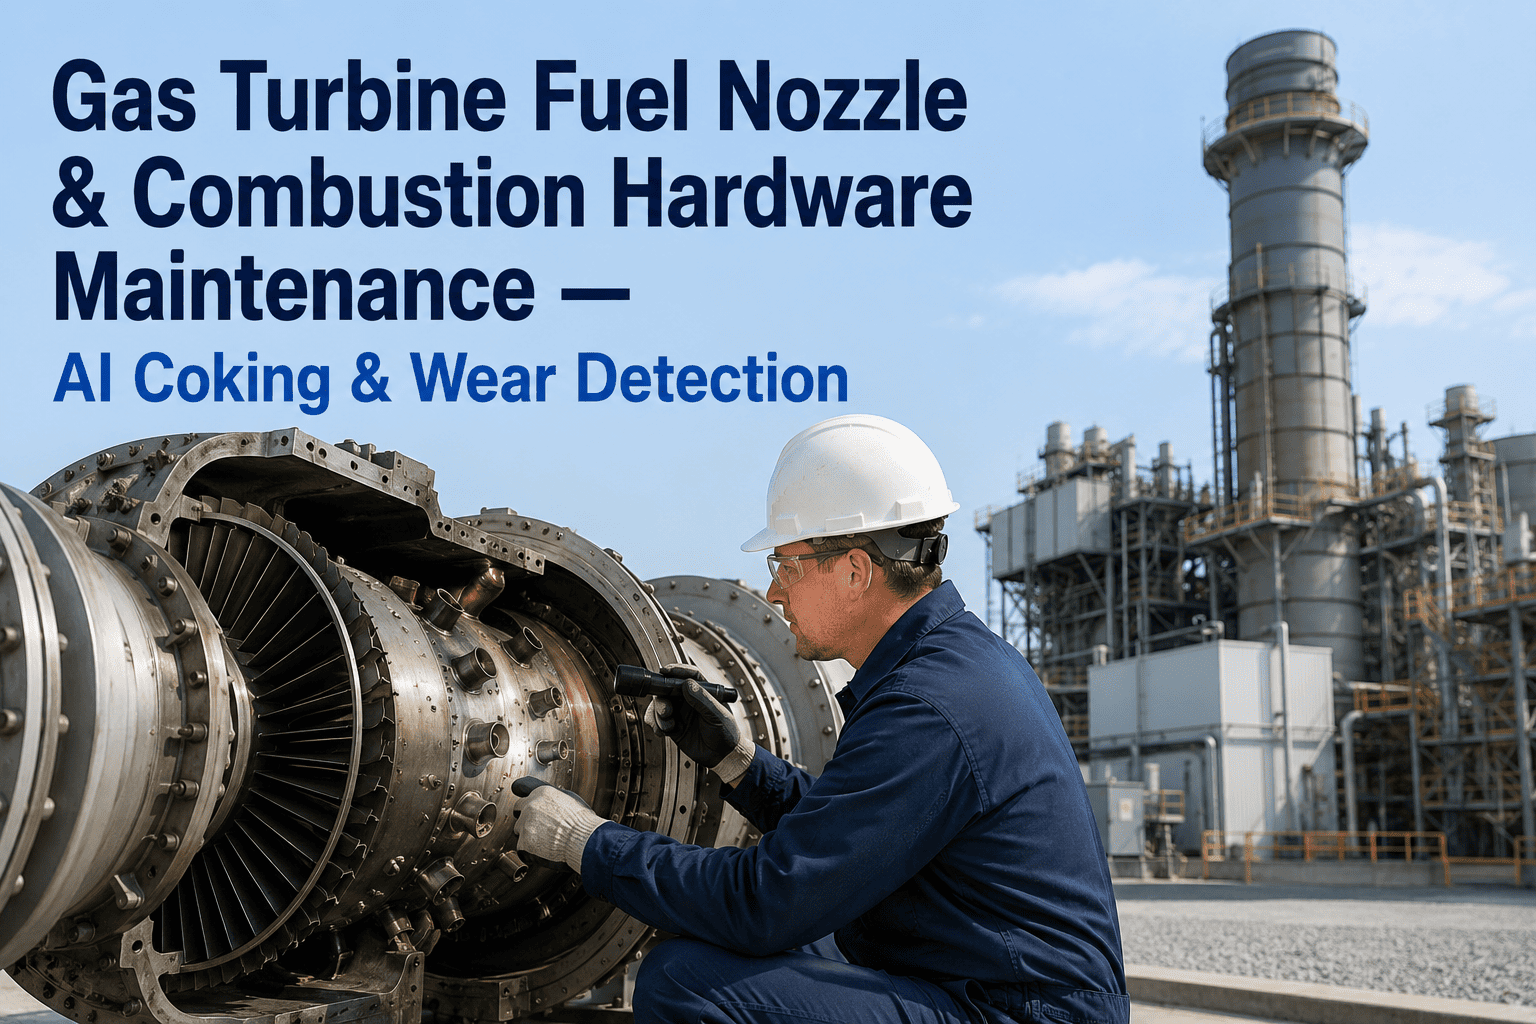
On a combined-cycle plant running a fleet of F-class gas turbines, a single coked fuel nozzle can reduce that unit's heat rate by 0.8% to 1.4% per outage interval. Most process engineers discover the degradation only during a scheduled borescope inspection, by which point the spray pattern has already shifted enough to create hot spots on the combustion liner and transition piece. The repair bill for that cascading damage runs $400,000 to $1.2 million per combustor can, and the plant has already burned through weeks of suboptimal efficiency. The data to catch this early exists in your existing thermal imaging, vibration signatures, and performance trends—but without AI-driven analysis, it stays invisible until someone puts a camera inside the combustor. Book a 30-minute walkthrough to see how iFactory surfaces these signals before the damage compounds.
Stop discovering fuel nozzle coking after the combustor is already damaged
iFactory's AI-powered combustion monitoring detects coking, wear, and spray pattern degradation on fuel nozzles—using data you already have—before it cascades into liner damage and forced outages.
From a 0.3mm carbon deposit to a $2.4M forced outage
Combustion hardware failure in gas turbines is rarely a single event. It is a progressive cascade where one degradation mode accelerates the next. Process engineers who only see the final outcome—liner cracking or transition piece bowing—miss the window where intervention could have prevented millions in damage.
Carbon Deposits Form
Fuel thermal cracking leaves carbon buildup on nozzle tip surfaces and primary orifice edges. This begins within 2,000 to 4,000 operating hours after a clean overhaul.
Spray Pattern Degrades
Coking narrows effective flow areas and distorts the fuel spray cone. Distribution becomes uneven with some flame zones receiving excess fuel while others run lean.
Local Hot Spots Develop
Uneven fuel distribution creates localized high-temperature zones on the combustion liner inner surface. These hot spots exceed material limits and accelerate thermal fatigue.
Liner and Transition Damage
Sustained hot spots cause liner panel cracking, transition piece bowing, and thermal barrier coating spallation. Secondary damage spreads to surrounding hardware.
Forced Outage
Damage reaches a threshold where continued operation risks catastrophic failure. The unit is tripped and the repair window extends for weeks on emergency parts lead times.
Your borescope catches the aftermath. AI catches the cause.
Most combined-cycle plants rely on periodic borescope inspections to assess combustion hardware health. But by the time a camera goes inside the combustor, the degradation chain has been progressing for thousands of hours. Here is what manual inspection misses versus what continuous AI monitoring captures.
Inspection every 8,000–12,000 hours
Massive visibility gaps between inspections. Degradation progresses unchecked for months. By the time the next borescope is scheduled, coking has already damaged the liner.
Subjective visual assessment
Condition ratings depend on the individual inspector. Two technicians examining the same nozzle can assign different severity scores. No quantified degradation metrics exist.
No spray pattern measurement
Borescope images show coking deposits but cannot measure the actual spray cone angle or distribution uniformity. The functional impact of observed coking is estimated, not measured.
Reactive maintenance only
Nozzles are cleaned or replaced after degradation is visually confirmed. There is no mechanism to predict when coking will reach a critical threshold before the next scheduled inspection.
No performance data correlation
Borescope findings exist in a separate report from performance monitoring data. The connection between observed coking and heat rate deviation is never formally established.
Continuous monitoring from existing sensors
Exhaust thermocouples, vibration sensors, and performance trending data are analyzed in real time. Degradation signals are detected within hours of onset, not months.
Objective, repeatable degradation scores
Every nozzle receives a quantified health score based on statistical deviation from baseline. The same data always produces the same score, eliminating inspector variability.
Spray angle deviation tracked to 0.5 degrees
AI infers spray pattern changes from exhaust temperature spread patterns and combustion dynamics signatures. Functional impact is quantified, not guessed.
Predictive degradation forecasting
Trending analysis projects when each nozzle will reach its degradation threshold. Maintenance is scheduled proactively, aligned with the next planned outage window.
Fused performance and hardware correlation
Every degradation signal is automatically correlated to heat rate, fuel flow, and emissions data. You see exactly how much each coked nozzle costs you in efficiency loss per operating day.
Four data signals that reveal nozzle degradation before visual inspection
iFactory does not require new sensors or hardware installations. The AI engine analyzes data streams your gas turbine already produces—exhaust temperatures, vibration signatures, combustion dynamics, and performance parameters—to detect coking, wear, and spray pattern degradation on fuel nozzles and combustion hardware.
Exhaust Temperature Spread Analysis
AI monitors exhaust thermocouple patterns across all combustor cans to detect can-to-can temperature imbalances. A coked nozzle creates a characteristic spread signature—typically a 15 to 30 degree Fahrenheit deviation from baseline—that emerges weeks before liner damage becomes visible. The system tracks this spread in real time and alerts when it exceeds statistically defined thresholds for your specific unit.
Combustion Dynamics Fingerprinting
Dynamic pressure sensors and vibration data carry acoustic signatures of combustion quality. When fuel atomization degrades due to nozzle coking, the combustion dynamics shift with higher low-frequency oscillations and changed flame transfer function characteristics. iFactory's AI learns the baseline fingerprint for each unit and detects deviations that indicate specific nozzle issues without any physical access to the combustor.
Performance Trend Deviation Correlation
Heat rate degradation, compressor discharge pressure changes, and fuel flow anomalies are correlated to isolate combustion hardware losses from compressor fouling, IGV calibration drift, or other performance factors. When the degradation isolates to the combustor section with a spatial pattern matching a specific can, the system narrows the diagnosis to that nozzle set with high confidence.
Predictive Degradation Scoring and Ranking
All detection signals are fused into a single nozzle health score for each combustor can, updated every operating hour. Nozzles are ranked by degradation severity with projected time-to-threshold estimates. Process engineers get a prioritized action list showing which nozzles to inspect first, which can wait for the next outage, and which are operating within normal bounds.
What your performance data is telling you about combustion health
These metrics represent the typical degradation patterns iFactory detects in F-class and H-class gas turbine fleets. Your actual values depend on fuel type, operating regime, and maintenance history—but the patterns are consistent across OEM platforms.
Everything you need to monitor fuel nozzles and combustion hardware
iFactory delivers a complete combustion health monitoring solution that connects to your existing turbine data infrastructure. No new sensors, no control system modifications, deployed on an NVIDIA appliance inside your plant network with zero cloud dependency.
Continuous nozzle health monitoring across all combustor cans
Real-time health scores for every fuel nozzle, updated every operating hour, with trend visualization showing degradation trajectory and projected time-to-threshold for each can.
AI-driven coking detection using existing sensor data
Exhaust thermocouple spread analysis, combustion dynamics fingerprinting, and performance correlation all work without a borescope for initial detection and trending.
Spray pattern degradation tracking and alerting
Inferred spray cone angle deviation, fuel distribution uniformity scoring, and automated alerts when degradation exceeds configurable thresholds per combustor can.
Combustion liner and transition piece thermal mapping
Spatial temperature distribution modeling across the liner surface with hot spot identification and thermal fatigue risk scoring for each liner panel and transition segment.
Correlation engine linking nozzle health to performance metrics
Automated correlation between nozzle degradation scores and heat rate, fuel flow, emissions, and capacity output with quantified dollar impact per degraded nozzle per day.
Digital inspection trail with degradation timeline
Full historical record of every degradation signal, alert, and maintenance action for each nozzle. Audit-ready reports for OEM warranty claims and insurance documentation.
Multi-unit fleet view for combined cycle plants
Single dashboard showing combustion health across all gas turbines in your fleet with cross-unit degradation rate comparison and optimized outage scheduling.
Integration with OEM borescope and thermal imaging systems
Import borescope images and thermal scan data to validate AI predictions and refine degradation models. Close the loop between predictive analytics and physical findings.
Stop waiting for the next borescope to find out your nozzles are coked
iFactory's AI combustion monitoring gives you continuous visibility into fuel nozzle health—detecting coking, wear, and spray degradation weeks before your next scheduled inspection. Book a 30-minute demo and see it on your turbine data.
Combustion hardware monitoring, explained
See what your exhaust data is telling you about your fuel nozzles
Process engineers at combined-cycle plants are using iFactory to detect combustion hardware degradation weeks before scheduled inspections. Book a 30-minute walkthrough and we will show you the analysis on your turbine data.