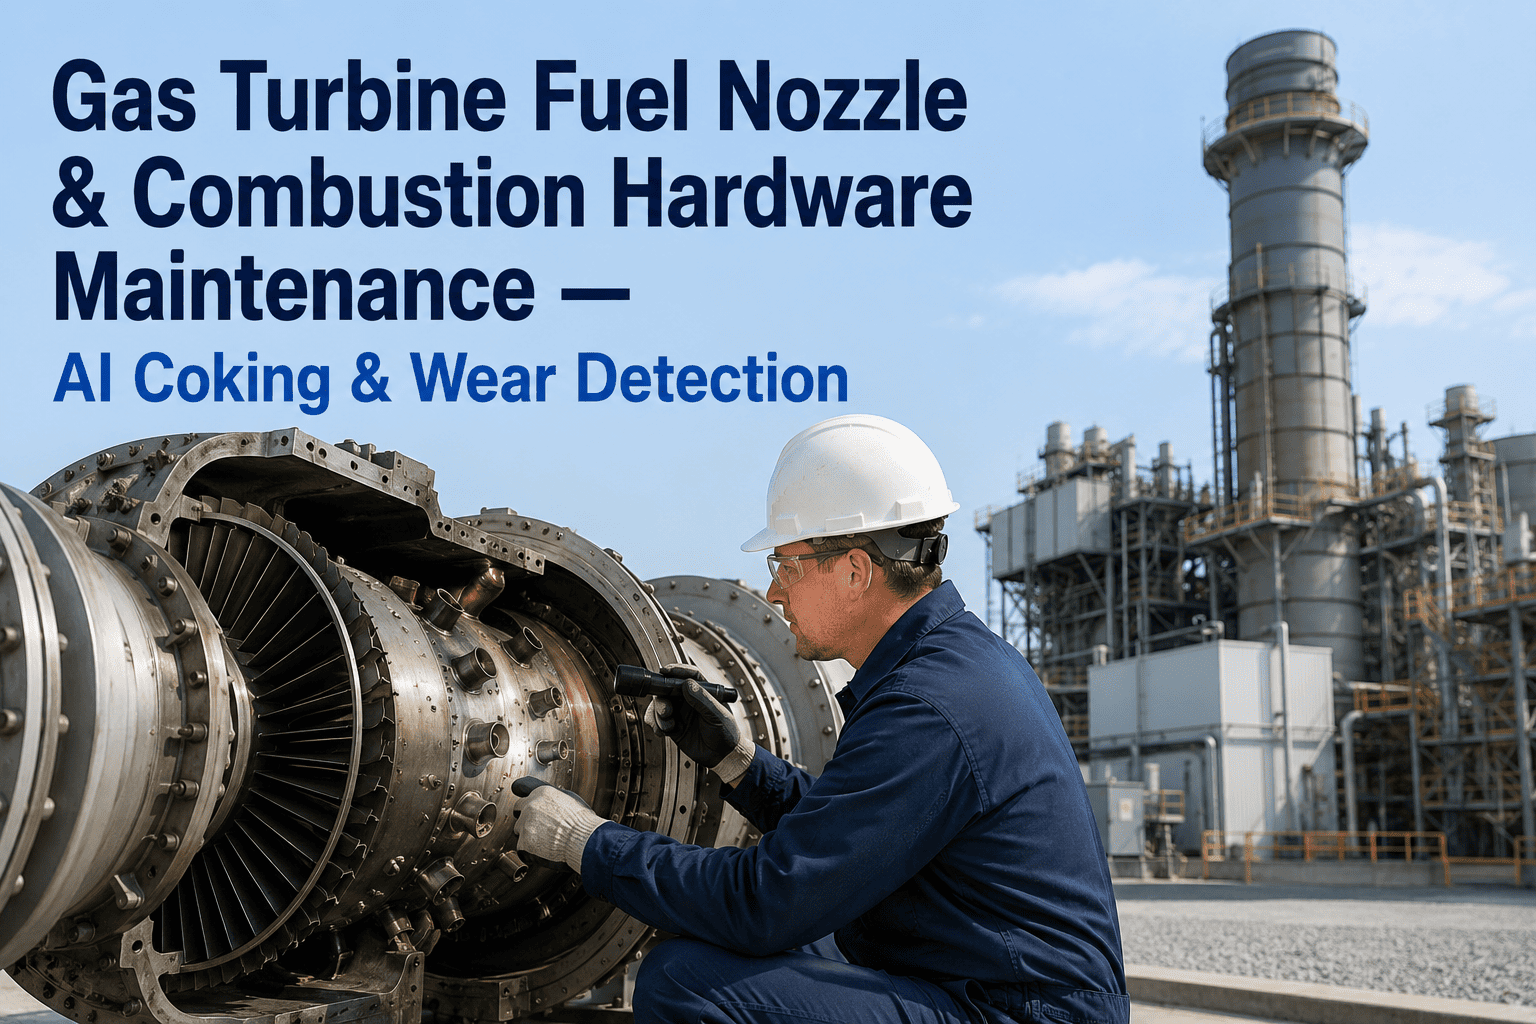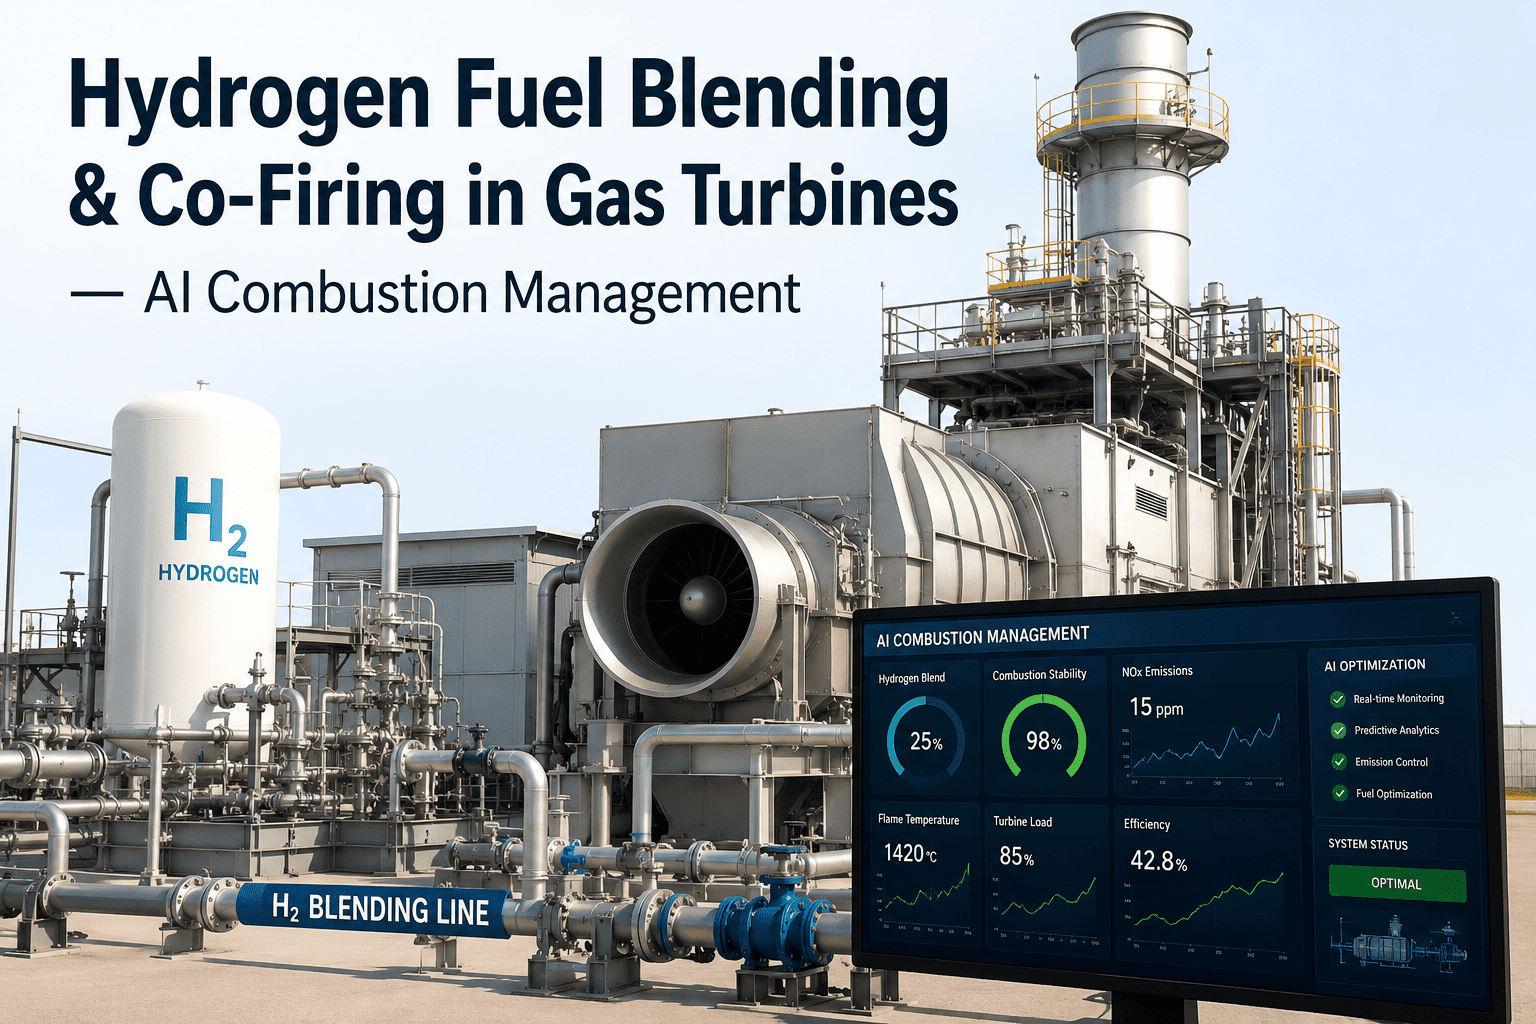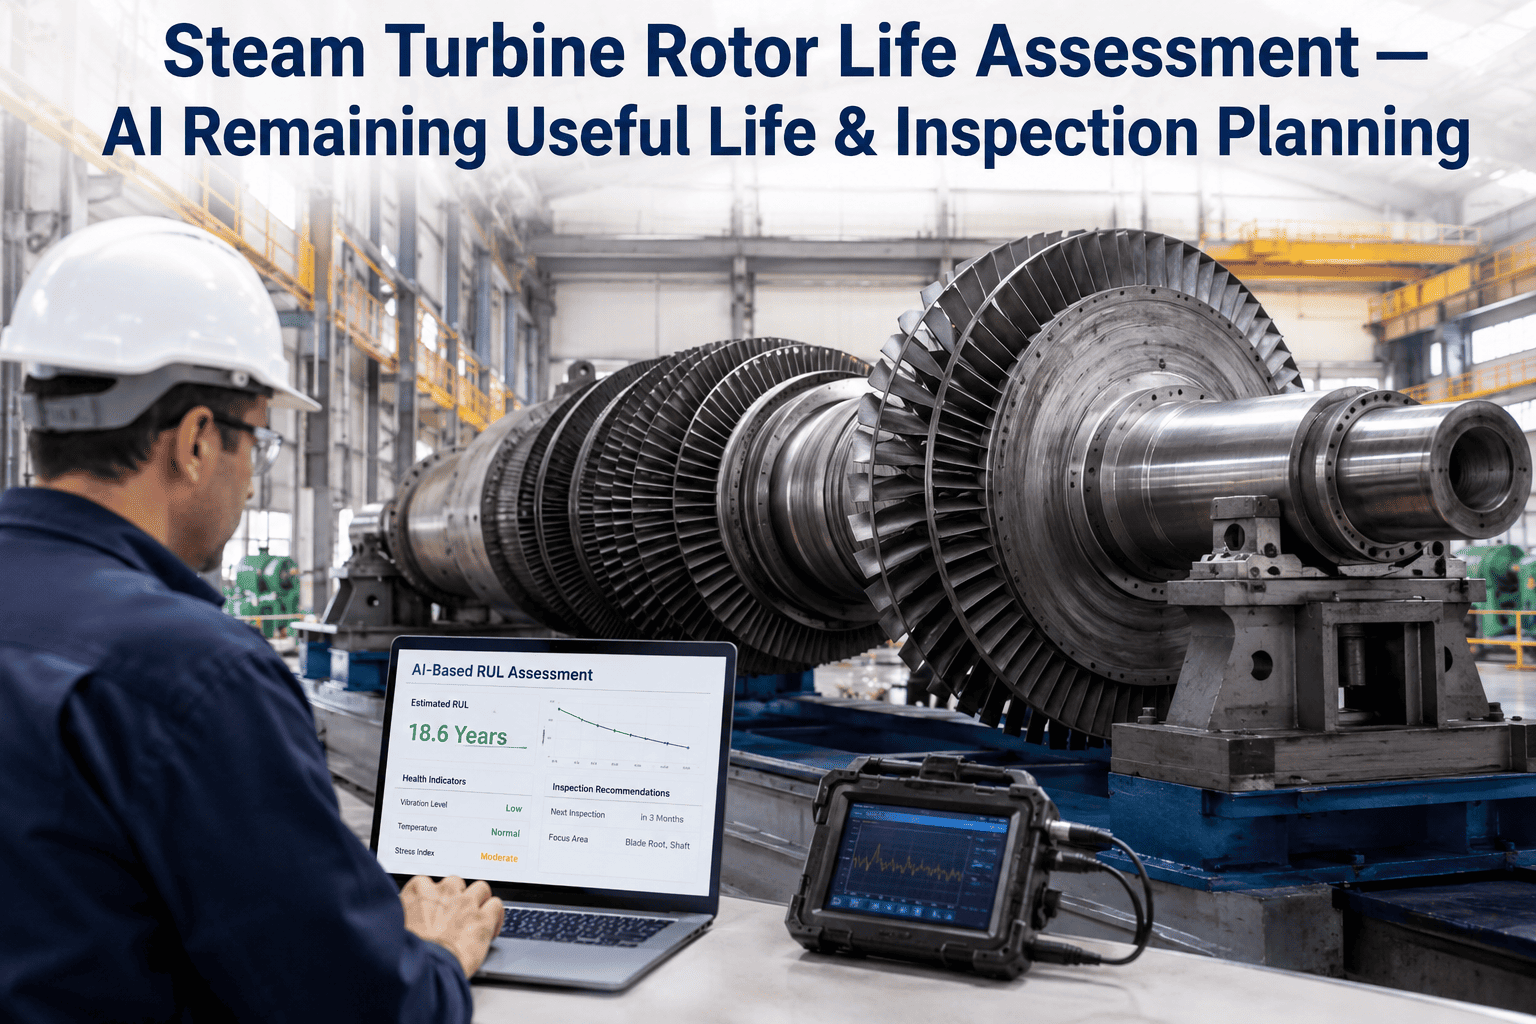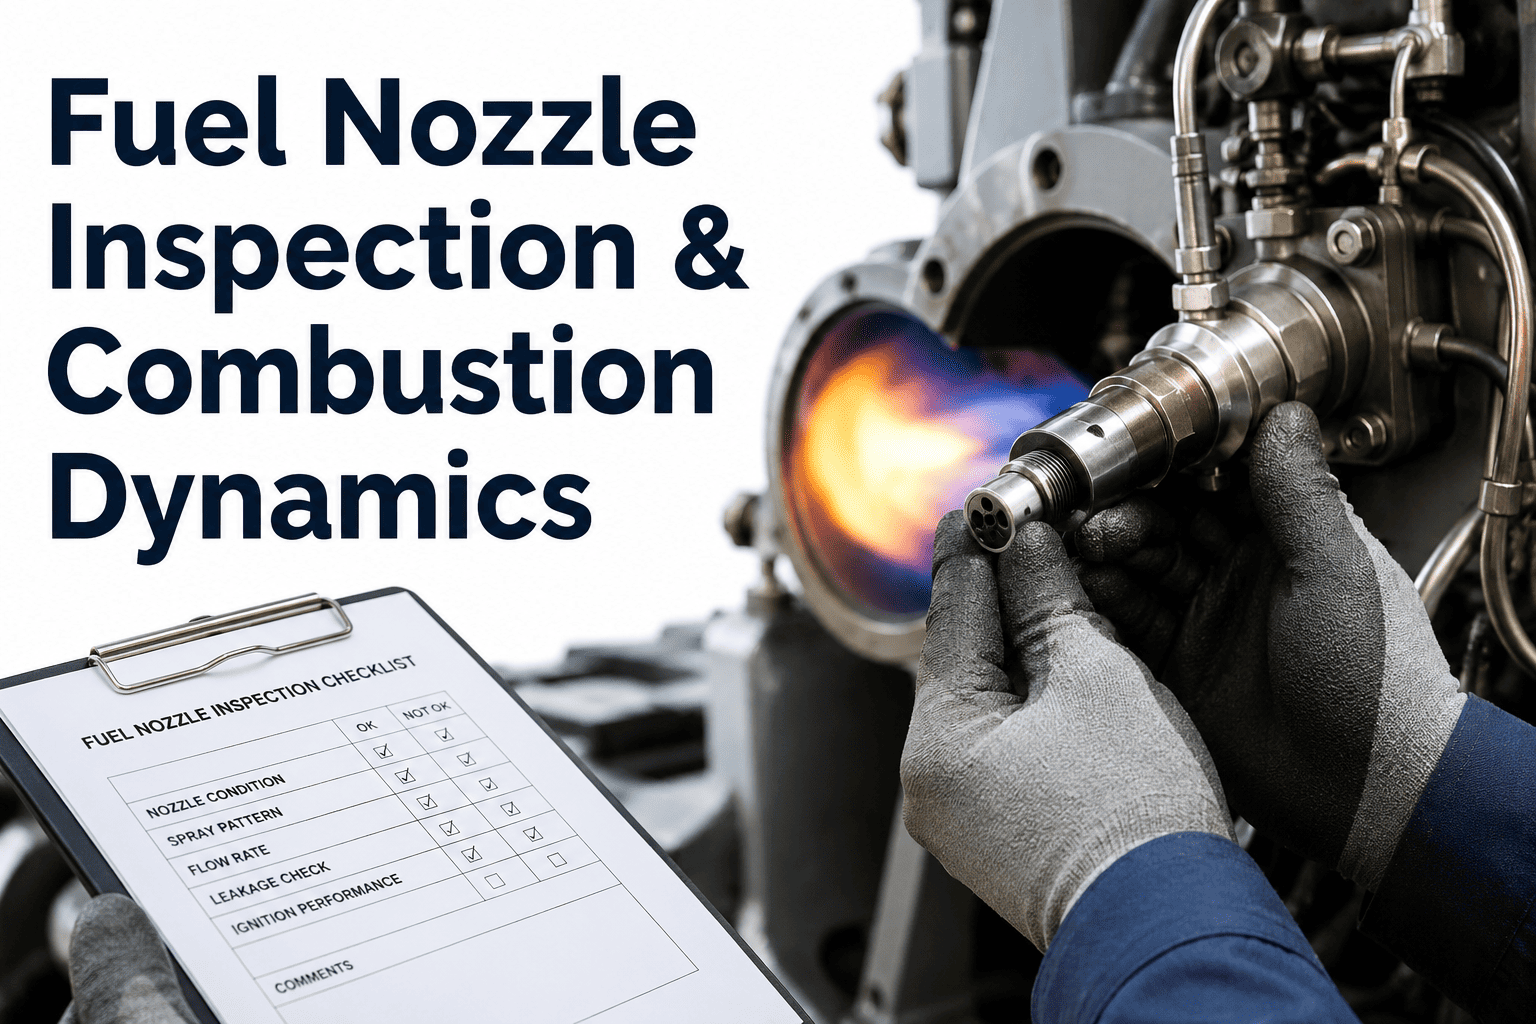
A gas turbine rarely fails at the fuel nozzle without warning first. Long before flashback, nozzle coking, or lean blowout show up as a trip, the combustion dynamics pressure signature has already shifted, and the nozzle tip has already started to change shape under repeated thermal cycling. Most operators only look closely at nozzle condition during a scheduled combustion inspection, which means the unit runs for thousands of fired hours on a slowly degrading fuel spray pattern nobody is watching in between. Book a demo to see how iFactory turns dynamics pressure data into an early nozzle-condition signal instead of a post-trip investigation.
Your Dynamics Pressure Sensors Are Already Warning You About Nozzle Condition. Most Plants Just Aren't Listening
Fuel nozzle degradation and combustion instability are two names for the same underlying problem: fuel-air mixing that no longer matches the pattern the combustor was tuned for. iFactory correlates dynamics pressure spectra, exhaust spread, and nozzle inspection history so reliability teams see the drift building weeks before it becomes a flashback event or an unplanned trip.
Why Fuel Nozzles Are the First Place Combustion Trouble Shows Up
A fuel nozzle's entire job is to deliver a precisely shaped, precisely proportioned spray of fuel into the combustion zone, matched to the air pattern the liner and swirler were designed around. Dry Low NOx combustors run especially lean, which means the margin between stable combustion and lean blowout is narrow by design, and any change in nozzle spray geometry pushes the flame closer to that edge. Coking deposits inside the nozzle passages, tip erosion from years of thermal cycling, and worn or scored fuel orifices all distort the spray pattern in ways that are invisible from the outside but immediately visible in the combustion dynamics spectrum.
The practical consequence is that nozzle condition and combustion dynamics should never be tracked as two separate maintenance topics. A rising dynamics amplitude at a specific frequency band is very often the acoustic fingerprint of a nozzle that has drifted out of its original spray pattern, and treating that signal as a control system nuisance alarm rather than a nozzle condition indicator is one of the more expensive blind spots in gas turbine reliability programs.
Reading Combustion Dynamics: What Each Pressure Signature Actually Means
Combustion dynamics sensors measure pressure oscillations inside the combustor at frequencies typically ranging from tens of hertz up into the low kilohertz range, and different failure modes show up as distinct patterns within that spectrum. A reliability team that only watches for a single overall amplitude threshold misses the diagnostic value entirely, because the frequency and shape of the signal is what actually points to a cause.
| Signature Pattern | Frequency Behavior | Likely Root Cause | Typical Response Window |
|---|---|---|---|
| Rising low-frequency amplitude | 10-50 Hz, slow build | Nozzle coking altering spray angle | Days to weeks |
| Sharp mid-frequency spike | 100-400 Hz, sudden onset | Fuel-air ratio excursion, possible orifice damage | Hours to days |
| Broadband noise floor rise | Across full spectrum | General mixing degradation, multiple nozzles affected | Weeks |
| High-frequency screech tone | 1-4 kHz, narrow band | Acoustic resonance, urgent flashback risk | Immediate |
The pattern matters more than the peak value on its own, since a narrow high-frequency tone at a modest amplitude can represent a more urgent flashback precursor than a larger but broadband low-frequency signal. Reliability teams that only alarm on overall RMS amplitude routinely miss the early, more actionable version of exactly this warning.
Sensor placement also affects how reliably these patterns can be attributed to a specific nozzle rather than the combustor as a whole. Multiple dynamics probes distributed around the combustor case, correlated against individual can exhaust thermocouple readings, make it possible to narrow a developing signature down to a specific can location rather than treating the combustor as a single undifferentiated source. Units instrumented with only one or two dynamics sensors can still detect that something is changing, but pinpointing which nozzle is responsible without that spatial resolution typically falls back on borescope inspection of every can in sequence, which takes considerably longer than a targeted check.
Why Fuel Gas Quality Data Belongs in the Same View as Dynamics Trending
Combustion dynamics tell a reliability team that something has changed inside the combustor, but they do not by themselves say whether the cause originated at the nozzle, the fuel, or the air side of the mixing process. Fuel gas composition, particularly heavier hydrocarbon content and moisture carryover, shifts the combustion characteristics in ways that can produce a dynamics signature that looks identical to early nozzle coking without any actual nozzle degradation being present yet.
Plants that log fuel gas chromatograph data alongside dynamics trends can rule fuel composition in or out as the driver before committing to a borescope inspection, which matters because a fuel-driven excursion is resolved through a fuel system or gas conditioning review rather than a nozzle teardown. Skipping this correlation step is a common reason inspection crews find a nozzle in acceptable condition despite a dynamics trend that clearly signaled a problem, since the actual root cause was sitting in the fuel supply data the whole time.
Nozzle Inspection Intervals by Fuel Type and Duty Cycle
Manufacturer-recommended inspection intervals are a starting point, not a ceiling, and units running on lower-quality fuel, frequent cycling duty, or high ambient dust loading typically need tighter intervals than the baseline schedule assumes. The table below reflects commonly used starting points that most reliability programs then adjust based on actual dynamics trending and borescope findings.
| Fuel / Duty Profile | Baseline Interval | Adjustment Trigger |
|---|---|---|
| Clean pipeline natural gas, baseload | 8,000-12,000 fired hours | Dynamics amplitude trend or exhaust spread widening |
| Associated / field gas, variable quality | 4,000-6,000 fired hours | Any coking observed at prior inspection |
| Dual-fuel with liquid backup | 4,000-8,000 fired hours | Every liquid fuel changeover event logged |
| Frequent start-stop cycling duty | 2,500-4,000 fired hours or per start count | Start count threshold reached regardless of hours |
Stop Waiting for the Scheduled Inspection to Learn What Your Nozzles Are Doing
iFactory streams dynamics pressure, exhaust thermocouple spread, and fuel flow data into a single nozzle-health view, flagging drift long before it reaches trip thresholds so your team can plan a borescope check on their schedule, not the turbine's.
What Actually Causes Nozzle Coking and Flashback Risk
Coking and flashback share a common thread: both are downstream consequences of fuel or air behaving differently than the nozzle design assumed. Understanding which driver is active in a given unit changes both the inspection priority and the operational response.
The Inspection Workflow, Step by Step
What Catching This Early Actually Returns
Common Questions About Nozzle Condition and Combustion Dynamics
Can combustion dynamics monitoring actually predict a nozzle problem before a borescope inspection would catch it?
Yes, and this is the core value of continuous dynamics trending rather than periodic borescope-only inspection. A nozzle that is beginning to coke or erode changes the local fuel-air mixing at that specific location in the combustor, which shows up as a measurable shift in the pressure oscillation spectrum well before the physical deposit is large enough to be an obvious concern visually. Plants that trend dynamics data continuously typically see two to four weeks of warning before a condition would otherwise surface only at the next scheduled inspection. Book a demo to see how this trending works against your unit's historical data.
What is the difference between a normal dynamics fluctuation and one that signals a real nozzle problem?
Every combustor has a baseline dynamics signature that varies somewhat with load, ambient temperature, and fuel composition, so the first requirement is establishing what normal looks like for that specific unit across its operating envelope rather than applying a generic threshold. A real problem shows up as a sustained shift away from that established baseline at a consistent frequency band, particularly when the shift correlates with rising exhaust thermocouple spread or a specific can showing up repeatedly in the pattern. Isolated single-cycle spikes without a sustained trend are usually noise rather than a developing fault.
How much can extending the interval between nozzle inspections actually save without increasing risk?
The savings come less from stretching the calendar interval and more from avoiding unnecessary teardown of nozzles that are still in good condition, since a full combustion inspection often removes every nozzle for evaluation regardless of individual condition. When dynamics and exhaust spread data can confirm which specific cans are stable, maintenance planning can focus labor and replacement parts on the nozzles actually showing drift, which reduces both outage duration and unnecessary parts consumption without extending risk on the units that need attention. Contact support for help structuring a condition-based inspection scope for your fleet.
Does fuel quality variability make dynamics-based monitoring less reliable?
Fuel quality variability actually makes continuous monitoring more valuable, not less, because manual inspection schedules built around a fixed hours interval have no way to account for a bad batch of field gas that accelerates coking well ahead of schedule. Correlating dynamics trends against logged fuel composition data lets a reliability team distinguish a fuel-quality-driven excursion from a genuine mechanical nozzle issue, which changes whether the correct response is a fuel system review or a physical nozzle inspection. Book a demo to see how fuel composition logging integrates with dynamics trending.
Is this approach only relevant for Dry Low NOx combustors, or does it apply to diffusion flame designs too?
Dry Low NOx combustors are typically the higher priority case because their lean operating point leaves less margin before lean blowout, making early detection of nozzle drift more operationally valuable. Diffusion flame combustors run richer and generally have wider stability margins, but they are not immune to the underlying mechanisms of nozzle coking, tip erosion, and flashback risk, and dynamics monitoring still provides useful early warning value on those designs, just with a somewhat wider tolerance before intervention is needed. Exhaust temperature spread trending is often the more sensitive companion indicator on diffusion flame units specifically, since a localized hot streak from an uneven spray pattern tends to show up clearly against the exhaust plane even when the dynamics shift itself is comparatively subtle.
The Warning Was Already in the Data. Now It Doesn't Get Missed
iFactory connects combustion dynamics, exhaust spread, and fuel data into one nozzle-health picture, so your team plans the inspection instead of reacting to the trip.