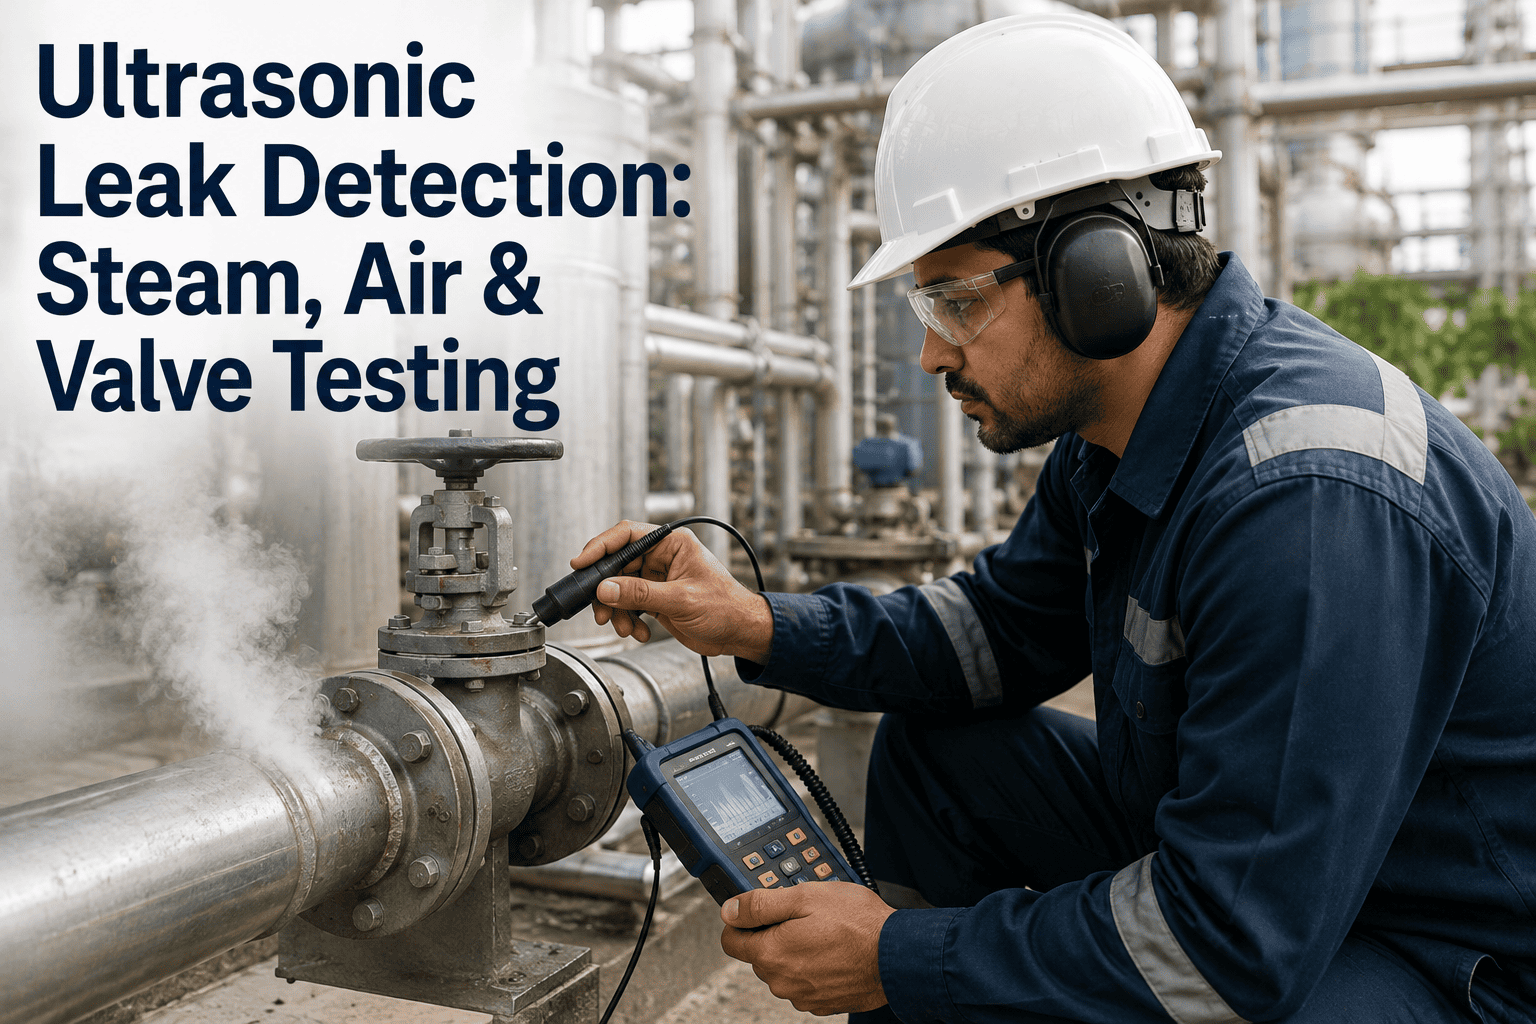
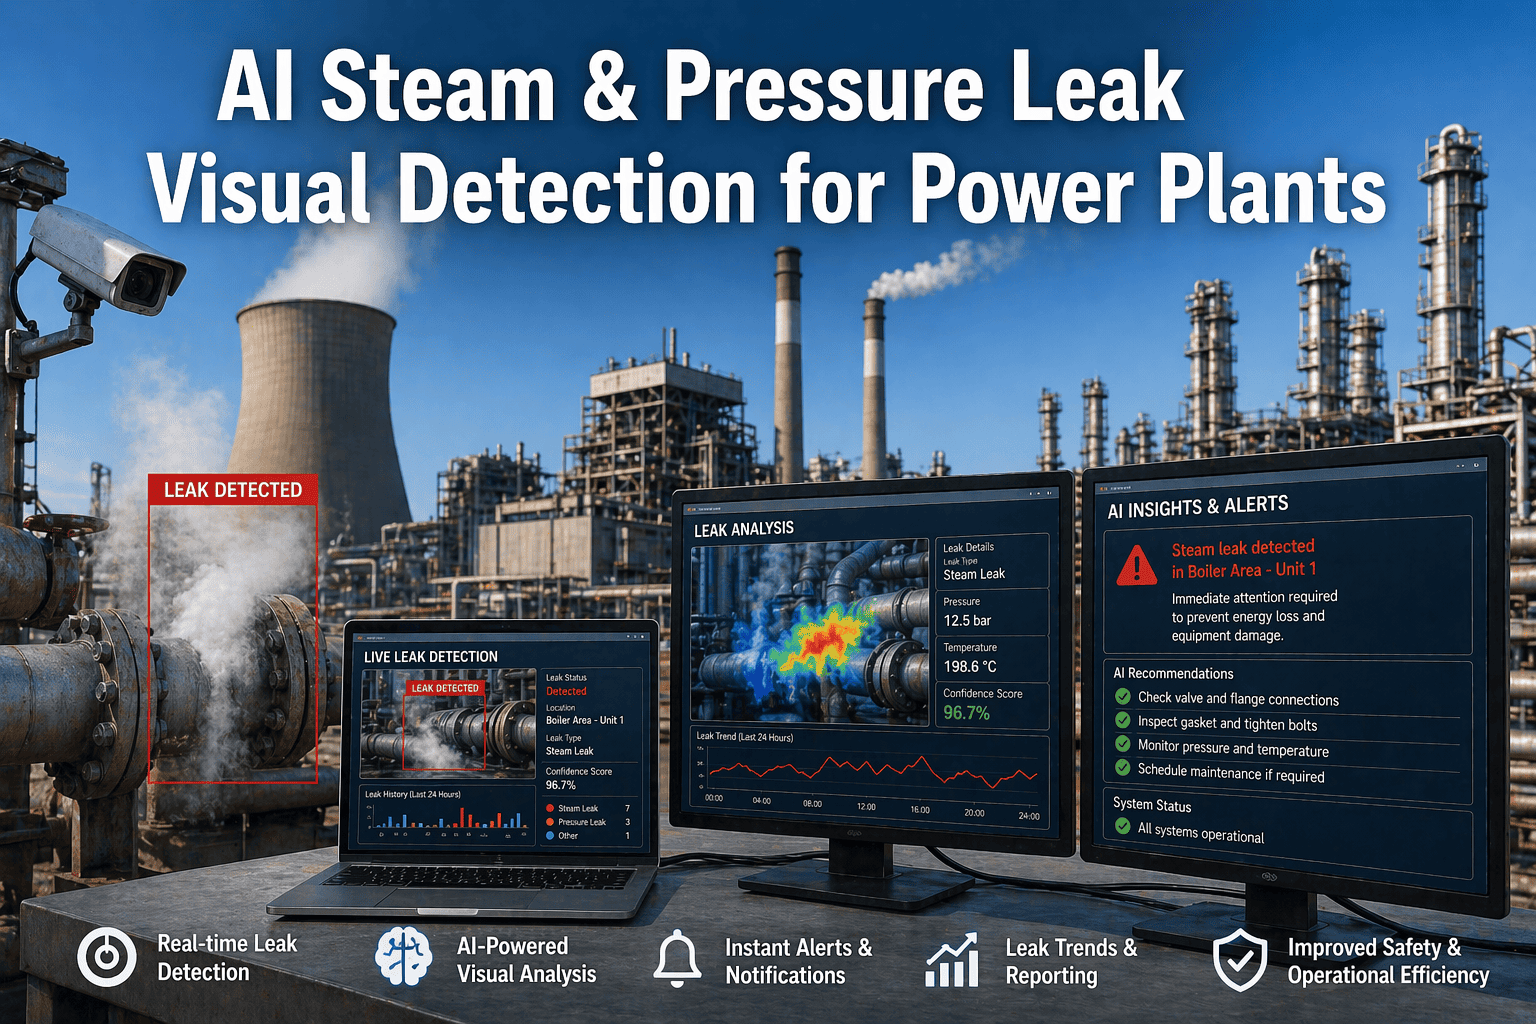
A compressed air leak the size of a pinhole makes almost no sound a human ear can pick up over normal plant noise, yet a handful of leaks like that running continuously can quietly add up to a meaningful chunk of a compressor's annual energy output. Steam leaks and passing valves behave the same way — invisible to a walk-through inspection, completely obvious to an ultrasonic detector tuned to the high-frequency turbulence every leak produces.
MANUFACTURING & INDUSTRIAL AI · ENERGY EFFICIENCY
Find the Leaks That Are Quietly Draining Your Energy Budget
iFactory turns ultrasonic survey data into a prioritized, trackable leak repair program instead of a spreadsheet nobody revisits.
How It Works
Why Ultrasonic Detection Finds What the Human Ear Misses
Every leak — whether it's compressed air escaping through a fitting, steam passing a worn valve seat, or a small crack in a pressurized line — creates turbulent flow as gas or vapor moves from high pressure to low pressure through a small opening. That turbulence generates sound across a wide frequency range, but the vast majority of the useful signal sits well above the range of normal human hearing, typically in the 20 to 100 kilohertz band.
Airborne ultrasonic detectors are built specifically to pick up this high-frequency signal and convert it into an audible tone or a numeric decibel reading a technician can hear through headphones, which is what allows a leak too quiet for the human ear to be identified with confidence even in a loud plant environment. Because ultrasonic sound doesn't travel far and is highly directional, a detector can also be used to pinpoint a leak's exact location, not just confirm that a leak exists somewhere nearby.
Where the Money Goes
Quantifying the Real Cost of an Undetected Leak
Compressed Air
Compressed air is widely regarded as one of the most expensive utilities in a typical industrial plant on a per-unit-delivered basis, and industry studies have repeatedly found that leaks account for a substantial share of total compressed air generation in unmanaged systems. A single leak that seems trivial in isolation can represent a continuous, 24-hour energy draw once the compressor has to work to replace the lost air.
Steam Leaks
Steam leaks waste both the energy used to generate the steam and the treated water lost with it, and because steam systems often run at higher pressure than compressed air, a steam leak of a given physical size typically wastes more energy per hour than an equivalently sized compressed air leak.
Passing Valves
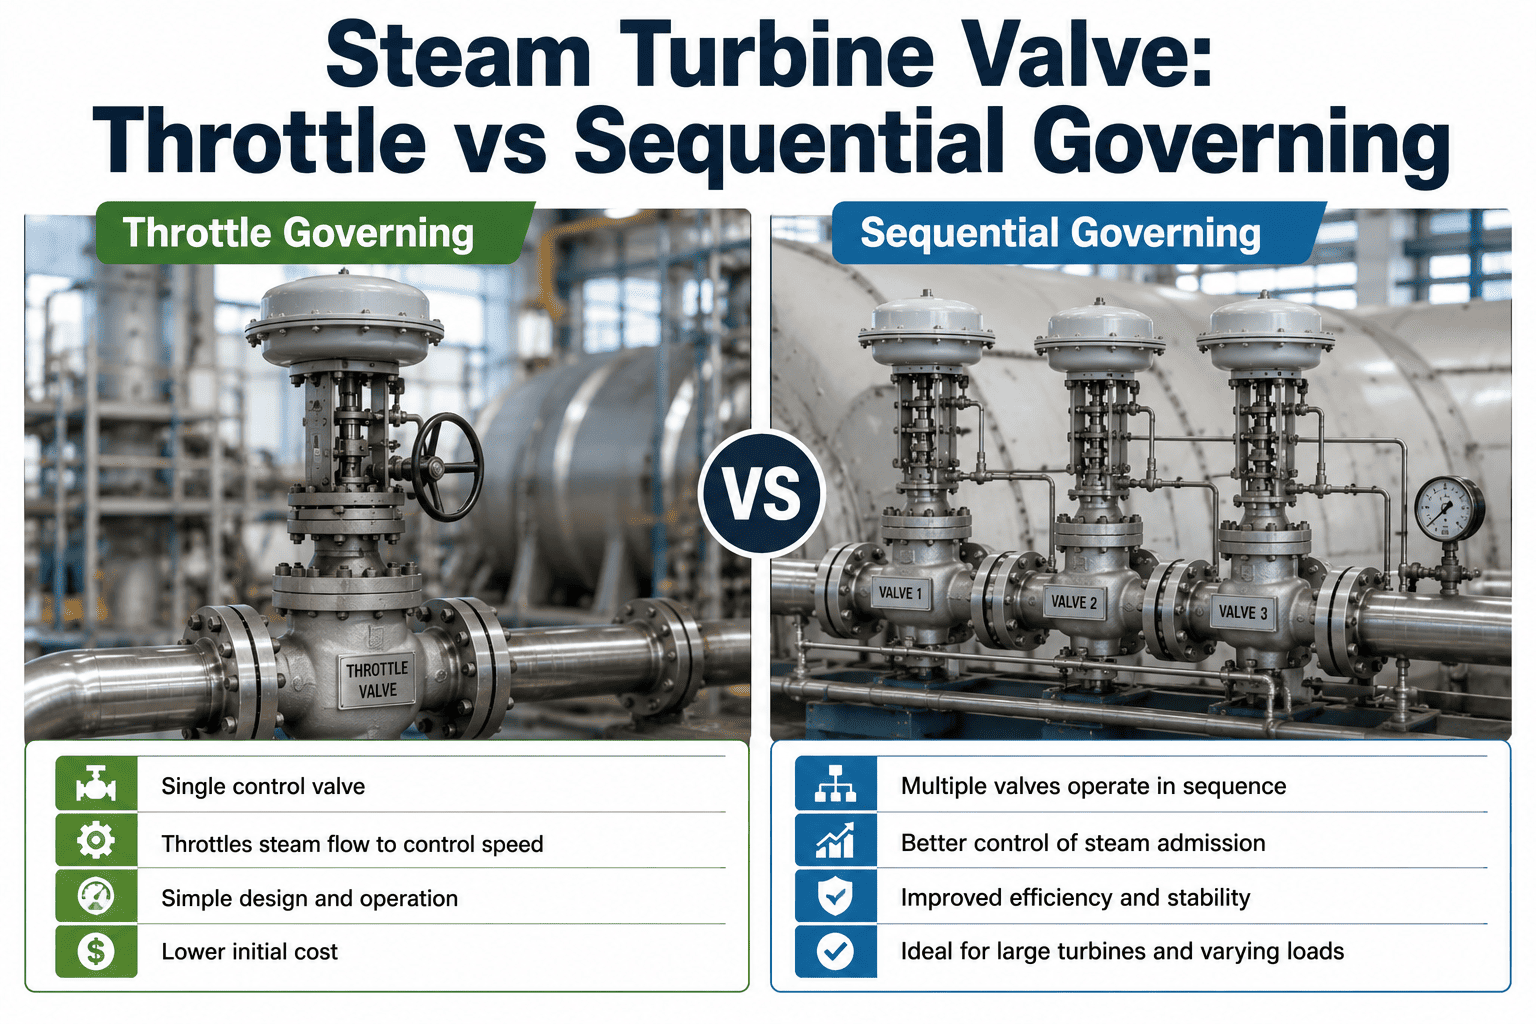
A valve that isn't fully seating internally — passing steam or process fluid across its seat while appearing closed from the outside — is functionally a hidden leak that a visual inspection will never catch, since there's nothing visible to see.
The common thread across all three leak types is that the cost accrues continuously and invisibly, which means it never shows up as a single line item a plant manager would notice — it simply raises the baseline energy consumption of the whole system in a way that's easy to overlook until a structured survey quantifies it directly.
Survey Process
Running a Structured Ultrasonic Leak Survey
01
Define the Survey Scope
Identify which systems — compressed air distribution, steam distribution, specific valve populations — will be covered, since each requires slightly different technique and equipment settings.
02
Survey During Low-Noise Periods
Where practical, surveys conducted during planned downtime or quieter production periods make it easier to isolate leak signals from background ultrasonic noise generated by other equipment.
03
Tag, Photograph, and Quantify Each Leak
Record location, estimated leak rate based on decibel reading, and a photo for each identified leak, creating a documented backlog rather than relying on a technician's memory.
04
Prioritize by Estimated Cost, Not Just Count
Rank the leak backlog by estimated annual energy cost rather than treating every leak as equally important, since a small number of large leaks often account for the majority of the total waste.
05
Repair and Verify Closure
Confirm each repaired leak with a follow-up ultrasonic check rather than assuming a maintenance work order closure means the leak is actually gone.
Frequency Planning
How Often Should a Plant Run Leak Surveys?
| System Type | Typical Survey Frequency | Rationale |
|---|
| Compressed air distribution | Quarterly to semi-annually | New leaks develop continuously from vibration, thermal cycling, and fitting wear |
| Steam distribution and traps | Semi-annually to annually | Steam trap and valve wear tends to be gradual, but consequences of a large leak are significant |
| Critical or high-pressure valves | Aligned with planned outages | Allows internal inspection alongside ultrasonic testing when the system is already isolated |
| Newly commissioned systems | Within first 90 days, then standard cycle | Installation-related leaks often surface early and are cheaper to catch before they become routine |
Plants that run leak surveys only reactively — after noticing a compressor running more than expected, for example — consistently find a larger and more expensive leak backlog than plants running them on a fixed proactive schedule, simply because leaks accumulate continuously between any two points of investigation. Book a demo to see how survey scheduling and backlog tracking work together in practice.
STOP PAYING FOR LOST AIR AND STEAM
Turn Leak Detection Into a Tracked, Repeatable Program
Our team will walk through how iFactory helps you quantify, prioritize, and close out leak repairs across your compressed air and steam systems.
Choosing Equipment
What to Look for in an Ultrasonic Detection Instrument
Not every ultrasonic detector is built for the same use case, and selecting one based on the specific mix of compressed air, steam, and valve testing a plant needs to perform will produce better survey results than defaulting to the cheapest available option.
Frequency Tuning Range
Adjustable frequency sensitivity helps isolate leak signals from background ultrasonic noise sources common in busy production areas.
Decibel Readout and Data Logging
Numeric readings that can be logged and compared over time turn a subjective "sounds louder than last time" observation into an objective, trackable measurement.
Contact Probe Attachment
A contact probe accessory allows internal valve passing to be assessed directly through the valve body, distinguishing it from airborne leaks nearby.
Leak Rate Estimation Software
Built-in or paired software that converts a decibel reading and distance measurement into an estimated flow rate and cost, removing manual calculation from the survey process.
Technician Training
Why Survey Quality Depends on the Technician, Not Just the Instrument
Two technicians using the identical ultrasonic detector on the same system can produce noticeably different survey results, since interpreting a reading, distinguishing a genuine leak from background ultrasonic noise, and deciding where to point the sensor all depend heavily on trained judgment rather than the instrument alone.
Recognizing False Positives
Nearby rotating equipment, electrical arcing, and even certain lighting ballasts can generate ultrasonic signals that mimic a leak, and distinguishing these requires hands-on training rather than instrument settings alone.
Consistent Scanning Technique
A systematic scanning pattern across fittings, valves, and connections ensures a survey doesn't miss sections simply because a technician moved through an area faster on one visit than another.
Calibration Awareness
Understanding how instrument calibration and battery condition affect reading sensitivity prevents a gradually degrading instrument from silently under-reporting leaks over successive surveys.
Safe Access Practices
Surveying elevated piping, confined spaces, and high-temperature steam lines safely requires training beyond instrument operation alone, since leak surveys often take technicians into areas not covered by routine walk-throughs.
Program Integration
Connecting Leak Data to Broader Energy Management Efforts
A leak survey that produces a one-time report and repair list captures only part of the available value. Plants that connect leak detection data to their broader energy management and reliability programs get a compounding benefit that a standalone survey never delivers on its own.
Tracking cumulative estimated savings from closed leak repairs against actual compressor or boiler energy consumption over time validates whether the repair program is delivering the results the initial survey projected, and it also surfaces whether new leaks are appearing faster than they're being closed — a pattern that often points toward an aging distribution system needing more than routine leak repair to address. Feeding leak locations and repair history back into a plant's broader maintenance and reliability data also helps identify whether certain fitting types, valve models, or installation practices are contributing disproportionately to the overall leak rate.
FAQs
Ultrasonic Leak Detection — Frequently Asked Questions
How accurate is the cost estimate a technician gets from an ultrasonic reading alone?
Decibel-based leak rate estimates are useful for prioritization purposes but should be treated as directional rather than precise, since the actual flow rate for a given decibel reading depends on factors like orifice shape, upstream pressure, and distance from the sensor at the time of the reading. Plants that want tighter cost figures for major leaks sometimes follow up high-priority findings with a more precise flow measurement before finalizing a repair business case, while using the ultrasonic estimate to build the initial prioritized backlog.
Can ultrasonic detection find leaks in systems that aren't under pressure at the time of the survey?
No — ultrasonic detection relies on the turbulent flow generated by pressure differential across an opening, so the system being surveyed needs to be pressurized and operating normally for a leak to generate a detectable signal. This is one reason surveys are often scheduled during normal operation rather than during a full plant shutdown, except for the specific case of testing isolated systems that remain pressurized during a partial outage.
How does ultrasonic testing differ from using soap solution to find leaks?
Soap solution testing works well for spot-checking a specific, already-suspected leak location at close range, but it's impractical for surveying large distribution networks or elevated piping, and it can't detect internal valve passing at all. Ultrasonic detection covers much larger areas efficiently and works on internal leaks that produce no visible bubbles, making it the more practical choice for structured, plant-wide survey programs.
Book a demo to see how survey coverage compares across detection methods.
Is ultrasonic leak detection useful for gas leaks other than compressed air and steam?
Yes — the same underlying principle applies to any pressurized gas system where a leak generates turbulent flow, including nitrogen, natural gas distribution, and various inert gas systems used in industrial processes. Detection sensitivity and safety precautions vary depending on the specific gas involved, particularly for flammable or hazardous gases, so equipment and procedures should be matched to the specific application.
How long does it typically take to see a return on a leak repair program?
Because most leak repairs are relatively low-cost — a fitting, a gasket, a valve reseating — compared to the continuous energy cost they eliminate, plants running a structured survey and repair program frequently recover the cost of the survey itself within the first several months, with ongoing savings continuing for as long as the repaired leaks stay fixed and new leaks are caught on a regular survey cycle.
MANUFACTURING & INDUSTRIAL AI · ENERGY EFFICIENCY
Build a Leak Detection Program That Actually Gets Tracked
iFactory helps you quantify, prioritize, and verify leak repairs across compressed air, steam, and valve systems, so savings don't quietly disappear back into the baseline.