Electrode cost is one of the few steel shop line items that moves every single heat, yet most mills only review it once a month on a cost report that arrives long after the furnace that drove the spike has already tapped a dozen more. A single percentage point of electrode consumption sounds small until it is multiplied across thousands of heats a year, and tip oxidation, side wall wear, and breakage rarely announce themselves until the stub is already short. Operators adjust power and current on instinct built from the last shift, not from a model of what actually consumed the graphite. Software that ties electrode wear back to power profile, current imbalance, and arc behavior turns a monthly surprise into a daily number. Mills comparing consumption against their own historical baseline can review a heat-by-heat electrode breakdown with the iFactory AI team.
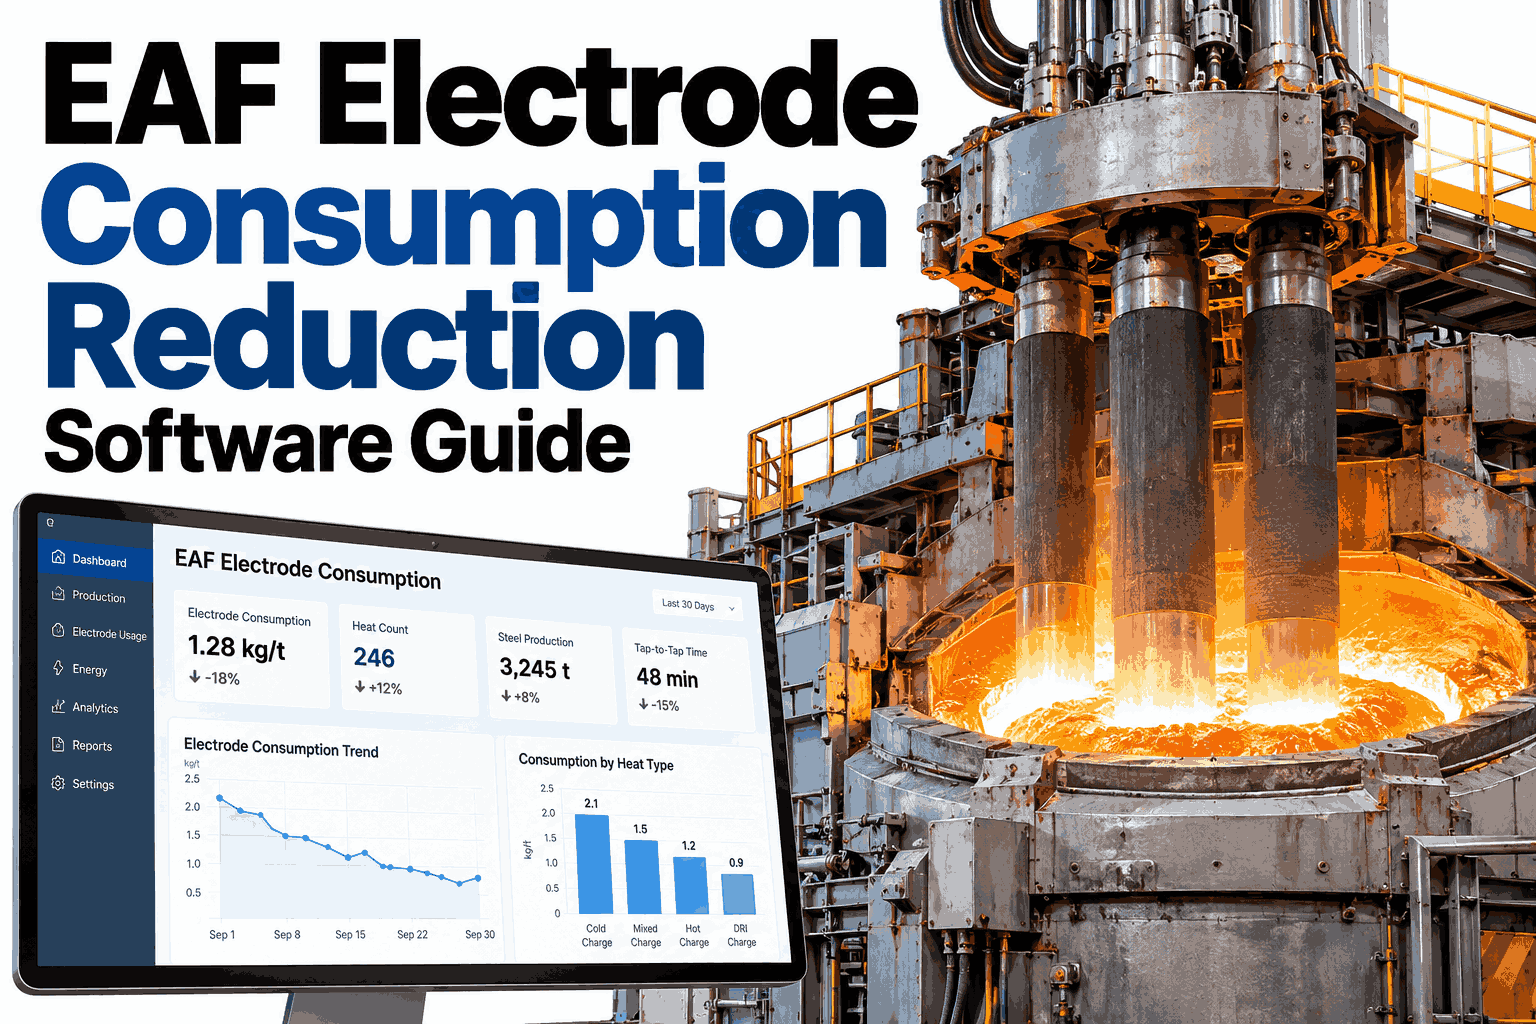
EAF Electrode Consumption Reduction Software Guide
iFactory EAF Energy AI tracks tip oxidation, side wall wear, and breakage root cause against power profile data, built on the iFactory EAF Energy AI and Power Profile Optimization foundation.
Three Ways Graphite Actually Disappears
Electrode consumption is not one phenomenon. It is three separate wear mechanisms stacked on top of each other, and each one responds to a different operating variable.
Tip Oxidation
The electrode tip reacts with oxygen and CO2 inside the furnace atmosphere, consuming graphite even when no current is flowing through it.
Side Wall Wear
Arc instability and current imbalance erode the column from the side, often invisibly, until the electrode diameter is thinner than the connection allows for.
Breakage
Thermal shock, mechanical stress during scrap collapse, or a weak joint snaps a section off in one event, the costliest and most sudden loss of the three.
A mill chasing one number, consumption per tonne, cannot see which of the three mechanisms is actually driving it.
What Drives Each Wear Mechanism
Each mechanism has its own set of operating variables, and a consumption model that treats them as one blended cost hides the lever that would actually fix it.
| Wear Mechanism | Primary Driver | Secondary Driver | Typical Share of Total Loss |
|---|---|---|---|
| Tip Oxidation | Furnace atmosphere and power-on time | Oxygen lancing practice | Roughly 60 to 70 percent |
| Side Wall Wear | Current imbalance between phases | Arc length and voltage tap selection | Roughly 20 to 30 percent |
| Breakage | Thermal cycling and joint integrity | Scrap charging practice | Roughly 5 to 15 percent, highly variable |
Shares vary by furnace design, scrap mix, and operating practice, which is why a mill's own data should set the baseline rather than an industry average.
A Composite Before and After, Shown as a Relative Index
A mid-size EAF shop tracked electrode cost per tonne before and after tying consumption data to power profile and current balance. Figures below are an illustrative composite, indexed to a starting point of 100.
The cost reduction came mostly from catching side wall wear early and correcting current imbalance before it compounded over several heats.
See Your Own Electrode Cost Broken Down by Cause
Book a 30-minute session and bring a month of heat data. iFactory EAF Energy AI will show which wear mechanism is driving your cost per tonne.
The Root Cause Path From Spike to Fix
A consumption spike on a cost report is an outcome, not a diagnosis. Tracing it back to a cause follows a consistent path once power and wear data are connected.
Flag the Heat
A heat with consumption above the rolling baseline is flagged automatically, instead of waiting for the end-of-month roll-up.
Pull the Power Profile
Voltage tap, current per phase, and power-on time for that heat are laid against the furnace's normal operating envelope.
Check Current Balance
An imbalance between phases points toward side wall wear rather than tip oxidation, narrowing the likely mechanism fast.
Cross-Check Scrap and Oxygen Practice
Scrap mix, charging pattern, and oxygen lancing for the same heat are reviewed for anything that would explain a tip oxidation spike.
Confirm With Physical Inspection
A crew check on the electrode confirms whether wear matches the data-driven hypothesis before any operating change is made.
Close the Loop
The operating adjustment, whether a tap change or a lancing practice fix, is recorded and tracked against the next several heats.
Without a logged path, the same root cause tends to resurface every few months because the fix was never confirmed against follow-up data.
Breakage Root Cause: Guesswork vs Tracked Evidence
A broken electrode is expensive and disruptive, and the instinct is to blame the last obvious event. Tracked evidence usually tells a different story.
Guesswork After a Break
Tracked Breakage RCA
Breakage is the smallest share of total electrode loss by volume, but it carries the highest cost per event and the most downtime risk.
What iFactory EAF Energy AI Adds
iFactory AI is smart manufacturing and industrial software built on the EAF Energy AI and Power Profile Optimization foundation, connecting electrode wear to the power data that explains it.
iFactory AI arrives pre-configured on an NVIDIA server that ships racked and ready with software pre-loaded. Rack it, connect power and Ethernet, and heat data starts flowing. Scope covers cabling, network, ERP and MES integration, team training, and 24x7 remote monitoring.
Electrode Program Self-Check
Use these checks to find where your electrode cost tracking depends on a monthly report instead of a daily, heat-level signal.
Each unchecked box is a place where electrode cost is likely drifting without anyone seeing the cause until the invoice arrives.
Frequently Asked Questions
How is electrode consumption actually calculated per heat?
Consumption is derived from electrode length or weight change between heats, adjusted for the number of columns added, and tied to that heat's power and scrap data. Ask how consumption is calculated for your furnace setup.
Can this reduce electrode cost without changing the electrode supplier?
In most cases, yes. The larger share of consumption loss tends to come from operating practice and current imbalance rather than the graphite grade itself, so the first gains usually come from the furnace side. See where your own losses are concentrated.
Does this replace the existing power profile optimization system?
No, it builds on it. Electrode tracking uses the same power profile data that drives energy optimization, so the two work from one connected data set rather than two separate systems.
How quickly can a current imbalance be caught before it causes wear?
Imbalance trending is monitored heat to heat, so a drifting phase is flagged within a shift rather than discovered after several heats of accelerated side wall wear. Talk through imbalance thresholds for your furnace.
What data does the mill need to have before starting?
A few months of heat records covering power profile, electrode additions, and any available breakage history give a strong starting baseline, though the system continues to refine thresholds as more heats are logged. Plan a data readiness review before kickoff.
Turn Electrode Cost Into a Daily, Traceable Number
iFactory EAF Energy AI connects tip oxidation, side wall wear, and breakage back to power profile data for every heat. Book a walkthrough using your own furnace data.