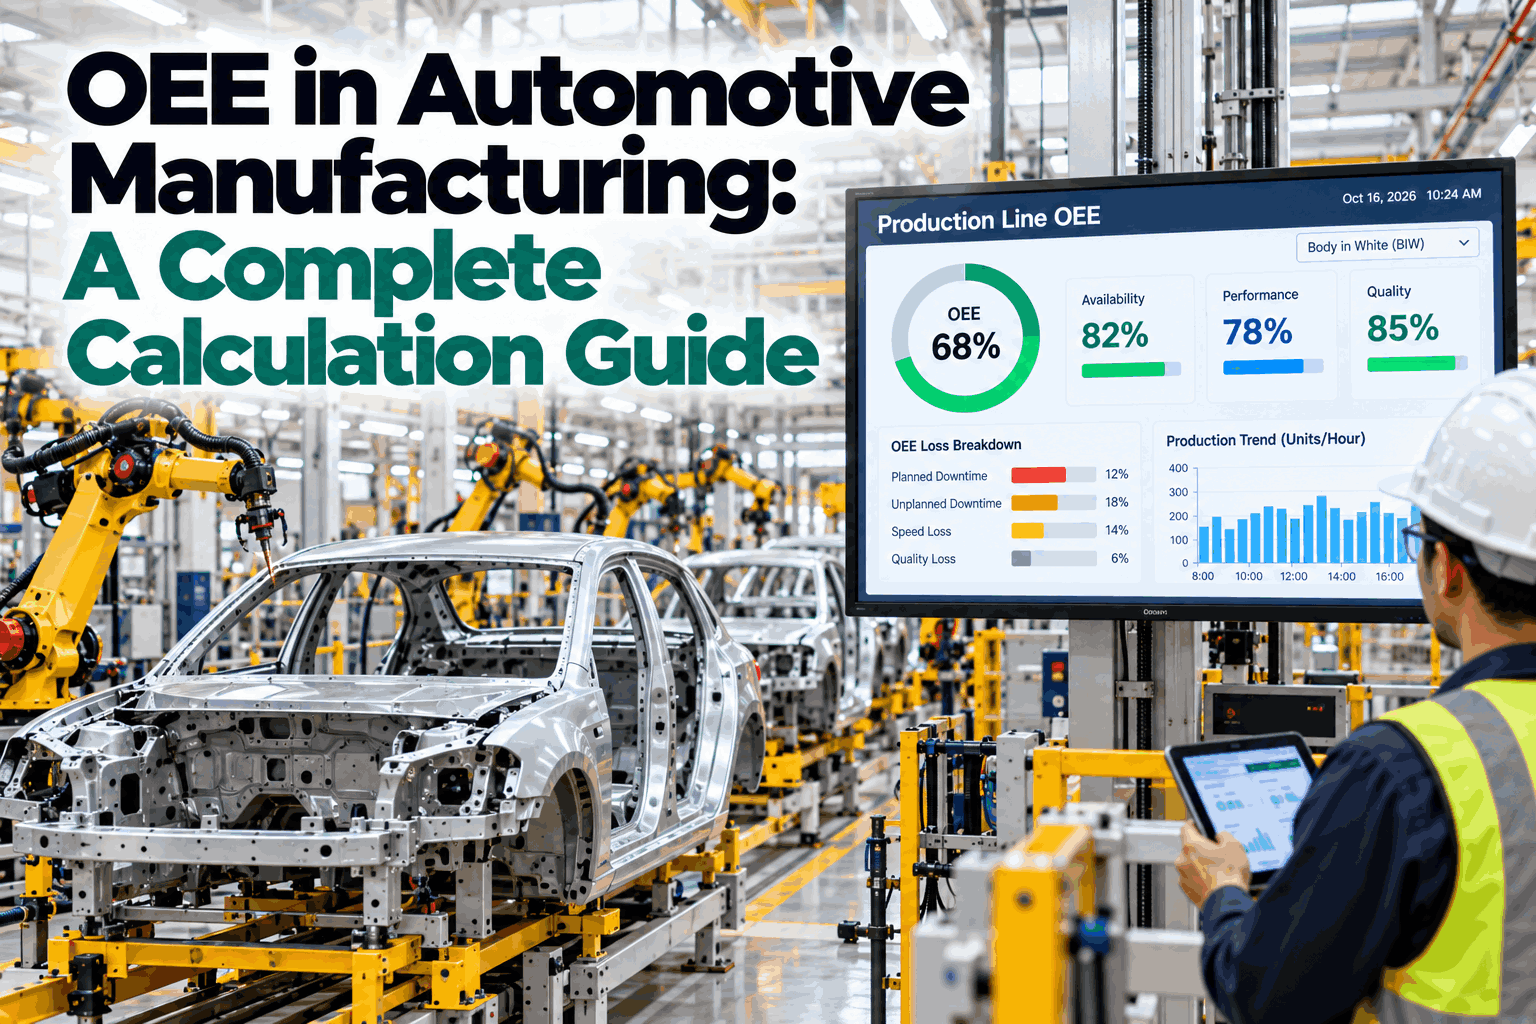
Every car plant reports OEE. Far fewer can explain how the number was reached, or why the press shop and the paint shop seem to use different rules. They do use different rules, and they should. A press counts strokes. A paint line counts bodies that pass inspection without repair. The formula is the same in every shop, but what you feed into it is not. This guide walks through the calculation step by step, with a worked example for stamping, body, paint and assembly, and the mistakes that most often bend the result. To check your own figures against it, book an OEE review.
OEE in Automotive Manufacturing: A Complete Calculation Guide
One formula, four shops, four ways of counting. See how to calculate OEE in stamping, body, paint and assembly so the numbers can be trusted.
- The formula in plain words
- A worked example for each of the four shops
- Seven mistakes that make OEE look better than it is
Did it run when it should?
Did it run at full speed?
Was it right first time?
The three multiplied
The whole calculation on one line. Everything else in this guide is about what goes into each box.
The Formula, in Plain Words
Three questions, each answered with a fraction.
OEE asks whether the equipment ran when it should, whether it ran at full speed, and whether what it made was right first time. Multiply the three answers and you have OEE. There is also a short cut: good units, times the ideal time for one unit, divided by planned time. It gives the same result, but hides which of the three is hurting you. Our support team can check your formula against this one.
Take out before you start
- Shifts with no production scheduled
- Meal and rest breaks, if the line stops for them
- Maintenance planned in advance
What is left is planned production time. It is the bottom of the availability fraction.
Leave in, and count as a loss
- Die changes and colour changes
- Waiting for parts, people or a quality decision
- Cleaning or adjustment needed to keep running
These are real losses. Moving them into planned time is the easiest way to flatter the score.
OEE measures against the time you planned to run. A related measure, TEEP, measures against every hour on the calendar, all day and all week. A two-shift plant can have a strong OEE and a low TEEP at the same time. Use OEE to judge how well a shop runs, and TEEP to judge how much spare capacity the plant still has.
Why Each Shop Counts Differently
Same formula. Different unit, different ideal rate, different meaning of good.
A press line makes thousands of parts a shift and changes dies several times. A paint line moves bodies at a fixed pace and almost never stops. An OEE rule written for one will mislead in the other. Before any calculation, agree three things for each shop: what is counted, what the ideal rate is, and what counts as good. To set these for your plant, book a working session.
A body shop line can stop because the next line is full, or because nothing has arrived from the last one. That is not the line's own fault, but the plant still lost the bodies. Record blocked and starved time as its own category. Then decide once whether it counts against the line, and apply the same rule in every shop.
Four Worked Examples, One for Each Shop
One shift, 450 planned minutes, worked through four times.
The figures below are illustrative, chosen to be easy to follow with a calculator. Each card shows the three fractions and the result. Put your own numbers in the same places and you have your OEE. If your result disagrees with your current report, ask our OEE specialists to look at why.
Stamping
Counts partsOne press line, rated at 14 strokes a minute.
Biggest loss: two die changes, 44 of the 70 minutes stopped.
Body shop
Counts bodiesOne weld line, designed for 60 bodies an hour.
Of 63 minutes stopped, 23 were blocked or starved, not the line's own faults.
Paint
Counts bodiesOne topcoat line, designed for 50 bodies an hour.
The line hardly stopped. One body in five needed repair, and that is the loss.
Assembly
Counts vehiclesOne final line, designed for 60 vehicles an hour.
A paced line runs at full speed or not at all, so speed loss is small. Repairs are not.
Worked examples with made-up figures, not data from a named plant. Notice how the weakest factor moves: stops in stamping and body, quality in paint and assembly.
How to read a result
Availability is lowest
Look at stops. Rank them by total minutes, and start with changeovers and the longest breakdowns.
Performance is lowest
Look at short stops and slow running. These rarely reach a manual log, so they need automatic counting.
Quality is lowest
Look at first-time results. Sort repairs by defect type and by the station that caused them.
The Short-Cut Check
One line of arithmetic that should always agree with the long way. If it does not, one of your three fractions is using the wrong figure.
Seven Mistakes That Bend the Number
Each one makes OEE look better. None of them makes a single extra car.
Most wrong OEE figures are not dishonest. They come from small choices made years ago that nobody has revisited. The seven below are the ones we would look for first in a car plant. To test your own rules against them, book a rules check.
Using takt as the ideal rate
Takt follows customer demand. The ideal rate is what the line was built to do. Use the design rate.
Counting repaired units as good
A body that needed polishing or a weld repair was not right first time. It fails the quality fraction.
Calling changeovers planned
Die and colour changes are losses, even when scheduled. Hide them and nobody works on them.
Missing the short stops
A robot that faults for forty seconds, fifty times a shift, rarely reaches a manual log.
One ideal rate for every part
A deep-drawn panel runs slower than a flat bracket. Each part and die needs its own rated speed.
Averaging the four shops
The shops count different units and sit behind buffers. An average of their scores means nothing.
Accepting performance over 100%
It means the rated speed is set too low. Fix the rate. Do not cap the score.
Do not multiply or average the shop scores. For the plant, count vehicles that left the end of the line right first time, and divide by what the plant was designed to build in the planned time. Then use the four shop scores to see which shop is holding that figure back.
Benchmarks by Shop, and Where to Start
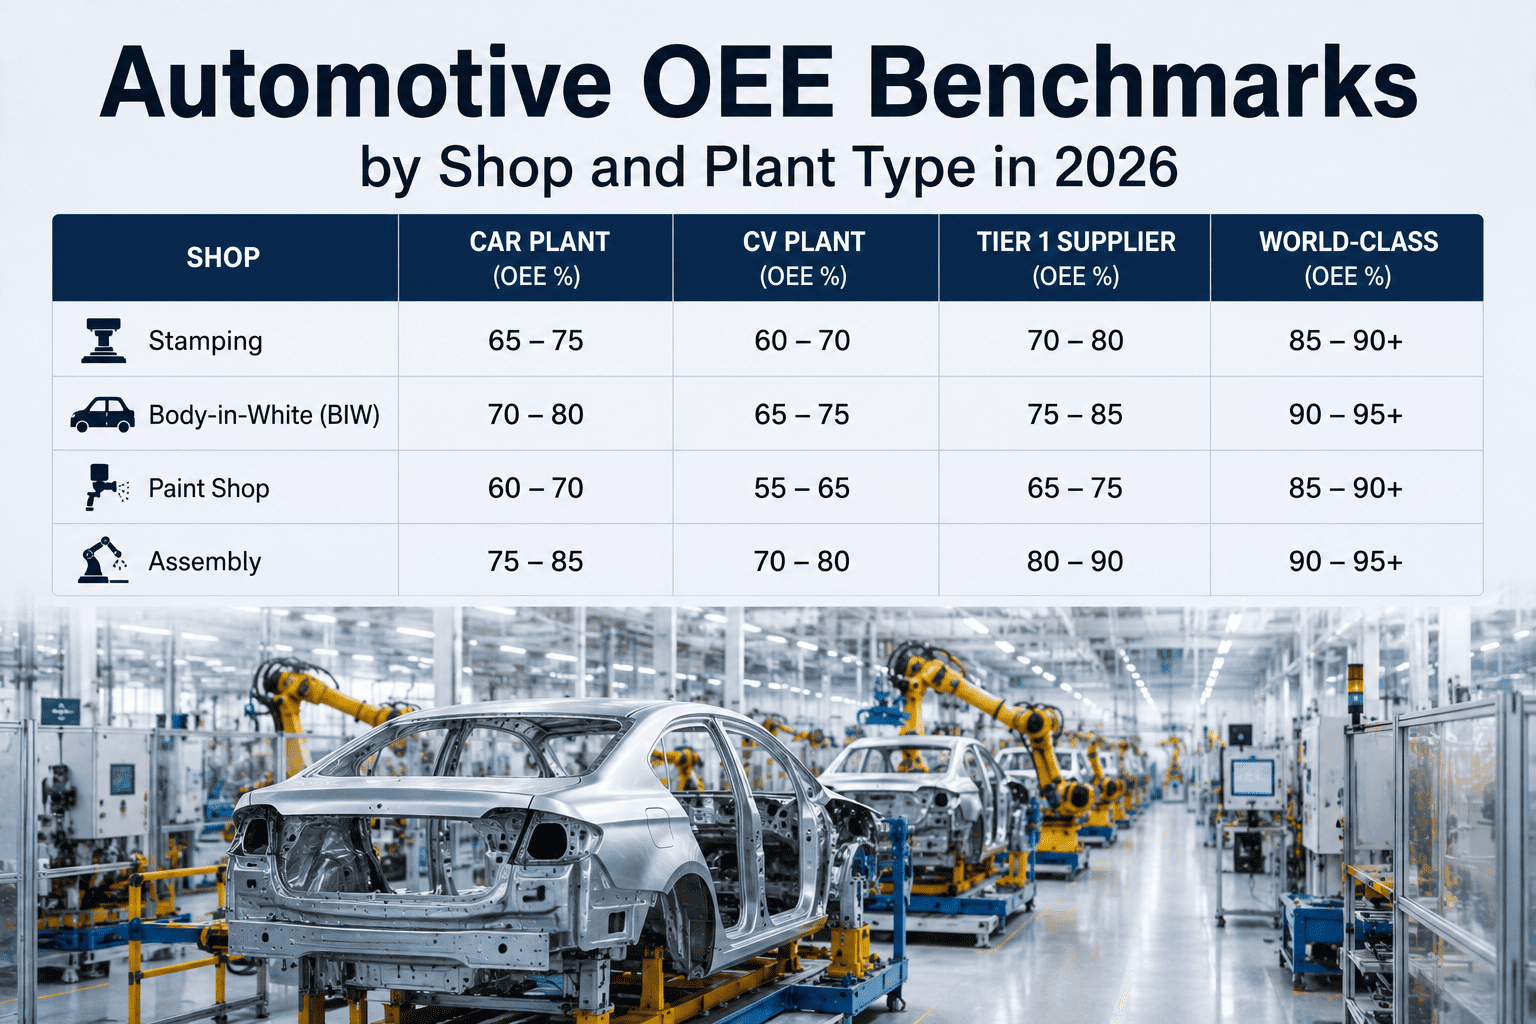
85% is not the target for every shop. Paint will never look like assembly.
The famous 85% came from Japanese car plants in the 1970s, and OEE.com itself warns it does not fit every process. The ranges below come from iFactory's own benchmark guide. Treat them as a rough map, not an audited survey. Your own best month on the same model mix is a better yardstick. iFactory calculates OEE for each shop by its own rules, from machine signals. Our integration team can confirm what your lines already report.
The first thing to work on, by shop
Stamping
Die change time. Time it from last good part to first good part, and shorten it.
Body shop
Short robot faults. Count every one by station, then fix the top three.
Paint
First-time quality. Log each repair by defect and booth to find the source.
Assembly
Line stops and end-of-line repairs. Trace each repair back to its station.
What automotive OEE software has to do
- Count automatically. Units, stops and speed from the machine, not from a clipboard.
- Hold a rate for each part. By die, model and line.
- Keep blocked and starved apart. So each shop sees its own losses.
- Take quality from inspection. First-time results, not final counts.
iFactory shows the calculation behind every score, so it can be checked by hand.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready, with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network.
Our team handles cabling, network setup, PLC and SCADA integration, operator training and 24×7 remote monitoring. The server sits inside your own network, so production and quality data stay on site. For a scope matched to your shops, request a turnkey quote.
Ship, network and data
Server installed. Press, robot, conveyor and inspection signals connected. Counting rules agreed for each shop.
Model training and pilot
One shop live. Automatic OEE compared with the current report, and every gap explained.
Go-live and training
Remaining shops added. Supervisors and managers trained. 24×7 remote monitoring begins.
Frequently Asked Questions
What is the OEE formula?
OEE is availability times performance times quality. Availability is run time over planned time. Performance is units made over units possible in the run time. Quality is units good first time over units made. The short form is good units over units possible in planned time.
What is a good OEE for an automotive plant?
It depends on the shop. 85% is often called world-class and about 60% is often quoted as typical, but neither is an audited automotive figure. Paint usually scores lower than assembly for sound reasons. Compare each shop with its own best month first.
Should takt time be the ideal cycle time?
No. Takt is set by customer demand and changes with the schedule. The ideal cycle time is the fastest the equipment was designed to run that part. Using takt hides slow running whenever demand is low, and can push performance over 100%.
Do repaired vehicles count as good?
Not in the quality fraction. OEE quality means right first time. A vehicle that was repaired and then sold is good for the customer, but the repair used time, people and space. Counting it as good hides the largest loss in paint and assembly.
Are die changes planned downtime?
They are scheduled, but they should stay inside planned production time and count as an availability loss. That keeps changeover time visible and worth reducing. Only time with no production scheduled, breaks and planned maintenance come out before the calculation.
How do we get one OEE for the whole plant?
Do not average the shops. Count vehicles that left the end of the line right first time, and divide by what the plant was designed to build in the planned time. Use the shop scores to find which shop limits that figure.
How long does automatic OEE take to set up?
Six to twelve weeks from delivery. We need a place for the server with power and Ethernet, read access to line signals, and time with each shop to agree its counting rules. To check your set-up first, contact our team.
Bring One Shift From One Shop
In thirty minutes we work through your own figures the same way as the cards on this page, and show where our result differs from your report. You keep the calculation whether or not you go further with iFactory.
- 1Shift length, breaks and planned maintenance
- 2The stop log, with changeovers marked
- 3Units made in the shift
- 4Units that passed first time, with no repair
- 5The rated speed or design rate you use today