Ask three people in an automotive plant for the OEE of the same line and you can get three answers. One counts breaks and changeovers as planned time, one uses the tool's design speed as the ideal cycle and one counts reworked parts as good. All three are calculating OEE, and none of them is lying. The number is only as accurate as three inputs: the planned-time definition, the ideal cycle time and the defect count. Fix those three and OEE becomes a figure the plant, the customer and the auditor can trust. To check yours, book an OEE accuracy review.
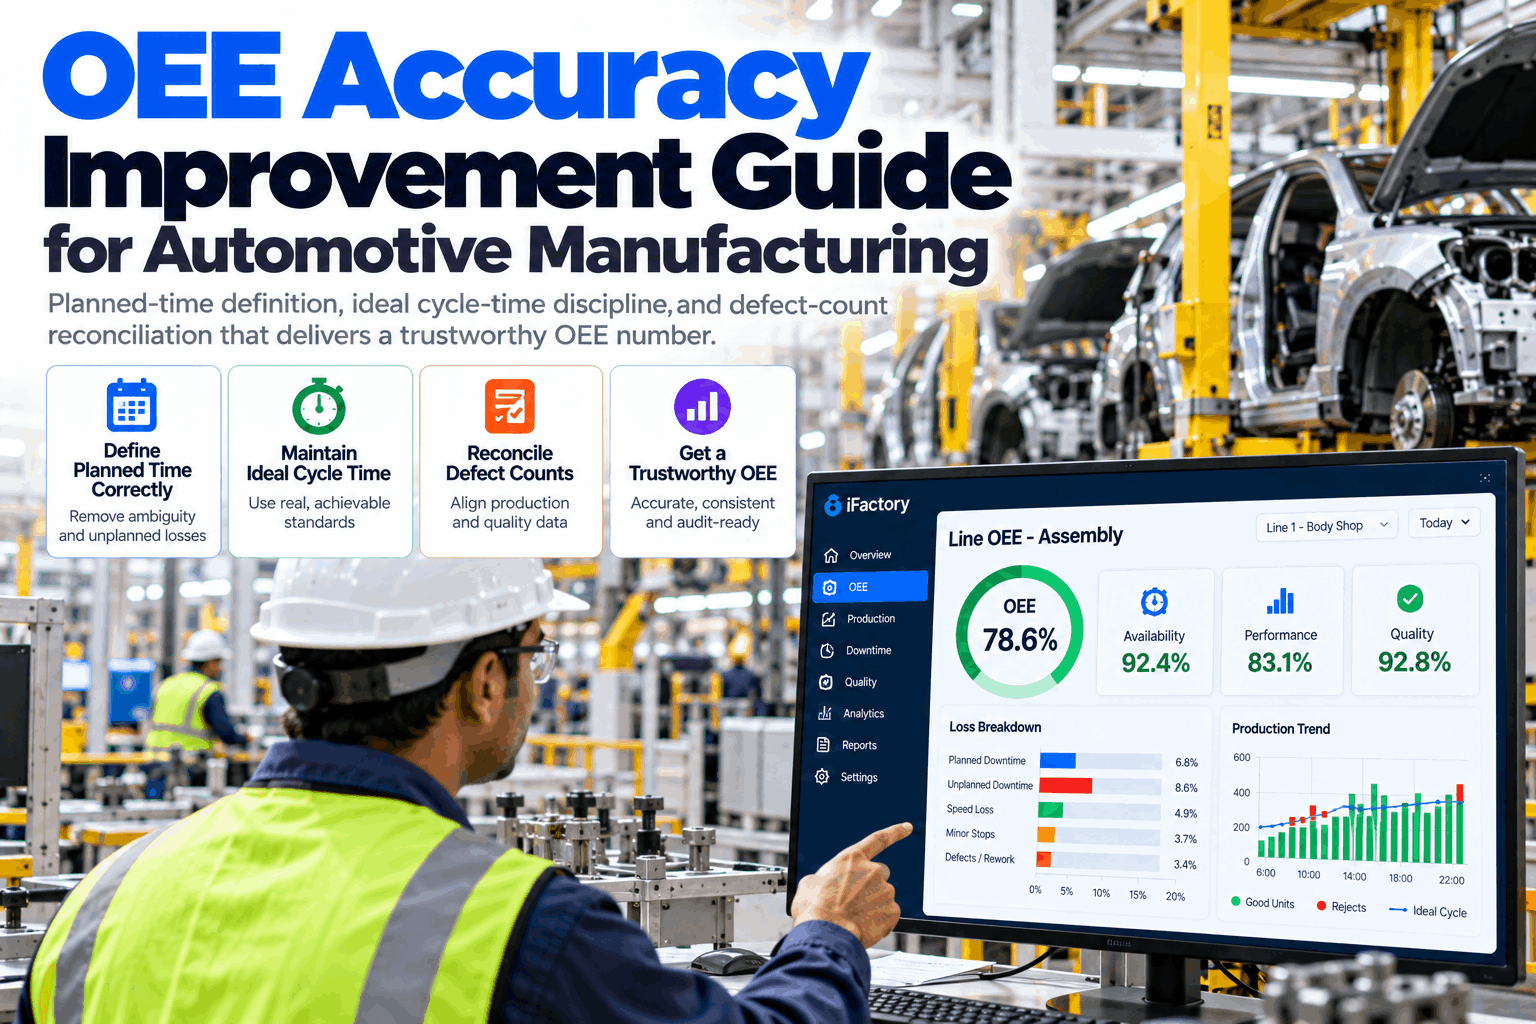
OEE Accuracy Improvement Guide for Automotive Manufacturing
A practical guide to the three inputs that decide whether automotive OEE can be trusted: how planned time is defined, how ideal cycle time is set and how defect counts are reconciled across systems.
- How to define planned time so losses stay visible
- How to set and protect ideal cycle times per part number
- How to reconcile scrap and rework across MES, quality and ERP
Four finding types explain more than four fifths of the overstatement. The first three are definition choices, not data faults, and can be fixed without new sensors. The dashed line marks where the cumulative share passes 80%.
Why Automotive OEE Is Often Wrong
The formula is simple. The inputs are where accuracy is won or lost.
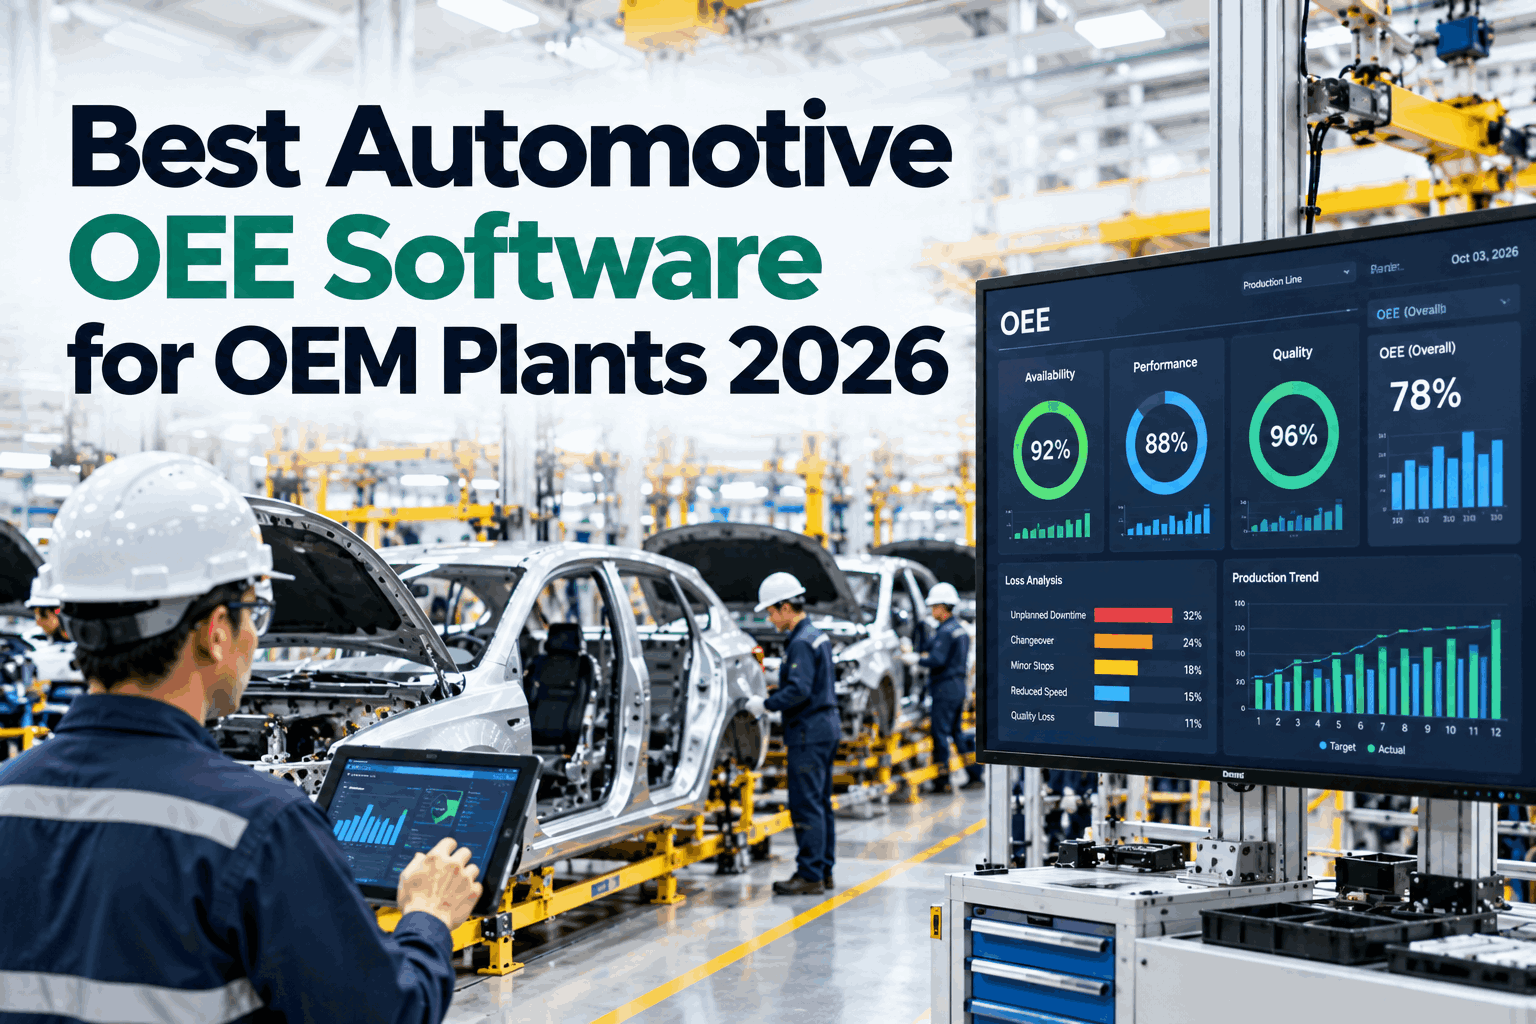
OEE multiplies availability, performance and quality, so a generous choice in any one of them lifts the final score. Automotive plants are especially exposed. They run many part numbers per line, with different cycle times and frequent changeovers, and they feed data from several systems that rarely agree. A score built on loose inputs also hides the real losses, so improvement effort goes to the wrong place. Our OEE team can review your definitions with you.
Planned time
What counts as available time sets the ceiling for everything else.
Ideal cycle
The reference speed decides how much performance loss is visible.
Defect count
Scrap and rework must match across every system that records them.
Time stamps
Machine events beat memory and rounded shift entries.
An accurate OEE will often be lower than the old one. That is a good sign. The gap is the hidden loss, and it is the pool of capacity you can recover without buying a machine.
Define Planned Time So Losses Stay Visible
If a loss is called planned, it disappears from OEE.
Some stops are truly outside the plan, such as scheduled breaks and no-demand periods. Others only look planned: long changeovers, material waits and quality holds. Treating them as planned removes the very losses OEE exists to expose. Write a rule for each category and apply it to every line. To review your rules, book a definition workshop.
OEE shows how well scheduled time is used. TEEP shows how much of all calendar time makes good parts. Reporting both keeps the plan decisions honest and shows how much capacity sits idle.
What a Nine-Point Overstatement Hides
An inflated OEE feels comfortable, but the lost capacity does not go away. It just stops being counted, and it stops being chased.
Ideal Cycle Time Discipline
The ideal cycle is the yardstick. If it moves, every result moves with it.
Performance only shows loss against a fixed, honest reference. When people quietly lower the ideal cycle to match what the line usually achieves, speed loss disappears from the report. Set the reference per part number, base it on the best demonstrated or designed rate and change it only through a recorded decision.
Weak practice
- One ideal cycle for the whole line
- Reference set from last month's average
- Edited without a record or approval
Strong practice
- Ideal cycle per part number and tool
- Based on design or best demonstrated rate
- Changes logged with owner and reason
Hold one master table of ideal cycles, owned by process engineering and reviewed each quarter or after a tooling change. A single source stops every line, plant and report from using a different yardstick.
Reconcile the Defect Count Across Systems
One part should be counted as good or bad once, in the same way, everywhere.
Automotive plants record defects in several places: the machine counter, the MES, the quality system and the ERP. These rarely match, because of timing, rework loops and different part definitions. The aim is a single reconciled good count that all four can agree on. This also supports management reviews and customer reports that depend on trusted performance data.
Count
Machine counts for total and rejected parts.
Match
Link counts to part number and time.
Classify
Scrap, rework and hold coded the same way.
Reconcile
Differences between systems explained.
Lock
Final good count frozen for the period.
Review
Gaps tracked and closed each month.
How iFactory Automotive OEE and Hidden Loss Analytics Works
Accurate OEE first, then the losses behind it.
iFactory collects machine states, counts and rejects from PLCs, applies your written rules for planned time and ideal cycle, and reconciles good counts with your MES and quality systems. It then breaks every point of lost OEE into its causes, so the hidden losses are ranked by hours and value. It runs on an on-prem server inside your plant network. Questions on fit go to our support desk.
Machine data
States, counts and rejects stamped by the machine.
Your rules
Planned time and ideal cycle per part number.
One good count
Matched across MES, quality and ERP.
Hidden losses
Micro-stops, speed loss and holds ranked by value.
Gains depend on your lines, part mix and how quickly the top losses are acted on. We measure OEE accuracy and recovered capacity on your own data during the pilot, rather than promising a general figure.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our team handles cabling, network setup, PLC, MES and SCADA integration, operator training and 24×7 remote monitoring. Data stays on your own network. For a scope matched to your plant, request a turnkey quote.
Ship, network and data
Server installed. Machine data, MES and quality records connected for the pilot line.
Rules and reconciliation
Planned time, ideal cycles and good counts agreed and tested against past data.
Go-live and training
Reconciled OEE and loss views live. Teams trained. 24×7 remote monitoring begins.
Frequently Asked Questions
What makes OEE inaccurate in automotive plants?
Mostly three inputs: a planned-time definition that hides losses, an ideal cycle set too low, and defect counts that differ between the machine, MES and quality system.
Should changeovers count as planned time?
We suggest counting them as an availability loss and tracking them separately. They are often the biggest recoverable loss on lines that make many part numbers.
How should the ideal cycle time be set?
Per part number and tool, from the design rate or the best demonstrated rate. Changes should be recorded with an owner and a reason, so the reference does not drift.
Should reworked parts count as good?
For OEE, count only first-pass good parts as good, and show rework as its own loss. That keeps hidden repair effort visible and comparable between lines.
Will our OEE go down after the audit?
Often, yes. A lower number is usually a more honest one. The gap is the hidden loss, and it points to where capacity can be recovered.
How do we start?
With one line and a written list of its planned-time rules, ideal cycles and defect sources. A 6-week pilot connects the data, tests the rules and shows the reconciled number. To plan it, contact our team.
Make Your OEE a Number People Trust
In thirty minutes we look at how you define planned time, set ideal cycles and count defects today. You keep the notes whether or not you go further with iFactory.
- 1Your current OEE definition and reports
- 2The ideal cycle times in use per part number
- 3Your shift pattern and planned downtime rules
- 4Scrap and rework data from MES and quality
- 5The lines where the number feels wrong