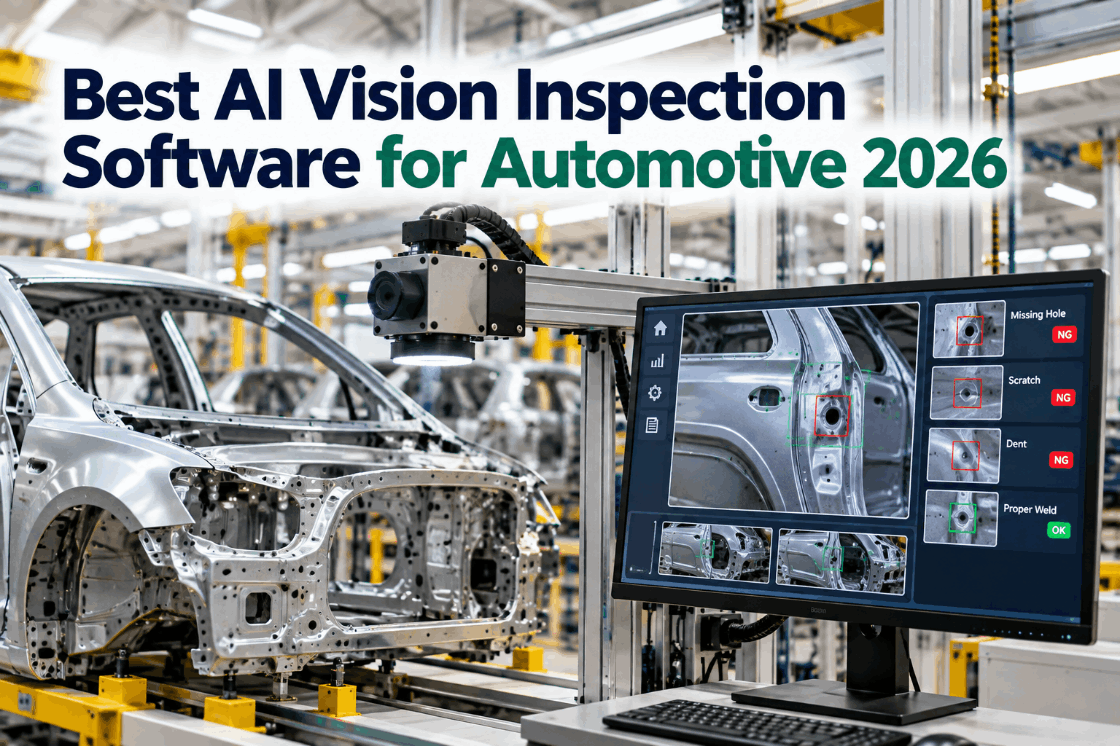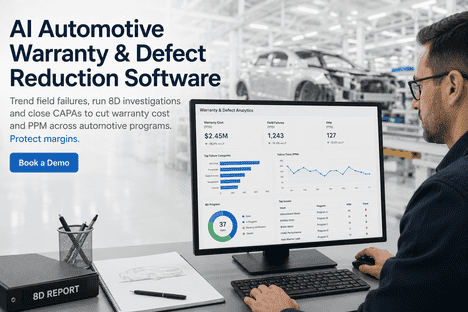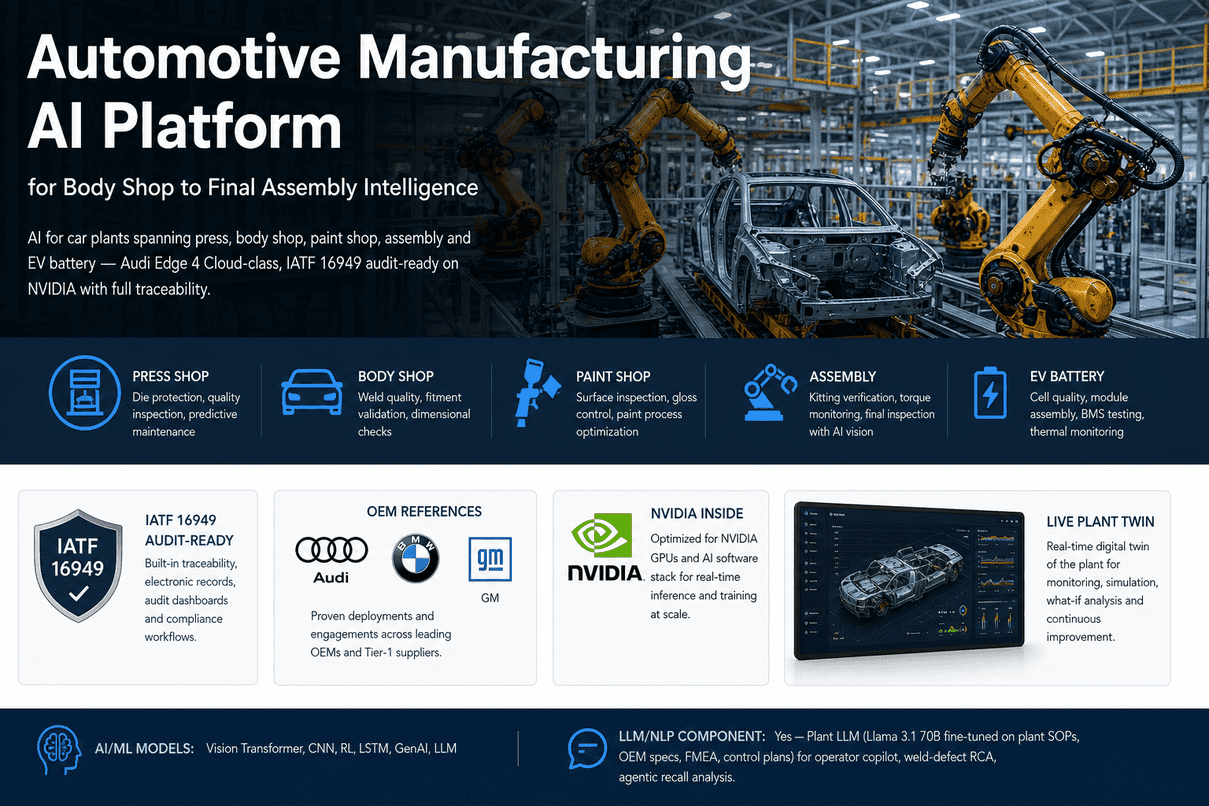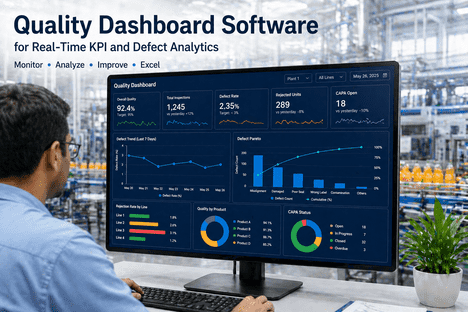
OEE was invented to judge a single machine. A vehicle plant is nothing like a single machine: it is a press shop, a body shop, a paint shop and an assembly line, joined by buffers and paced by one customer order after another. Put one OEE percentage on all of that and it hides far more than it shows. This guide explains what OEE software has to do differently in an OEM plant, the five kinds on the market in 2026, how to score them fairly, and where iFactory fits. Siemens puts an hour of unplanned downtime at a large automotive plant at $2.3 million, so the choice is worth getting right. To look at your own lost minutes first, book a loss review.
Best Automotive OEE Software for OEM Plants 2026
Availability, performance and quality mean something different in every shop. The best software knows that, and shows where the hidden minutes go.
- OEE explained shop by shop, in plain words
- Five kinds of software, compared without a ranking
- A scorecard you can use with any vendor
Loses time to die changes.
Loses time to short stops.
Loses time to repaint loops.
Loses time to line stops.
Four factories under one roof. Each loses time in its own way, and each needs OEE measured in its own way.
Why One OEE Number Fails an OEM Plant
A plant-wide percentage tells you something is wrong. It cannot tell you where.
The three parts of OEE stay the same everywhere: was the equipment running, was it running at full rate, and was the output good? What changes from shop to shop is what each of those questions means, and where the losses hide. Software that treats a paint booth like a press will give you tidy numbers and wrong answers. Our support team can map this for your shops.
Three numbers that each look healthy multiply into one that does not. That is the point of OEE, and also why the split matters more than the total.
A station that is waiting for bodies is starved. A station that cannot pass its work on is blocked. Neither has anything wrong with it, yet simple OEE tools count both as downtime for that station. Good automotive software keeps them separate, and follows the chain back to the station that actually stopped.
What "Tuned for Automotive" Really Means
Six abilities separate OEE software built for vehicle plants from software built for machines.
Most OEE tools were designed for a machine that makes one part at a steady cycle. A vehicle line makes a different car every minute, with thousands of robots and almost nobody free to type a stop reason. Use these six as a first filter. To see them on your own line data, book a working session.
Takt, not machine cycle
Performance is measured against the line rate in vehicles an hour, for the mix running today.
Starved and blocked kept apart
Waiting time is traced back to the station that caused it, not charged to the one that waited.
Aware of variants
A long-wheelbase body or a three-coat colour takes longer. The target should move with the sequence.
Quality by vehicle
First time through is counted for each body and each vehicle, not as a daily scrap total.
Stop reasons without typing
Causes come from controller fault codes and line signals. Operators confirm; they do not write.
Bottleneck and buffers
The software shows which shop limits output right now, and how full each buffer is.
The shift log recorded the 22 minutes of line stops. The other 62 lost minutes appear nowhere on paper.
The hidden losses, in plain words
- Short stops. Too brief to log, too many to ignore.
- Slow running. The line moves, a little under rate, all shift.
- Waiting. Good stations idle because of trouble elsewhere.
- Second passes. A body repainted has used the booth twice.
- Wrong causes. A stop blamed on the nearest station, not the real one.
None of these is a breakdown. Together they are often the larger share of lost output.
Five Kinds of OEE Software in OEM Plants
We compare kinds, not brands. No vendor should mark its own exam.
You will meet five kinds of product. Each is strong at something, and none does everything. The examples are real, and what we say about them comes from each company's own published material. Ask our automotive specialists which kind suits your plant, even if the answer is not ours.
What the companies themselves say
Siemens Opcenter
Aimed at car OEMs and complex first-tier suppliers: variant handling, quality gates along the line and just-in-time messaging.
DELMIA Apriso
A manufacturing operations suite built to roll one set of processes out across sites worldwide.
Vorne XL
A device that fits onto an existing process, with no software to install and no recurring fees, according to the vendor.
Dürr DXQ
Digitises more than 120 paint process steps and uses AI to find fault patterns that hurt first-run rate.
Volkswagen
43 of 114 sites connected to its own platform, with more than 1,200 AI applications across the group.
How to read these
As descriptions, not as results. Ask each vendor for a plant like yours that you can call.
What a Lost Minute Costs
These are Siemens estimates for large plants, not your figures. They explain why a few hidden minutes a shift deserve a proper look.
How to Choose: A Scorecard, Not a Ranking
Score every vendor on the same seven lines. The weights are yours to change.
A list of "best" products cannot know your plant. A scorecard can. Give each vendor a mark out of five on each line, multiply by the weight, and add up. Then ask for evidence on any line where the score surprised you. To fill one in against your own requirements, book a scoring session.
Suggested weights that add up to 100. A plant with an MES already in place might move points from fit to bottleneck logic.
Pick one line. For two shifts, have someone tally every stop by hand with a stopwatch while the software records the same line. Compare the two lists. If the software found the short stops the tally found, and named causes a supervisor agrees with, it understands your line. If not, no demonstration will fix that.
Where iFactory Fits
Beside your MES, not instead of it.
iFactory is the fifth kind in the list above. It reads the controllers, MES and quality systems you already run, measures each shop in its own terms, and shows where the hidden minutes went and why. It advises; your line controls stay as they are. Our integration team can confirm what your plant already provides.
A good fit when
- You have an MES or line controls, and still cannot explain your lost minutes.
- You want all shops on one board, with the bottleneck shown.
- Short stops and waiting time are not being captured today.
- Plant data has to stay on your own network.
Look elsewhere first when
- You need sequencing, work instructions and material calls. That is an MES suite.
- You have one machine and a small budget. A stand-alone device will do.
- Your only question is paint process quality. Start with the paint shop builder.
In each case iFactory can sit above that system afterwards.
One set of data, three views
- Team leader. My zone this shift: stops, causes and what to fix first.
- Shop manager. My shop against plan, with starved and blocked time shown apart.
- Plant manager. Every shop on one board, the bottleneck, and the trend.
All three see the same minutes, so the morning meeting starts from agreed facts.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready, with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network.
Our team handles cabling, network setup, PLC and SCADA integration, operator training and 24×7 remote monitoring. The server sits inside your own network, so production data stays on site. For a scope matched to your plant, request a turnkey quote.
Ship, network and data
Server installed. Controllers, MES counts and quality results connected for one line. Loss categories agreed with the shop.
Model training and pilot
Stop causes learned from fault codes. Software results compared with a manual tally for two shifts, then tuned.
Go-live and training
Shop and plant boards go live. Team leaders and managers trained, shift by shift. 24×7 remote monitoring begins.
Frequently Asked Questions
What does OEE mean in an automotive OEM plant?
The same three questions as anywhere: was the equipment running, was it at full rate, and was the output good? The difference is that each shop answers them in its own way. A press counts strokes, a body shop counts jobs an hour, paint counts bodies right first time, and assembly counts vehicles against takt.
What is a good OEE for an OEM plant?
There is no trustworthy public figure for a whole vehicle plant. The well-known 85% was set for single machines decades ago. Compare each shop with its own past, and with sister plants that measure the same way. A steady gain on your own baseline is worth more than a borrowed target.
Why keep starved and blocked time separate?
Because the waiting station is not the one with the problem. If its waiting time is counted as its own downtime, maintenance is sent to the wrong place and the real cause is left alone. Separating the two points attention at the station that actually stopped.
Do we have to replace our MES?
No. An MES runs production: sequence, work instructions, material and records. OEE and loss analysis can sit above it and read its data. Many plants keep their MES and add analysis, since changing an MES is a multi-year project and finding lost minutes should not wait for it.
How are stop reasons captured without operators typing?
From the controllers. Robots, conveyors and stations already raise fault codes and state signals. The software reads them, groups them into causes people recognise, and asks an operator only to confirm the cases it cannot work out. That is the only way to catch stops that last seconds.
Is OEE the right measure for final assembly?
Only in part. Assembly is paced by takt and depends heavily on people and parts supply. Most plants watch vehicles an hour, first time through and line-stop minutes beside OEE. Good software shows all four from one set of data, so nobody argues about which is right.
How long does it take to go live?
Six to twelve weeks from delivery for a first line. We need a place for the server with power and Ethernet, read access to controllers and MES data, and time with the shop's team leaders. To check your set-up first, contact our team.
Bring One Line and One Bad Shift
In thirty minutes we take a shift that went badly and walk through where the minutes went: stops, slow running, waiting and repairs. You keep the breakdown whichever software you choose.
- 1The shift report for one bad shift
- 2Planned and actual vehicles by hour
- 3How OEE is worked out today, in each shop
- 4Your MES and controller makes
- 5The stops your supervisors complain about most