A mixed-model assembly line builds different vehicles one after another: a base sedan, then a premium SUV with a sunroof, then an estate with a tow hitch. The order matters. Too many heavy variants in a row overload stations. Too many colour changes waste paint and time. A sequence that ignores what suppliers are delivering breaks just-in-sequence timing for Tier 1 partners. Model mix scheduling decides that order. This guide explains the constraints that shape a good sequence, how ratio rules and colour batching compete, how supplier sequence fits in, which optimization methods work and how to measure sequence quality. To see model mix optimization on your line, book a short walkthrough.
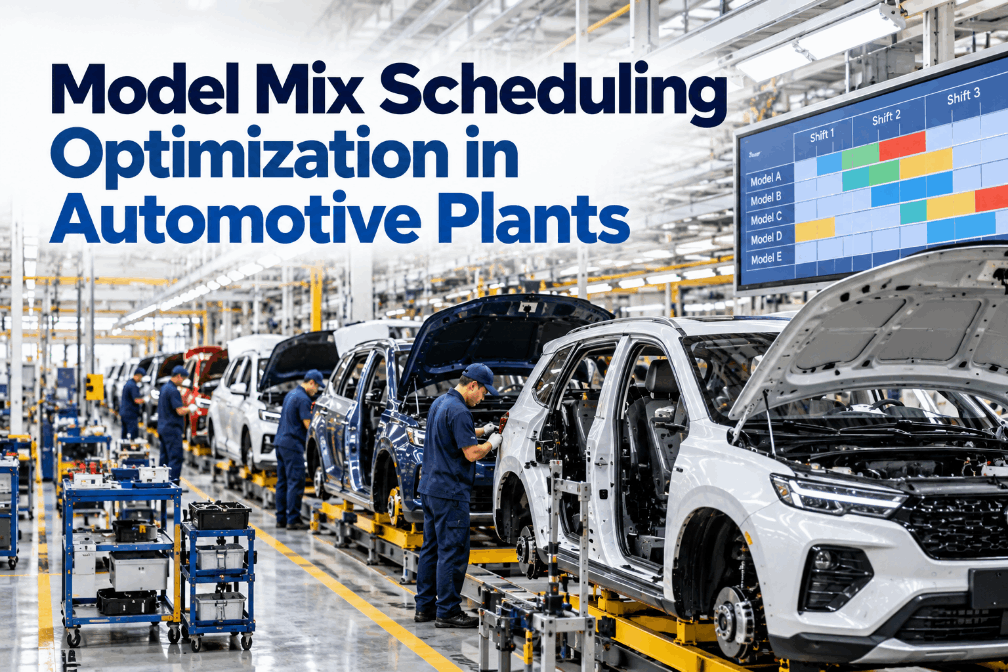
Model Mix Scheduling Optimization in Automotive Plants: Protect Tier 1 Sync and Final JPH
Ratio rules, colour blocks, work content and supplier sequence balanced in one optimized sequence, so heavy variants never pile up and JIS partners receive what the line will build.
Why the Order of Vehicles Matters So Much
Mixed-model lines let plants build many variants on one line, but they only work if the sequence respects each station’s capacity. When three sunroof vehicles arrive in a row at a station designed for one in two, the operator falls behind, the line stops or the work is left for rework. When the paint shop receives bodies in constantly changing colours, it spends time and paint on purging. When suppliers deliver seats in one order and the line builds another, parts are missing at the station.
This is a well-studied problem. Renault posed its version, the car sequencing problem with ratio constraints and paint colour batches, as the ROADEF challenge in 2005, and it remains a benchmark for optimization research. In a real plant the problem is harder still, because the sequence must also work for suppliers and adapt when things go wrong.
A well-optimized sequence protects line speed, paint efficiency and supplier sync at the same time. We can look at your current sequencing rules on a call.
The Constraints That Shape a Sequence
A sequence has to satisfy several kinds of constraint at once. Some are hard limits; others are preferences with costs.
Ratio rules and material availability are usually hard constraints; colour batching and work content balance are often weighted objectives. Getting those weights right is a business decision, which our planners help you make.
How Ratio Rules Work in Practice
Ratio rules are simple to state and hard to satisfy together. Here is an illustrative check on a short sequence.
Illustrative. Real sequences apply many ratio rules at once, which is why optimization software is needed.
Rules are not always strict limits. Some stations can absorb a short burst of heavy variants using a floater or a longer station zone, so rules may allow occasional exceptions at a penalty rather than forbidding them outright. Capturing that nuance lets the optimizer use real flexibility instead of treating every rule as absolute.
Each option with extra work has its own rule, and the rules interact. A swap that fixes the sunroof rule might break the tow hitch rule or split a colour block. That interaction is what makes manual sequencing slow and error-prone at scale.
Ratio rules should come from the line balance, and be revised when the balance changes. Our engineers derive them from your station work content.
Ratio Rules Versus Colour Blocks
The central tension in automotive sequencing is between assembly and paint.
- Fewer paint changes and purges
- Lower paint and solvent use
- Better paint shop throughput
- Risk of options clustering together
- Assembly stations may overload
- Resequencing needed after paint
- Options spread evenly for assembly
- Stable work content for operators
- Protects final assembly JPH
- More colour changes
- Higher paint cost and purge waste
- Paint shop may become the constraint
The cost of each side is measurable. Paint changes cost purge solvent, paint and time; assembly overload costs stops, rework and overtime. Putting both in the same units, usually cost per vehicle, lets the optimizer weigh them honestly rather than by habit or by whichever department argues hardest.
Many plants resolve this with a painted body storage between paint and assembly. Bodies are painted in colour blocks, then resequenced in storage to meet assembly ratio rules. The size of that storage limits how much freedom each side has.
Optimization finds the best balance for your plant’s cost of paint changes, assembly overload and storage capacity. See the trade-off curve in a demo.
Keeping Tier 1 Suppliers in Sync
Just-in-sequence suppliers build and deliver parts in the order the line will use them. The model mix sequence is their schedule.
The build sequence is fixed for the frozen horizon.
JIS call-offs sent to suppliers with vehicle, variant and position.
Seats, cockpits or bumpers built in sequence at the supplier.
Parts delivered in racks in build order.
Part matched to vehicle at the station.
Lead times differ by part: a seat supplier may need hours, a cockpit supplier longer, and the frozen horizon must cover the longest of them with some margin for delays.
Any change to the sequence inside the supplier’s lead time causes a mismatch. That is why sequence stability matters as much as sequence quality. A slightly less optimal sequence that holds is usually better than an optimal one that keeps changing.
Sequence stability and supplier call-off accuracy should be measured alongside ratio compliance. Our sequencing views show all three.
Optimization Methods for Model Mix
Several approaches are used to build sequences. Most commercial systems combine them.
Build the sequence position by position, choosing the vehicle that breaks the fewest rules. Fast but can get stuck.
Improve a sequence by swaps and moves, as many ROADEF 2005 approaches did. Good quality in reasonable time.
Strong at hard rules; may struggle with large weighted objectives.
Exact for smaller problems; often used for sub-problems.
Learns which rules and weights lead to good outcomes on the actual line.
Heuristics for speed, search for quality, rules for feasibility.
The method matters less than the model of the problem. A clever algorithm with the wrong ratio rules or weights produces a bad sequence quickly. Ask our team how rules and weights are validated.
Measuring Sequence Quality
A sequence should be judged on several measures at once, because improving one can harm another.
| Measure | What it shows | Typical target direction |
|---|---|---|
| Ratio rule violations | Stations at risk of overload | As close to zero as possible |
| Average colour block size | Paint efficiency | Larger, up to the maximum allowed |
| Work content variation | Operator load smoothness | Lower |
| Sequence stability | Share of vehicles built in planned position | Higher |
| JIS call-off accuracy | Supplier sync | Higher |
| Line stops from mix | Real effect on JPH | Lower |
Measures should be reviewed by shift as well as by day, because problems often cluster at shift starts or around breaks.
The last measure closes the loop. If ratio rules are met but stations still stop, the rules are wrong. Comparing sequence measures with real line stops shows where the model needs correcting.
Weekly review of these measures, with planning and production together, keeps the sequencing model honest. We provide that review pack in every rollout.
Model Mix Scheduling Checklist
Use this checklist to strengthen model mix scheduling.
Refreshing ratio rules after every line rebalance is the step most often forgotten. We flag it automatically when the balance changes in your MES.
How iFactory Delivers Model Mix Optimization
Ratio rules from your line balance, kept current.
Hybrid heuristics and search for large sequences.
Colour block size balanced with assembly rules.
JIS call-offs aligned with the frozen sequence.
Fast resequencing when vehicles fall out of order.
Rule compliance, stability and line stops tracked.
It works with your MES, ERP and supplier systems. Share a week of orders and we will sequence them in a session.
See a Better Sequence for Your Own Orders
Share a week of orders with options and colours. We apply your ratio rules and paint limits, build an optimized sequence and compare it with your current one on every measure.
Three sunroof vehicles fall inside a five-car window at positions 214–218, breaking the 2-in-5 rule. Swapping two vehicles fixes it without adding a colour change.
A Rule Break Caught Before Freeze
This exchange shows how a sequence planner might use iFactory.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the model mix sequencing and optimization models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensors and data connections across body, paint, assembly and utility systems, PLC/SCADA, MES, CMMS and ERP integration, cabling and network setup, operator and quality team training, and 24×7 remote monitoring.
Server installed, PLC, MES and ERP links live, historical production, quality and maintenance data loaded.
Models calibrated on your own lines, then run in advisory mode on one line or area with your planners and engineers reviewing every output.
Rollout to the agreed lines under your change management, planner, supervisor and engineer training, and 24×7 remote monitoring in place.
Software, server and integration come as one package. For pricing on your lines, contact our sales team.
Frequently Asked Questions
Deciding the order in which different vehicle variants are built on a mixed-model line so that station capacity, paint efficiency, supplier sequence and material availability are all respected.
Rules of the form at most p vehicles with a given option in any q consecutive vehicles, protecting stations that have extra work for that option.
Paint prefers long blocks of one colour; assembly prefers options spread evenly. Painted body storage between the shops allows resequencing to balance both.
Suppliers build and deliver parts in the planned sequence. Changes inside their lead time cause mismatches, so sequence stability is as important as sequence quality.
Greedy heuristics, local search, constraint programming, integer programming and AI-assisted approaches, often combined in hybrid systems.
A first line can usually be sequenced within a 6–12 week rollout once orders, rules and line balance data are available. Plan it with our planners.
Build Every Vehicle in the Order That Works
iFactory sequences your mix to meet ratio rules, respect paint and stay stable for suppliers, then checks the result against real line stops so the rules keep getting better.
Illustrative. Each measure is tracked against target so trade-offs stay visible.