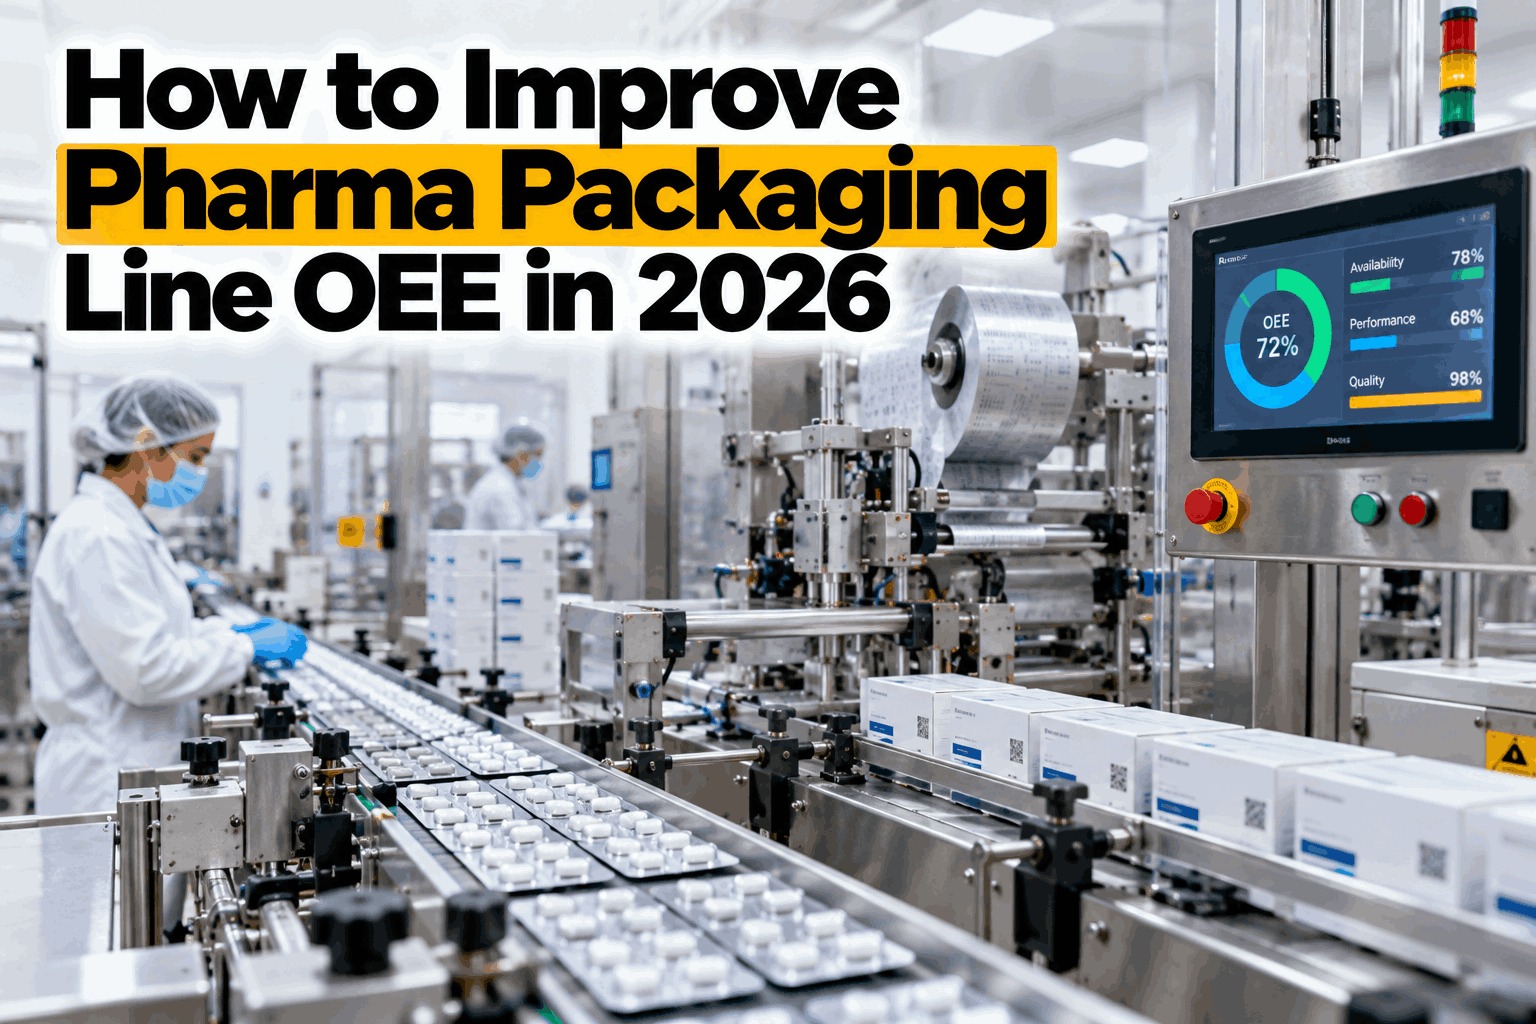
"Our packaging line runs at 56% OEE" is a sentence many pharma plants could say, and it is close to the median for blister packaging. The number alone does not say where the other 44% goes. It could be changeovers between formats, film and foil jams at the blister machine, a cartoner starved of product, serialization rejects or simply a line that is set to run slower than it can. Pharma packaging OEE improvement starts by splitting that gap into losses you can name, rank and fix. This guide shows how to define OEE correctly for a packaging line, find the pacer stage, rank the losses and lift blister, carton and serialization performance. To apply it to your own line, book a packaging OEE walkthrough.
How to Improve Pharma Packaging Line OEE
A practical guide to lifting blister, cartoner and serialization performance: how to define OEE so it holds up, find the stage that paces the line and turn each loss into a ranked action.
- How to define OEE so packaging losses are counted fairly
- Where blister, carton and serialization stages lose time
- How to rank losses by OEE points and value
Five causes explain more than nine tenths of the loss. The dashed line marks where the cumulative share passes 80%. A packaging OEE figure is only useful if it points at causes like these, not just at a total.
What Packaging Line OEE Really Is
OEE shows how much of the planned time produced good packs at the rated speed.
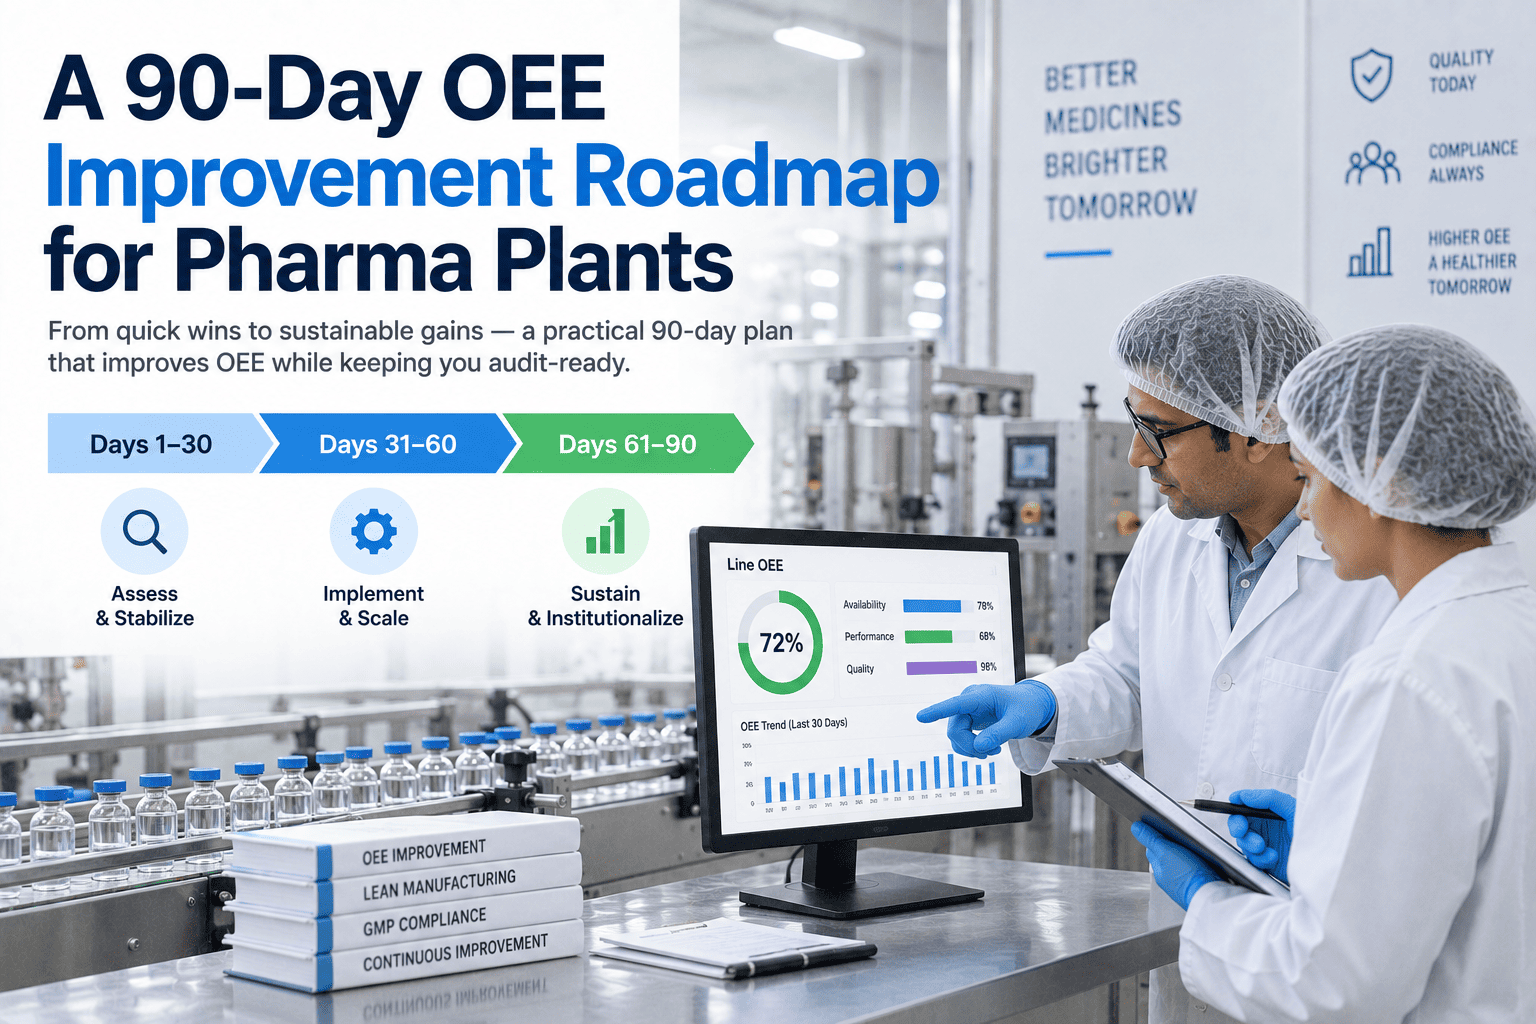
Overall equipment effectiveness multiplies three factors: availability, performance and quality. On a pharma packaging line that means time the line is actually running, speed against the validated rate for that format, and good packs against everything that was started. A line can look busy and still score poorly, because short stops, slow running and rejects are easy to miss on the shop floor. Our OEE analytics team can show how this looks on your own line data.
Record every state
Run, stop, changeover and wait, straight from the line.
Give each stop a reason
Coded causes, not a single downtime bucket.
Find the big losses
Ordered by OEE points and by value.
Fix and verify
Owners, dates and a check against the baseline.
Averaging machine OEE hides the real constraint. Track the pacer stage and the line as a whole, because a fast cartoner behind a slow blister machine cannot make the line faster.
Where Pharma Packaging Lines Lose OEE
Each stage loses time in its own way.
A typical line runs blister forming and sealing, cartoning, serialization and aggregation, then case packing. The losses differ by stage, and so do the fixes. Start with the pacer, because every minute it loses is a minute the whole line loses. To see which stage paces your line, book a line loss review.
When a cartoner waits for blisters, the cause sits upstream. Code it as starved, not as a cartoner breakdown, or the wrong machine gets the maintenance work.
Set the OEE Definition Right
An OEE figure is only fair if everyone counts the same way.
Two sites can report very different OEE on identical lines because they define planned time, rated speed and good packs differently. Agree the rules once, write them down and apply them to every line, so improvement shows up as a real change and not as a change of definition.
If the rated speed is set to the best shift ever recorded, performance looks poor for the wrong reason. If it is set low, losses disappear. Tie it to the validated speed for each format and review it when the format or equipment changes.
What a Point of Packaging OEE Is Worth
A few OEE points can look small on a dashboard. Multiplied by a year of rated capacity and the contribution of each pack, they become a number worth acting on.
From OEE Loss to Action
A loss only matters once it is traced to a cause and an owner.
The OEE figure tells you which line and which shift to look at. Stop codes and machine data tell you which cause. Together they give a short list of actions with a value on each, which is what a plant head needs to approve the work.
Connect
Line states and counters from every stage.
Classify
Every stop coded to a cause.
Rank
Losses ordered by OEE points.
Act
Fixes assigned with owners and dates.
Verify
Gain checked against the baseline.
Sustain
New standards held shift after shift.
Common Packaging OEE Mistakes
Most poor OEE data comes from unfair counting.
OEE is easy to calculate and easy to distort. A few simple checks keep the numbers honest and keep the shop floor's trust in them.
Good practice
- Track the pacer stage and the line as a whole
- Code every stop automatically with a reason
- Use a validated rated speed for each format
Common mistakes
- Averaging machine OEE across the line
- Hiding changeovers inside planned time
- Counting reworked packs as good first time
A pack that needs a second pass used up time and labour even if it ships. Track rework as its own loss so quality problems at the blister or serialization stage stay in view.
How iFactory OEE Analytics Works
Line data in, ranked losses out.
iFactory collects machine states and counters from your packaging lines, classifies every stop and builds OEE by stage, line, product and shift. It shows the pacer, ranks losses by OEE points and value, and tracks each fix against the baseline. It runs on an on-prem server inside your network, with one view across all lines and sites. Questions on fit go to our support desk.
All line signals
PLC and SCADA data, plus counters from vision and serialization stations where available.
Coded stops
Every stop given a cause, with operators confirming the rest.
Stages and shifts
Blister, carton and case packing on one scale.
Ranked losses
Causes sized in OEE points and value, with owners.
Gains depend on your lines, formats and how quickly losses are acted on. We measure OEE and the effect of each fix on your own data during the pilot, rather than promising a general figure.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our team handles cabling, network setup, PLC and SCADA integration, team training and 24×7 remote monitoring. Data stays on your own network. For a scope matched to your lines, request a turnkey quote.
Ship, network and line data
Server installed. Line states and counters connected for the pilot lines.
Loss codes and baselines
Stop codes and rated speeds agreed. OEE baselines checked with your teams.
Go-live and training
Dashboards and alerts live. Teams trained. 24×7 remote monitoring begins.
Frequently Asked Questions
What is a good OEE for a pharma packaging line?
Median blister packaging OEE is around 56%, so a target in the low 70s is a reasonable stretch for many lines. Set the target from your own best demonstrated week and your format mix rather than from a single published number.
How is packaging line OEE calculated?
Multiply availability, performance and quality. Availability is run time over planned time, performance is actual speed against the validated rated speed, and quality is good first-time packs over total packs started.
Should changeover and line clearance count as OEE losses?
Most sites count them as availability loss so the time stays visible, even though line clearance itself is required. Reducing the time they take, without cutting any compliance step, is often the biggest single gain.
Which stage should we measure first?
The pacer, which is usually the blister machine. It sets the speed of the whole line, so its losses are the line's losses. Then measure the stages that wait on it.
How does serialization affect OEE?
Through stops for read failures, rejected packs and reprints, and through time spent on code and label checks. Track these as their own losses so you can tell whether serialization is a real constraint or just a visible one.
How do we start?
With one blister line and the stages that follow it. A 6-week pilot connects the line data, agrees stop codes and rated speeds, and shows the first ranked loss list. To plan it, contact our team.
Know Where Your Packaging Line Really Loses Time
In thirty minutes we look at your line, your stop data and how you calculate OEE today. You keep the notes whether or not you go further with iFactory.
- 1A month of line stop and downtime records
- 2Rated speeds for each pack format
- 3Changeover logs and the format schedule
- 4Reject and rework counts by cause
- 5The line you suspect loses the most