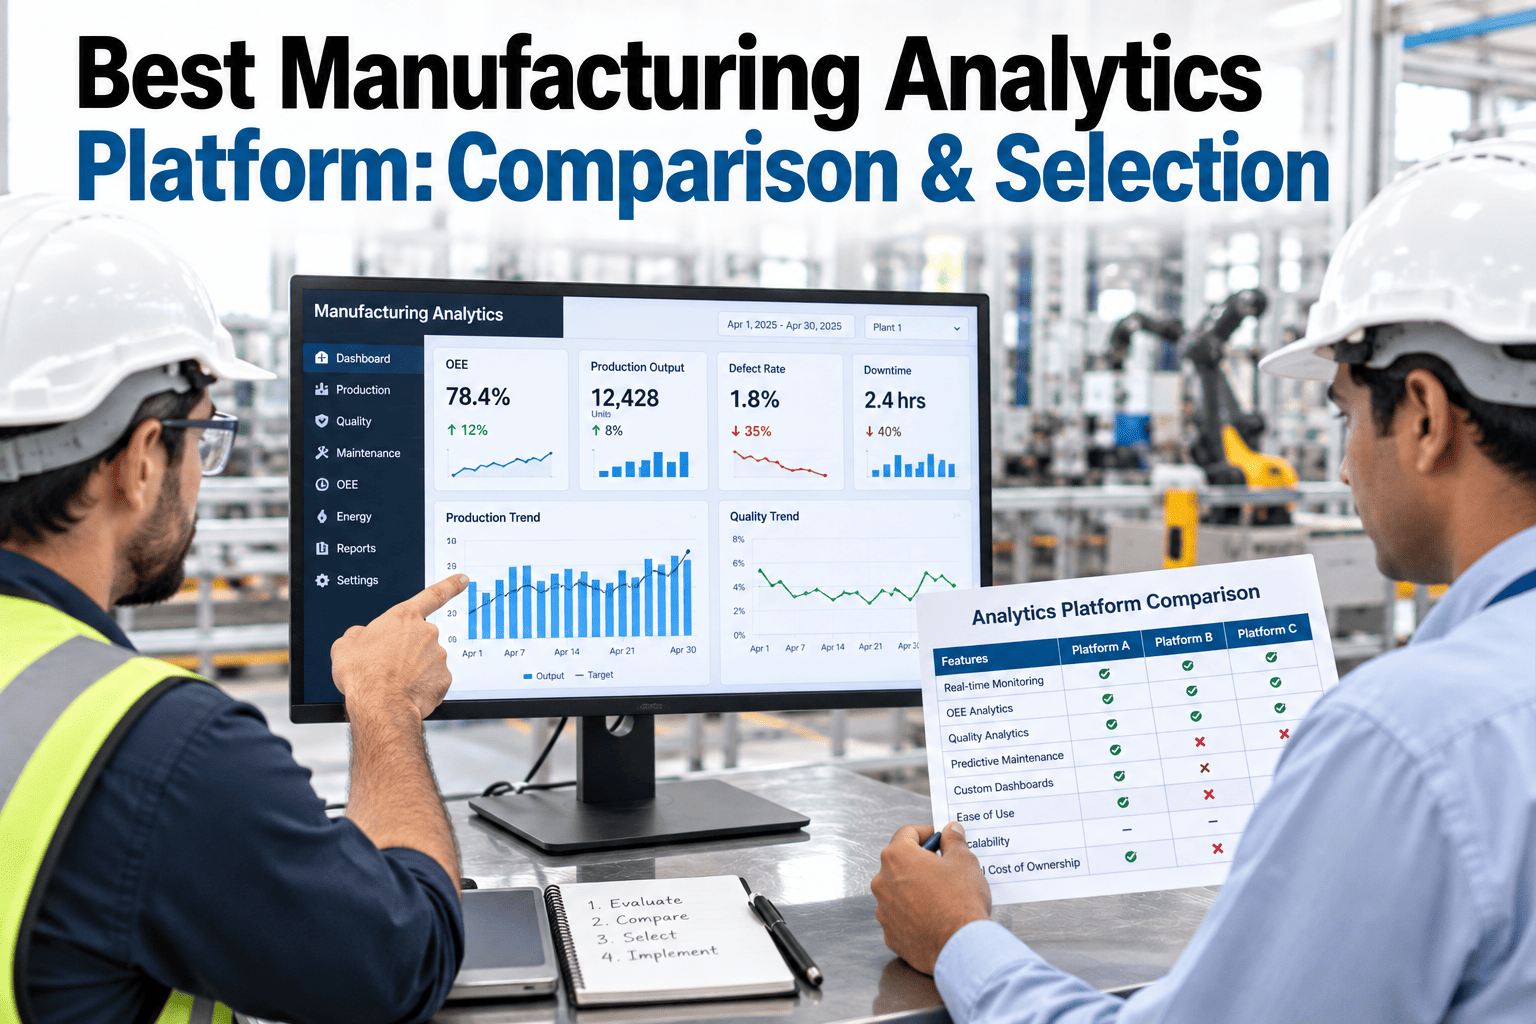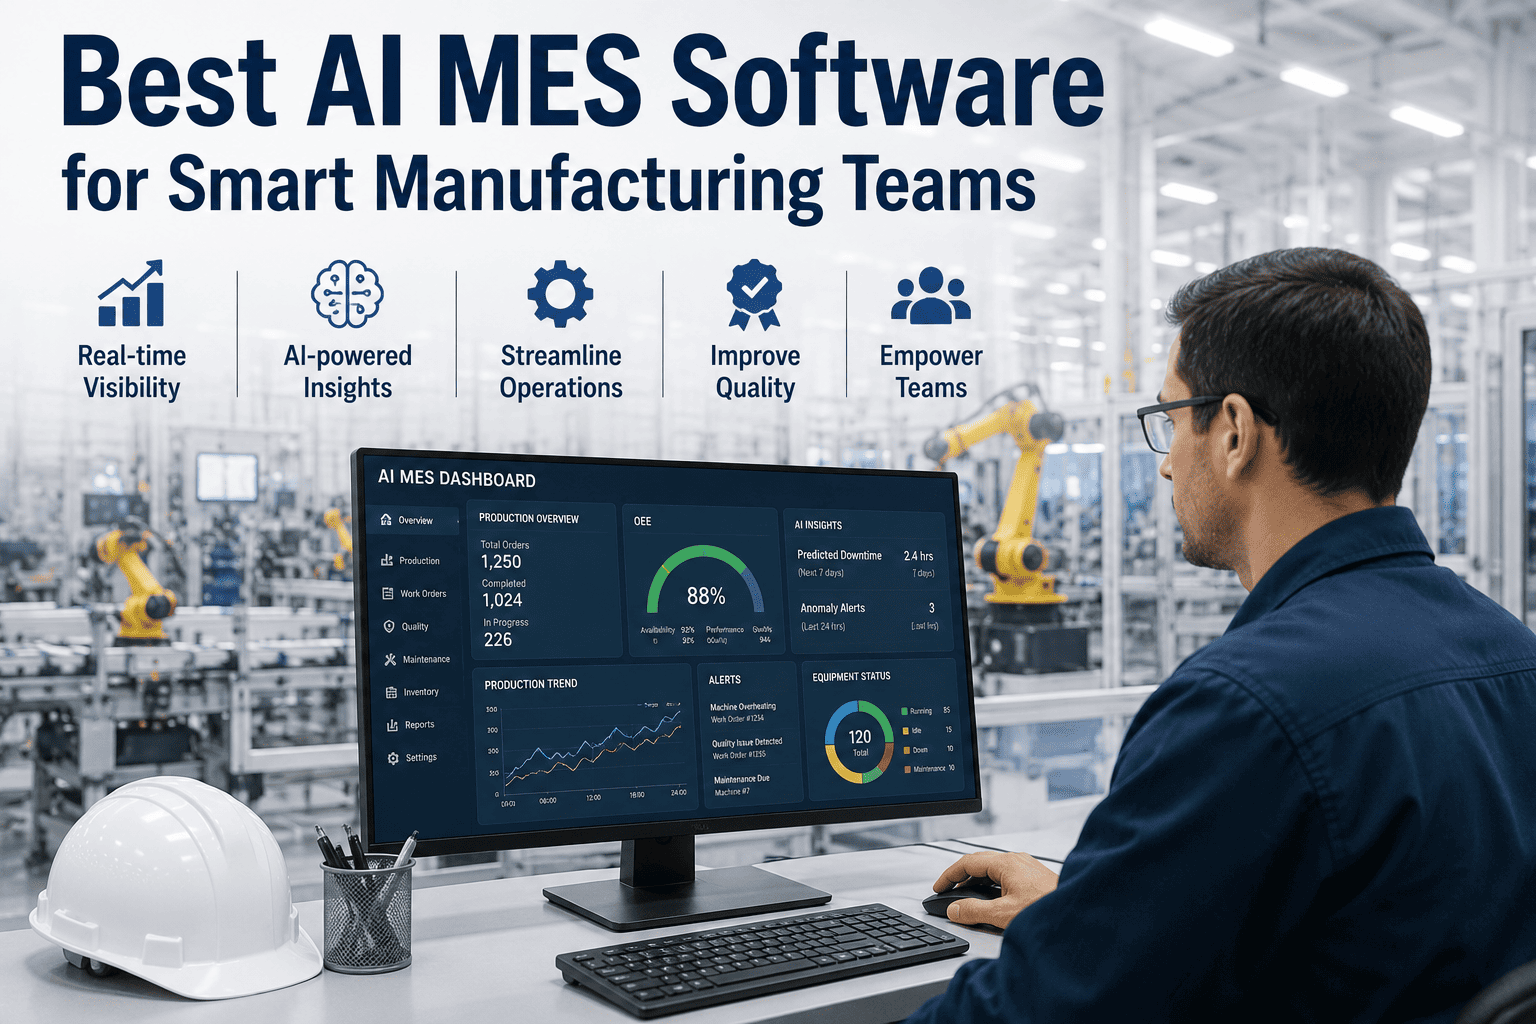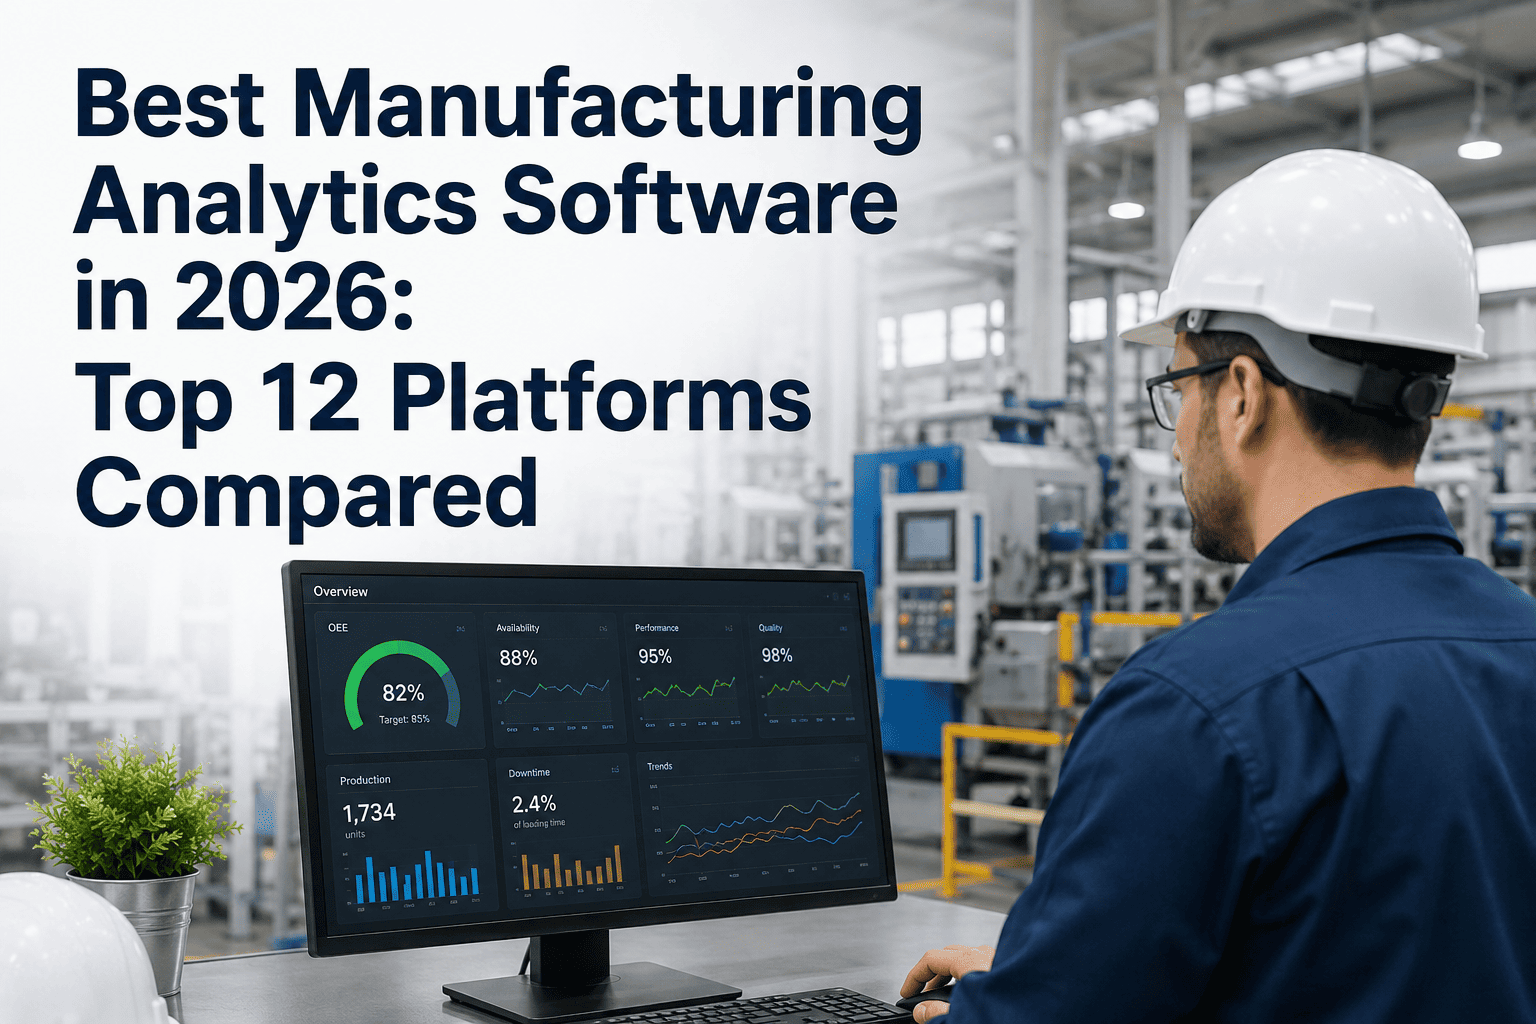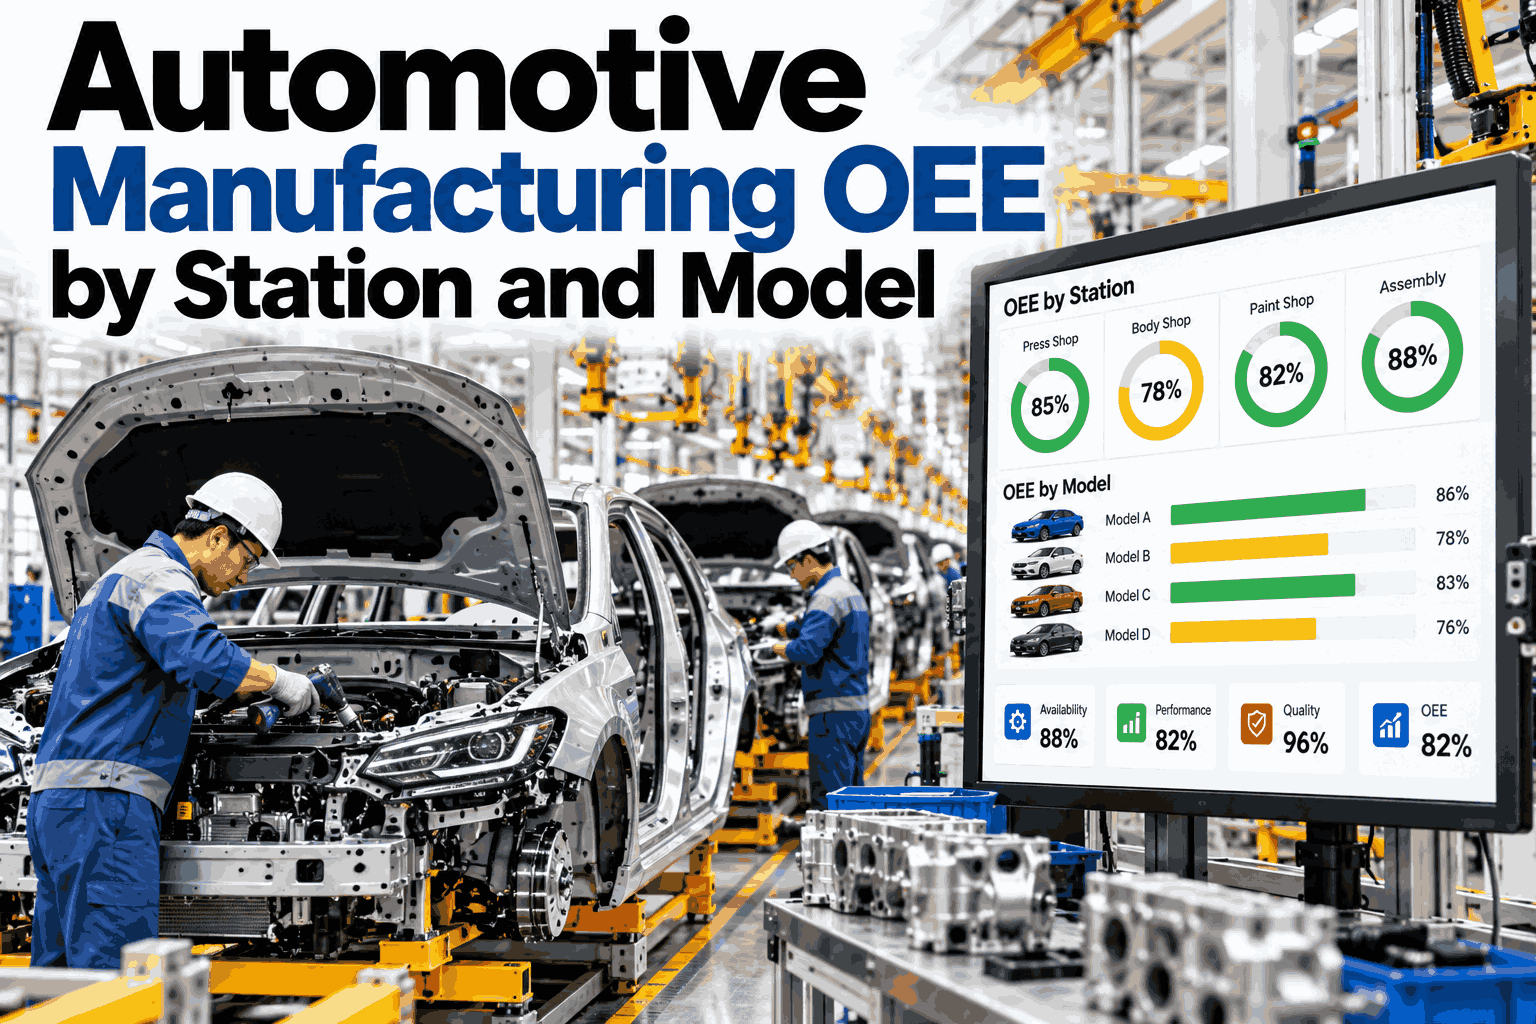
A single plant-wide OEE number on a monthly scorecard tells a plant manager almost nothing about where to act next. An automotive plant running multiple models across body weld, paint, and final assembly can show a respectable blended OEE while one station on one model line is quietly dragging the whole average down. Stations differ in cycle time, changeover frequency, and failure pattern, and a model running through final assembly with extra trim content behaves nothing like the same station running a base trim. Blending all of that into one percentage hides exactly where the next improvement project should start. Breaking OEE down by station and by model turns a vague scorecard into a ranked list of real opportunities. Plant teams can review a station-by-model OEE breakdown with the iFactory AI team before the next production review.
Automotive Manufacturing OEE by Station and Model
iFactory AI breaks Availability, Performance, and Quality down by station and by model, so a plant-wide OEE number becomes a ranked list of real opportunities.
The Three Components Behind Every OEE Number
A dropping OEE score can come from three completely different places, and each one needs a different fix.
Availability
The share of scheduled time a station is actually running, reduced by breakdowns, changeovers, and material starvation.
Performance
How close actual cycle time runs to the ideal cycle time, reduced by minor stops, slow cycles, and small adjustments operators make on the fly.
Quality
The share of parts that are right the first time, reduced by rework, scrap, and startup rejects after a changeover.
A station with poor availability and a station with poor quality can land on the same OEE number and need completely opposite action plans.
OEE by Station and Model, at a Glance
A station and model grid turns a single blended number into a map of exactly where performance is strong and where it is slipping.
The grid above is illustrative. Strong marks OEE comfortably above target, Watch marks a station worth monitoring, and At Risk marks a station and model pair pulling the plant-wide average down.
See Your Own Station and Model Grid
Book a 30-minute session and bring a recent production run. iFactory AI will show which station and model pairs are driving your real OEE loss.
Where the Six Big Losses Show Up
Each of the classic six big losses hits a different part of the OEE equation, which is why tracing a low score back to its cause depends on knowing which factor actually moved.
| Loss Category | Typical Cause on an Auto Line | OEE Factor Affected |
|---|---|---|
| Breakdowns | Robot fault, conveyor jam, tooling failure | Availability |
| Changeovers | Model or variant switch at the station | Availability |
| Minor Stops | Short jams, sensor faults, operator adjustments | Performance |
| Reduced Speed | Running below rated cycle time on a difficult variant | Performance |
| Startup Rejects | Early parts after a changeover before process stabilizes | Quality |
| Process Rejects | Ongoing defects tied to fixture wear or material variation | Quality |
A station showing heavy loss from changeovers needs a sequencing or SMED fix, while the same score driven by process rejects needs a quality investigation instead.
Building the Station and Model View
A useful station and model breakdown is built in stages, starting from the data a plant already has rather than a clean-sheet system.
Connect Station-Level Data
Cycle times, stop reasons, and reject counts are pulled from each station's existing controller or line system.
Tag Every Event by Model
Each cycle, stop, and reject is tagged to the model and variant running at that moment, not just the station.
Set Ideal Cycle Time per Variant
Performance loss is measured against the correct ideal cycle time for each model, since a harder variant should not be penalized against an easier one's target.
Classify Loss Reasons
Stops and rejects are categorized against the six big losses, so a low score points toward a cause, not just a symptom.
Rank and Act
Station and model pairs are ranked by OEE loss and production volume, focusing improvement work where it moves the most output.
Skipping the model tagging step is the most common reason a plant has good station-level OEE data but still cannot explain why one variant underperforms.
A Composite Scenario: One Final Assembly Line, Four Models
A plant running four models through one final assembly line found its blended OEE acceptable but one EV variant pulling output well below plan. Figures below are an illustrative composite, indexed to a starting point of 100.
Once loss was tagged by model, the EV variant's shortfall traced back to startup rejects after changeovers rather than a speed problem, which redirected the entire improvement project.
Plant-Wide Average vs Station and Model View
The blended number is not wrong, it is just too coarse to act on by itself.
Plant-Wide Average
Station and Model View
The plant-wide number still matters for reporting, it just should not be the number a team uses to decide what to fix next.
What iFactory AI Adds to Automotive OEE Tracking
iFactory AI is smart manufacturing and industrial software that connects station-level data to model and variant context, so OEE becomes a tool for prioritization, not just reporting.
iFactory AI arrives pre-configured on an NVIDIA server that ships racked and ready with software pre-loaded. Rack it, connect power and Ethernet, and station data starts flowing. Scope covers cabling, network, ERP and MES integration, team training, and 24x7 remote monitoring.
OEE Program Self-Check
Use these checks to see how much of your OEE program still depends on one blended number.
Each unchecked box is a place where the blended OEE number is quietly hiding a bigger opportunity.
Frequently Asked Questions
How granular should the station breakdown be?
Most plants start at the major process level, such as body weld, paint, powertrain, and final assembly, then drill into individual sub-stations once the high-level grid shows where attention is needed most. Ask how to scope station granularity for your line.
Can this work with mixed-model lines where sequencing changes daily?
Yes, tagging events to the model running at the moment of each cycle is exactly what makes mixed-model sequencing visible, rather than averaging it away into one line-level number. See how mixed-model sequencing is handled.
Does a new model variant need its own target before it can be tracked?
A reasonable starting target can come from engineering cycle time studies, and it gets refined with real production data as the variant ramps up, so tracking can begin before the target is perfectly tuned.
How does this connect to existing MES or line controller systems?
Station-level cycle time, stop, and reject data is pulled from existing controllers and MES systems rather than requiring new sensors at every point, with integration scoped during the rollout. Talk through your current system landscape with the team.
How soon can a plant see its first station and model grid?
Most plants see an early version of the grid within the first phase of the rollout, with loss classification and ranking refined as more production cycles are logged. Plan a rollout timeline for your plant.
Turn Your OEE Scorecard Into a Ranked Action List
iFactory AI breaks Availability, Performance, and Quality down by station and model so improvement work goes where it matters most. Book a walkthrough using your own line data.