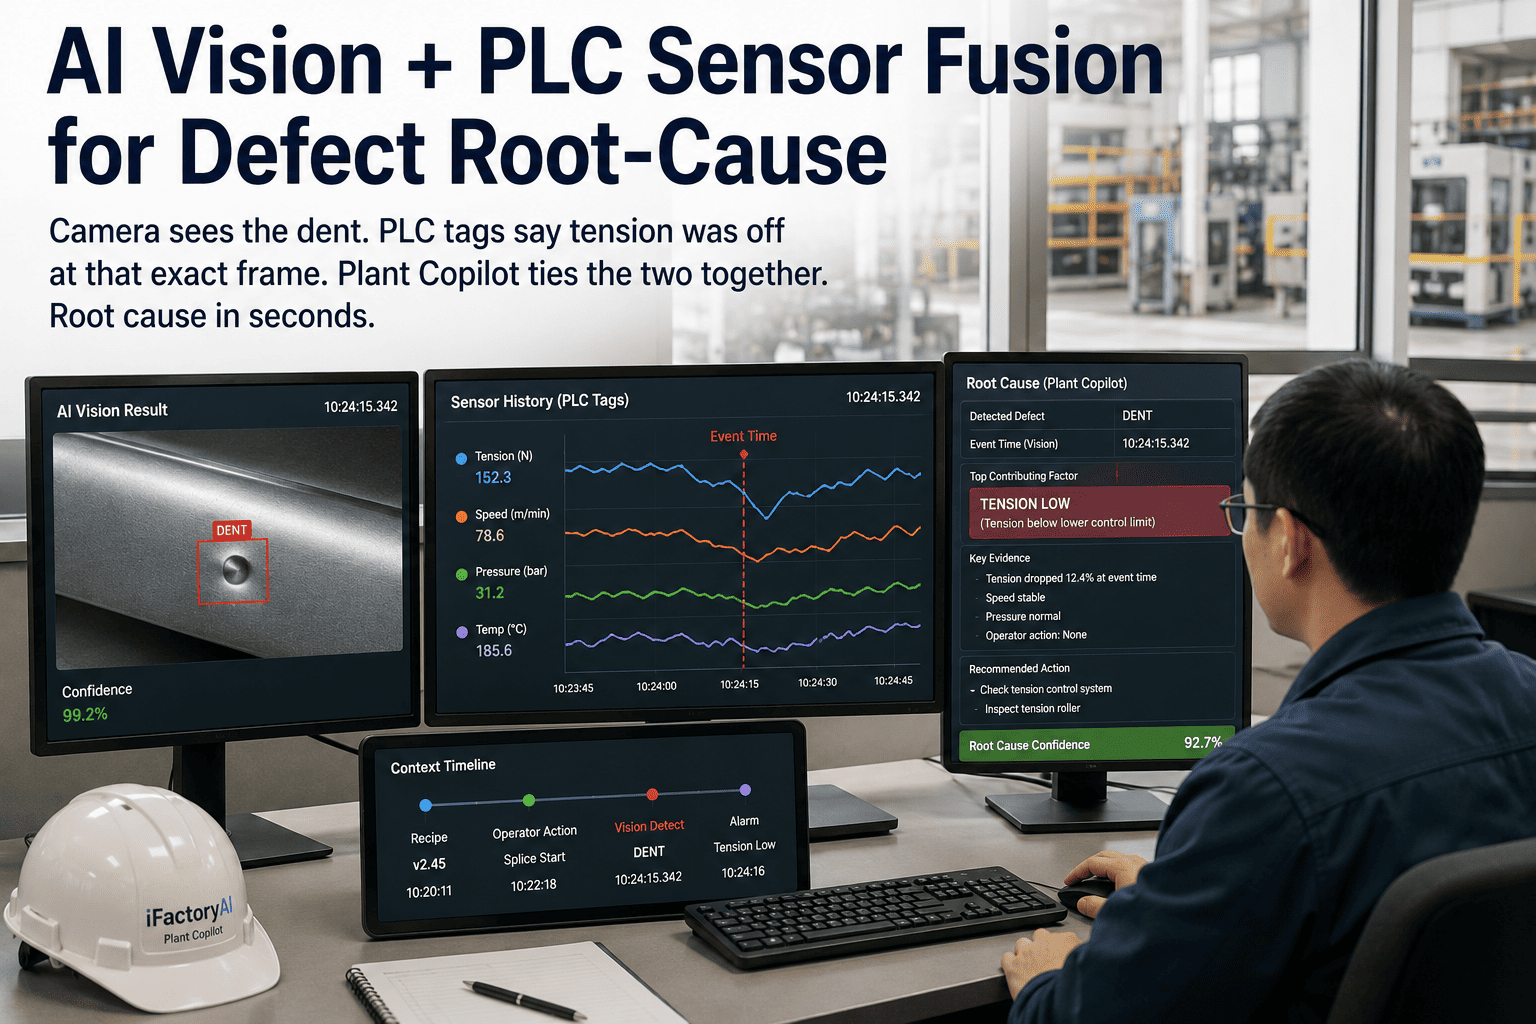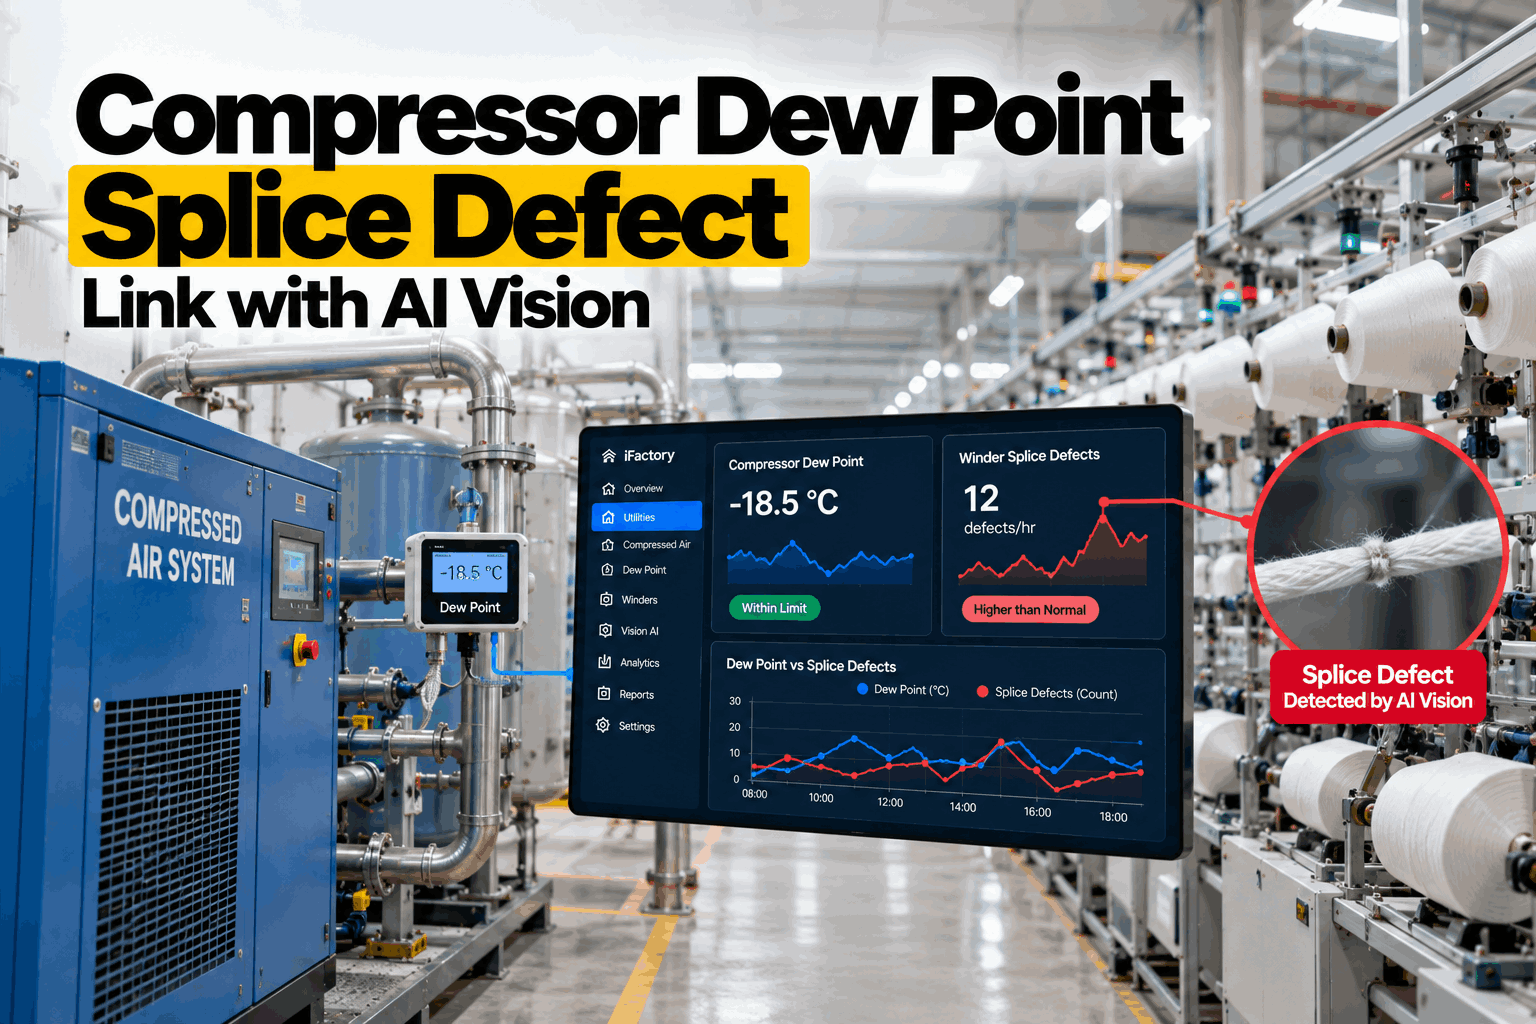
When splices start failing at the winder, the first suspects are the splicer, the settings and the yarn. The compressor room is rarely on the list, because it sits two departments away and keeps its own records. Yet the splicer is an air tool, and the air it gets is only as dry as the dryer was that hour. iFactory puts dew point sensors on the utility loop and vision AI at the winder, then lines the two up on one clock — so you can show that a splice problem came from the air, or show just as clearly that it did not. To see it on your own loop, book an air review.
Is It the Air? Linking Compressor Dew Point to Splice Defects at the Winder
IoT sensors on the utility loop and vision AI at the winder put dew point, pressure and splice quality on one timeline, so root cause takes hours instead of weeks.
- Dew point measured at the dryer and at the winder
- Splice faults counted and graded, winder by winder
- The air system confirmed or cleared, with evidence
A Utility Problem That Shows Up as a Quality Problem
The splicer is an air tool. What comes down the pipe helps decide how the splice turns out.
Every splice is made by two short blasts of compressed air. If that air carries water, the splicer is working with something it was never set up for. Our support team can go through your winder maker's air requirements with you.
Bring
Suction arms find the two yarn ends and lay them into the splicing chamber.
Open
A first air blast untwists the ends and opens the fibres into fine, tapered tails.
Join
A second blast swirls the two tails together and twists them into one yarn.
What wet air can do
- Liquid water is carried into the splicing chamber with the blast.
- Damp fibres clump instead of opening into clean tails.
- Small valves and pistons stick, so the blast comes late or weak.
- Rust and oil from wet pipework arrive with the water.
- The far end of the loop gets the worst of it.
An honest starting point
Published splicing studies look mainly at air pressure and timing. In one, pressure was the setting that moved splice strength most. Air moisture is far less studied.
So "it is the dew point" should be treated as a suspect to test on your own plant, not a known fact. Testing it is exactly what this link is for.
A splice that fails at the winder is simply made again, at a cost of a few seconds. The expensive splice is the weak one that passes, then breaks in warping or weaving at your customer. A good splice keeps 85–90% of the yarn's strength. Splices made during a wet spell may not.
Three Sets of Data That Never Meet
Each department holds one piece. Nobody holds the picture.
The utility team sees the dryer. Winding sees the splice counts. Quality sees the test results. They are stored in different systems and stamped by different clocks, so a link between them stays a hunch. Clocks are the hidden problem: if winder reports are stamped by shift and dryer logs by the hour, a 40-minute lag can never be seen. To map what your site already records, book a working session.
The air
Compressor load, header pressure and dryer status. Real dew point is often not measured at all; the dryer shows only its own refrigerant temperature.
The splices
Splice attempts, repeats and clearer cuts at the splice, for every spindle. Rich data, but usually read as a shift total.
The results
Splice strength tests and appearance checks on a few samples a shift, plus complaints that arrive days later.
Pressure dew point is the temperature at which water starts to condense out of the compressed air. The lower it is, the drier the air. If the pipe is colder than the dew point, water forms inside it.
ISO 8573-1 water classes. Your winder maker's air specification says which one applies to you.
How the Link Is Made
Put everything on one clock, then ask a simple question: when the air got wetter, did the splices get worse?
The answer has to hold up against the other things that spoil a splice. So the same timeline carries pressure, room humidity, lot changes and setting changes, and each is tested in turn. Ask our process specialists how the check is done.
Sense
Dew point and pressure, at the dryer outlet and again at the winder header.
Count
Splice repeats and splice cuts for each winder, every few minutes.
See
Vision AI grades sampled splices by appearance: good, thick, thin or loose tails.
Link
All of it is lined up in time. The AI checks whether splice faults rise after dew point does.
The other suspects, checked at the same time
A link is reported only when splice faults move with dew point and the other suspects do not explain it.
One afternoon is a clue, not proof. The link firms up as it repeats across several wet spells — or fades if it does not. Either way, you know more than you did.
One Afternoon, Two Outcomes
With the link, a dryer fault is caught the same afternoon and the affected lots are known. Without it, the first sign is yarn breaking in a customer's warping room days later.
What the Utility Head Does With It
The shape of the drift points to the fault in the air system.
A dew point that climbs every hot afternoon is a different problem from one that is dry at the dryer and wet at the winder. Reading the pattern saves a lot of walking the pipework. To review your own dryers and drains this way, book a loop review.
Sometimes the answer is that the air was fine. That is worth just as much. The utility team is cleared with evidence, and winding can look at splicers and settings without a week of argument.
Three habits that keep dew point honest
Measure real dew point
A dryer's own display shows refrigerant temperature. Only a dew point sensor in the air line shows what the winders receive.
Measure it twice
Once after the dryer, once at the far end of the loop. The gap between them is the state of your pipework and drains.
Alarm before the limit
Set the alarm a little above normal, not at the limit, so the standby dryer starts before the winders notice.
One Timeline, Read by Three Departments
When everyone looks at the same picture, the meeting gets shorter.
Each team sees the part it can act on, drawn from the same record. Nothing in the winder or the compressor controls is changed; iFactory reads, links and advises. Our integration team can check what your winders and compressors make available.
Who sees what
- Utility head. Dew point and pressure by loop, with dryer and drain alerts.
- Winding supervisor. Splice repeats by winder, flagged when they move with the air.
- Quality manager. Splice appearance grades, and the lots wound during any wet spell.
- Maintenance planner. Dryer and drain jobs raised from the trend, not from a breakdown.
iFactory advises. Compressor, dryer and winder controls stay exactly as they are.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready, with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network.
Our team handles cabling, network setup, PLC and SCADA integration, operator training and 24×7 remote monitoring. The server sits inside your own network, and your plant data stays on it. For a scope matched to your mill, request a turnkey quote.
Ship, network and data
Server installed. Dew point and pressure sensors fitted on each loop. Compressor, dryer and winder data connected.
Model training and pilot
Normal ranges learned for each loop and winder. Vision grading set up on sample splices. Links checked with utility and winding together.
Go-live and training
Live timeline and alerts for all three teams. Training by role. 24×7 remote monitoring begins.
Frequently Asked Questions
What is pressure dew point?
It is the temperature at which water begins to condense out of compressed air at line pressure. A dew point of +3°C means no water forms unless the pipe is colder than 3°C. If the dew point drifts up to 12°C, water forms in any pipe cooler than that.
Can wet compressed air really cause bad splices?
It is a reasonable suspect, because the splice is made by the air itself and by small air-driven parts. But published studies focus on pressure and timing, not moisture. That is why the link has to be shown on your own winders, with the other causes ruled out.
What dew point should a winding department run at?
Follow your winder maker's air specification. Many mills use refrigerant dryers that give about +3°C, which is ISO 8573-1 Class 4. What matters as much as the target is holding it at the winder, not only at the dryer. A loop that is dry at the dryer but wet at the winder has not met it.
Where do the sensors go?
One dew point sensor straight after each dryer, and one at the winder header or the far end of each loop. Pressure is measured at the same points. Two readings per loop show whether a problem starts at the dryer or in the pipework. Room temperature and humidity in the winding hall are logged as well.
What does vision AI add to the winder's own counts?
The winder counts splices that fail and are repeated. It does not grade the ones that pass. Vision AI looks at sampled splices and grades their appearance, so a run of weak-looking splices is seen even when the repeat count is still normal.
Does it work with our existing winders and compressors?
In most cases. Splice counts are read from the winder's production data where the machine makes them available. Compressor and dryer signals come from their controllers. Where a signal is missing, a sensor is added. Nothing in the machine controls is changed.
How long does it take to go live?
Six to twelve weeks from delivery. We need a place for the server with power and Ethernet, access to the compressor room and winder data, and a layout of your air loops. A pilot normally covers one loop and its winders. To check your set-up first, contact our team.
Bring Your Air Layout and a Month of Splice Reports
In thirty minutes we mark where dew point should be measured on your loops and show how your splice data would line up against it. You keep the sketch whether or not you go further with iFactory.
- 1Compressed air layout: compressors, dryers, loops
- 2Dryer types and ratings
- 3A month of winder splice reports
- 4Any dew point or pressure logs
- 5Dates of recent splice complaints