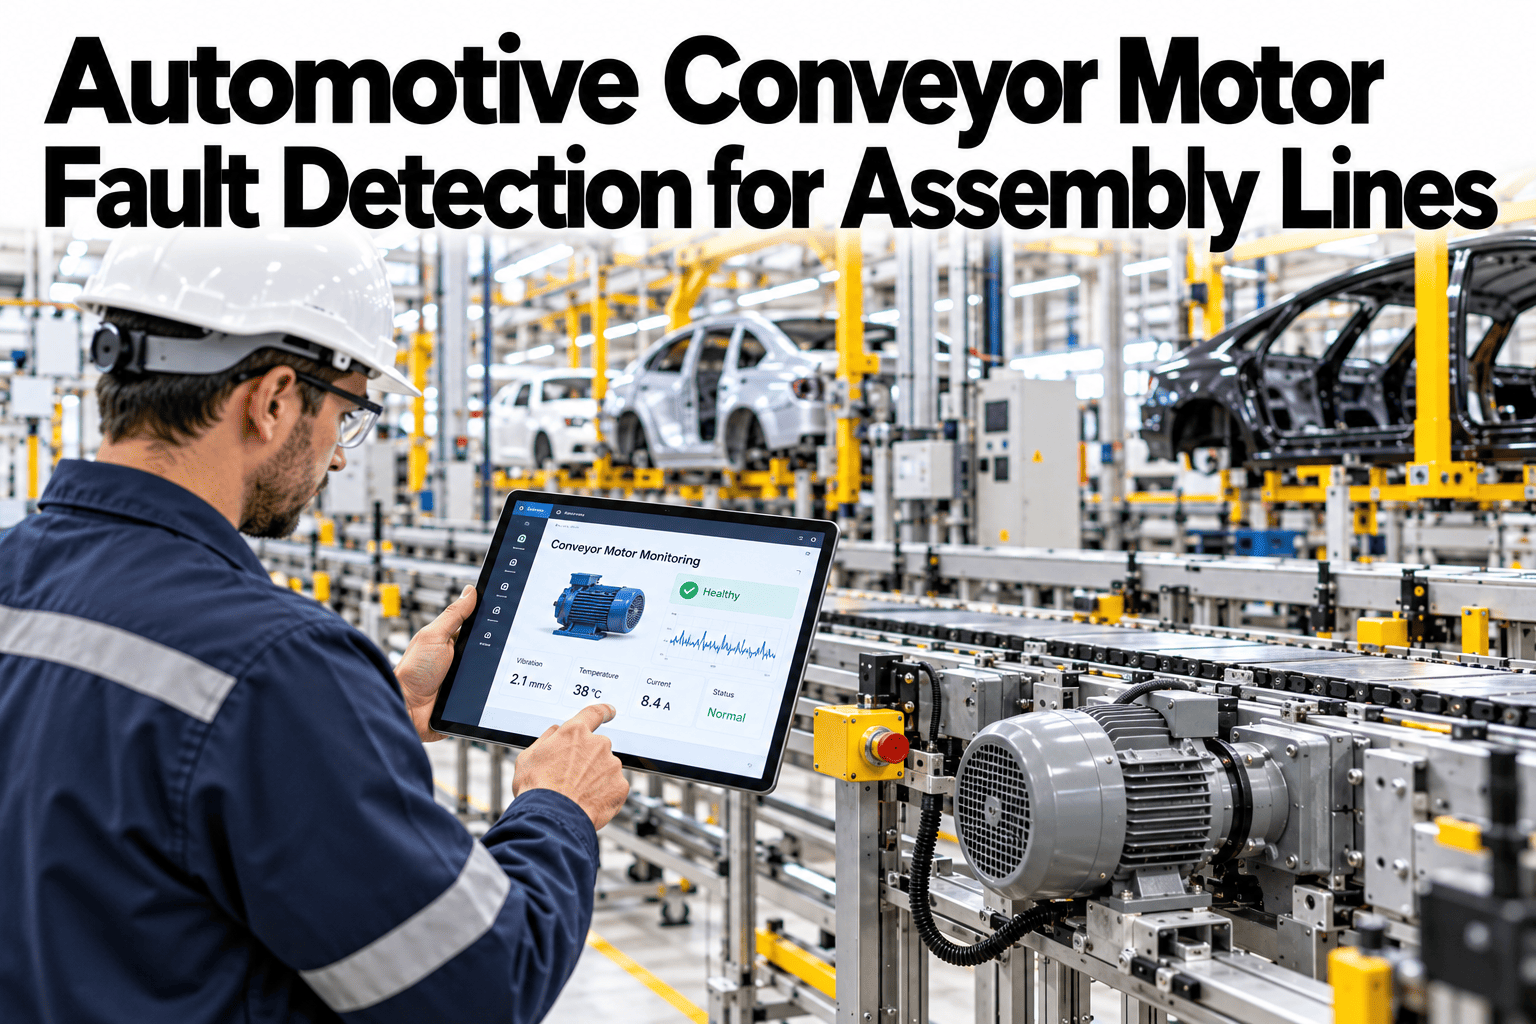
Every conveyor motor on an automotive assembly line is broadcasting its condition continuously through the current it draws — and most plants are not listening. Motor current signature analysis reads the electrical waveform of a running motor and extracts the fault-specific frequency components that distinguish a healthy stator from one with developing winding damage, a good rotor bar from one that is cracking, and a well-loaded drivetrain from one where mechanical drag is developing in the gearbox or chain. iFactory AI applies MCSA alongside thermal profiling and speed-load correlation to catch conveyor motor faults on assembly lines weeks before they produce a unplanned line stop. See how iFactory AI detects conveyor motor faults on your assembly line.
Catch Conveyor Motor Faults Before They Stop the Line
Current signature analysis, thermal profiling, and speed-load correlation — three detection layers that identify developing motor and gearbox faults 2–4 weeks before failure on automotive assembly conveyor drives.
No thermal or vibration change
Thermal trend starts rising
Vibration detectable
Thermal elevated
Audible noise
Speed instability
Why Conveyor Motors Fail on Assembly Lines
Assembly line conveyor motors operate under a combination of duty conditions that accelerates failure rates compared to most other industrial motor applications.
The Three Detection Technologies and What Each Catches
No single monitoring technology catches all conveyor motor fault types. iFactory AI fuses three technologies to cover the complete fault population with the highest combined detection confidence.
Current sensors at the motor control center capture the three-phase current waveform. iFactory AI analyzes the frequency spectrum for fault-characteristic sidebands — twice slip frequency sidebands for rotor bar faults, stator fault signatures, and mechanical load anomaly patterns that appear as current modulation without any physical sensor on the motor itself.
Motor winding temperature sensors or thermal cameras track heat rise rates relative to load and ambient conditions. The thermal profile catches insulation degradation and cooling system failures that MCSA detects late or misses entirely. Thermal trending also confirms MCSA findings — a genuine winding fault shows in both the current spectrum and the thermal profile, while a harmonic artifact from a VFD change shows only in the current spectrum.
Speed feedback from encoder or tachometer data, correlated against motor current draw, reveals changes in the mechanical efficiency of the drive system. A motor that is drawing 12% more current for the same conveyor speed and load than it was six weeks ago is working against developing mechanical drag — chain elongation, gearbox bearing wear, or guide rail contamination — that the motor data makes quantifiable before any other indicator is detectable.
Deploy Motor Fault Detection Across Your Assembly Line Conveyor Fleet
iFactory AI connects at the MCC — no physical sensor installation on each motor — and monitors your full conveyor drive fleet with MCSA, thermal, and speed-load analytics. Book a session to see detection applied to your motor population.
Fault Detection Across the Conveyor Drive Train
The conveyor motor is one component in a drive train that includes the gearbox, coupling, drive sprocket, and chain. iFactory AI's motor fault detection extends through the full mechanical system.
| Drive Train Component | Fault Type | Primary Detection Signal | Typical Detection Lead Time |
|---|---|---|---|
| Motor stator | Winding insulation degradation | Thermal trend + MCSA phase balance | 4–8 weeks |
| Motor rotor | Rotor bar cracking | MCSA sideband at 2sf | 3–6 weeks |
| Motor bearings | Race or ball wear | MCSA mechanical load + vibration | 2–4 weeks |
| Gearbox | Gear tooth wear, bearing damage | Vibration + thermal rise + load current | 2–5 weeks |
| Coupling | Misalignment, flexible element wear | Vibration 1× and 2× shaft frequency | 2–4 weeks |
| Drive sprocket | Tooth wear accelerated by chain elongation | Chain pitch sensor + load current pattern | 3–6 weeks |
From Fault Detection to Maintenance Action
Detection without a clear path to action is monitoring theater. iFactory AI closes the loop from fault signal to work order automatically.
Frequently Asked Questions
Does MCSA work on VFD-driven conveyor motors, or only on direct-online starts?
MCSA works on VFD-driven motors, but requires algorithms specifically designed for variable-frequency operation. The VFD introduces its own harmonic content that must be separated from fault signatures before analysis — a step that standard MCSA tools designed for fixed-frequency motors handle poorly. iFactory AI uses VFD-aware MCSA algorithms that account for the drive's output frequency spectrum and switching harmonics, allowing fault detection on variable-speed conveyor drives with the same detection confidence as fixed-speed motors. Ask about VFD-specific MCSA configuration for your conveyor drives.
How many motors can iFactory AI monitor simultaneously across an assembly plant?
iFactory AI scales to cover the full conveyor motor population of a multi-line assembly plant — typically 50 to 200 conveyor drive motors across body, paint, and final assembly — from a single edge AI server deployment. Adding motors requires current sensor connections at the MCC, which can be installed progressively by plant section without interrupting production on other sections. Walk through the phased deployment plan for your plant's motor population.
What current sensor hardware is needed, and does it require the motor to be de-energized for installation?
Current transformers (CTs) are installed at the MCC panel using split-core designs that clamp around the existing motor supply cables without cutting or splicing the conductor. Split-core CT installation is performed live — the motor continues running during sensor installation, which eliminates the need for a production stop to deploy the monitoring hardware. This is the primary reason MCSA deployment is faster and less disruptive than vibration sensor installation at the motor body.
How does iFactory AI handle load variation to avoid false alarms on assembly line conveyors?
iFactory AI builds load-normalized motor health models that establish separate baseline current profiles for different load states — the motor at full production speed, at slow speed, at startup, and at idle. Fault signatures are evaluated against the baseline for the current operating state rather than a single threshold, so a current increase during a heavy-variant body's passage through a station does not trigger an alarm while a genuine electrical fault component that appears consistently across all load states is correctly identified. Get details on load normalization methodology for assembly line conveyors.
Can the system detect when a motor is being overloaded due to a mechanical problem in the conveyor rather than an electrical fault?
Yes. The speed-load correlation layer specifically targets this scenario — detecting when a motor is drawing abnormally high current for its current speed and load conditions. This pattern identifies developing mechanical drag in the drive train: chain elongation adding friction, a seized guide roller increasing resistance, or gearbox oil degradation increasing internal drag. Mechanical overload detection often precedes the mechanical failure itself by weeks, making it one of the highest-value outputs of the motor monitoring system for conveyor health.
Monitor Every Conveyor Drive Motor From the MCC — No Line Stoppage Needed
iFactory AI deploys MCSA, thermal profiling, and speed-load correlation across your full assembly line conveyor motor fleet with live installation at the MCC. Book a walkthrough to see fault detection applied to your drive configuration.