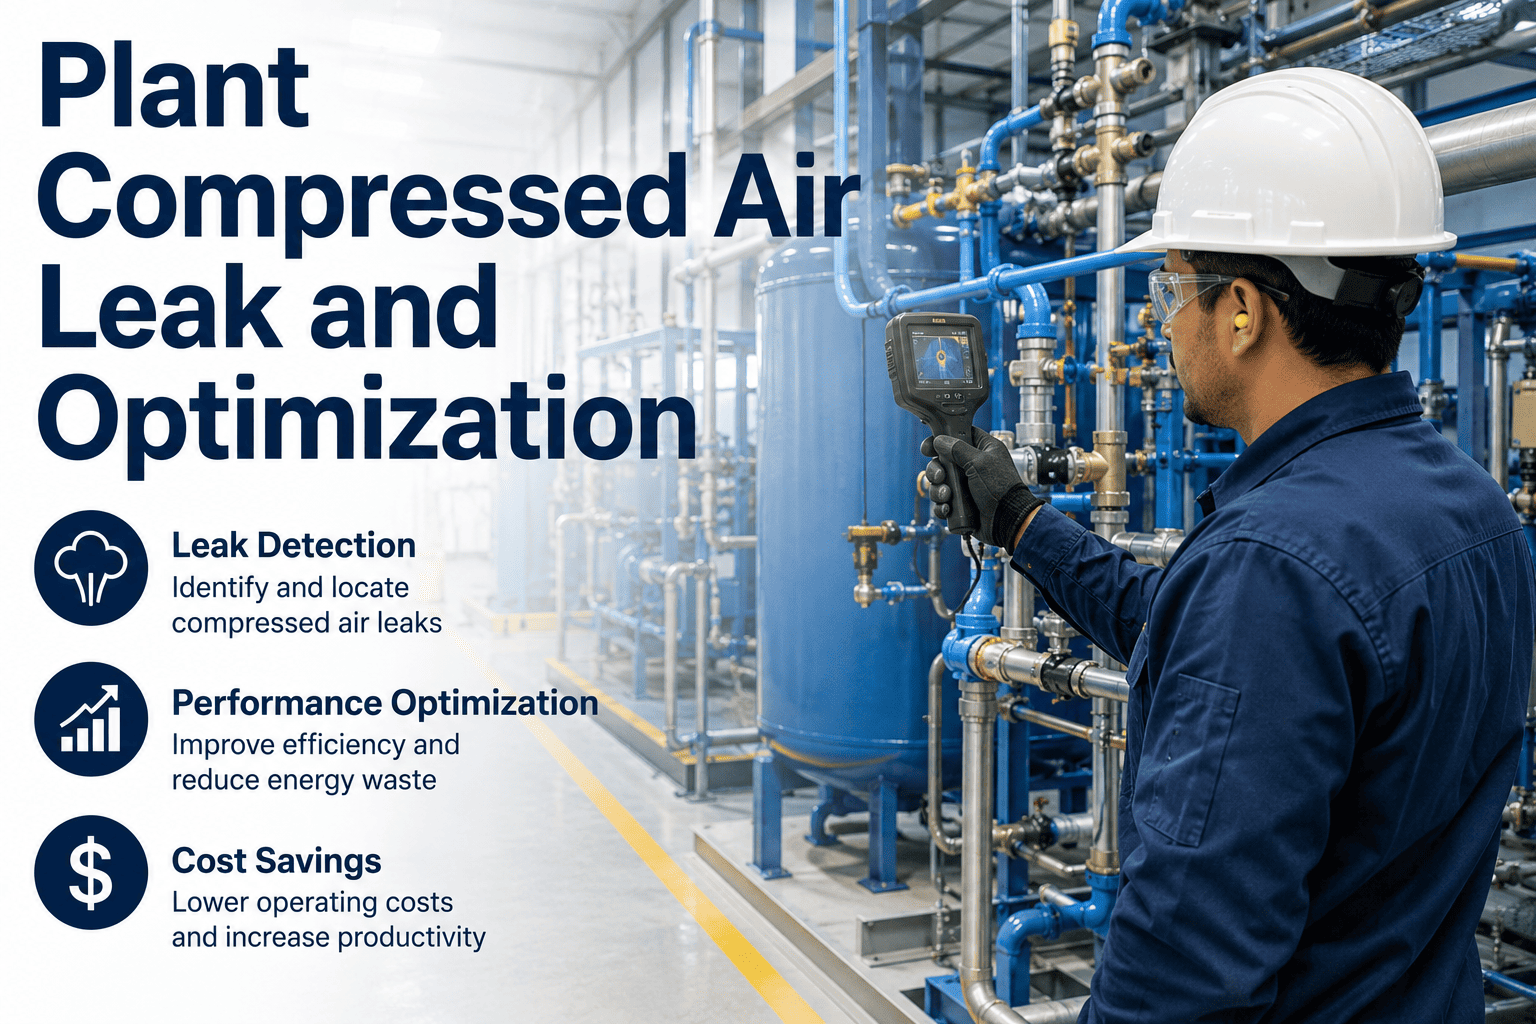
Compressed air is the most expensive utility in almost every automotive plant, and it earns that distinction almost entirely through waste rather than productive use. A single 1/8-inch leak at 100 PSI bleeds roughly 30 cubic feet per minute continuously — every hour, every shift, every day the compressors run, whether or not any tool is actually consuming air. Multiply that by the 80 to 150 leaks that a typical unmanaged plant air system accumulates over a few years of gasket wear, hose fatigue, and quick-connect failure, and the annual cost routinely exceeds $150,000 in electricity paid to compress air that never does a single unit of production work. Compressed air leak losses are not a mystery — they are measurable, locatable, and fixable — but only if the plant has a systematic detection programme rather than the annual or biennial manual survey that most facilities rely on, which misses the majority of leaks that develop and worsen in the months between surveys. Book a session with the iFactory compressed air optimization team to see how continuous AI-driven monitoring changes the economics of plant air.
Production Efficiency · Compressed Air Systems
Plant Compressed Air: Finding the Leaks, Cutting the kWh, Fixing the Sequencing
Compressed air is the most wasted utility in any automotive plant. AI-driven ultrasonic leak detection and compressor sequencing optimization close the gap between what your compressors produce and what your production actually consumes.
The Leak Size Ladder — What One Leak Actually Costs
1/16"
6.5 CFM
$1,850/yr
1/8"
30 CFM
$8,400/yr
1/4"
106 CFM
$29,800/yr
1/2"
420 CFM
$118,000/yr
Basis: 100 PSI system pressure, $0.08/kWh, continuous operation. A typical unmanaged plant carries 80–150 leaks of mixed size.
Cost Anatomy
From CFM Loss to Dollar Cost — The Calculation Chain Behind Every Leak
The financial impact of a compressed air leak is not intuitive because the connection between a hissing sound and an electricity bill passes through several conversion steps that are rarely made explicit. Understanding this chain is what allows a Compressed Air Lead to prioritize repair work by actual dollar impact rather than by how loud or accessible a leak happens to be.
01
Orifice size → CFM loss
Leak flow rate is a function of orifice diameter and system pressure, following standard compressible flow equations. At constant pressure, CFM loss scales roughly with the square of the orifice diameter — meaning a leak twice the diameter loses approximately four times the air, not twice.
02
CFM loss → compressor kW
Every CFM of compressed air requires a specific power input to generate, typically 4 to 5 kW per 100 CFM for well-maintained rotary screw compressors at typical industrial pressures — this specific power figure (kW per 100 CFM) is the conversion factor connecting flow loss to electrical demand.
03
kW → annual kWh cost
Multiplying continuous kW demand by annual operating hours (typically 6,000 to 8,000 hours for a multi-shift plant) and the plant's electricity rate produces the annual dollar cost — the number that makes leak repair prioritization a straightforward financial exercise rather than a subjective judgment call.
04
Aggregate leak cost → system oversizing
Beyond the direct energy cost of leaks, sustained artificial demand from an unmanaged leak population often forces plants to run an additional compressor, or run existing compressors at higher pressure than production actually requires — compounding the direct leak cost with system-wide inefficiency.
Detection Technology
Ultrasonic Acoustic Detection — How It Works and Why Continuous Beats Periodic
Compressed air leaks generate turbulent flow at the leak orifice that produces ultrasonic frequencies (typically 25 to 100 kHz) well above the range of human hearing and largely above the range of typical industrial background noise, which is concentrated below 20 kHz. This frequency separation is what makes ultrasonic detection technology effective even in a loud production environment — the detection instrument filters for the specific frequency signature of turbulent leak flow, which stands out clearly from motor noise, stamping impacts, or conveyor operation that would mask a leak to human hearing.
Method
Coverage
Detection Frequency
Typical Miss Rate
Best Suited For
Manual ultrasonic survey
Point-in-time, walked route
Annual or semi-annual
30–50% of leaks active at any moment
Baseline audit, initial programme establishment
Soap solution testing
Targeted, suspected joints only
Ad hoc, reactive
Very high — misses most leaks entirely
Confirming a specific suspected leak location
Fixed ultrasonic sensors
Continuous, at instrumented points
Real-time
Low for instrumented zones, zero coverage elsewhere
High-value zones — main headers, critical equipment feeds
AI-driven continuous acoustic monitoring
Continuous, plant-wide via distributed sensors
Real-time, 24/7
<10% — new leaks flagged within hours of onset
Full-plant leak population management
The critical limitation of periodic manual surveys is not detection accuracy at the moment of the survey — a skilled technician with a good ultrasonic gun finds leaks reliably. The limitation is time coverage: a leak that develops the week after the annual survey runs undetected and unrepaired for up to twelve months, accumulating its full annual cost before anyone knows it exists.
AI-Driven Continuous Monitoring
How Distributed Acoustic Sensors and AI Close the Detection Gap
Continuous AI-driven leak detection deploys a network of fixed ultrasonic and acoustic sensors at strategic points across the compressed air distribution system — main headers, branch lines to major production zones, and points near historically leak-prone equipment types (quick-connects, FRL units, rotary unions). The AI layer performs three functions that transform raw acoustic data into an actionable leak management programme.
Signal Classification
Distinguishing genuine leak signatures from background noise, valve actuation sounds, and other transient ultrasonic events common in a production environment. Trained classification models reduce false positive rates that plagued earlier generation fixed sensor systems, which often triggered constant nuisance alerts.
Leak Severity Estimation
Acoustic signal amplitude and frequency profile correlate with orifice size, allowing the AI model to estimate CFM loss and therefore annual dollar cost directly from the detected signature — automatically prioritizing the repair queue by financial impact rather than requiring separate manual estimation.
Location Triangulation
Where sensor density permits, signal timing and amplitude differences across multiple sensors allow approximate location triangulation — directing maintenance technicians to a specific zone rather than requiring a full walked survey to locate a leak that the fixed sensor network has already detected.
Trend and New-Leak Alerting
Continuous baseline monitoring allows the system to flag a new leak signature appearing at any point, or an existing leak's severity increasing over time — enabling repair before a small leak grows into a large one, which is the typical failure progression for hose and fitting degradation.
Find Out What Your Leak Population Is Actually Costing
iFactory's Compressed Air Assessment Quantifies Every Leak by CFM, kWh, and Dollar Cost
Most plants have never seen a complete, ranked inventory of their compressed air leaks with actual dollar cost attached to each one. iFactory's assessment combines ultrasonic survey data with AI-driven cost modelling to produce a prioritized repair list — starting with the leaks that cost the most, not just the ones that happen to be easiest to reach.
Beyond Fixed Lead-Lag: How AI Sequencing Adapts to Real Demand
Most multi-compressor plants operate on a fixed lead-lag sequencing scheme — a designated lead compressor runs continuously, and lag compressors start and stop based on simple pressure setpoints. This approach is simple to configure and reasonably effective at meeting demand, but it is structurally unable to account for the actual efficiency curve of each compressor at different load levels, the real-time demand variation across a production shift, or the cost differential between running one large compressor at high load versus two smaller ones at partial load. AI-driven sequencing optimization addresses each of these limitations directly.
Load-Efficiency Curve Matching
Every compressor has a specific power efficiency curve that varies with load percentage — most rotary screw compressors are meaningfully less efficient (in kW per CFM delivered) at partial load than near full load, particularly with older fixed-speed units. AI sequencing selects the combination of running compressors that collectively meets demand at the lowest total specific power, which often means running fewer compressors closer to full load rather than more compressors at partial load — a decision matrix too complex for simple pressure-based sequencing logic to solve.
Demand Forecasting
Production schedules create predictable compressed air demand patterns — a shift change, a specific production line starting a high-air-consumption process, a scheduled maintenance activity using pneumatic tools. AI models trained on historical demand patterns correlated with production schedule data can pre-position compressor sequencing ahead of anticipated demand changes, avoiding the pressure sag and reactive compressor starts that occur when sequencing only responds after pressure has already dropped.
Pressure Band Optimization
Every 2 PSI reduction in average system pressure typically reduces compressor energy consumption by approximately 1%, but most plants run higher average pressure than production actually requires — a safety margin added historically and never revisited as leaks and equipment changed the system's real pressure requirements. AI-driven pressure optimization identifies the true minimum pressure needed to satisfy the most pressure-sensitive point of use in the plant, then narrows the operating band around that minimum rather than the wide, conservative band typical of manually configured systems.
Trim Compressor Selection
In systems with variable-speed drive (VSD) compressors alongside fixed-speed units, correctly assigning the VSD unit as the trim compressor — handling the variable portion of demand — while fixed-speed units run at their efficient full-load point captures the efficiency advantage of VSD technology. Many plants with VSD compressors do not configure sequencing to exploit this correctly, running the VSD unit inefficiently or leaving it as a backup rather than the primary trim source.
ROI Framework
Building the Financial Case for a Compressed Air Optimization Programme
Compressed air optimization programmes typically have among the fastest payback periods of any industrial energy initiative, because the waste being eliminated is pure cost with no corresponding production benefit — unlike most energy efficiency investments that require balancing energy savings against production or quality trade-offs.
Initiative
Typical Investment
Typical Annual Savings
Typical Payback
Initial leak survey and repair (one-time)
$15,000–$40,000
$80,000–$220,000
1–3 months
Continuous AI acoustic monitoring (sensor deployment)
$60,000–$150,000
$50,000–$140,000/yr ongoing
8–18 months
AI compressor sequencing optimization
$40,000–$90,000
$35,000–$95,000/yr
10–20 months
System pressure reduction programme
$5,000–$15,000
$15,000–$45,000/yr
3–8 months
These figures assume a mid-size automotive plant with a 2,000–4,000 CFM compressed air demand and $0.07–$0.10/kWh electricity cost. Actual figures scale with plant size, current leak population, and existing sequencing sophistication — the initial leak assessment establishes the specific baseline for a given facility.
Compressed Air Programme KPIs
Six Metrics That Define Compressed Air System Efficiency
Specific Power
Target: <18 kW/100 CFM
Total compressor electrical power divided by total delivered CFM at rated pressure. The primary system-level efficiency metric — captures both individual compressor efficiency and sequencing effectiveness. World-class systems achieve 16–18 kW per 100 CFM; poorly optimized systems often exceed 22–24.
Leak Load Percentage
Target: <10%
Total leak CFM as a percentage of total compressed air production, typically measured via off-shift or weekend baseline load (when production demand should be near zero, remaining flow is almost entirely leaks). Industry average sits at 20–30%; well-managed systems maintain under 10%.
Mean Time to Leak Repair
Target: <5 days
Time from leak detection to confirmed repair. A leak identified but not repaired continues accumulating its full cost — detection without a responsive repair workflow captures only part of the available savings. Prioritizing the repair queue by dollar cost (not just detection order) maximizes savings per repair-hour invested.
Average System Pressure
Trend: minimize to true requirement
Mean operating pressure across the distribution system. Should be tracked against the actual minimum pressure required by the most pressure-sensitive point of use — any margin beyond that requirement, adjusted for line losses, is pure energy waste.
Compressor Load Factor Distribution
Target: >80% at full load
Percentage of total compressor operating hours spent at or near full load versus partial load. Since most fixed-speed compressors are less efficient at partial load, a high concentration of partial-load operation indicates sequencing is not correctly matching running compressor count to actual demand.
Artificial Demand Ratio
Target: <1.05
Ratio of actual compressed air demand at elevated system pressure to the demand that would exist at the true minimum required pressure — quantifies how much extra flow (and therefore extra energy) is being consumed purely because the system runs at higher-than-necessary pressure, since most pneumatic devices consume more air at higher supply pressure regardless of whether they need it.
From the Utilities Floor
“
Compressed air is unique among plant utilities in how invisible its waste is. If a cooling water line has a major leak, you see the puddle. If a steam line fails, you feel the heat and hear the release. A compressed air leak often produces a barely audible hiss lost in the ambient noise of a production floor, and the only symptom anyone notices is that the electricity bill is a little higher than expected — a signal so gradual and so easily attributed to other causes that most plants never trace it back to the actual source. In every plant I have assessed over the past two decades, the leak population was larger than facilities management believed, and the largest handful of leaks — usually five to ten out of eighty or more — accounted for the majority of the total cost. That concentration is what makes AI-driven continuous monitoring so valuable: it does not just find leaks faster than an annual survey, it ranks them by actual dollar impact so the maintenance team's limited repair time goes to the leaks that matter most, rather than being spent chasing whichever leak happens to be loudest or most conveniently located that week.
Declan O'Farrell-Nakamura
Plant Utilities Engineer · Certified Compressed Air System Specialist · 19 years optimizing industrial compressed air systems across automotive and heavy manufacturing · Former Energy Manager, multi-plant North American automotive supplier · AIRMaster+ certified auditor
Utilities Team Questions
Compressed Air Leak Detection and Optimization — Frequently Asked
How large is a typical compressed air leak population in a plant that has never run a systematic detection programme?
Plants that have never run a systematic leak detection and repair programme typically carry a leak population equivalent to 20 to 30 percent of total compressed air production — meaning roughly a quarter of every dollar spent generating compressed air is lost to leaks before any of that air performs productive work. This translates to somewhere between 80 and 150 individual active leaks in a mid-size automotive plant, distributed across quick-connect fittings (the single most common leak source), hose connections, FRL units, cylinder seals, and pipe joints. The good news embedded in this bad news is that initial leak survey and repair programmes routinely achieve some of the fastest payback of any energy initiative available to a plant, because the majority of leaks are inexpensive to repair — a new fitting, a replaced hose, a tightened connection — against savings that continue for the life of the repair. For a baseline assessment of your specific facility's leak population, book a compressed air audit with the iFactory utilities team.
How many acoustic sensors do we need to achieve meaningful continuous leak detection coverage across our plant?
Sensor density depends on the size and layout of the compressed air distribution system, but a practical starting configuration for a mid-size automotive plant typically deploys sensors at the main compressor room header, each major branch line feeding a production zone, and any known historically leak-prone areas identified from prior manual surveys — often 15 to 30 sensor points for a facility in the 300,000 to 600,000 square foot range. This configuration does not achieve leak-level location precision everywhere in the plant, but it does achieve reliable detection of new leak events at the zone level, allowing a focused ultrasonic walk-down of the flagged zone rather than a full-plant survey. Higher sensor density, approaching leak-level triangulation across the entire distribution system, is achievable but represents a larger capital investment typically justified only in facilities with extremely high compressed air cost sensitivity or very large leak populations where manual location time is the binding constraint on repair throughput. Contact our support team for a sensor deployment plan specific to your facility layout.
Will optimizing compressor sequencing risk not meeting production demand during peak compressed air usage periods?
This is the most common concern raised when introducing AI-driven sequencing, and it reflects a reasonable caution — but it misunderstands how the optimization actually works. AI sequencing optimization does not reduce total system capacity or remove the safety margin that protects against demand spikes; it improves the efficiency of how existing capacity is deployed to meet demand, and in practice includes more sophisticated demand forecasting than fixed pressure-based triggering, which means it often responds to anticipated demand increases earlier and more reliably than a system that only reacts after pressure has already begun to drop. The optimization system is configured with the same reliability constraints and minimum reserve capacity requirements that the plant's engineering team specifies — it operates within those bounds while finding the most efficient way to satisfy them, rather than removing the bounds themselves. Implementation typically includes a validation period running the optimized sequencing logic in an advisory (non-controlling) mode alongside the existing control system, allowing the engineering team to confirm the recommended sequencing would have reliably met all historical demand peaks before transitioning to live control.
How do we prioritize which leaks to repair first when we have a large backlog identified from an initial survey?
Prioritize strictly by estimated annual dollar cost, not by leak audibility, accessibility, or the order in which they were discovered during the survey — a loud, easily accessible small leak is a lower priority than a quiet, harder-to-reach large leak if the large leak's dollar cost is higher, even though the small leak feels more urgent to address. Ultrasonic survey equipment and AI-driven acoustic monitoring both provide amplitude and frequency data that correlates with leak orifice size, allowing a reasonably accurate CFM and therefore dollar cost estimate for every detected leak without requiring individual flow measurement at each location. Rank the full leak inventory by this estimated annual cost and work down the list — this approach consistently captures the majority of available savings from repairing a relatively small percentage of the total leak count, since leak cost distributions are typically heavily skewed toward a small number of large leaks rather than evenly distributed across the population. For a cost-ranked leak inventory from your facility, book a compressed air assessment with our team.
How quickly does a repaired leak population tend to regrow, and how often should the plant repeat leak detection surveys?
Without ongoing monitoring, leak populations regenerate steadily as new hose connections wear, quick-connects fail, and gaskets degrade — industry data on plants that repair leaks once and then return to periodic (annual) surveying typically shows the leak load percentage climbing back toward 15 to 20 percent within 18 to 24 months, substantially eroding the initial repair investment's ongoing value. This regrowth pattern is the core argument for continuous monitoring rather than periodic survey-and-repair cycles: a continuously monitored system catches each new leak within days to weeks of onset rather than allowing it to run undetected for up to a year, keeping the leak load percentage consistently low rather than sawtoothing between a low point immediately after each survey and a high point just before the next one. Facilities transitioning from periodic surveys to continuous AI monitoring typically see their steady-state leak load percentage settle 40 to 60 percent lower than what periodic surveying alone achieves, because the detection-to-repair cycle time shrinks from months to days.
Every Leak Has a Dollar Value. Most Plants Have Never Calculated It.
Find Your Leak Population, Rank It by Cost, and Fix What Actually Matters
iFactory's compressed air optimization programme combines AI-driven continuous acoustic leak detection with compressor sequencing optimization — quantifying every leak by CFM and dollar cost, prioritizing repairs by financial impact, and adapting compressor operation to real production demand instead of fixed pressure triggers. Most facilities recover their initial investment within the first two to four months of leak repair alone.