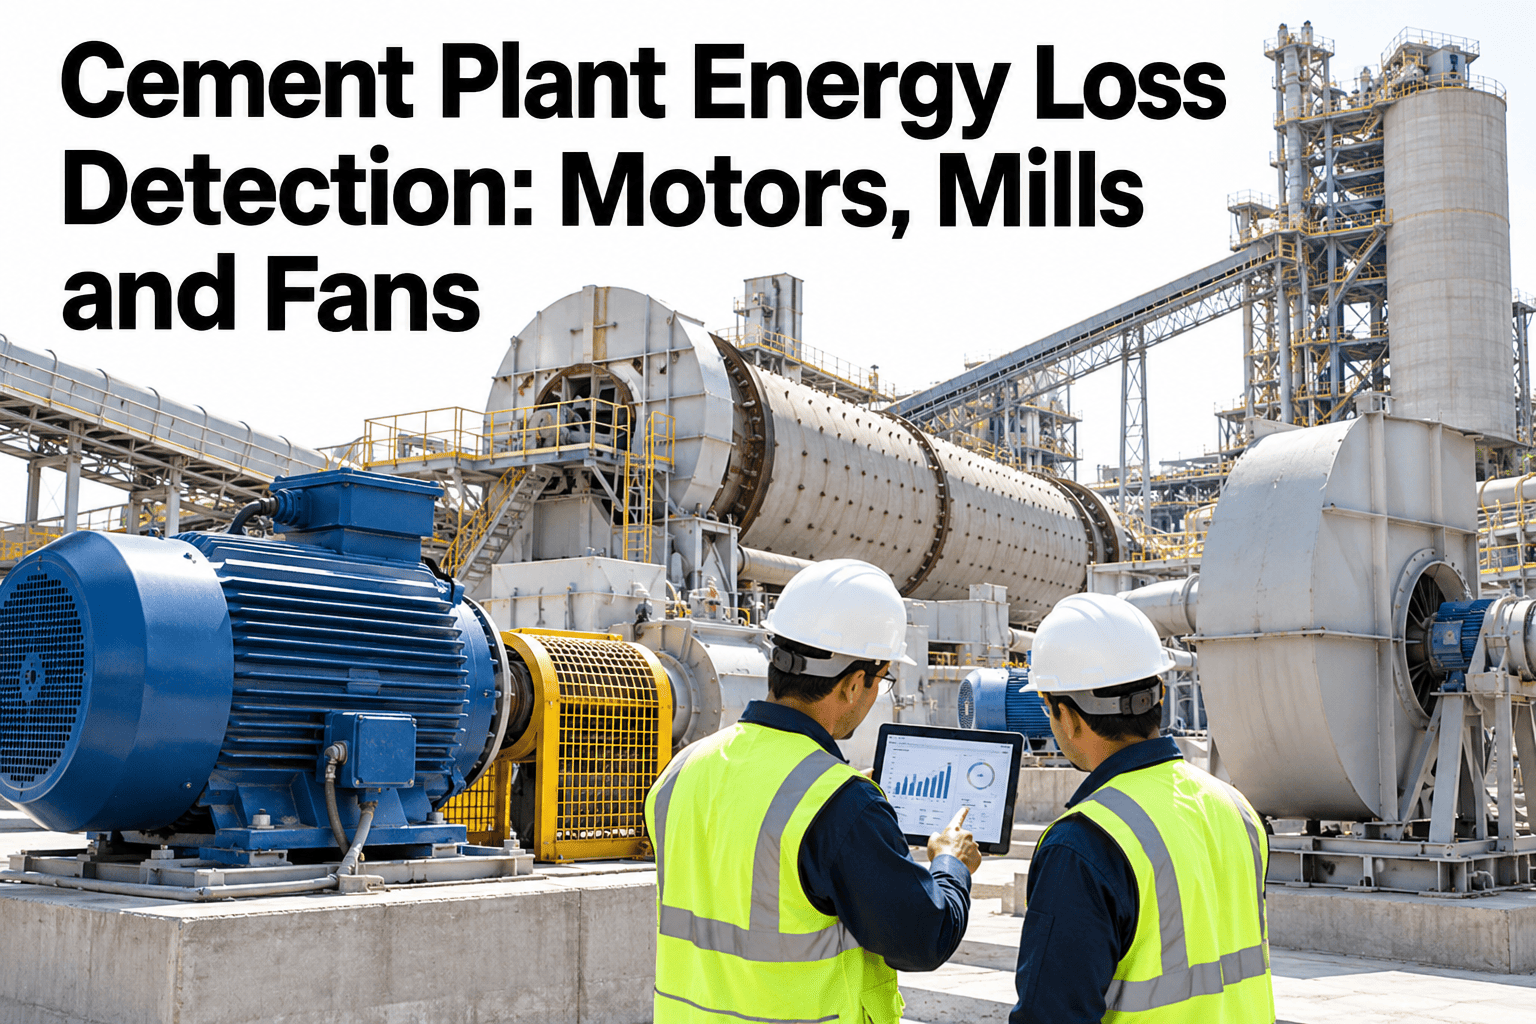
Cement Plant Energy Loss Detection for Motors, Mills and Fans

By James Smith on October 16, 2026

cement-plant-energy-loss-detection-motors-mills-fans

A motor running a few percent above its normal baseline load rarely trips anything, and a fan left running during a low-production period looks completely ordinary on a daily walk-through. These small, unflagged losses are exactly why energy loss detection has to work differently from fault detection, since there is no alarm waiting to fire, only a baseline quietly being exceeded. Comparing current load and runtime against each motor's own established normal pattern, rather than a generic plant-wide threshold, is what actually catches this kind of loss while it is still small enough to fix cheaply. If you want to see this kind of baseline comparison run against your own motor and fan data, you can review a sample deviation report with our team.

Energy loss detection, 2026

Catch the Energy Loss No Alarm Would Ever Flag

Baseline-based monitoring for motors, mills, and fans that flags deviation in load, runtime, and idle energy before it quietly becomes a permanent part of your plant's cost base.

Where energy loss typically hides
Idle equipment runningCommon, unflagged
Load drift from baselineGradual, easy to miss
Equipment triggering alarmsRare
Typical detection method neededBaseline comparison
Setting the reference point

Why Baseline Consumption Comes Before Any Deviation Check

Without a documented normal operating baseline for each piece of equipment, there is nothing to compare today's reading against, and every reading just looks like more data without context.

Equipment-specific baseline
Each motor or fan gets its own normal operating range rather than a shared plant-wide figure.
Built from recent history
Baselines are set from a recent period of known-good operation, not a theoretical nameplate rating.
Updated periodically
Baselines are refreshed as equipment ages or operating conditions genuinely change over time.
Context-aware
Baselines account for production rate, since load naturally varies with how much the line is actually running.
What gets compared

Load and Runtime Against the Established Baseline

Once a baseline exists, two figures matter most on an ongoing basis, how hard the equipment is working and how long it is actually running.

Deviation typeWhat it typically signalsFirst check to run
Load creeping above baseline Mechanical wear or misalignment developing Vibration and bearing condition check
Load below baseline for production rate Possible blockage or feed issue Material feed and process flow check
Runtime exceeding expected hours Equipment left running during idle periods Shift handover and shutdown procedure review
Frequent short cycling Control logic or sensor issue Control system and sensor calibration check

Each deviation type points toward a different investigation path, which is why a single combined alert without this breakdown tends to send the wrong team to check the wrong thing first.

The quiet cost

Why Idle Energy Deserves Its Own Category

Equipment that is on but not actually doing productive work is one of the most common and most overlooked sources of avoidable energy cost in a plant.

1
Idle periods are identified by comparing runtime against actual production output for the same window.
2
Idle energy consumption is calculated separately from productive operating consumption.
3
Recurring idle patterns, such as equipment left on through breaks or shift changes, are flagged specifically.
4
A running total of idle energy cost is tracked monthly to show the cumulative size of the opportunity.

See Your Own Idle Energy Total

Share runtime and production data for a recent period and we will estimate how much idle energy is currently going uncounted.

Getting the alert right

How Deviation Alerts Avoid Becoming Noise

A system that flags every small fluctuation quickly gets ignored, so the alert logic needs to separate genuine drift from normal day-to-day variation.

Flat threshold alerting
Same trigger point regardless of equipment or condition
Frequent false alerts during normal variation
Teams start ignoring alerts after repeated false positives
Baseline-aware alerting
Threshold set relative to each equipment's own normal range
Alerts reserved for sustained, genuine deviation
Teams trust and act on alerts because they are rarely false
Beyond the alert

Connecting Detected Loss to Maintenance Context

A flagged deviation becomes genuinely useful once it is checked against what else is known about that equipment, not reviewed in isolation.

Maintenance history
Recent service work checked against the deviation timing for a possible connection.
Equipment age and condition
Older equipment weighted differently when assessing how urgent a flagged deviation is.
Corrective action log
What was done in response to a past deviation, so recurring issues build a documented history.
Cost impact tracking
Estimated cost of each flagged loss, helping prioritize which deviations to address first.
Expert review

What iFactory Cement and Energy Specialists See Across Motor Fleets

iFactory cement and energy specialists who review motor and fan data across multiple plants consistently find that idle energy, equipment left running without corresponding production, accounts for a larger and more persistent cost than most teams initially expect, often more than the gradual load-drift cases that get more attention.

They recommend starting detection efforts on fans and auxiliary motors specifically, since these are the equipment types most commonly left running out of habit during idle periods, and the fix is almost always a simple procedural change rather than a mechanical repair.

Frequently asked questions

What Maintenance and Energy Teams Ask About This Detection

How long does it take to establish a reliable baseline for a piece of equipment?
A few weeks of normal operating data is usually enough for a stable baseline, though equipment with highly variable production patterns may need a longer period to capture the full range of normal operation. Discuss baseline setup for your equipment mix.
Can this detection work without dedicated sensors on every single motor?
Starting with higher-value or higher-consumption equipment first is a common approach, expanding sensor coverage gradually rather than instrumenting the entire motor fleet at once. Ask about a phased rollout with our support team.
How does the system avoid flagging normal seasonal or production-driven variation?
Baselines are built to reflect typical variation across different production rates, so the alert logic compares against the expected range for current conditions rather than a single fixed number. See how seasonal variation is handled on a short call.
Who typically receives and acts on a flagged deviation alert?
Alerts usually route to the maintenance team for load-related deviations and to shift supervisors for runtime or idle-related deviations, since the appropriate response differs between the two. Map alert routing for your team structure.
Can this estimate the actual cost impact of a detected loss?
Yes, once equipment-level energy cost is established, a flagged deviation can carry an estimated cost figure, which helps prioritize which issues are worth addressing first. Discuss cost estimation with our team.
Catch the loss no alarm would ever flag

Bring Baseline-Based Energy Loss Detection to Your Plant

Book a session with iFactory AI to see motor, mill, and fan deviations flagged against your own equipment baselines.
Share This Story, Choose Your Platform!