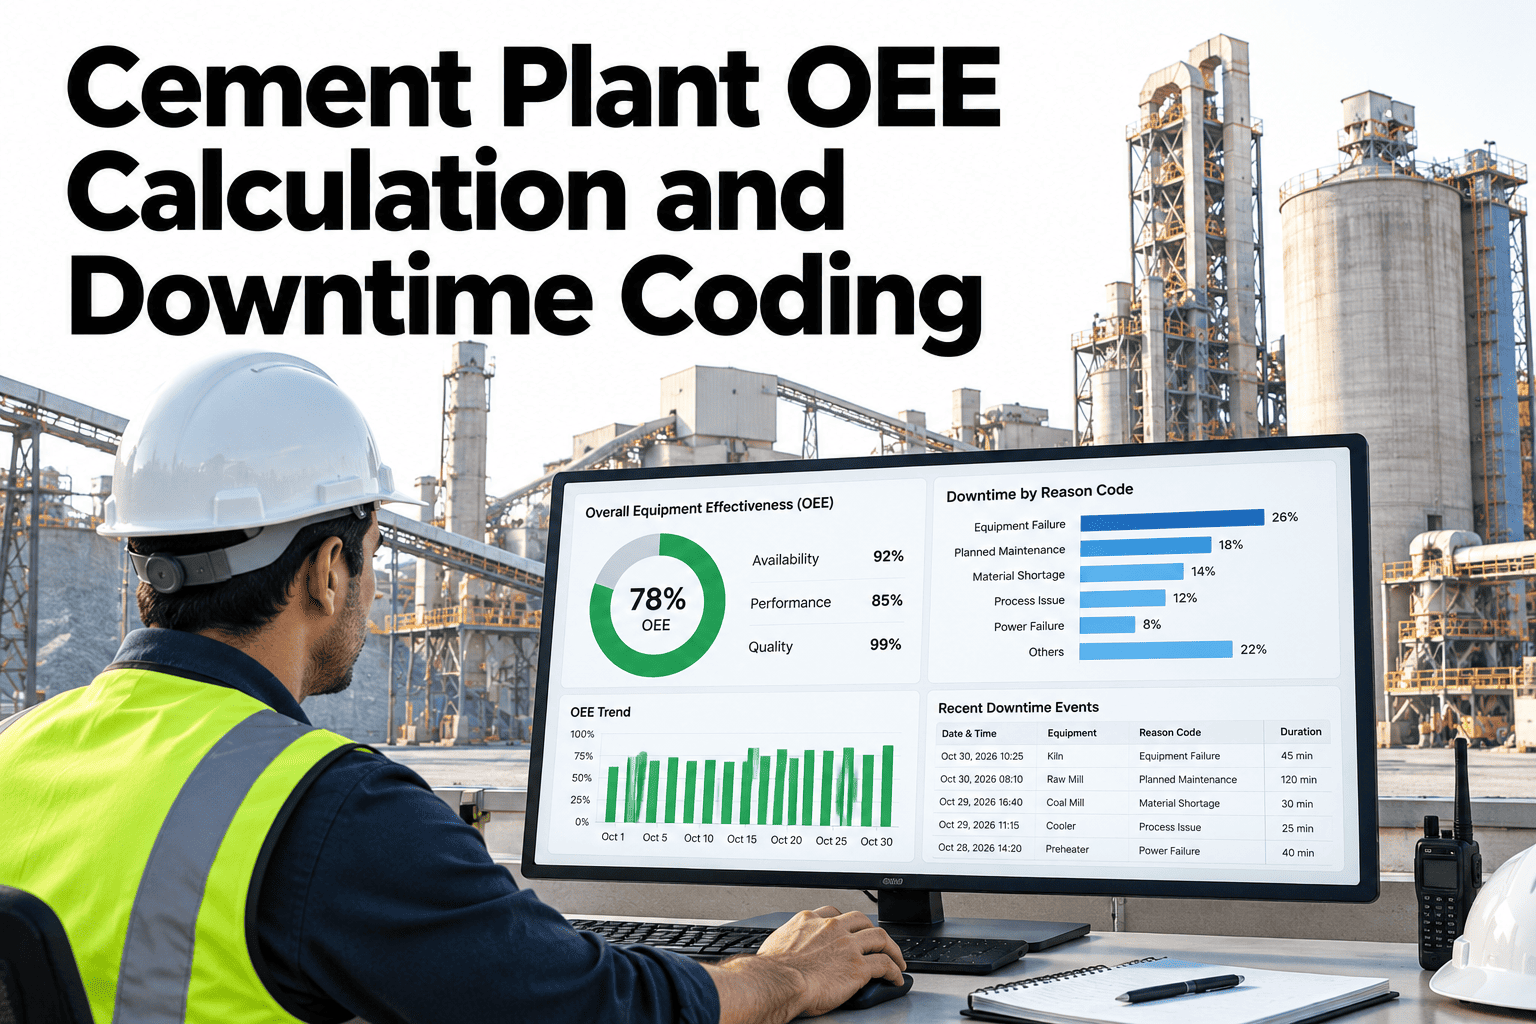
Ask three people at the same cement plant how OEE is calculated and it is not unusual to get three slightly different answers, especially around what counts as planned versus unplanned downtime, and whether a quality loss gets subtracted from availability or from performance. Those small definitional differences compound over a year into a number that looks precise on a report but means something different depending on who built it. A clear formula, consistent downtime categories and documented shift rules are what make an OEE figure something teams can actually compare and trust over time. Plant leaders can discuss their own OEE methodology and use case with iFactory AI before the next reporting cycle.
An OEE Number Is Only as Trustworthy as the Rules Behind It
iFactory AI applies one documented OEE formula and downtime category set consistently, so the number means the same thing every time it is reported.
Where OEE Calculations Quietly Diverge
The OEE formula itself is simple, three factors multiplied together, but the inputs feeding each factor are where plants most often diverge from each other, and sometimes from one reporting period to the next within the same plant.
Disagreement over whether scheduled maintenance counts against planned time.
The same stoppage coded differently depending on who logs it.
Rework and scrap sometimes counted inconsistently against the quality factor.
Different shifts applying slightly different rules for the same stoppage type.
The Formula and Its Components
| Factor | Formula | What It Captures |
|---|---|---|
| Availability | Run time ÷ planned production time | Time lost to unplanned and planned stoppages |
| Performance | Actual output ÷ theoretical maximum output | Speed losses and minor stops below full rate |
| Quality | Good output ÷ total output | Product that does not meet specification |
Review Your Own OEE Methodology
Bring your current calculation approach to a 30-minute working session.
Building a Downtime Category Set That Holds Up
A small set of categories covers nearly every stoppage type.
Detail sits underneath each top-level category for specificity.
Written rules remove ambiguity about edge cases across shifts.
A review group owns changes to the category set over time.
Why the Theoretical Maximum Rate Needs Its Own Scrutiny
The performance factor depends entirely on an accurate theoretical maximum output rate, and this number is sometimes set once at commissioning and never revisited, even as equipment ages or process changes shift what a realistic maximum actually looks like.
A theoretical maximum that no longer reflects reality skews the performance factor in ways that are easy to misread, either flattering a plant that is actually running well below a stale benchmark or unfairly penalizing one that has made genuine improvements the outdated number does not account for.
A Scenario: The OEE Number That Didn't Match the Floor
Picture a monthly OEE report showing a steady 82 percent, while the shift supervisors on the floor describe a month that felt noticeably worse than that number suggests.
A review of the underlying downtime codes sometimes finds the gap: a changeover delay that one shift logs as planned downtime and another logs as unplanned, each choice technically defensible but producing different availability numbers for what was functionally the same event. Once the rule is written down and applied consistently, the OEE figure starts to match what the floor is actually experiencing, which is usually more valuable than the number moving up or down on its own.
Why Benchmarking Against Other Plants Rarely Works Cleanly
Comparing OEE across plants, or even against published industry benchmarks, is tempting but often misleading unless both sides are using genuinely the same definitions, which in practice is rare given how much variation exists in how different organizations handle the same edge cases.
A plant is usually better served comparing its own OEE trend over time, under a stable and documented methodology, than chasing a cross-plant comparison where an apparent gap may reflect nothing more than a difference in how changeovers or minor stops happen to be coded at each site.
Inconsistent Coding vs a Governed Category Set
Connecting OEE to the Conversations It Should Actually Drive
A trustworthy OEE number is only valuable if it leads somewhere, informing a maintenance priority, a changeover improvement project, or a staffing decision. A number nobody trusts gets quietly ignored in those conversations, even while it continues to appear on a monthly report.
Getting the methodology right is not an end in itself, it is what makes the number credible enough to actually shape the decisions it was meant to inform in the first place, rather than becoming a figure people nod at in a meeting and then set aside.
What Belongs in a Downtime Category Standard
Why Shift Rules Need to Be Written, Not Assumed
A rule that lives only in one supervisor's head works fine until that supervisor is off shift, at which point the next person makes a reasonable but different judgment call on the same type of event, and the OEE record quietly becomes inconsistent without anyone deciding that outcome on purpose.
Writing the rule down, with a specific example of how to classify a common ambiguous case like a short changeover delay or a minor jam, removes that dependency on any one person's memory and keeps the record consistent regardless of who is on shift when the event happens.
Common Edge Cases Worth Defining in Advance
A handful of recurring situations account for most of the inconsistency in downtime coding at cement plants. Defining these in advance, rather than leaving them to individual judgment, removes most of the ambiguity that erodes trust in the OEE number.
Clarify whether a delay beyond the standard changeover time counts as planned or unplanned.
Define a minimum duration threshold for logging a stop versus treating it as speed loss.
Decide whether ramp-up time after a stop counts against performance or availability.
Clarify how a utility outage or supply shortage outside the plant's control is categorized.
Rolling Out a Revised Standard Without Breaking Historical Trends
Changing a downtime category standard midstream raises a fair concern, that historical trend comparisons become harder once the rules change. A thoughtful rollout addresses that concern directly rather than ignoring it.
Where iFactory AI Fits
Applies one formula
Calculates availability, performance and quality consistently every time.
Standardizes downtime codes
Uses the same category set across every line and shift.
Tracks shift rules
Keeps the documented rule set visible and applied consistently.
Supports governance
Logs changes to the category set so the history stays traceable.
Expert Review
A cement operations perspective, reviewed for accuracy before publication: OEE is a genuinely useful metric, but only when the definitions behind it are stable enough to compare over time, and most plants underestimate how much their own number drifts simply from inconsistent coding rather than real operational change. A written, governed standard is a small upfront effort that pays off every time the number gets reported. Reviewing your own current OEE methodology against this structure often surfaces a gap or two quickly. Confirm specific feature capabilities against your plant's systems before relying on any workflow.
Frequently Asked Questions
Should scheduled maintenance count as planned downtime?
Most standard OEE methodologies exclude scheduled maintenance from planned production time entirely, rather than counting it as a loss, though the specific choice should be documented and applied consistently across the plant. Discuss how scheduled maintenance should be treated for your OEE.
How many downtime categories does a cement plant typically need?
Most plants find a focused set of six to eight top-level categories, with sub-categories for detail underneath, strikes a good balance between specificity and ease of consistent use. Ask about a category structure sized for your operation.
Who should own changes to the downtime category standard?
A small cross-functional group, typically operations and reliability, works best, with changes made on a set review schedule rather than informally whenever a disagreement comes up. Explore a governance structure for your category standard.
Can historical OEE data be remapped to a new category standard?
Usually yes, through a one-time mapping exercise from old categories to new ones, though some historical entries may need a judgment call to classify under the new structure. Talk through remapping your historical downtime data.
How does this help across multiple kilns or plants?
A shared formula and category standard makes OEE genuinely comparable across lines and sites, which is often the point where plants discover their numbers were never truly comparable to begin with. See how a shared standard works across multiple lines and sites, even where equipment and operating conditions differ.
Make Your OEE Number Mean the Same Thing Every Time
iFactory AI applies one formula and one downtime category standard consistently across your plant. Discuss your own plant data and use case.