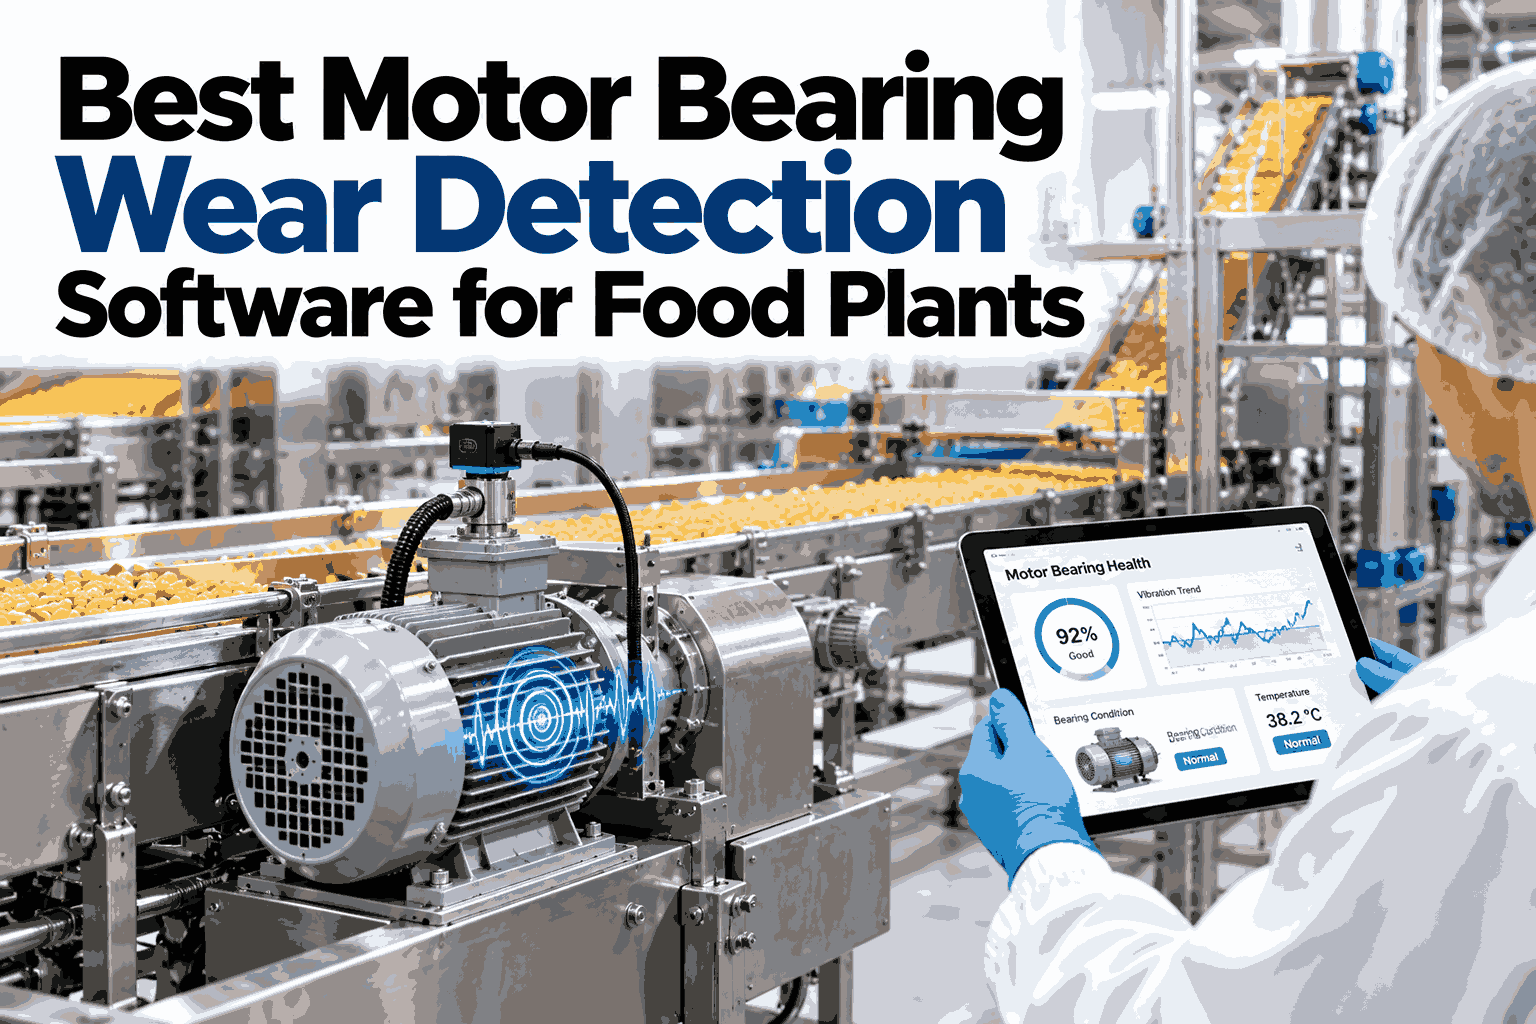
A motor bearing rarely fails without warning, but in a food plant the warning is easy to miss. Washdown spray, sanitation chemicals, cold rooms and constant start-stop cycles all hide the early signs that a bearing is wearing out. By the time an operator hears the noise, the motor is often days from seizing a conveyor, a mixer or a filler mid-shift. The best bearing wear detection software reads vibration, heat and motor current together, so the fault is caught weeks earlier. Teams shortlisting tools can watch iFactory AI score the bearings on a real running motor before deciding.
Catch Bearing Wear Weeks Before the Line Stops
iFactory AI combines vibration, thermal and motor current signatures into one bearing health score, tuned for washdown and cold-chain conditions.
How a Bearing Wears Out: Four Stages
Bearing failure is a slow slide, not a sudden event. Each stage leaves a different fingerprint, and the earlier software spots it, the more options a planner has.
Tiny surface pitting appears. Only high-frequency vibration and envelope analysis pick it up. Nothing is audible or warm yet.
Repeating fault tones show up at the bearing's characteristic frequencies. Motor current begins to carry faint sidebands.
Friction raises bearing temperature and the motor gets audible. This is where most manual routes finally notice.
Vibration and heat climb fast. Shaft play, cage breakup or seizure follows, often mid-production.
The purpose of good software is to move your first alert from stage 3 back to stage 1 or 2, where a repair can be booked into a planned sanitation window.
Why Food Plants Are Harder Than Other Factories
Generic condition monitoring was built for dry, stable plants. Food manufacturing adds conditions that distort sensors and speed up wear.
Washdown ingress
High-pressure water and caustic cleaners can push past seals, wash out grease and corrode races from the inside.
Thermal swings
Motors move between cold rooms, ovens and hot rinses, so a fixed temperature limit throws false alarms or misses real heat.
Variable loads
Mixers, conveyors and pumps change speed with each recipe. Software must learn each operating state, not one baseline.
Lubrication limits
Food-grade grease and strict contamination rules limit how often and how freely bearings can be relubricated.
Sanitation windows
Repairs must fit narrow cleaning gaps, so early notice is worth far more than in a plant that can stop at will.
Hard-to-reach motors
Many motors sit inside enclosures or over open product, which makes handheld route-based checks slow and risky.
Three Signals, Three Different Views of the Same Bearing
No single signal is enough. Each one sees wear at a different point in its life and fails in a different way in a wet plant.
Bar length shows how early in the wear cycle each signal typically becomes useful, not a measured percentage.
Envelope analysis isolates the repeating impacts from a damaged race or rolling element. Sealed, stainless-housed sensors survive washdown.
Motor current signature analysis reads the drive cabinet, not the wet motor. It suits motors that cannot carry a sensor.
Temperature trends, compared against load and ambient, back up the other two signals and expose lubrication failure.
See Which Motors Would Alert First on Your Line
Book a 30-minute session and bring a list of your critical motors. iFactory AI will map which signals suit each one.
Scorecard: What the Best Software Must Do
Use this list to compare any tool you are considering. A product that misses several rows will produce noise or blind spots in a washdown plant.
| Capability | What to Look For | Risk If Missing |
|---|---|---|
| Multi-signal fusion | Vibration, thermal and current read together | Single-signal false alarms |
| Operating-state baselines | Separate normal ranges per speed, load and recipe | Alerts every product changeover |
| Fault identification | Names race, cage or rolling element defect | Unclear what part to stock |
| Remaining-life estimate | Trend-based weeks-to-failure range | Repairs cannot be scheduled |
| Washdown-ready hardware | Sealed, corrosion-resistant sensors | Sensor failure after cleaning |
| Work order link | Alert opens a task with the fault detail | Findings stay in a dashboard |
How to Rank Motors Before You Monitor Them
Monitoring every motor on day one is rarely sensible. Rank by what a failure costs, then start where the downside is largest.
No backup, whole line down. Monitor first.
Failure could spoil batches or contaminate product.
Motors with slow replacement times or custom mounts.
Add once the first three groups run smoothly.
A Composite Scenario: The Conveyor Motor That Whispered First
Picture a packaging line where a drive motor on the main infeed conveyor is checked by a monthly handheld route. Two weeks after a clean route reading, the motor seizes during peak production.
A continuous system watching the same motor would have shown a rising defect tone in vibration and a matching current sideband well before the heat appeared. The bearing could have been swapped in the next Sunday sanitation window, with a spare already on the shelf.
Where iFactory AI Fits
iFactory AI is built to turn raw machine signals into a plain ranking a maintenance planner can act on.
One health score per motor
Vibration, thermal and current readings merge into a single score, so a planner sees the worst motors first.
Learns each operating state
Baselines adapt to speed, load and recipe, which cuts nuisance alerts during changeovers and washdown.
Fault type in the alert
Alerts describe the likely defect and urgency, so the right bearing and tools are ready before the stop.
Feeds maintenance planning
Findings flow into work orders and spare planning, so the repair lands inside a sanitation window.
Frequently Asked Questions
What is the best way to detect motor bearing wear in a food plant?
Combining vibration, thermal and motor current data works best, because each signal covers a different stage of wear and a different weakness of the washdown environment. A single signal tends to miss early faults or raise false alarms after cleaning. Fusing all three gives the likely fault type, its severity and its trend over time, so planners know what to fix and when. A guided walkthrough of one motor's bearing health score shows this in practice.
Can bearing wear be detected without putting sensors on wet motors?
Yes. Motor current signature analysis reads electrical data from the drive or motor control cabinet, well away from spray, steam and cleaning chemicals. It is less sensitive than vibration for some faults, but it suits motors that are enclosed, sit over open product or are hard to reach. Many plants use it as a first layer and add sensors only on the most critical assets. Book a quick review of which of your motors suit current-based monitoring.
How early can software warn me before a bearing fails?
It depends on the motor, load, speed and fault type, but the aim is to alert at the early defect stages, which can leave weeks to plan a repair instead of hours. Fixed temperature alarms usually fire much later, because heat only rises once damage is advanced. A trend view also shows how quickly wear is moving, which helps decide whether to repair now or wait for the next window. See a session that maps warning windows for your own motors.
Will washdown cycles trigger false alarms?
They can with basic tools that apply one fixed limit to every condition. Software that learns separate baselines for cleaning, idle, startup and full-load periods filters out most of that noise. It also compares each motor with its own history instead of a generic threshold, so a normal spike after a rinse is not mistaken for damage. That keeps alerts meaningful and reduces alarm fatigue. Explore baselines built around your own washdown routine with the team.
Which motors should we monitor first?
Start with motors that stop a whole line, put product at risk or have long spare lead times. Ranking by the cost of failure gives the fastest return and a clean, low-risk pilot. Once alerts prove reliable, extend coverage to pumps, fans, gearboxes and secondary conveyors, using the same scoring so results stay comparable. Bring your equipment list to a working session that ranks your motors by failure cost.
Stop Finding Bearing Failures by Their Noise
iFactory AI reads vibration, heat and motor current together so your team plans bearing repairs inside sanitation windows. Book a walkthrough on your own motors.