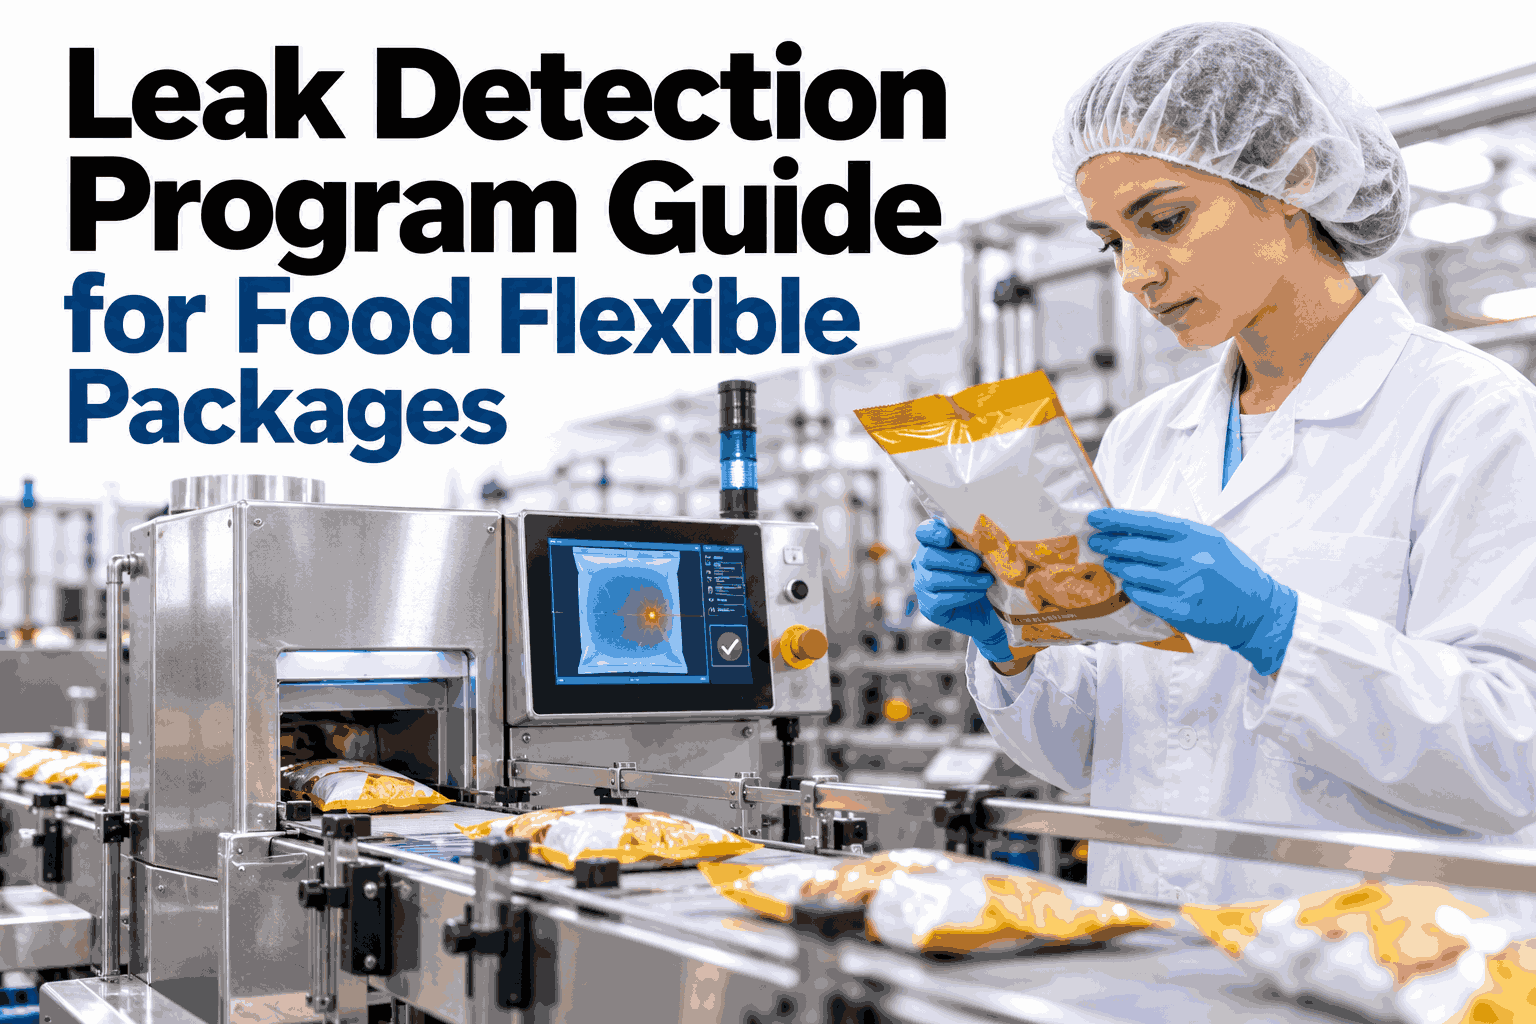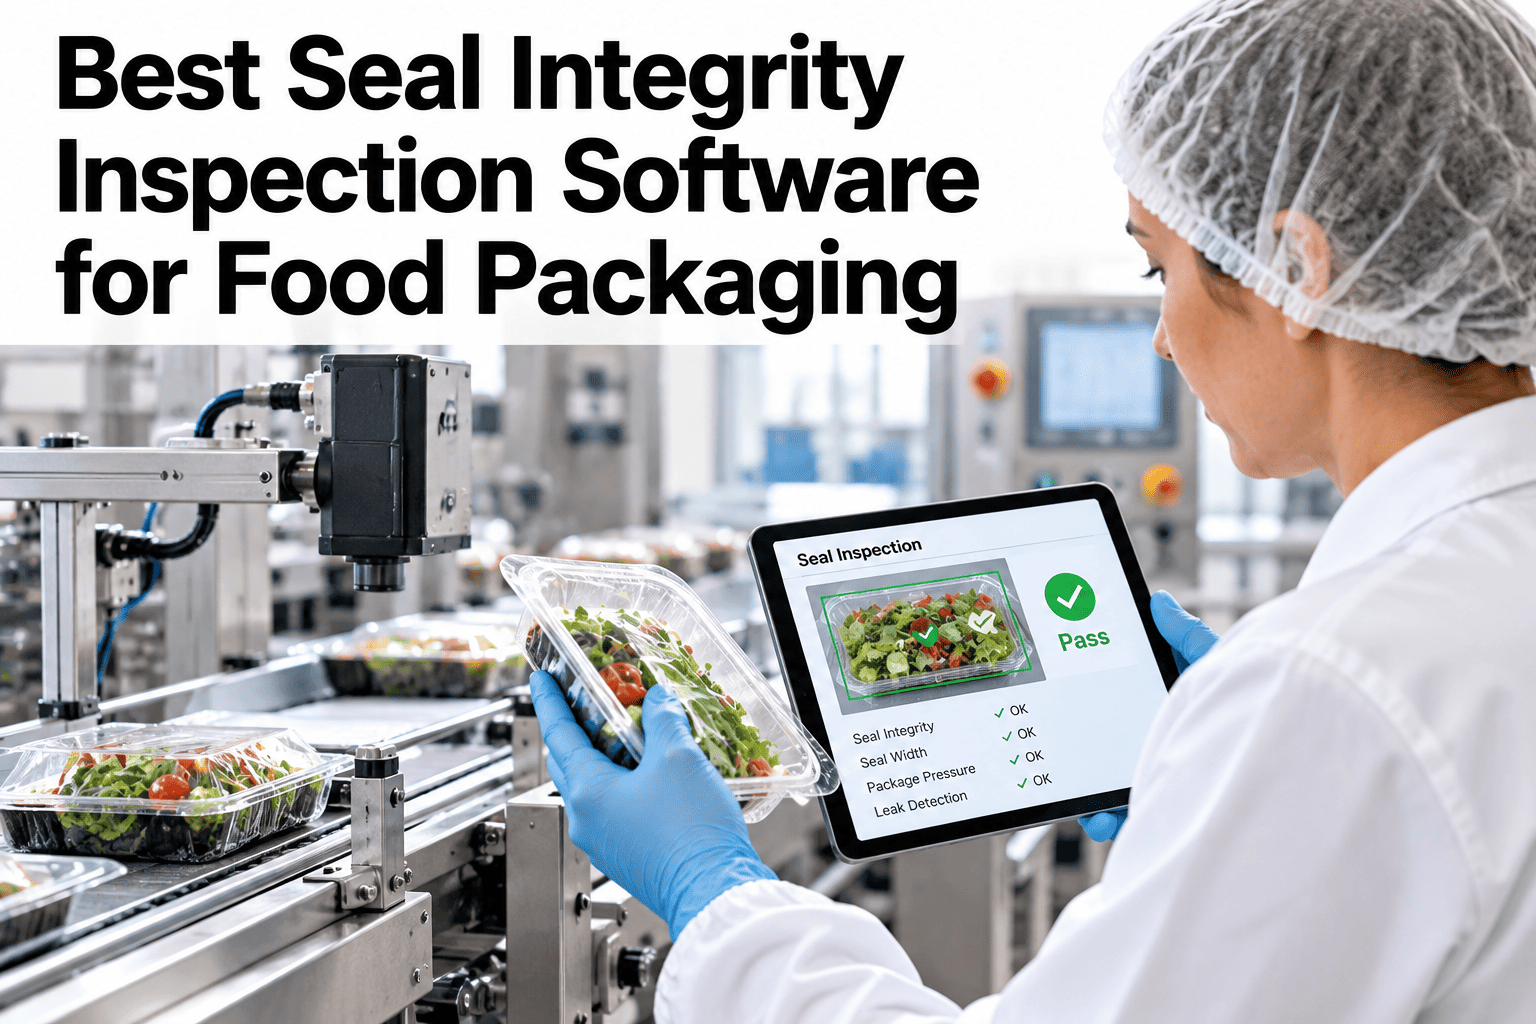
A flexible package can look perfectly sealed on the line and still leak by the time it reaches the distribution center. The culprit is often a seal channel, a path through the seal narrow enough to escape a quick glance and wide enough to let air in or product out. Channels as small as half a millimetre can shorten shelf life or cause a return. Catching them takes more than looking: it takes vision inspection of the seal area combined with leak testing. Packaging teams can review how combined seal vision and leak testing would run on their own lines and what it would catch.
Catch the Half-Millimetre Seal Channel Before the Truck Leaves
iFactory inspection software combines vision of the seal area with leak testing, so channels, wrinkles and contamination are caught at the line.
A Good Seal and a Channel Leak
Both seals can look closed from above. Only one holds. The channel is a narrow path through the sealed area.
Schematic only. Real channels are far smaller relative to the seal width.
Vision Only vs Vision Plus Leak Test
Each method sees what the other can miss. Together they cover more of the failure modes.
Seal Defects Worth Looking For
Different defects come from different causes and need different fixes.
Channels and gaps
Narrow openings in the seal area that allow leaks
Wrinkles and folds
Material folded into the seal, often leaving weak spots
Contamination in the seal
Product, grease or dust between the layers
Inline Seal Inspection From Seal to Reject
The flow stays short so it can run at line speed.
See What Your Seals Are Hiding
Send a few packages with known seal problems. We will show what vision, leak testing and both together catch.
From Defect to Cause to Fix
Seal defects are signals about the sealing process. Read them that way.
| Defect | Likely Cause | First Check |
|---|---|---|
| Channel through seal | Low pressure or uneven jaw contact | Jaw pressure and alignment |
| Wrinkled seal | Film tension or fold during forming | Film path and tension |
| Weak seal | Low temperature or short dwell | Temperature and dwell time |
| Contaminated seal | Product in the sealing area | Fill and product handling |
Where Seals Fail Most Often
Frequency varies by plant. Rank your own causes to decide where to focus.
Illustrative frequency. Your own reject records give the real ranking.
Disposition: Pass, Review or Reject
A three-way decision keeps the line moving without letting doubtful packs through.
Rolling Out Seal Inspection
Start where seal failures cost the most.
Sealing Process Variables That Matter
Seal quality comes from a handful of settings. Track them along with inspection results.
Temperature
Too low gives weak seals, too high can damage the film
Pressure
Uneven pressure leaves channels or thin spots
Dwell time
Short dwell may not fuse the layers properly
Jaw condition
Worn or dirty jaws produce repeating defects
Inspection Methods Compared
Each method has a place. Many plants combine two or three.
| Method | Strength | Limit |
|---|---|---|
| Seal area vision | Fast, sees every pack, finds contamination and wrinkles | Cannot confirm a fine channel is leak-free |
| Leak test | Confirms whether the pack holds | Usually slower and applied to selected packs |
| Manual peel or burst test | Measures seal strength directly | Destroys the pack and samples only a few |
| Pack weight and gas checks | Detect loss of product or atmosphere | Indirect and later in the process |
Responding to a Seal Failure Trend
Treat a rising reject rate as a signal about the process.
Lot-Level Release vs Pack-Level Inspection
Sampling a lot leaves room for failures. Inspecting every pack closes it.
Cost of a Seal Failure by Stage
The later a leak is found, the more it costs.
Illustrative relative cost. Your own returns and rework figures give the real ones.
What Experienced Packaging Engineers Look For in Seal Inspection
Frequently Asked Questions
How small a channel can inspection find?
It depends on the film, seal width and test method. Combining vision with leak testing reaches finer defects than either alone. Detection depends on film clarity, seal width, camera resolution and test pressure, so the practical limit should be shown on samples from your own packaging. Collect a few packs with known defects of different sizes during setup, and use them regularly as a check that the system still finds what it should. Test your own smallest problem channels with our engineers.
Will inspection slow our line?
Inspection is designed to run at line speed, with leak tests applied where needed. Stations are sized for your pack rate and layout. Leak tests can be applied to a selected share of packs or to specific lots, which keeps throughput while still checking the packs most at risk. Where a leak test is slower than the line, a diverter and a short holding lane can keep the line moving while selected packs are tested.
Do we still need manual seal checks?
Periodic checks remain a useful reference and calibration. Automation covers every pack, and manual checks confirm the system stays accurate. Periodic manual checks also serve as a reference for calibrating the automatic system and for confirming it still agrees with the physical seal. A weekly manual check logged alongside automatic results gives a simple record of agreement between the two methods. See how both fit together on one line in a short walkthrough.
What about different film types?
Films vary in transparency, gloss and sealing behavior, so each needs its own settings. Calibrate on real samples of every film you use. Metallized, clear and laminated films reflect light differently, so each family needs its own vision settings and its own reference samples. New films should go through a short trial before first use, so settings are ready by the time the film is in production.
How does this help with customer complaints?
Lot-level records show which packs were tested and passed. A record showing the exact lot, line and time of inspection lets the quality team answer a complaint quickly and with evidence. Keeping images of rejected seals with the lot record also helps the team see how a defect looked when a complaint is investigated. Explore how seal records support complaint investigations on a call.
Stop Leaks Before They Reach the Distribution Center
Bring your packages and your reject history. We will show the seal problems inspection would catch at the line.