A tablet press is one of the hardest working machines in a solid dose plant. Punches and dies take millions of compression cycles, the turret spins at high speed and pressure rollers carry heavy loads, all while producing tablets that must meet weight, hardness and appearance specifications. When something wears, the press often keeps running while quality drifts, until a punch sticks, a bearing seizes or a force overload stops the line. Predictive maintenance uses the data the press already produces, plus a few added sensors, to spot those problems before the next campaign. This guide covers failure modes, compression force as a health signal, tooling life management and how to plan work around campaigns. To see press monitoring on your machines, book a short walkthrough.
Tablet Press Predictive Maintenance: Catch Tooling Wear and Bearing Faults Before the Next Campaign
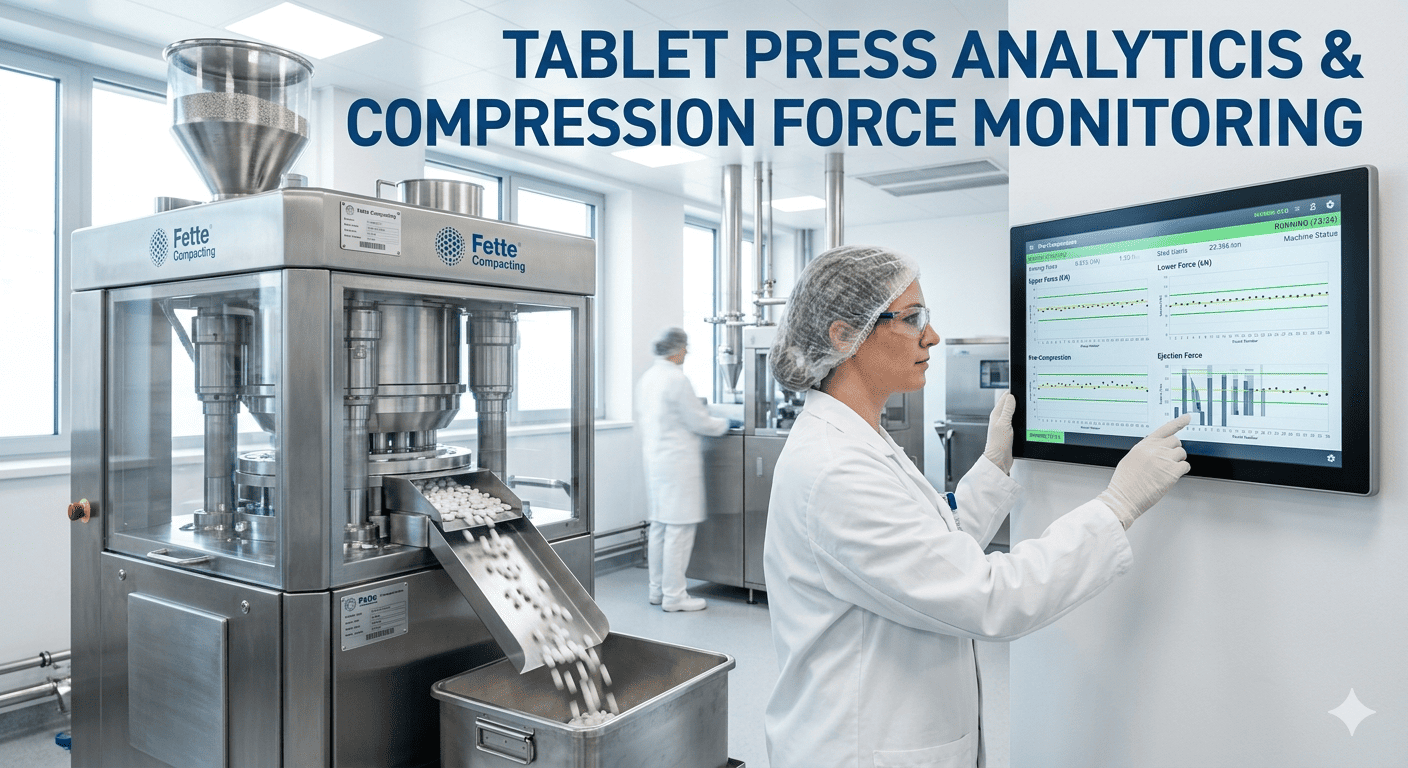
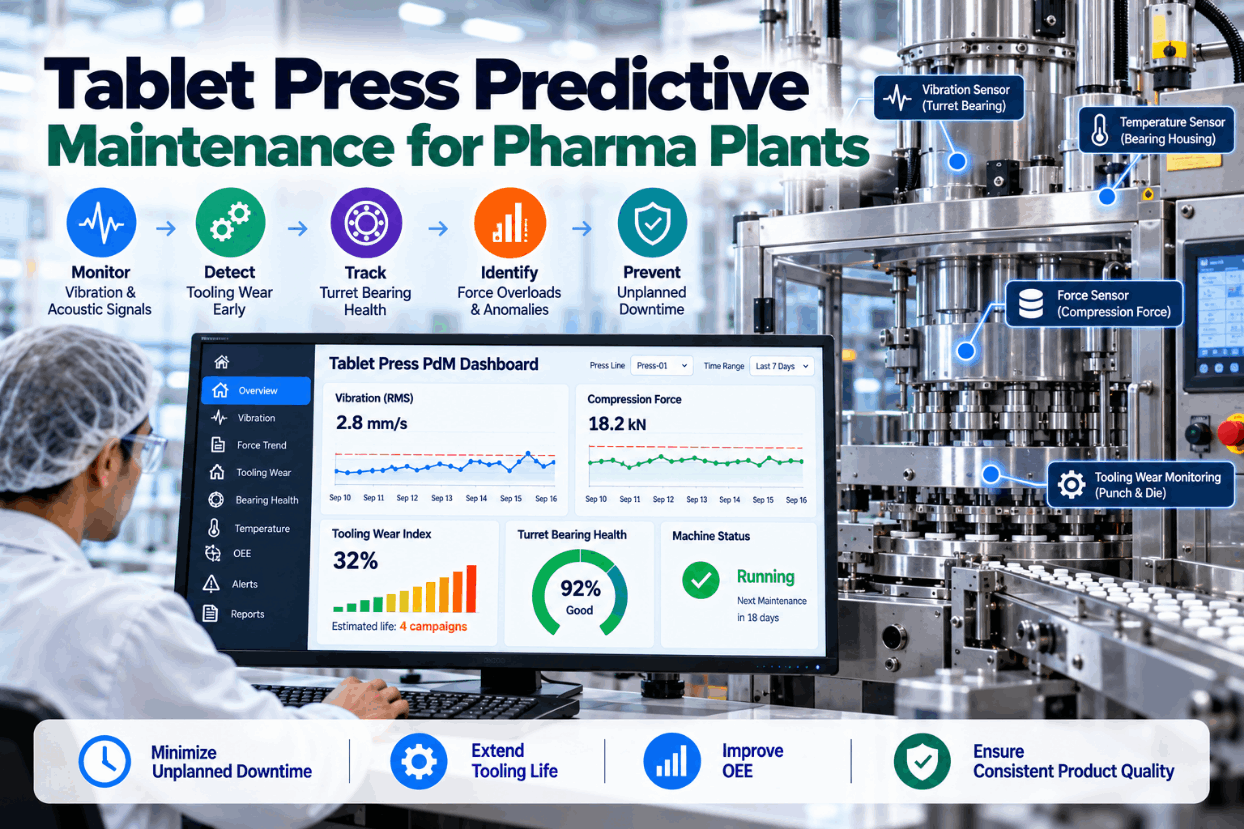
Compression force profiles, turret vibration and drive current trended per station, so tooling and bearings are serviced at changeovers instead of mid-run.
Why Tablet Press Problems Hurt Twice
Tablet press failures cost in two ways. The first is downtime: a seized bearing or broken punch stops the press, and in a campaign-planned plant, that can push back every product behind it. The second is quality: worn tooling and drifting mechanics often do not stop the press at all. They produce tablets with more weight variation, capping, sticking or picking, which lead to deviations, rejected tablets and investigations.
Pharma plants have little slack to absorb either. Benchmarks compiled by IntuitionLabs put industry-wide pharma OEE at around 35–37%, with roughly one-third of time lost to planned activities such as cleaning, changeover and setup. Unplanned stops on top of that are expensive, and much of the planned time could be better used if maintenance were targeted.
Predictive maintenance targets both costs: it prevents stops and catches the wear that causes quality drift. We can review your press downtime and deviation history on a call.
Tablet Press Failure Modes Worth Watching
A handful of components cause most tablet press problems. Each has a signature in the data.
| Component | What goes wrong | How it shows | Consequence |
|---|---|---|---|
| Punch tips | Wear, J-hooks, lost land, damage | Force scatter or offset on one station | Weight and hardness variation, capping |
| Punch barrels and heads | Scratches, wear, tight fit | Rising ejection or pull-down force | Binding, press stops |
| Dies | Bore wear rings, build-up | Ejection force rising | Sticking, dark spots from scorched build-up |
| Turret and guides | Punch guide wear, misalignment | Station-specific force patterns, vibration | Tooling damage, uneven tablets |
| Pressure rollers | Bearing wear, surface damage | Periodic force pattern each revolution | Force variation across stations |
| Cams and tracks | Wear, lubrication issues | Noise, vibration, force irregularities | Punch damage |
| Main drive and gearbox | Bearing and gear wear | Vibration and current changes | Unplanned stops |
Natoli notes that material build-up from punch and die wear can scorch and break off into the formulation, causing dark spots in tablets. That makes tooling wear a quality issue as much as a maintenance one. Our engineers map these modes to your press models.
Compression Force: The Press’s Built-In Health Monitor
Most modern presses measure compression force on every tablet for weight control. The same data is a detailed health record of the tooling and mechanics, if it is analysed per station and over time.
The key is to look at the data by station and over weeks. The press’s own control loop uses force to adjust fill and reject tablets in real time; it is not designed to spot slow mechanical trends. A separate analysis layer does that.
Because the force data already exists, this is usually the fastest predictive maintenance win on a press. We can show it on your data in a demo.
Managing Punch and Die Life With Data
Tooling is one of the largest recurring costs on a press, and Natoli points out that poor handling is the main cause of tooling damage. A data-driven tooling program combines careful handling with condition-based decisions.
Each tooling set and punch tracked by ID and station.
Compression cycles logged per set from press data.
Tip, cup depth and working length measured at set intervals and after campaigns.
Inspection results matched with force behaviour in production.
Sets polished, refurbished or replaced on condition, not only on count.
Linking inspection measurements with force data is the powerful step. Over time it shows how force behaviour relates to measured wear for each product and tooling type, so the next set can be pulled at the right moment rather than too early or too late.
Natoli also advises against cleaning presses with compressed air, which can force formulation into bearings and crevices, and against water-based cleaners that can cause rust. Good cleaning practice is part of any tooling program.
Turret, Rollers and Drive: Catching Mechanical Wear
Beyond tooling, the press mechanics wear in ways that force data alone may not reveal early enough.
Vibration sensors on the turret bearing housing and main drive detect bearing wear, gear problems and imbalance weeks before failure. Temperature at bearing housings adds a second signal. Motor current on the main drive shows changing load at the same speed, which can come from mechanical drag, lubrication problems or product changes.
Lubrication deserves its own attention. Many presses have automatic lubrication systems; a blocked line or empty reservoir can damage cams and bearings quickly. Monitoring lubrication cycles and pressures, where the press exposes them, closes that gap.
Mechanical and force data together give a full picture: tooling health per station, and machine health overall. The combined view is standard in our press dashboard.
Reactive Versus Predictive Press Maintenance
The practical change predictive maintenance brings is in when work happens.
- Tooling pulled on a fixed count or when problems appear
- Bearings replaced after failure or on a calendar
- Stops occur mid-campaign
- Quality drift found in IPC results or deviations
- Parts ordered after failure
- Changeover time used for routine tasks
- Tooling pulled when data shows wear
- Bearings replaced when trends show need
- Work moved to changeovers and cleaning windows
- Drift caught before tablets are affected
- Parts ready before the planned window
- Changeover time used for targeted tasks
Because pharma plants already stop presses for cleaning and product changeover, there are regular windows for maintenance. Predictive data tells you which tasks to put in each window, so no extra downtime is needed.
Combining maintenance with planned cleaning windows is one of the quickest ways to recover time. Ask our team how others schedule it.
Tablet Press Monitoring Checklist
Use this checklist to set up predictive maintenance on a tablet press.
Most presses need only a few added sensors because force data already exists. We confirm the sensor list during a short site survey.
Sizing the Value of Press Monitoring
The value of press monitoring comes from three places: fewer unplanned stops, lower tooling cost and fewer quality events. A simple estimate with your own numbers shows which matters most.
Illustrative numbers. Replace them with your own stop log, deviation records and tooling spend.
The tooling line is often the surprise. Without cycle counts and wear data, sets are either retired early, wasting their remaining life, or run too long, causing defects. Natoli’s estimate of more than 40% savings from a structured program shows how much is at stake.
Deviation effort is the hidden cost: each tooling-related deviation takes investigation time from QA and production. Our advisors can help count it.
How iFactory Delivers Tablet Press Predictive Maintenance
Per-station force and ejection trends over weeks.
Turret, roller and drive vibration and current.
Sets, cycles and inspection results linked to force data.
Force trends compared with IPC results and deviations.
Tasks proposed for the next cleaning or product change.
Alerts turned into planned jobs with evidence attached.
It connects to your press controls, MES and CMMS. Share a recent tooling or bearing failure and we will show its early signs in a session.
See Tooling and Bearing Wear Before It Stops a Campaign
Pick one or two presses. We connect force data, add vibration and current sensors and show station-level tooling health and mechanical trends through your next campaigns.
Upper punch force on station 23 is running 6% above the turret average for three days. Pattern matches tip wear.
A Tooling Problem Found Before It Showed in Tablets
This exchange shows how a maintenance planner might use iFactory on a press line.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the tablet press monitoring and tooling analytics models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensors and data connections across tablet press rooms and solid dose suites, PLC/SCADA, MES, LIMS and ERP integration, cabling and network setup, operator and quality team training, and 24×7 remote monitoring.
Server installed, sensors and system links live, historical batch, lab and maintenance records loaded.
Models trained on your own batches and equipment, then run in parallel on one area with your quality and engineering teams reviewing every output.
Rollout to the agreed areas under your change control and validation procedures, team training and 24×7 remote monitoring in place.
Sensors, server, software and integration come as one package. For pricing on your presses, contact our sales team.
Frequently Asked Questions
It uses compression force data, vibration, temperature and motor current to detect tooling wear and mechanical faults early, so maintenance is planned into changeovers instead of forced by breakdowns or quality problems.
When one station’s force drifts away from the turret average or becomes more scattered, its punches or guides are the likely cause. Patterns repeating every revolution point to rollers or cams instead.
Punch tips and dies, punch guides in the turret, pressure rollers, cams and tracks, turret bearings and the main drive and gearbox are the usual sources of problems.
Often only a few. Most presses already record force per station. Vibration and temperature sensors on turret bearings and the main drive, plus drive current, complete the picture.
Tracking cycles and linking inspections to force data lets tooling be refurbished or replaced on condition. Natoli notes that a structured maintenance program can save more than 40% on tooling costs.
A typical rollout takes 6–12 weeks: data links and sensors, then baselines over a few campaigns, then go-live and training. Plan it with our engineers.
Move Press Maintenance Into Your Changeover Windows
iFactory reads force data per station, watches bearings and drives and tracks tooling life, so presses are serviced when they need it and campaigns run without surprises.
Tooling health is scored per station from compression force profiles.