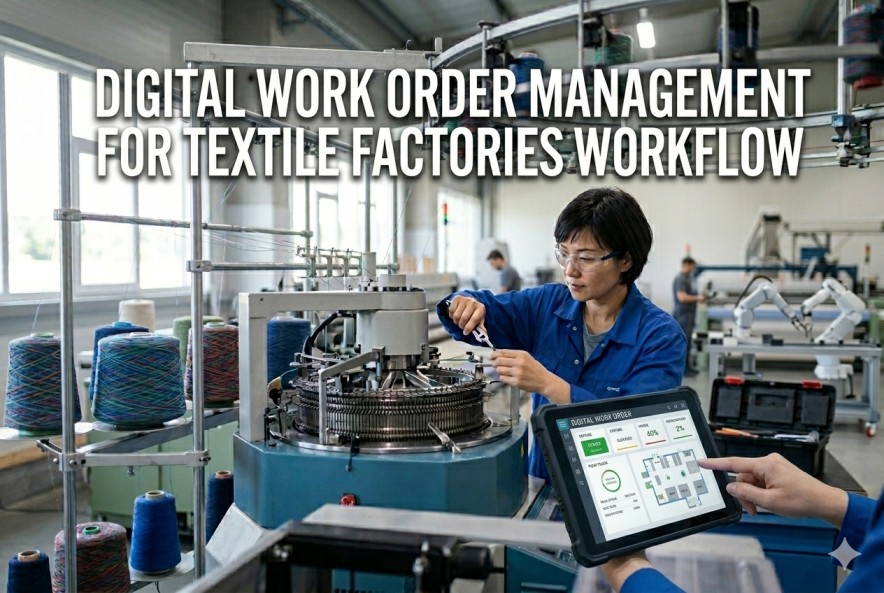
A loom stops. The technician arrives within minutes — response time was never the problem. What happens next is where the real delay lives: fifteen minutes walking to the storeroom because nobody could confirm the reed was in stock, another ten hunting for the correct knotting tool because it was left on a different shed, and five more searching for the setting sheet for this specific loom model because the binder was last seen in someone else's toolbox. The repair itself took twelve minutes. The delay around it took thirty. Book a demo to see how iFactory eliminates the search time hiding inside your MTTR.
Textile → Production Downtime → Delay Reduction
Your Technicians Aren't Slow. They're Searching — for Parts, Tools, and Instructions That Should Already Be There Before They Ever Left the Shop.
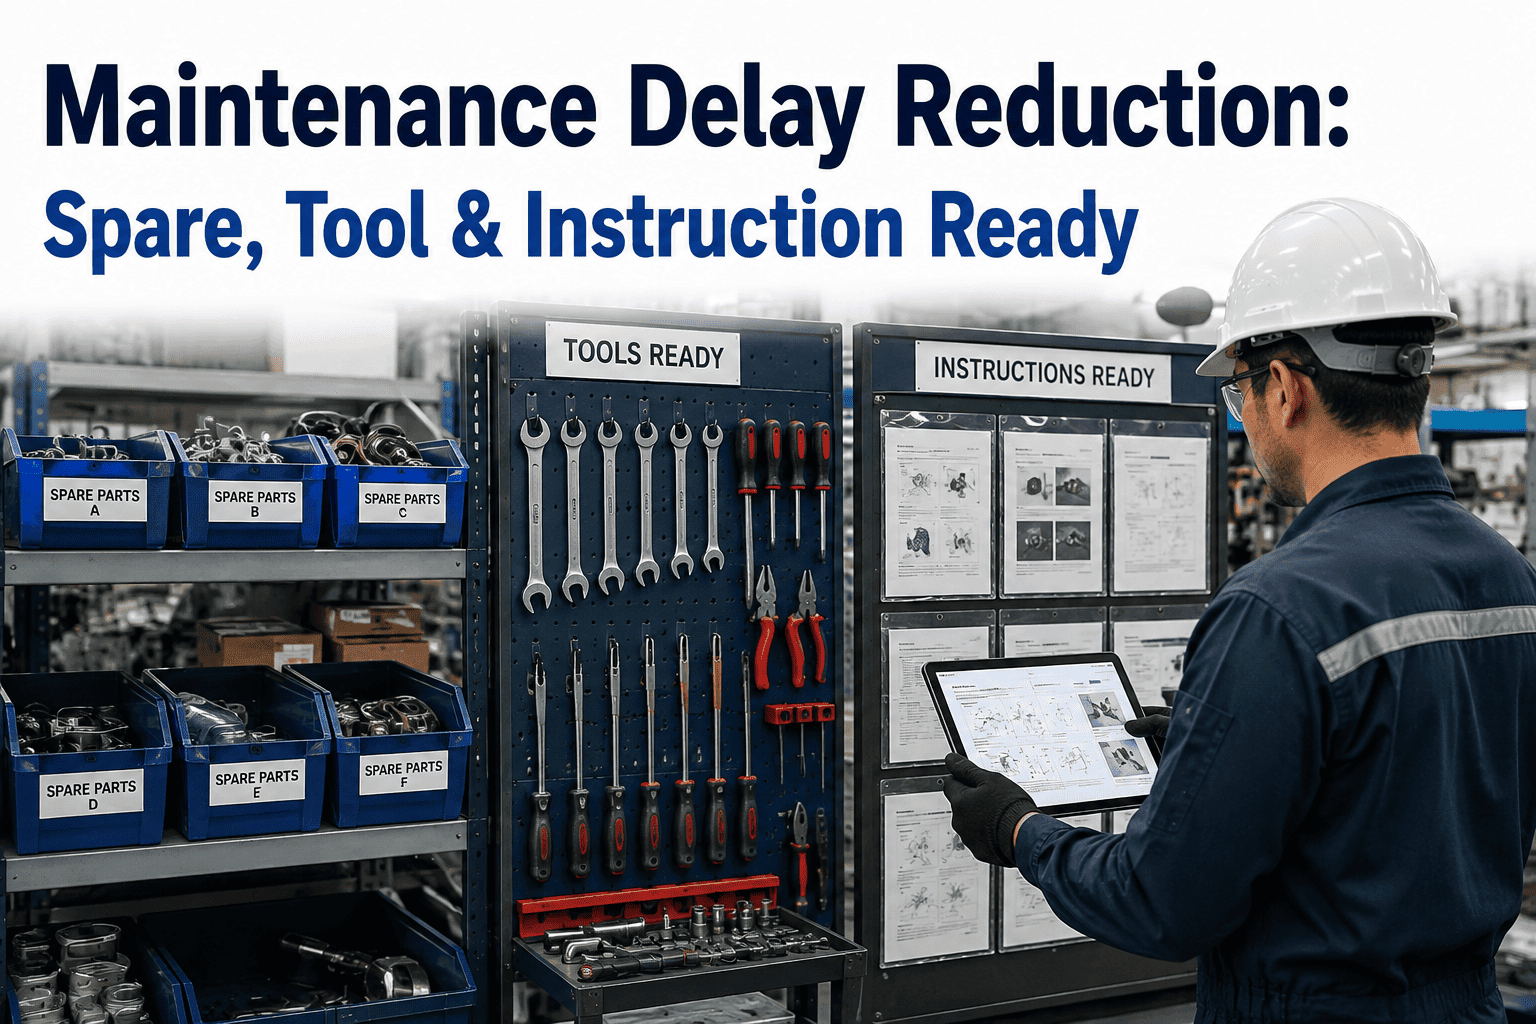
Most textile mills measure MTTR as if it were pure repair time. In reality, a large share of it is delay time: walking, hunting, and waiting for something that a small amount of upfront preparation would have staged before the technician ever left the maintenance shop for the loom.
15-25%
Of total MTTR in spinning and weaving mills is parts-hunting time, not repair time
30-40%
Premium paid on emergency procurement forced by an avoidable stockout
~30%
Wrench time gain typically documented from structured kitting programs
Where the Time Actually Goes
The Anatomy of a Loom Repair That Should Take Fifteen Minutes
Break a typical unplanned loom stoppage into its component phases and the repair itself is usually the shortest one. Everything surrounding it — diagnosis, retrieval, and verification — is where delay accumulates, and almost none of it requires more technical skill to fix. It requires more preparation. This distinction matters because a mill that responds to rising MTTR by hiring more skilled technicians is solving the wrong problem if the actual bottleneck is search time, not repair competence.
Diagnosis
3-8 min
Identifying the fault — a broken reed dent, a worn cam follower, a failed drop wire — often without a documented history of this loom's past failures to speed the process along and point toward the likely cause.
Search & Retrieval
15-40 min
Walking to the storeroom to check part availability, hunting for the correct tool, tracking down the setting sheet or SOP for this specific loom model and style — often across three separate trips rather than one.
Actual Repair
10-20 min
The part of the job the technician was actually trained and equipped to do — and the only phase that meaningfully shrinks with more skilled labor rather than better preparation and staging.
Verification & Restart
5-15 min
Trial picks, tension confirmation, and quality check before the loom is released back to full-speed production — the stage where an incomplete or improperly calibrated repair first becomes visible.
Search and retrieval alone can rival or exceed the repair phase itself. This is not a technician performance problem — it is a readiness gap that exists before the technician ever leaves the shop, and no amount of individual effort or urgency closes it once the walk to the storeroom has already begun.
The Three Readiness Pillars
Spare, Tool, and Instruction Readiness — Solved Independently, Not Together
Most mills that attempt to fix delay time focus on spare parts alone, because stockouts are the most visible failure. Tools and instructions cause the same delay pattern and are addressed far less often, which is exactly why they remain a persistent source of lost wrench time even in mills with a mature parts program — the second and third pillar often go unaddressed for years after the first is finally solved.
Spare Readiness
The Right Part, Confirmed Before the Walk
Reeds, heald frames, travellers, and cam followers classified by criticality and lead time, with stock levels tied to actual consumption against each asset — not a static reorder point set years ago and never revisited. The classification determines shelf strategy, not just reorder timing.
Tool Readiness
The Right Tool, in the Right Place
Specialty knotting tools, gauges, and calibration equipment tracked by location and assigned to specific job types, so a technician does not discover a required tool is on the other shed only after arriving at the loom and beginning diagnosis.
Instruction Readiness
The Right Procedure, on the Technician's Device
Model-specific setting sheets, tension specifications, and repair procedures available digitally at the machine — replacing a paper binder that is inevitably in someone else's hands when it's needed most, or simply out of date relative to the loom's current configuration.
See All Three Readiness Gaps on Your Own Floor
iFactory links spare parts, tools, and digital work instructions to every asset — so a work order arrives with everything the technician needs already confirmed, not discovered mid-repair one trip at a time.
How Readiness Gets Built
The Kitting Workflow: From Planned Job to Ready-to-Execute Package
Readiness is not a single action — it is a sequence that has to happen before a work order is released, not after a technician has already started walking toward the loom. Skipping a step in this sequence is how a mill ends up with an accurate parts list that still results in a delayed repair.
1
Identify
The planner or the CMMS identifies which parts, tools, and instructions a specific job type requires, based on the asset's bill of materials and its documented repair history for similar past failures.
2
Verify
Stock levels, tool location, and instruction currency are confirmed before the job is scheduled — not assumed based on what should theoretically be on the shelf or in the tool crib.
3
Stage
Parts and tools are physically pulled and placed together in a labeled location keyed to the work order, and digital instructions are pushed directly to the assigned technician's device ahead of time.
4
Release
Only once staging is confirmed complete does the scheduler lock in the work order date — preventing the common failure of scheduling a job and discovering a missing part on the morning it was due to start, when it is already too late to react calmly.
The sequencing matters as much as the content. A mill that identifies requirements accurately but skips verification will still discover stockouts mid-repair. A mill that verifies but does not physically stage the kit still leaves the technician walking between the loom and the storeroom multiple times during the job — the delay reduction only fully materializes once all four steps happen in order, every time, without shortcuts under schedule pressure.
Spare Readiness in Practice
Not Every Loom Part Deserves the Same Shelf Space
The single biggest mistake in loom spare parts management is treating every component the same way. A structured classification separates parts by consequence and lead time, not just by how often they fail — because failure frequency alone tells you almost nothing about how much production time is actually at risk.
Tier A — Critical, Always Stocked
Reeds, heald frames, main shaft bearings, and picking mechanism components specific to the loom model. Stops the loom immediately on failure and carries long procurement lead times — the carrying cost of holding a few units is trivial against the downtime cost of not having one, especially when a stockout idles an entire shed section rather than a single machine.
Tier B — Important, Moderate Turnover
Bearings, cam followers, travellers, and apron cords consumed continuously in normal operation. Stocked to a calculated reorder point based on real consumption rate and supplier lead time, reviewed regularly rather than frozen at whatever level was set at initial setup years earlier.
Tier C — Insurance Spares
Dobby drives, main controllers, and other low-frequency, high-consequence components. Low usage rate but held anyway because the alternative — an extended stop waiting on a special order — is unacceptable for the asset's criticality, even if the part sits unused on the shelf for a year or more between installations.
The key indicator for Tier A classification is not how often a part fails, but how much production time is lost if it fails and no replacement is immediately available. A rarely-failing part with a six-week lead time and a full shed shutdown consequence still belongs in Tier A, regardless of how infrequently it actually shows up in a failure log.
Instruction Readiness in Practice
Why "The Setting Sheet Is Somewhere in the Office" Costs More Than It Looks Like
Every loom model and every fabric style carries its own tension specifications, timing settings, and known-issue history. When that information lives in a paper binder, a technician's personal notebook, or a supervisor's memory, the mill is effectively re-deriving the same knowledge every time a different technician handles the same fault — paying the diagnostic cost repeatedly for a problem that has already been solved once before.
Paper-Based Instructions
Setting sheets stored in a binder that travels between shifts and sheds unpredictably, often unavailable exactly when a repair is underway
Tribal knowledge concentrated in senior technicians, lost when they are absent, on leave, or leave the company for good
No link between a repair and the failure history of that specific machine, so every diagnosis starts from scratch
Updates to procedures require physically finding and correcting every printed copy across every shed and shift
Digital Work Instructions
Model and style-specific procedures available instantly on a technician's device at the loom, no walk to the office required
Institutional knowledge captured once and available to every shift, not just senior staff who happen to be on duty
Each repair automatically linked to the asset's full failure and service history for faster diagnosis next time
A single update propagates to every device immediately — no printed copies to chase down or correct manually
What Readiness Looks Like Applied
The Shed That Cut MTTR by Solving the Delay, Not the Repair
A 200-loom weaving shed reviewed six months of unplanned stop data and found that repair time itself had barely moved year over year — technicians were not getting slower. Delay time around the repair was the variable actually driving MTTR, and it had been drifting upward quietly while everyone's attention stayed focused on the machines themselves rather than the process surrounding a repair.
25%
Faster average repair completion after linking spare parts directly to asset records and consumption history
30%
Reduction in unplanned downtime within six months of a structured readiness rollout across all three pillars
58%
Faster repair completion documented in mills with fully linked BOM and kitting data across the whole fleet
40%
Lower parts expenditure once consumption data replaced static, years-old reorder points
None of these gains came from faster technicians or new equipment. They came from making sure the part, the tool, and the procedure were already confirmed and staged before anyone walked toward the loom — a shift in where effort gets spent, not an increase in how much effort gets spent overall.
Common Mistakes
Where Readiness Programs Break Down
01
Solving spares while completely ignoring tools and instructions.
A perfectly stocked storeroom does not help a technician who cannot find the calibration gauge or the correct setting sheet. All three readiness pillars need to close together, or the delay simply relocates to whichever pillar was left unaddressed — a mill that reports its parts program as a success while overall MTTR barely moves is usually looking at exactly this pattern.
02
Setting reorder points once and then never revisiting them again.
A minimum stock level frozen at whatever was set during initial setup cannot see a machine aging into a higher failure rate, a style change altering wear patterns, or a supplier's lead time quietly stretching over time. Reorder points need the same periodic review discipline as any other planning assumption.
03
Treating every part as equally critical across the whole storeroom.
Stocking every SKU at a high safety level ties up working capital in slow-moving parts, while stocking everything lean risks the one true Tier A component that idles an entire shed section when it runs out. Neither extreme is the goal — the classification itself is the deliverable, not just the resulting stock level.
04
Letting institutional knowledge live only in senior technicians' heads.
A mill that depends on one experienced technician to know which setting sheet applies to a specific loom and style has a single point of failure just as real as an unstocked critical part — and considerably harder to notice until that person is unavailable, on leave, or has left the company entirely, at which point the gap becomes visible all at once rather than gradually.
Common Questions
Maintenance Delay Reduction — Frequently Asked Questions
How much of our current MTTR is actually delay time versus repair time?
Most spinning and weaving mills that break down their downtime data carefully find that 15-25% of total MTTR is parts-hunting time alone, before accounting for tool search or instruction retrieval delays on top of that. The only reliable way to know your own figure is to timestamp each phase of a repair separately — diagnosis, search and retrieval, actual repair, and verification — rather than logging a single undifferentiated repair duration that hides where the time actually went. Most mills that run this exercise for the first time are surprised by how small the actual repair phase turns out to be relative to everything surrounding it.
iFactory captures this phase breakdown automatically from work order and technician activity data.
What is the difference between a bill of materials and a kit, and why does it matter for delay reduction?
A bill of materials is simply the list of parts a job requires; a kit is the physical bundle of those parts, tools, and instructions actually pulled, verified, and staged together before the technician begins. Having an accurate BOM without kitting still leaves a technician walking to the storeroom to retrieve each item individually — the delay reduction only materializes once the kit is staged and ready before the work order is released, not merely documented on paper as available somewhere in inventory. This distinction is where many otherwise well-intentioned CMMS rollouts fall short: the data exists, but nobody physically assembled it into something a technician can simply pick up.
Why does tool readiness get overlooked compared to spare parts readiness?
Spare part stockouts are visible and dramatic — a missing reed idles a loom immediately and everyone notices, which creates organizational pressure to fix the parts problem first. Tool unavailability causes the identical delay pattern of walking and searching, but because a shared knotting tool or calibration gauge is usually eventually found somewhere on the floor, the delay it causes rarely gets logged as a distinct problem the way a stockout does — it simply blends into the general noise of "the repair took longer than expected" without a clear root cause attached to it.
Book a demo to see how iFactory tracks tool location and availability alongside spare parts.
How do we classify which spare parts deserve Tier A critical stocking versus lighter coverage?
The determining factor is not failure frequency but consequence: a part that stops the loom immediately on failure and has a long procurement lead time belongs in Tier A regardless of how rarely it actually fails, because the carrying cost of holding a few extra units is trivial compared to an extended, avoidable stoppage that idles an entire shed section. Parts consumed continuously in normal wear — bearings, travellers, cam followers — instead belong in a moderate-turnover tier managed through a calculated reorder point tied to actual consumption rather than a static shelf minimum set once and forgotten.
What does a realistic first step toward readiness look like for a mill that has never formally tracked this?
Start by timestamping the phases of unplanned repairs on a representative subset of looms for two to three weeks — diagnosis, search and retrieval, repair, and verification — to establish where delay is actually concentrated before investing in a full kitting or digital instruction rollout across the entire fleet. Most mills are surprised by which pillar turns out to be the largest contributor, and that data should drive the sequence of the readiness program rather than assuming spare parts are automatically the biggest opportunity simply because stockouts are the most visible symptom.
Book a demo to see this phase breakdown running against your own floor.
Stop Paying for Search Time Nobody Has Ever Actually Measured
iFactory links spare parts, tools, and digital work instructions to every asset in your mill, so technicians arrive at a loom with everything confirmed and staged — not discovered mid-repair, one walk to the storeroom at a time.