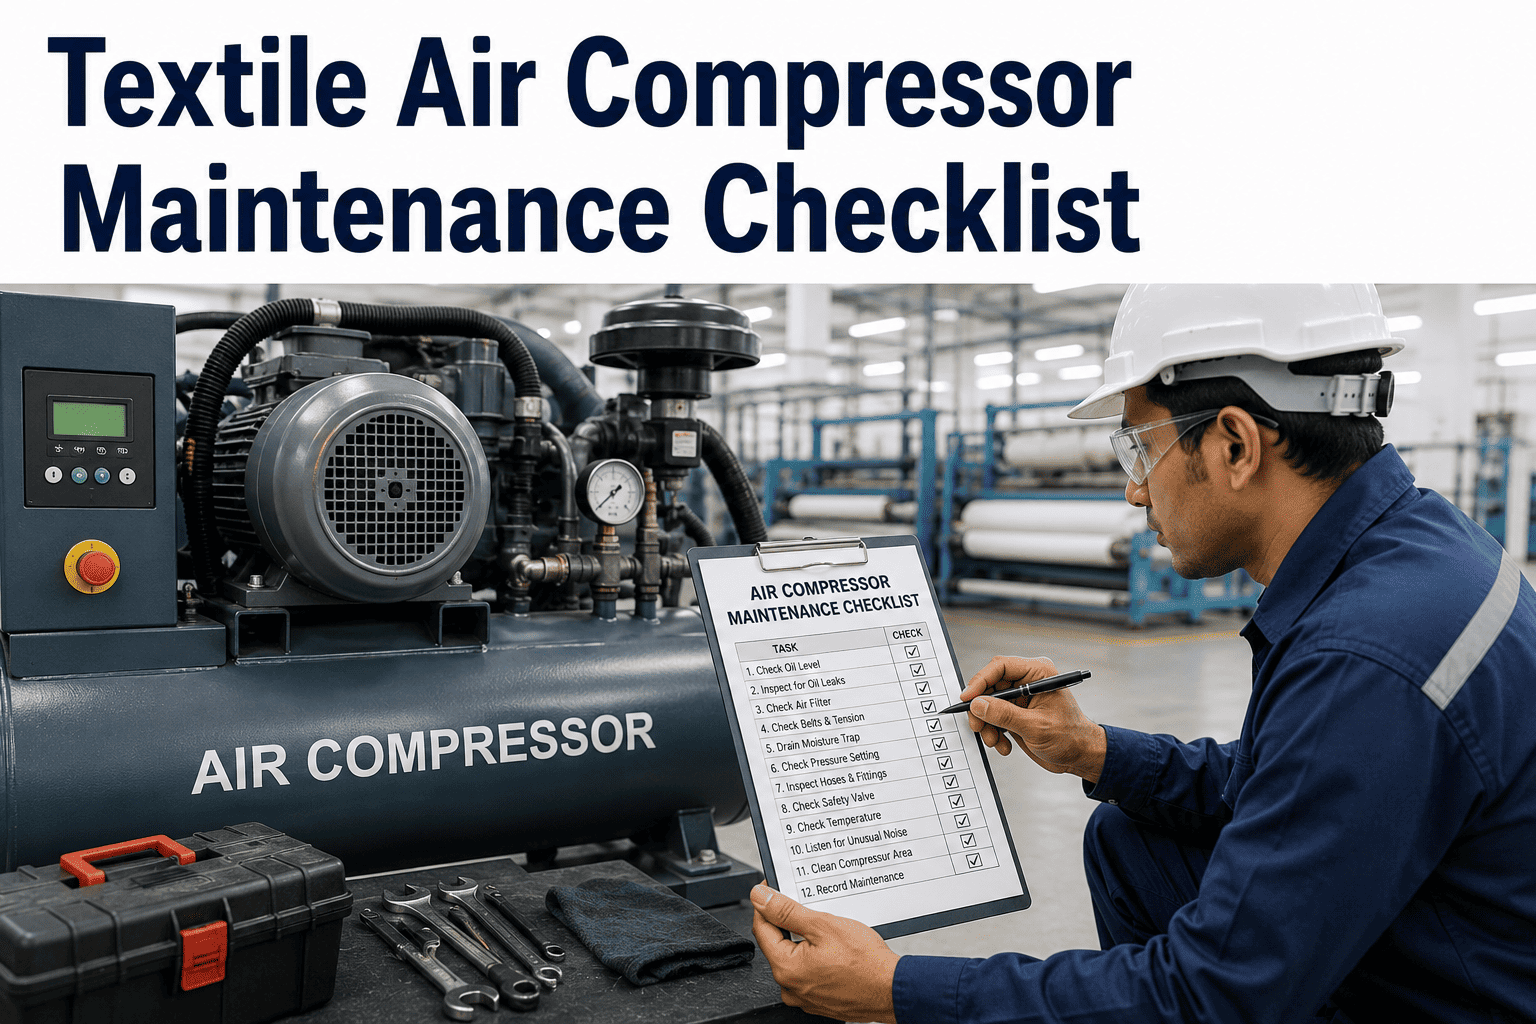
Compressed air maintenance in a textile mill isn't a single job — it's a set of recurring tasks across daily, weekly, monthly, and annual intervals, each targeting a different failure mode. A missed daily drain leads to condensate buildup. A slipped filter replacement schedule adds 5–8% to energy consumption before anyone notices. This checklist covers every interval with the specific checks that prevent the gradual efficiency losses that rarely announce themselves. iFactory monitors compressor performance continuously between manual checks — connect with iFactory support to see how automated alerting fits alongside your existing maintenance routine.
Textile Maintenance · Compressed Air Systems
Compressed Air Maintenance Checklist for Textile Mills
Daily through annual — every check your compressor room needs to avoid the efficiency losses that accumulate quietly and get blamed on everything else.
25–30%
Energy lost to air leaks in unmanaged systems
4 Tiers
Daily / Weekly / Monthly / Annual checks
5 Modes
Common failure points this checklist prevents
22%
Energy increase caught by continuous monitoring
How to Use This Checklist
Four Maintenance Intervals, Each Targeting a Different Failure Mode
Daily
Catches acute failures — pressure deviations, leaks, condensate overflow — before a shift ends in a stoppage.
Weekly
Catches early-stage degradation — rising filter differential, belt wear, dew point drift — while repair is still routine.
Monthly
Addresses consumables and slow-moving wear — oil condition, intake filters, cooling system — on a schedule that prevents compounding.
Annual
Full overhaul tasks — oil change, filter replacement regardless of condition, safety valve verification — that can't be deferred.
What These Checks Prevent
Five Common Failure Modes and Which Checklist Interval Catches Each One
| Failure Mode |
How It Hides |
Interval That Catches It |
If Missed |
| Air/oil separator degradation |
Compressor runs normally; oil appears in downstream tools |
Monthly (scavenge line + diff pressure) |
Oil contamination of loom pneumatics, textile web breaks |
| Dryer refrigerant loss |
Dew point rises gradually over weeks — rarely trips an alarm |
Weekly (dew point reading) |
Moisture in air line, corrosion in distribution, freeze-related pneumatic failures |
| Intake filter clogging |
Energy consumption rises; delivered pressure appears normal |
Monthly (intake filter inspection) |
5–8% energy waste; fine fiber entering compression stage |
| Belt slippage |
Compressor runs, no alarms, but delivered airflow drops |
Weekly (tension + visual check) |
Pressure shortfall at loom headers, unexplained weft stop events |
| Condensate drain valve failure |
Stuck closed: water builds silently. Stuck open: continuous air loss. |
Daily (drain verification) |
Receiver water damage, distribution corrosion, or continuous unnoticed air loss |
Manual Checks Cover the Intervals. Continuous Monitoring Covers Everything in Between.
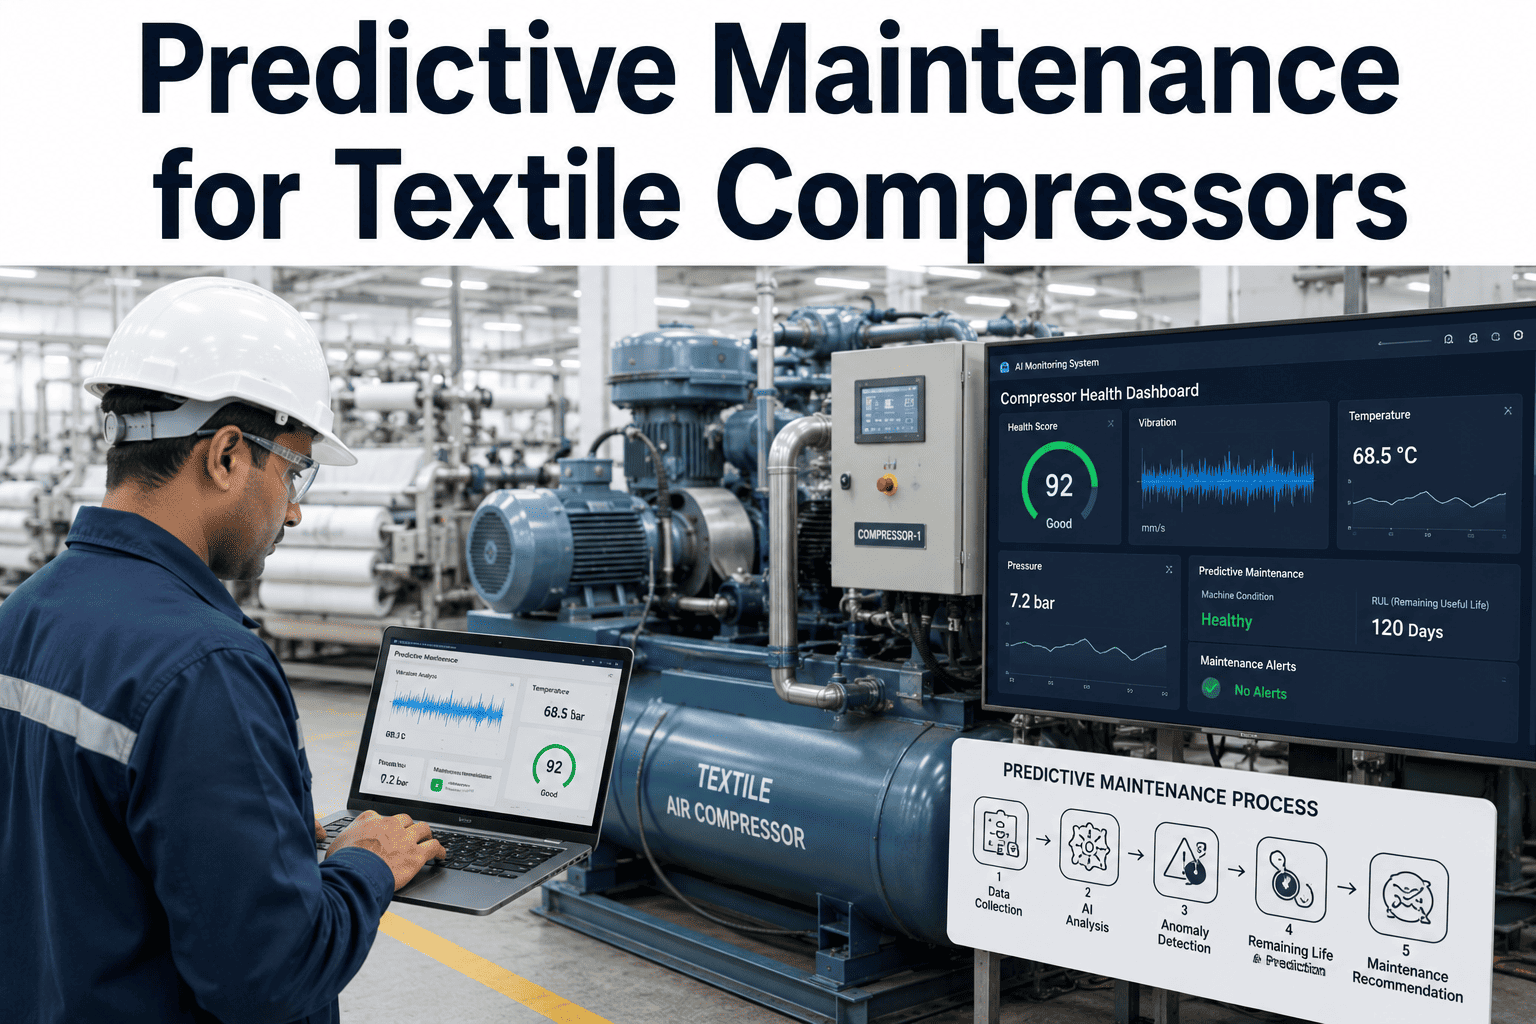
iFactory tracks compressor efficiency, filter differential, dryer dew point, and off-shift loading patterns automatically — alerting your team to degradation that a weekly walk-through would miss.
Energy Loss Reference
Efficiency Losses This Checklist Targets — and Typical Recovery Potential
25–30%
Compressed Air Leaks
Caught by: Daily visual + Weekly off-shift check + Annual torque pass
8–12%
Excess Pressure Setting
Caught by: Daily pressure check against actual demand profile
5–8%
Filter Pressure Drop
Caught by: Weekly differential pressure read + Monthly intake inspection
3–6%
Poor Heat Recovery
Caught by: Annual efficiency review with waste heat utilization assessment
Frequently Asked Questions
Using This Checklist — Common Questions
How does iFactory complement a manual checklist like this?
The checklist covers scheduled inspection intervals — what your team checks on a daily, weekly, monthly, and annual basis. iFactory fills the time between those checks with continuous monitoring: compressor loading patterns, filter differential trends, dryer dew point, and energy consumption per unit of delivered air. The two work together — the checklist confirms condition at inspection; continuous monitoring flags degradation between inspections.
Book a Demo to see what the monitoring layer looks like alongside your existing maintenance program.
Which checklist interval has the highest impact on energy cost?
In textile mills specifically, the weekly off-shift leak check and monthly intake filter inspection typically have the largest impact on energy cost. Leak buildup and clogged intake filters together account for the majority of recoverable compressed air energy waste — and both are gradual enough that they rarely trigger a reactive response before they're significant.
Contact support to discuss how to baseline your current compressed air specific energy before starting improvement work.
Do we need different check intervals for older compressors?
Generally yes — older units with higher running hours may need oil condition checks monthly rather than relying solely on the annual change interval, and intake filter inspection may need to move from monthly to bi-weekly if historical data shows high loading rates. The intervals in this checklist are appropriate baselines; actual intervals should be adjusted based on the trend data your team collects over the first few months of consistent logging.
Is there a recommended format for logging checklist results?
A paper logbook works, but it makes trending difficult — you can't easily graph differential pressure readings from a handwritten log to spot a filter loading faster than expected. A simple spreadsheet that captures date, technician, and numeric readings for the key parameters allows basic trending. For full trending and alert capability, iFactory integrates checklist findings with continuous monitoring data so the picture is complete in one place.
How quickly can we see results from implementing this checklist consistently?
Mills that transition from reactive to scheduled compressed air maintenance typically see energy improvements within two to three months as accumulated leak points are addressed and overdue filters are replaced. The compressor case study on this page — a 22% specific energy increase caught and corrected in two months — is representative of what consistent monitoring and scheduled maintenance can recover.
Book a Demo to discuss a baseline assessment for your site.
This Checklist Covers the Intervals. iFactory Covers Everything in Between.
Get continuous compressor efficiency monitoring alongside your manual inspection program — so degradation is caught as a maintenance task, not a production stoppage.