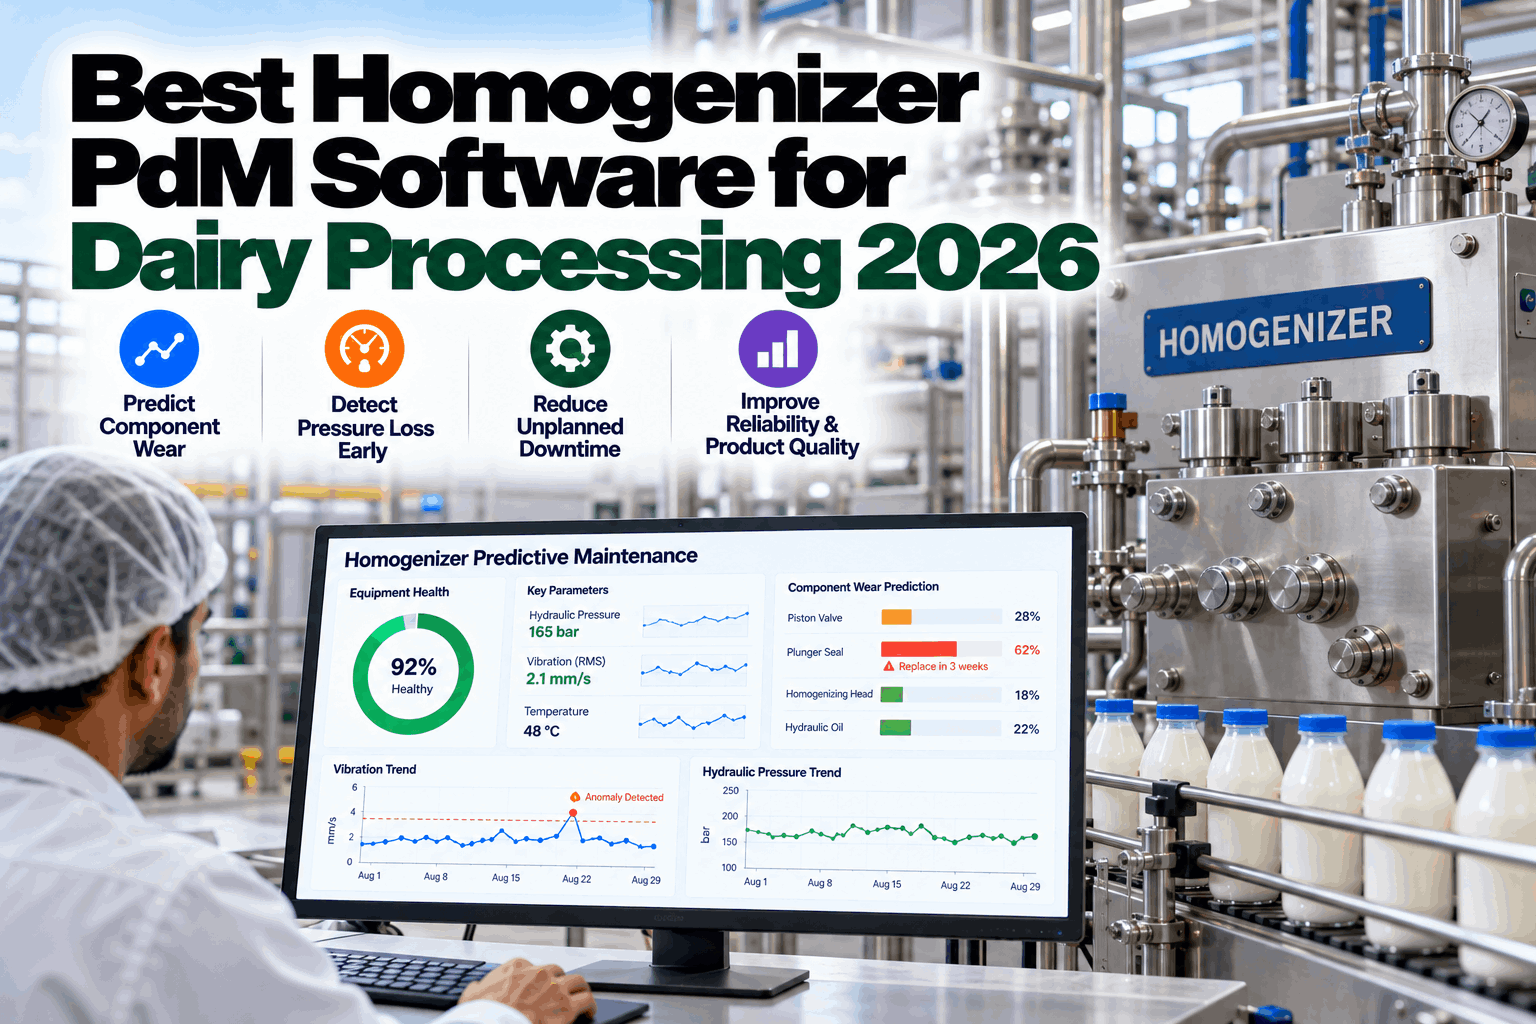
A homogenizer rarely fails without warning. It drifts. The homogenizing valve and seat wear, a plunger seal starts to weep, a suction valve on one cylinder stops closing cleanly, and the machine still holds pressure, just less efficiently, until the day it cannot. By then the line is down, product is on hold and the maintenance team is rebuilding a pump block under pressure. Predictive maintenance for dairy homogenizers catches that drift weeks earlier by reading the pressure pulsation, hydraulic effort, vibration and temperature signatures the machine already produces. This guide shows which failure modes matter, which signals reveal them and how to turn early alerts into planned rebuilds. If you want to see it on your own equipment, book a live demo.
Homogenizer Predictive Maintenance: Catch Valve Wear, Seal Drift and Pressure Loss Before a Batch Is Lost
Per-cylinder pressure signatures, hydraulic effort and bearing health tracked on every run, so rebuilds happen on your schedule, not the machine’s.
Why Homogenizer Failures Hit Dairy Lines So Hard
In most dairy plants the homogenizer sits in series between standardization and pasteurization or filling. There is usually no bypass and no spare. When it stops, the whole line stops, product in the balance tank waits, and depending on where the stop happens, product may need to be reprocessed or diverted. A homogenizer is also a high-energy machine: the Tetra Pak Dairy Processing Handbook uses the example of 68 kW for 10,000 litres per hour at 200 bar. It is built around a positive-displacement piston pump with three to five pistons, driving product through a homogenizing gap of roughly 0.1 mm between seat and forcer.
That combination of high pressure, tight clearances and continuous duty is exactly what wears parts quickly. Most plants manage it with calendar rebuilds: swap seals and valves every so many hours whether they need it or not. That works until a component wears faster than the calendar, because of an abrasive product, a CIP chemistry change or a pressure increase for a new recipe. Plants that want to test a condition-based approach on one machine can start with a short pilot plan.
Anatomy of Wear: Where Homogenizer Failures Start
A homogenizer has two halves that fail differently. The pump end, meaning plungers, seals and suction and discharge valves, wears with every stroke and shows up as pressure pulsation changes. The homogenizing device, the seat, forcer and impact ring, wears with pressure and product abrasiveness and shows up as more effort to hold the same pressure and poorer homogenization. The power end, crankshaft, connecting rods, bearings and lubrication, fails slowly and shows up in vibration and oil temperature.
| Component | Failure mode | What changes first | Best data source |
|---|---|---|---|
| Homogenizing valve, seat, forcer | Erosion and wear of the gap surfaces | Hydraulic or actuator effort to hold setpoint rises; efficiency drifts | Hydraulic pressure, actuator position, lab efficiency tests |
| Second-stage valve | Wear, sticking, incorrect setting | Second-stage pressure unstable or off target | Second-stage pressure transmitter |
| Plunger seals | Wear, scoring, dry running | Leakage at the seal flush; suction pulsation | Seal-flush flow or temperature, suction pressure |
| Suction and discharge valves | Seat wear, spring fatigue, debris | Pressure pulse on one cylinder loses symmetry | High-rate discharge pressure synced to crank angle |
| Crankshaft and bearings | Fatigue, lubrication breakdown | Vibration at bearing frequencies; oil temperature rise | Accelerometers, oil temperature |
| Drive train and motor | Belt or gearbox wear, motor faults | Current signature and load changes | Motor current, vibration |
| Hydraulic unit | Leaks, pump wear, valve drift | Pressure drifts from setpoint or cycles more often | Hydraulic pressure and pump run time |
Most homogenizers already expose several of these signals through their PLC. The rest can usually be added with a pressure transmitter, a pair of accelerometers and a temperature sensor, which our engineers scope during the first site review.
The Signals That Give Weeks of Warning
Per-cylinder pressure pulsation
Every piston stroke produces a pressure pulse at the discharge. On a healthy three-piston machine the pulses are nearly identical. When a suction or discharge valve on one cylinder starts to leak, or a plunger seal lets product bypass, that cylinder’s pulse changes shape and amplitude. Sampling discharge pressure fast enough and aligning it to crank angle shows which cylinder is drifting, long before the average pressure changes.
Effort to hold homogenizing pressure
As the seat and forcer wear, the hydraulic or pneumatic actuator has to work harder to hold the same homogenizing pressure. A slow upward trend in actuator pressure, normalized for product, flow rate and temperature, is one of the clearest wear signals available.
Temperature rise as a cross-check
The Dairy Processing Handbook notes that product temperature rises by roughly 1°C for every 40 bar of pressure drop across the homogenizing device. Comparing measured temperature rise with expected rise gives an independent check on pressure transmitters and on how much energy is going into homogenization. The analytics logic behind all three signals is something we walk through in a technical session.
Homogenization Efficiency Is a Maintenance Signal Too
A worn homogenizing device can still reach its pressure setpoint while doing a worse job. The fat globules are not broken down as finely, and the product creams faster on the shelf. Plants measure this with creaming tests and particle size analysis. The Dairy Processing Handbook cites typical homogenization efficiency of 60–70% for pasteurized milk using the NIZO creaming method, and laser diffraction to measure particle size distribution.
Most plants store these lab results in a LIMS that maintenance never sees. Connecting them to the machine’s condition data changes that. When efficiency results drift in the same weeks that actuator effort climbs, the diagnosis is no longer a guess, and the rebuild can be scheduled before a customer notices a cream line.
If your lab data lives in a separate system, ask our team how the LIMS link works in practice.
Calendar Rebuilds Versus Condition-Based Rebuilds
- Seals and valves replaced every fixed number of hours
- Good parts thrown away; fast-wearing parts fail early
- Recipe or pressure changes are not reflected in intervals
- Failures between rebuilds cause unplanned stops
- Little evidence of which cylinder or part actually wore
- Rebuilds triggered by measured drift per cylinder and valve
- Parts replaced when the data says they are worn
- Intervals adapt automatically to product and pressure
- Warnings arrive weeks ahead, inside planned windows
- Every rebuild records which signal predicted it
The economics follow a well-established pattern. The U.S. Department of Energy’s O&M Best Practices Guide, prepared by PNNL, puts savings from predictive maintenance at 8–12% over preventive programs and more than 30–40% over reactive maintenance. On a homogenizer, most of that comes from fewer unplanned stops and from not replacing parts that still had life in them. Your own numbers can be estimated with our support team.
From Early Alert to Planned Rebuild
A per-cylinder pulse change, rising actuator effort or bearing vibration trend crosses its learned band for long enough to count.
The alert names the likely component and cylinder, with the signals that support it and how fast it is progressing.
Parts are checked against stock, and the rebuild is proposed for the next CIP or changeover window rather than mid-run.
Technicians receive a work order with the cylinder, part list and the evidence attached.
After the rebuild, pulse symmetry and actuator effort return to baseline, and the alert closes with a record of what was found.
Each step can be tested on your own machine data in a guided demo.
How iFactory Solves Homogenizer Reliability
High-rate discharge pressure aligned to crank angle to isolate valve and seal faults.
Homogenizing pressure effort normalized for product, flow and temperature.
Vibration and oil temperature models for bearings, crankshaft and drive.
Lab efficiency and particle size results on the same timeline as machine signals.
Alerts converted into CMMS work orders with parts and evidence attached.
Post-rebuild baselines confirm the fix and refine future predictions.
The same models run on multiple homogenizers across plants, so learning from one machine improves predictions on the rest. See it on your fleet with a quick call.
See Early Warnings on Your Own Homogenizer
Share a few weeks of pressure, hydraulic and vibration data, or let us install temporary sensors. We show which cylinder, valve or seal is drifting and when it needs attention.
Discharge pulse has lost symmetry over nine days. The pattern matches discharge valve seat wear, not a seal.
How Deployment Works
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the homogenizer models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensor and PLC/SCADA integration, cabling and network setup, operator and technician training, and 24×7 remote monitoring.
Server installed, sensors and controllers connected, historical work orders and failure history loaded.
Baselines learned per asset, alerts piloted on the first line with your maintenance team reviewing every finding.
Rollout to the agreed assets, technician training, CMMS hand-off and 24×7 remote monitoring in place.
Most dairy plants start with the homogenizer that has caused the most unplanned stops in the last year, then extend to separators, pumps and fillers on the same line once the first alerts have proven themselves. The rollout plan can be discussed on a scoping call.
What One Avoided Failure Is Worth
Downtime costs vary by plant, but the benchmarks are sobering. Siemens’ True Cost of Downtime 2024 report puts the cost of a lost hour in fast-moving consumer goods at about $36,000, and says an average large plant still loses 27 hours a month to unplanned downtime.
Most plants find that preventing a single unplanned homogenizer stop pays for monitoring the machine for years. Our specialists can build the case with your own line value and failure history.
Frequently Asked Questions
Discharge pressure pulsation per cylinder, homogenizing actuator effort, second-stage pressure, seal-flush condition, vibration and oil temperature on the power end, and motor current. Together they cover the pump end, the homogenizing device and the drive. See how it works on a short call.
Pump-end faults typically appear in the per-cylinder pressure pulse days to weeks before they affect average pressure or cause visible leakage. Warning time depends on the fault and operating conditions. Our engineers can review your history.
Yes. A worn homogenizing device can reach setpoint with more actuator effort while efficiency drops. Linking lab creaming or particle size results with machine data exposes this. Ask about the lab link.
Often only a few. Many machines already expose pressure and hydraulic data through the PLC. A fast-sampling discharge pressure transmitter and accelerometers on the power end are the most common additions. Get a sensor plan.
Alerts become work orders in your existing CMMS with the component, cylinder, parts and evidence attached, and rebuild results are recorded back against the alert. We can show you.
Typical programs go live in 6–12 weeks: server and data connection in weeks one to four, model training and pilot in weeks five to eight, and rollout with training in weeks nine to twelve. Talk to our team.
Rebuild Homogenizers When the Data Says So
iFactory reads per-cylinder pressure, actuator effort and bearing health on every run, then hands your team a dated, planned rebuild instead of a mid-shift breakdown.
Scores combine pressure pulse, actuator effort and vibration trends per component.