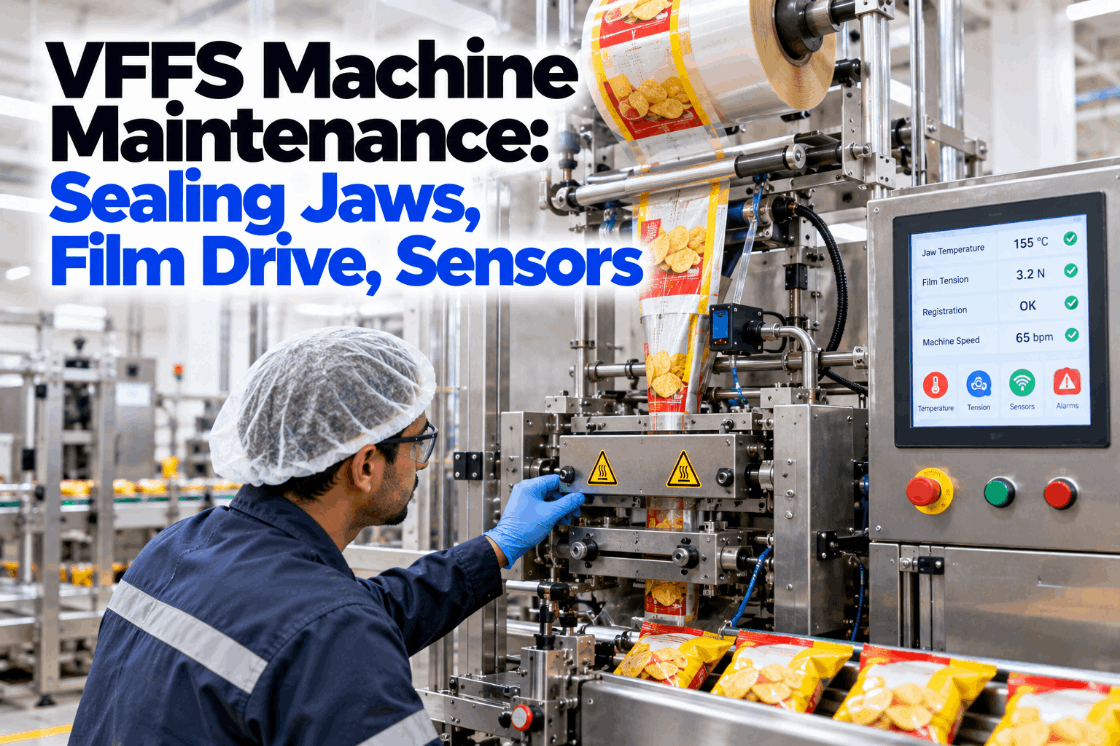
A vertical form fill seal bagger rarely fails all at once. A jaw face picks up product, a pull belt glazes, the dancer starts to hunt, and a registration sensor misreads a mark now and then. Each change is small, but together they show up as leaking bags, short bags and film breaks that get blamed on the film or the operator. VFFS machine maintenance works best when every seal failure and film break is tied back to the wear point that caused it. See how iFactory trends jaw temperature and film tension on a real bagger in a short VFFS maintenance demo.
Tie Every Leaking Bag and Film Break to the Part That Wore
iFactory trends jaw temperature, film tension and pull belt signals on each bagger, links seal leaks to the jaw or belt behind them, and lets crews log jaw cleanings by voice during changeovers.
Six Places a Vertical Form Fill Seal Machine Wears
A VFFS machine unwinds flat film, forms it into a tube around a collar, pulls it down with belts, seals the back seam, then closes cross jaws to seal and cut each bag while product falls through the tube. Every one of those steps has parts that wear, and each wear point leaves a different fingerprint on the bags. Packaging Digest notes that inconsistent film tension is a major cause of problems on VFFS baggers, which is why the film path deserves as much attention as the jaws. Map the wear points on your own baggers with our packaging team.
Temperature, Pressure and Dwell Time Work as a Set
A heat seal needs three things at once: enough heat at the sealant layer, enough pressure across the full jaw face, and enough dwell time for the layers to fuse. Change one and the other two have to move with it. That is why a jaw that reads the right temperature can still make weak seals. The controller reads one point in the jaw body, while a worn face, a weak air cylinder or a faster line speed changes what the film actually sees. Review your seal settings with our seal process specialists.
Packaging Strategies warns that a strong seal does not necessarily mean seal integrity. Channels and voids can leak even when a seal passes a strength check, so test for leaks as well as strength.
Each Jaw Type Wears in Its Own Way
Most baggers use constant heat jaws, held at sealing temperature all the time. Impulse jaws heat a thin element for a short time and then hold the film under pressure while it cools, which suits many polyethylene films. Ultrasonic jaws use high-frequency vibration rather than heated faces, and vendors such as Dukane say they can seal through product residue. These are vendor claims, so test them on your own product. Your PM list should match the jaw type you actually run. Ask our support team to help build it.
What Usually Sits Behind Each Problem
Seal failures and film breaks look like random events on a shift report. Equipment makers' troubleshooting guides tell a more useful story: most causes trace to a short list of setup and wear points. Rovema's guide, for example, links forming tube jams to a vertical seal that runs too hot, and inconsistent bag length to dirty feed belts. Use these lists as a starting point and confirm against your own failure records. Walk through your top failures in a bagger review session.
- Product in the cross seal, often from filler and jaw timing being out of step
- Buildup or scoring on the jaw faces
- Jaws out of parallel, so pressure is uneven across the seal
- Low jaw air pressure
- Heater or thermocouple faults causing temperature drift
- Film creased or wrinkled as it enters the jaws
- Uneven tension from an off-centre roll or a sticking dancer
- Guide rollers not turning freely
- Splice tape caught in the forming collar
- Dirty forming set or high film friction adding drag
- Pull belts set too tight against the tube
- Film sticking to an overheated vertical seal bar
Ask the Bagger What Changed
iFactory watches jaw temperature, film tension and pull belt signals together, so a rise in leakers points to the part most likely behind it. Crews log jaw cleanings by voice at changeover, and that record sits next to the trend.
Signals Worth Trending on Every Bagger
Pull belts set the bag length, and the registration sensor corrects it each cycle by reading the eye mark. When belts glaze or vacuum weakens, film slips and the sensor has to correct more often. Short bags, long bags and misplaced print are often the first sign. Rovema lists clogged vacuum filters and hoses, dirty or worn belts and low belt pressure as causes of slipping, and notes that a misaligned registration eye can add length to every bag. The signals below show wear before it becomes a stop. Check which ones your controls already record with our integration team.
Bubble and Burst Tests That Confirm a Seal Fix
After a jaw repair or a settings change, a test proves the fix. Two ASTM methods are widely referenced. ASTM F2096 detects gross leaks by inflating a package underwater and watching for bubbles. It was written for medical tray and pouch packaging, and its stated sensitivity was not evaluated for nonporous films, so validate it on your own bags. ASTM F1140 pressurizes unrestrained packages, either to burst or held at a set pressure for a set time (creep). Plan a test routine with our quality specialists.
A burst that starts at the same end of the cross seal every time points to jaw parallelism or one worn face. Log the location with each test so it can be matched to the jaw.
A Changeover Jaw Cleaning Record Crews Can Speak
Viking Masek's daily routine is a good base: check the jaws for dirt, remove the knife before cleaning the faces, wear heat-resistant gloves, and lock out energy before any work. What most plants lose is the record. A voice entry at each changeover captures the condition of each face so the trend has context. Ask our support team for a blank record.
Seal Leaks Grouped by the Wear Point Behind Them
Once each leak or break is tagged with the signal that moved before it, a weekly view shows where the maintenance effort should go. The breakdown below is an illustration of the format, not data from a real plant. See the same view built from your bagger signals in a live walkthrough.
Five Steps From First Signal to Planned Jaw Work
Start with one bagger that causes the most leakers or breaks, prove the links, then spread the setup across the line. Most of the data already exists in the bagger controls. Plan your first bagger with our implementation team.
Size the Value With Your Own Numbers
The value comes from fewer seal-related stoppages and fewer leaking bags reaching the case. Every input below is an assumption made to show the arithmetic only. Put in your own figures before drawing any conclusion. Our team can build the case with your line data.
Add film saved from fewer breaks and rethreads, and fewer customer complaints about leaking bags, only where your own records support them.
Bagger Analytics and AI Server, Ready to Rack
iFactory ships as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready, with the predictive models and micro-stop mining loaded, and connects to your bagger controls on the plant network. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your packaging lines, ask our deployment team.
- Pre-configured NVIDIA AI server, racked and ready
- Connectors for bagger PLCs and seal controllers
- Jaw temperature and film tension trend models
- Micro-stop mining linked to seal leak tests
- Voice logging for jaw cleanings at changeover
- Work orders raised into planned stops
- 24×7 remote monitoring of models and hardware
Baggers connected, signals mapped, normal patterns learned for each film.
Leak tests and breaks tagged to signals, alerts checked by maintenance.
Alerts switched on, voice logging rolled out, planners trained.
VFFS Machine Maintenance Software Focused on Wear Points
iFactory is built for packaging lines where seal quality, uptime and changeover speed all matter at once. Our specialists can show it on your own baggers.
What Plant Managers Ask About VFFS Machine Maintenance
Fix the Jaw Before the Leakers Start
Trend jaw temperature and film tension, link every seal leak to a wear point, and keep jaw cleanings on record by voice. The full system is delivered turnkey and goes live in 6 to 12 weeks.