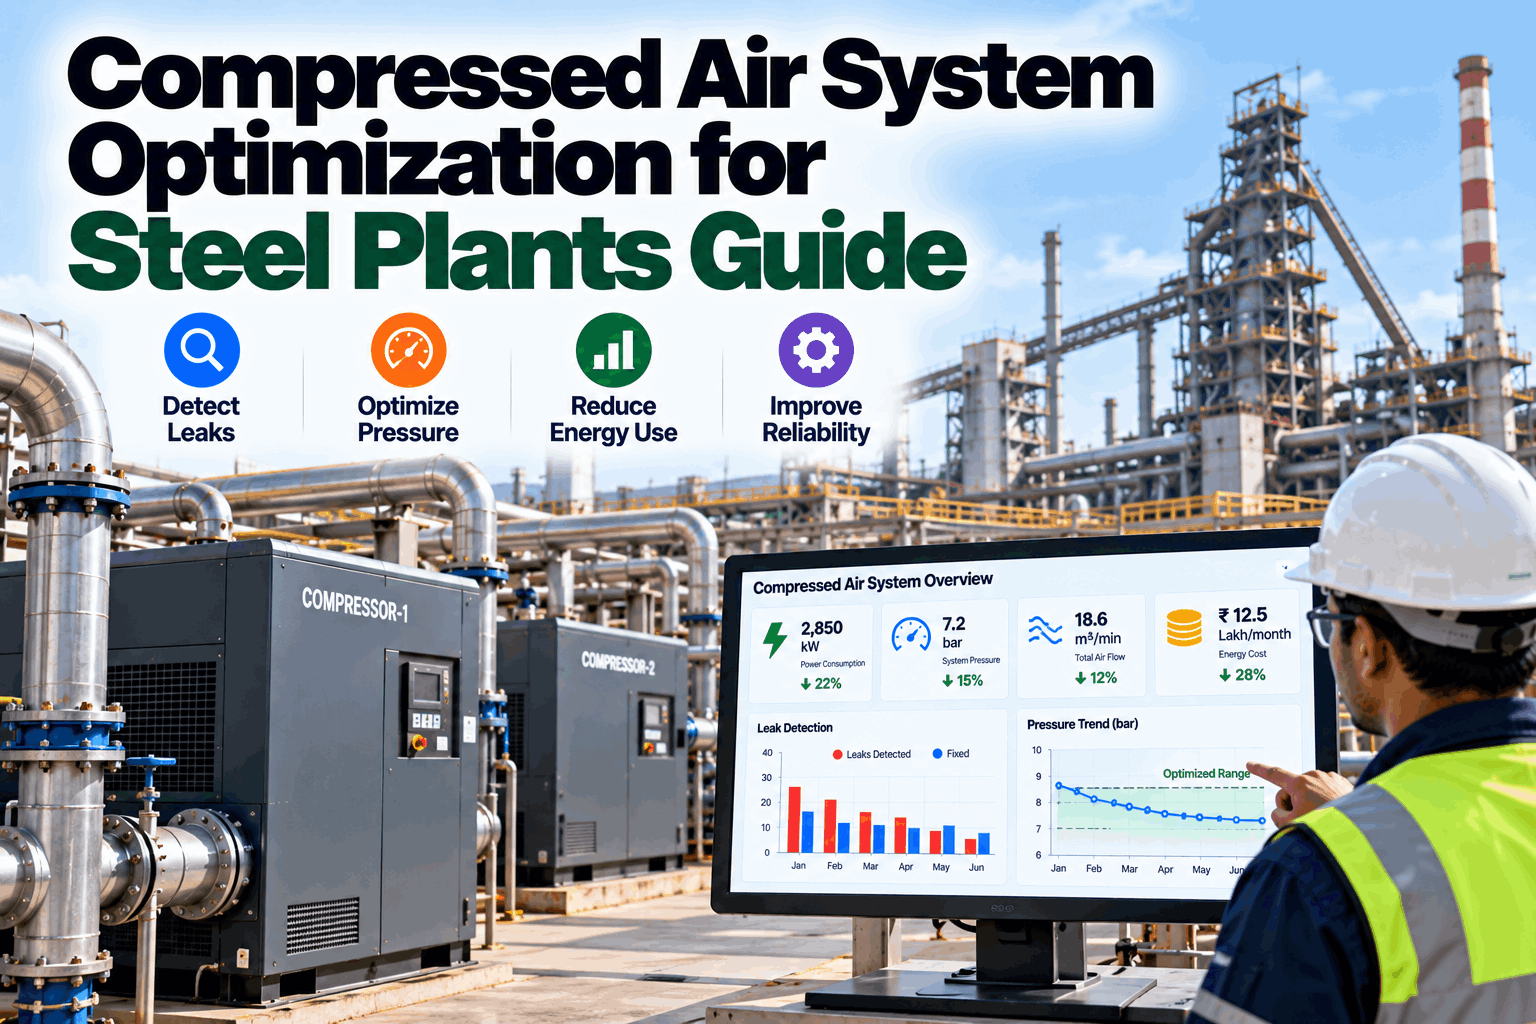
Compressed air keeps a steel plant moving, driving actuators on furnace doors, instrument air on control valves, bag filter cleaning and blow-off across the mills. It is also one of the least efficient ways to use electricity, and most of its waste is invisible: leaks in hot, noisy areas, headers run at higher pressure than anyone needs, and open blow-off pipes that nobody questions. This guide covers the three levers of leak detection, pressure reduction and demand-side management that together can recover 20–35% of compressed air energy, and how to keep the savings from drifting back. Book a 30-minute compressed air review using your plant’s own data.
Leaks, pressure and demand-side waste, measured continuously and fixed in the right order, so savings stay recovered.
At a Glance
Why Compressed Air Is a Steel Plant’s Most Expensive Utility
Steel plants run on compressed air in places most people never see: pneumatic actuators on furnace doors and mill guides, instrument air for control valves, pulse-jet cleaning of bag filters, blow-off and scale cleaning, conveying and cooling. The U.S. Department of Energy’s compressed air sourcebook notes that in many industrial facilities, air compressors use more electricity than any other type of equipment, and that the typical system delivers only around 10% of its input energy as useful work.
Because the waste is invisible and spread across hundreds of connections, compressed air rarely gets the attention its cost deserves. The good news is that the fixes are mostly low-capex and quick to pay back.
Where the Air Goes
| Category | What it looks like in a steel plant | Main lever |
|---|---|---|
| Productive demand | Actuators, instrument air, filter cleaning and process uses that genuinely need air | Keep, but supply at the lowest pressure that works |
| Leaks | Fittings, hoses, filter-regulator-lubricators, quick couplings and condensate drains stuck open, often in hot, dusty areas | Find, tag and repair; measure the leak rate regularly |
| Artificial demand | Extra flow consumed because the header runs at higher pressure than users need | Lower header pressure; fix pressure drop; boost locally |
| Inappropriate uses | Open blow-off pipes, cabinet cooling, personnel cooling, air-driven sumps and sparging | Replace with engineered nozzles, blowers or electric alternatives |
| Idle areas under pressure | Lines to mills or bays that are down but still pressurized | Isolation valves interlocked with production status |
Lever 1: Find and Fix Leaks
Leak programs fail when they are treated as an annual survey. Leaks come back, especially where vibration, heat and scale are part of daily life. A durable program combines three things: a way to size total leakage, a way to locate individual leaks, and a way to track repairs.
Measure compressor power and flow during a planned stop, when demand should be close to zero. What remains is mostly leakage.
Acoustic leak detectors pinpoint individual leaks in noisy areas; each leak is tagged with size and location.
Tagged leaks become work orders, and the next base-load test confirms the leak rate actually fell.
The cost adds up quickly. The Compressed Air Challenge estimates that a single quarter-inch leak costs about $8,400 a year at $0.05 per kWh. At today’s industrial tariffs the figure is often double that, and a large plant can have hundreds of leaks.
Lever 2: Bring Pressure Down
Header pressure is often set by habit: high enough that nobody complains, never revisited. The DOE sourcebook’s rule of thumb is that every 2 psi increase in discharge pressure raises compressor energy by about 1%. Lower pressure also reduces the flow through every leak and every unregulated user.
Measure pressure at the most demanding users under peak load; that, plus a margin, sets the header.
Clogged filters, undersized dryers and long, narrow piping force the compressor room to overcompensate.
If one or two users need high pressure, a local booster is cheaper than running the whole plant high.
Sequence compressors with a master controller and a trim machine with variable speed, so pressure bands stay narrow.
Lever 3: Manage the Demand Side
Once leaks and pressure are under control, the remaining waste sits in how air is used. Open blow-off pipes can often be replaced by engineered nozzles or blowers, cabinet coolers by fans or small chillers, and air-driven diaphragm pumps by electric ones where practical. Idle areas should be isolated automatically when a mill or line is down. Storage near large intermittent users stops them from dragging the whole header down, and heat from the compressors themselves can often be reused for space or process heating.
The 20–35% planning range reflects plants that tackle all three levers together. Leak repair alone can deliver a large share when the starting leak rate is 20–30%; pressure reduction and demand-side changes add the rest. Your own measured baseline decides where in the range you land.
KPIs That Keep Savings From Drifting Back
Compressor kW per unit of delivered flow, the efficiency of the supply side. It rises when compressors run unloaded or controls fight each other.
Leakage as a percentage of output, measured by base-load tests. The target is below 10%.
The number that proves header pressure can come down, or shows where pressure drop is hiding.
Night and weekend consumption compared with production hours. A rising ratio usually means new leaks.
Dryer performance. Wet air damages actuators and instruments, and oversized drying wastes energy.
What iFactory Delivers
kW, flow, pressure and dew point by compressor and header, with specific power trended.
Leak rate estimated from every planned stop, with no dedicated test needed.
Pressure at critical users against header setpoint, showing how far pressure can safely come down.
Idle areas under pressure and new unregulated users flagged as they appear.
Survey findings linked to work orders and verified by the next base-load result.
Energy saved measured against a production-normalized baseline.
Share compressor power, flow and pressure data, or let us install temporary logging. We size leakage, artificial demand and pressure savings for your plant.
How Deployment Works
Server racked on site, historian, meter and production data connected, and metering gaps listed against the units that matter most.
Baselines and expected-energy models built per unit, then piloted with your energy and process engineers reviewing every finding.
Dashboards, alerts and reports rolled out plant-wide, teams trained, and 24×7 remote monitoring of the system in place.
Compressed air is often the fastest energy win in a steel plant, so many programs start here. Where compressors lack flow meters, temporary logging during the first weeks gives the baseline while permanent meters are installed.
Frequently Asked Questions
The Compressed Air Challenge reports that poorly maintained systems can waste 20–30% of compressor output through leaks, while proactive leak programs can bring that below 10%.
The DOE sourcebook’s rule of thumb is about 1% of compressor energy for every 2 psi reduction in discharge pressure, plus lower leak and unregulated flows.
It is a realistic planning range when leaks, pressure and demand-side waste are addressed together. Your measured leak rate and pressure margin decide where you land.
A base-load test: measure compressor power and flow during a planned stop, when real demand is close to zero. The remaining consumption is mostly leakage.
Specific power, leak rate, pressure at critical users, the night-to-day base-load ratio and dew point.
Compressor power is usually available already. Flow, pressure and dew point meters may be needed; temporary logging can establish the baseline first.
iFactory measures leaks, pressure and demand continuously, turns findings into work orders and verifies every kWh recovered.