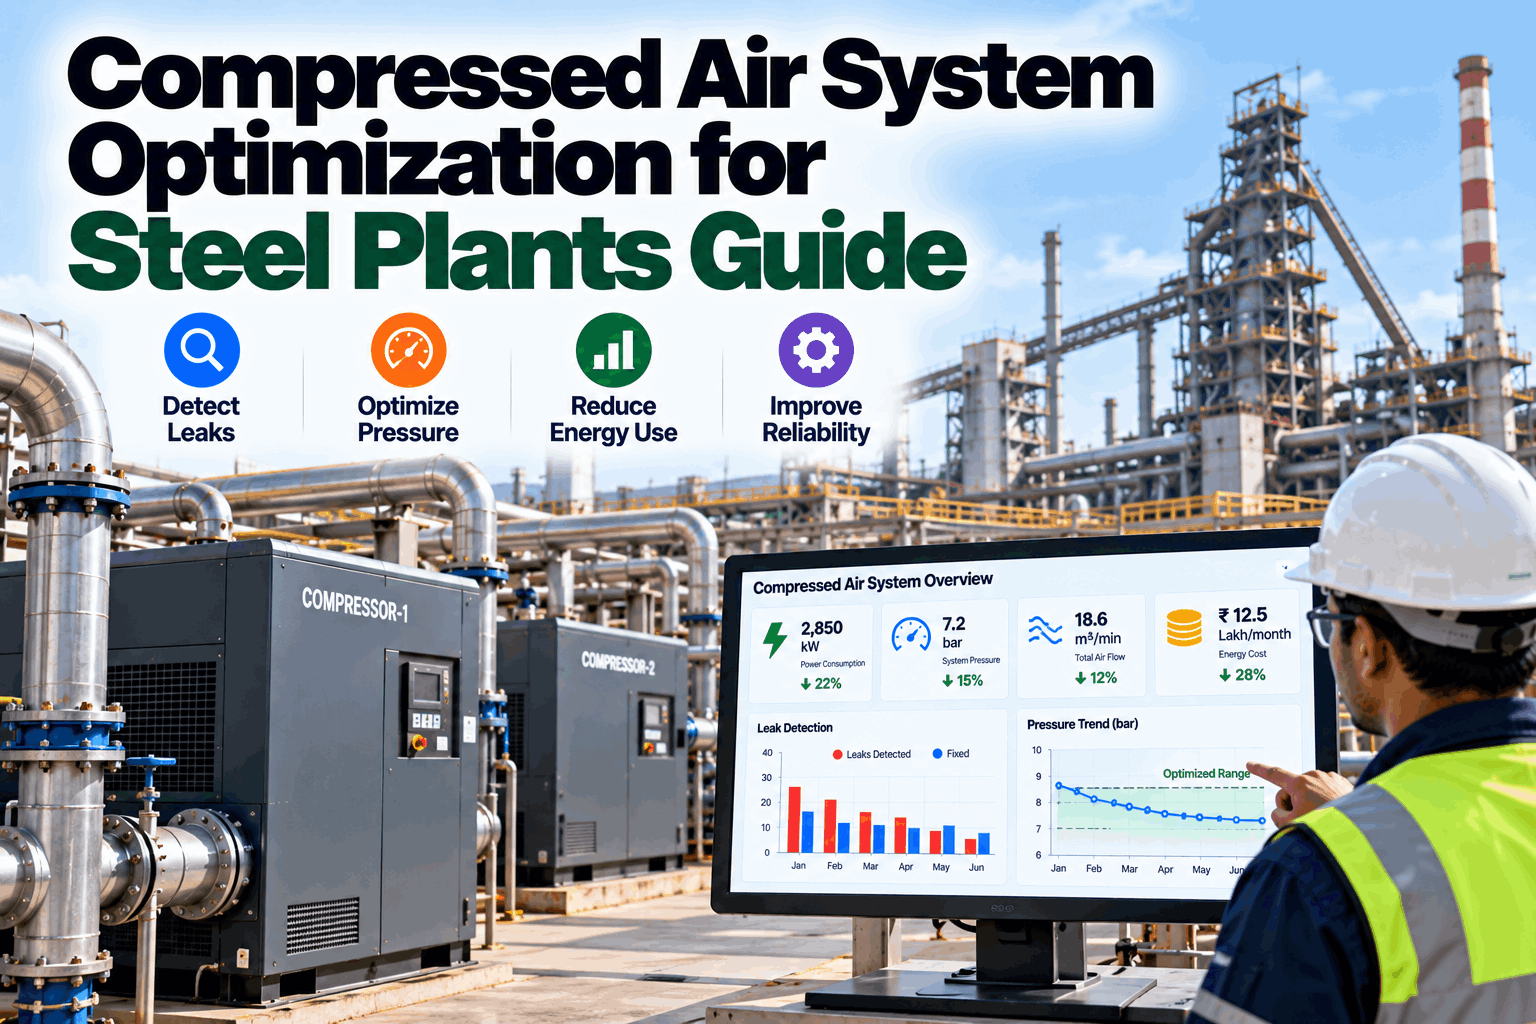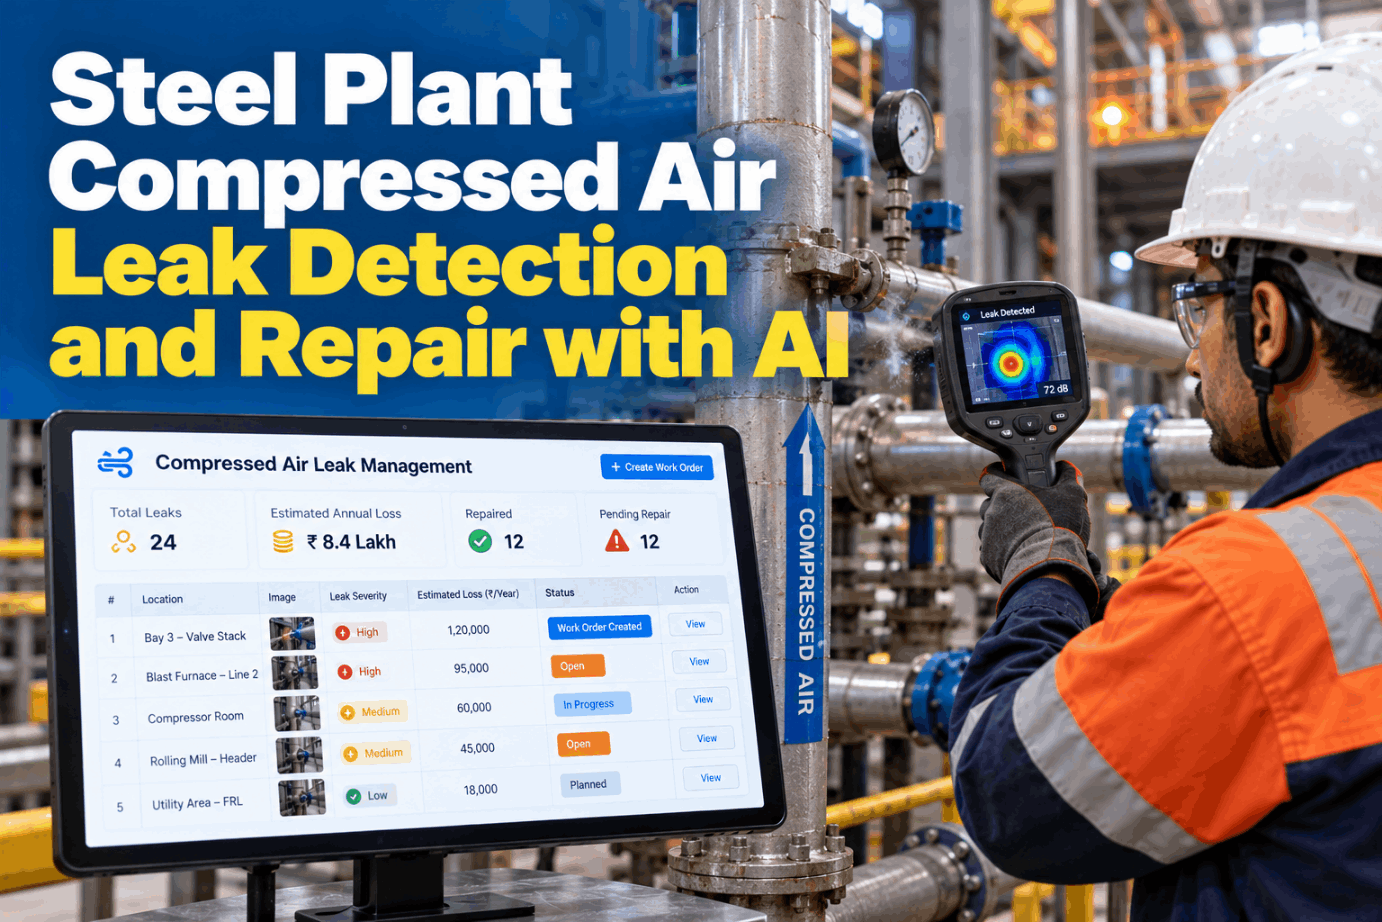
In a steel plant, compressed air leaks hide in plain sight. The hiss is lost under fans, drives and furnaces, and the cost lands on the power bill instead of on anyone's work list. A leak repair program fixes that by finding leaks with ultrasound, putting a flow and a price on each one and turning the list into ranked repair work. This guide covers leak surveys, the orifice chart, the cost-per-year formula, flow baselines, repair ranking and verification. See the survey-to-work-order loop in a short leak program demo.
Turn Every Tagged Air Leak Into a Ranked Repair Work Order
iFactory Energy AI reads ultrasonic survey results and voice-tagged leaks such as "leak, bay 3 valve stack, loud". Each leak gets a flow and cost estimate, and repair work orders are ranked by estimated cost per year.
Five Air Users Where Steel Plant Leaks Cluster
A steel plant runs compressed air into almost every area, often through long headers across hot, dusty bays. The DOE leak tip sheet names couplings, hoses, tubes, fittings, pipe joints, quick disconnects, filter-regulator-lubricator sets, condensate traps, valves, flanges, packings, thread sealants and point-of-use devices as the usual problem areas. In a mill, those parts sit on the users below. Map your own air users with our energy team.
How an Ultrasonic Survey Finds Leaks in a Noisy Mill
Air escaping through a small gap makes turbulence, and much of a small leak's sound energy sits above human hearing. Most leak detectors listen around 40 kHz and use heterodyning to shift that sound down into a headset, while a bandpass filter rejects ordinary plant noise. Ultrasound is also directional, so the inspector can point at one fitting and know the hiss comes from it. Some machinery and fast-switching electronics also emit ultrasound, so aim the sensor away from them. Plan a survey route with our leak specialists.
An Orifice Chart for Leaks at 100 psig
An ultrasonic reading proves a leak exists. To price it, you need a flow estimate. DOE Compressed Air Tip Sheet 3 lists leak rates by equivalent hole size and supply pressure, taken from Compressed Air Challenge training material. The listed figures are multiplied by 0.97 for well-rounded orifices and by 0.61 for sharp-edged ones, and DOE's own worked example uses 0.61. Real leaks are rarely neat holes, so treat the result as an estimate. Cost uses the assumed rates from the next section, which work out to $144 per cfm per year. Ask our support team for the chart at other pressures.
The Formula Behind Every Leak's Price Tag
DOE's tip sheet prices leaks with one line: leak flow in cfm × kW per cfm × hours × electricity price. kW per cfm is your compressor's specific power, shown on its CAGI data sheet as kW per 100 cfm; the DOE example uses 18 kW per 100 cfm, or 0.18 kW/cfm. Steel plants that run around the clock build up hours fast, which is why mid-size leaks matter. Every input below is assumed. Run it with your own compressors in an energy review.
At these inputs every cfm of leakage costs 0.18 × 8,000 × $0.10 = $144 a year. The saving only reaches the bill if compressor controls cut power when demand falls, so check control mode and sequencing too.
From a Spoken Leak Tag to a Ranked Work Order
Technicians tag leaks by voice as they walk the route. iFactory files each tag against the asset, adds the flow and cost estimate and places the repair in the queue by estimated cost per year.
Measure the Total Leak Load, Not Just Single Leaks
Tags show where leaks are. A baseline shows how much they add up to, and it is the number that proves the program works. The simplest method is a flow meter on the main header during a non-production period, when nearly all remaining flow is leakage. Where compressors modulate and no meter exists, the Compressed Air Challenge leak fact sheet gives a pressure-decay test. Steel plants rarely stop everything at once, so baseline each header during its own area stop. Get help setting one up from our support team.
- Pick a period with production stopped on that header
- Read flow at normal operating pressure
- Note demand that cannot be stopped, such as purges
- Repeat at the same conditions after repairs
- Leakage (cfm free air) = V × (P1 − P2) ÷ (T × 14.7) × 1.25
- V is system volume in ft³, P1 operating pressure, P2 about half of P1, T minutes
- The 1.25 corrects to normal pressure, since leaks slow as pressure falls
- Assumed example: 300 × (100 − 50) ÷ (5 × 14.7) × 1.25 ≈ 255 cfm
Rank Repairs by Cost, Access and Process Risk
A long leak list does not fix itself. DOE recommends a program built on identification and tagging, tracking, repair, verification and employee involvement. Ranking makes the list workable: big leaks first, live repairs done fast and shutdown-only repairs bundled into planned stops. In a steel plant, a leak that starves instrument air or a baghouse header can outrank a bigger leak elsewhere. Review your ranking rules in a program review.
Fields Every Leak Tag Should Carry
Whether tags are paper, handheld or voice, the same fields make a leak repairable and its cost traceable. Missing location or parts details are the usual reason a tagged leak stays open for months. Ask our support team for a printable tag.
Prove the Leak Is Gone Before the Tag Comes Off
A repair is not finished when the fitting is changed. It is finished when the leak is confirmed gone and the saving shows in the baseline. Verification also catches the common case where a retightened fitting leaks again within weeks. Tick through this list for each repair, or speak it on a voice round. See the steps in a short verification walkthrough.
Three Leaks and How a Ranked List Handles Them
These are illustrations, not case studies. They show how cost, access and process risk change the order of repairs. Walk through your own leak list with our support team.
Size the Program From Your Own Baseline
Program value should start from your measured baseline, not from published percentages. The worksheet below uses assumed inputs and the same cost-per-cfm arithmetic as above, so replace each figure with your own. Build your case with our energy engineers.
Set that against survey time, parts and labour. Leaks come back, so plan repeat surveys and keep trending the baseline to hold the saving.
Energy AI, Leak Tagging and NVIDIA Server in One Package
iFactory delivers Energy AI and leak tagging as a turnkey bundle. Flow, pressure and power signals from the compressor room and main headers are connected, and a pre-configured NVIDIA AI server ships racked and ready with the baseline, leak costing and ranking models pre-loaded. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your plant, request a turnkey quote.
- Pre-configured NVIDIA AI server, racked and ready
- Flow, pressure and kW links for compressors and headers
- Import of ultrasonic survey readings and photos
- Voice leak tagging on handheld devices
- Cost per year from your own kW/cfm and tariff
- Ranked repair work orders in your CMMS
- 24×7 remote monitoring of models and hardware
Meters and compressor data linked, first non-production baseline recorded per header.
First ultrasonic route walked, voice tags and cost ranking checked with energy and maintenance.
Ranked work orders switched on, verification steps and baseline review started.
Leak Repair That Shows Up on the Power Bill
iFactory links the survey, the price of each leak and the repair work in one loop, so fixes are ranked by value and checked afterwards. Our energy team can walk you through a pilot plan.
What Plant Managers Ask About Compressed Air Leak Detection in Steel
Put a Price on Every Leak, Then Fix the Costliest First
Tag leaks by voice, estimate flow and cost per year, rank the repairs and verify each one against the baseline. The full system is delivered turnkey and goes live in 6 to 12 weeks.