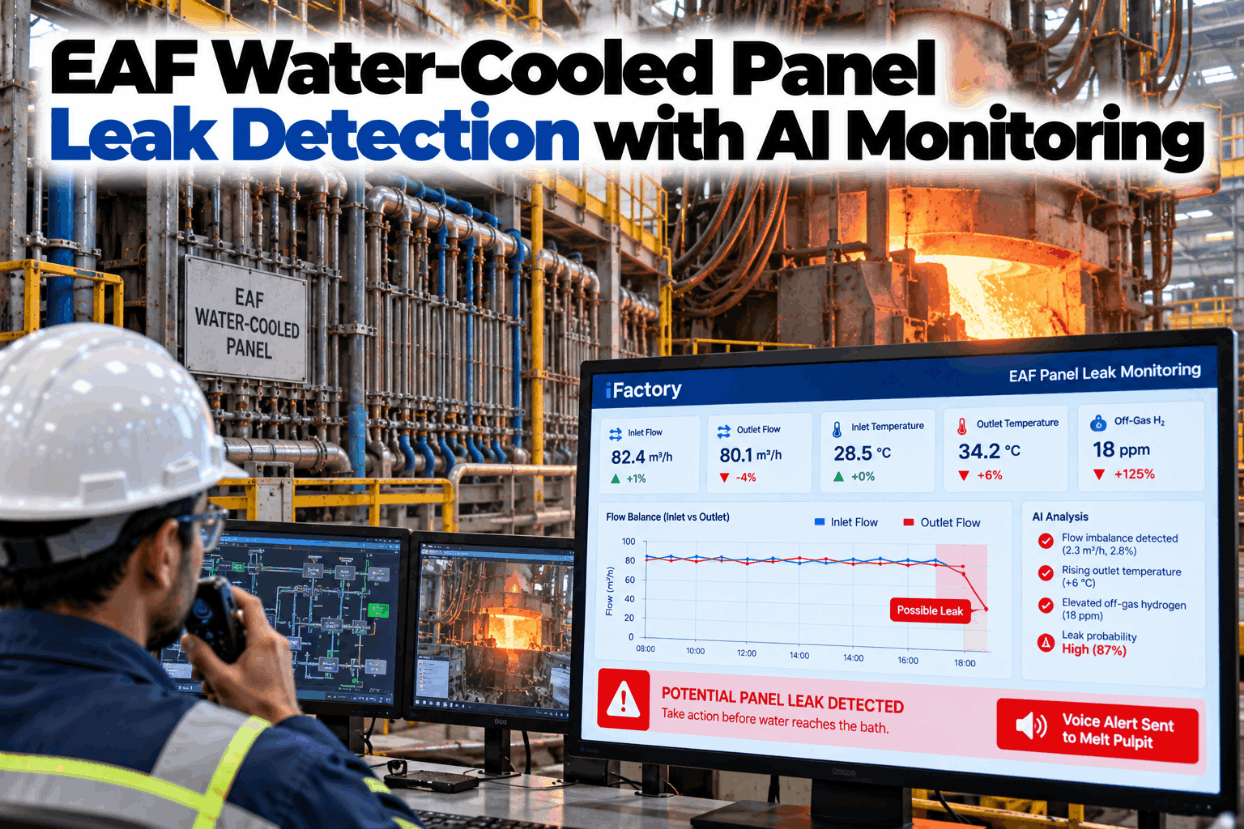
A cracked water-cooled panel rarely announces itself. The first litres boil off quietly on the slag, the heat carries on, and the circuit looks normal on a gauge nobody is watching. The danger comes when that water gets trapped under molten steel. EAF panel leak detection with AI compares inlet and outlet flow on every circuit, checks heat load and off-gas hydrogen, and speaks the alarm to the melt pulpit within seconds. See it on real furnace data in a short leak detection demo.
Catch a Panel Leak Before the Water Reaches the Bath
iFactory Predictive AI runs a flow-balance model on every panel circuit and cross-checks it against off-gas hydrogen. When both point to a leak, it calls the melt pulpit by voice and raises a panel repair work order with the evidence attached.
Why a Small Furnace Water Leak Is a Big Risk
Water that lands on top of the slag usually boils away. The risk changes when the water is covered. AIST's Safety First column on EAF water leaks explains that tilting a furnace can let molten metal trap water, which then flashes to steam and expands roughly 1,700 times. Tenova and Steel Dynamics engineers add that a steam explosion can be followed by a second, more severe hydrogen and CO explosion. Talk through your own furnace risks with our melt shop team.
The AIST column lists several US melt shop incidents linked to water entering a furnace, including fatal ones. In one, a pump kept feeding water into the furnace for at least seven minutes. Speed of detection and a clear response both matter.
Where Water-Cooled Panel Leaks Usually Start
Modern EAFs replace most of the upper shell and roof refractory with water-cooled panels. That keeps the furnace running longer between relines, but it puts hundreds of metres of pressurised pipe a short distance from the arc. Most leaks begin as thermal fatigue cracks in heavily welded tubular panels, according to AIST, while arc strikes and punctures cause sudden ones. Map the circuits on your furnace in a circuit review session.
Five Ways to Detect a Panel Leak, and What Each Misses
No single signal catches every leak. A CCPS Process Safety Beacon on water and molten metal recommends comparing inlet and outlet flows continuously and installing hydrogen detection with high-priority alarms. The vendor of one off-gas system states plainly that it is not a failsafe that can catch every leak. Layering methods covers the gaps of each. Ask our support team which signals your furnace already has.
A Worked Flow-Balance Example for One Circuit
In a closed cooling circuit, what goes into a panel should come out of it. A steady gap between inlet and outlet flow means water is going somewhere else. The numbers below show the arithmetic for one sidewall circuit. Before trusting a small gap, check that it is larger than the combined accuracy of the two flow meters and that it holds for more than a few seconds. Walk through your own circuits in a flow balance session.
Heat Load Shows Which Panel Is Under Stress
Heat load turns flow and temperature into one number: flow × specific heat × temperature rise. For SW-07, 42.0 m³/h is about 11.67 kg/s, and with an 11 °C rise and water at 4.18 kJ/kg·K that gives 11.67 × 4.18 × 11 ≈ 536 kW. Comparing each panel with its own normal level shows where the arc is working hardest, and where the next crack is likely. The grid is an illustration. Review your panel map with our cooling specialists.
Using Off-Gas to Confirm Water Is Inside the Furnace
When water enters a furnace, part stays as vapour and part breaks down to hydrogen, so off-gas systems measure both. A paper by Tenova and Steel Dynamics notes that under normal reducing conditions the H₂ to CO ratio is usually below 1, and starts closer monitoring when it goes above 1. Wet scrap, humidity, burner combustion and electrode spray also add water, which is why off-gas works best next to flow balance. See the correlation on real heats in a live data walkthrough.
A Leak Alarm the Melter Hears, Not a Trend Nobody Opens
iFactory speaks leak alarms to the melt pulpit, names the circuit and the evidence, and records the response. Slow-growing leaks become a repair work order for the next planned stop, with the flow trend attached.
Watch, Alarm, Trip: Three Levels With Clear Owners
An alarm system that cries wolf gets ignored, and one that waits too long is useless. The off-gas paper above describes alerts graded by the severity and duration of the event, and the same idea works for flow balance. The limits below are examples only. Each furnace needs its own, set from meter accuracy, normal circuit behaviour and your safety review. Set your tiers with our safety engineers.
What the Crew Does When the Leak Alarm Sounds
The response belongs in your written procedure, and iFactory shows it rather than replacing it. Common guidance points the same way. India's Ministry of Steel EAF safety code lists stopping the arc, stopping any tilt or furnace movement and closing the water valve. AIST cites a procedure calling for shutting off the water and leaving the area. The sequence below follows that pattern, always per your site procedure. Rehearse it with our melt shop team.
The Panel Repair Work Order iFactory Raises for You
Finding a leak is half the job. The CSB's recommendation after the Carbide Industries furnace explosion called for a mechanical integrity programme with leak detection and repair. iFactory raises the repair order automatically, with the circuit, the evidence and the safety steps already filled in, so the panel shop does not start from a blank form. Ask our support team to map it to your CMMS.
Sizing the Value Without Inflating It
The main value of leak detection is the incident that never happens, and that should not be turned into a made-up number. What you can size is delay from leaks found late. The worksheet uses assumed inputs only to show the arithmetic. Replace them with your own delay records in a value review session.
Leak Models, Voice Alarms and Edge Server in One Delivery
iFactory delivers leak detection as a turnkey package. A pre-configured NVIDIA AI server ships racked and ready, with flow-balance and off-gas correlation models pre-loaded, and connects to your cooling water PLC and off-gas analyser on site. You rack it, plug in power and Ethernet, and the AI is live. Scope it for your furnace with our deployment team.
- Pre-configured NVIDIA AI edge server, racked and ready
- Flow-balance model for every panel circuit
- Heat-load baseline per panel, learned heat by heat
- Off-gas H₂ and H₂O correlation with your analyser
- Voice alarms to the melt pulpit with confirm-back
- Automatic panel repair work orders in your CMMS
- 24×7 remote monitoring of models and hardware
Server racked, PLC and analyser linked, every circuit mapped and meter health checked.
Baselines learned per circuit, alarms run silently and are reviewed with the melt team.
Voice alarms switched on, response drills run, work orders flowing to maintenance.
How iFactory Fits Your Melt Shop
iFactory works alongside your furnace control and safety interlocks, adding circuit-level insight and a faster human response. See how it fits in a short furnace demo.
What Melt Shop Leaders Ask About EAF Panel Leak Detection
Know Which Circuit Is Leaking Before Anyone Tilts
Run flow balance on every panel circuit, confirm with off-gas hydrogen and put a voice alarm in the melt pulpit. Repair orders follow automatically. Delivered turnkey and live in 6 to 12 weeks.