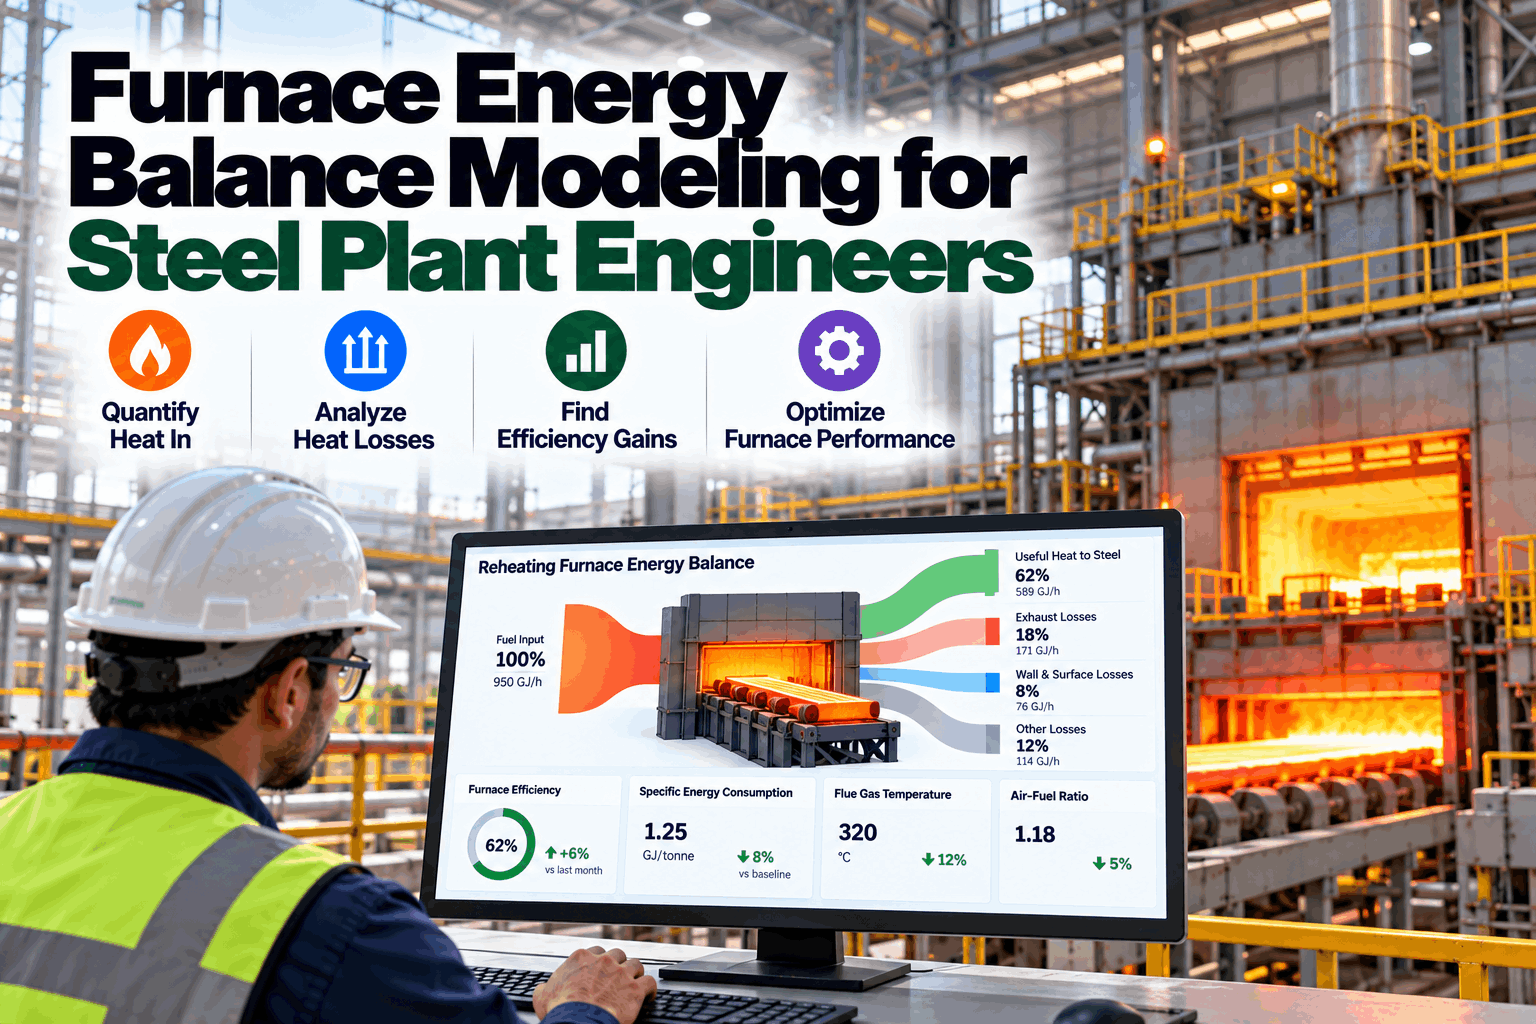
Reheating furnaces, hot blast stoves and ladle preheaters burn a large share of a steel plant’s fuel, yet most plants track them with one number: fuel per tonne. When that number rises, engineers are left guessing whether it was excess air, cold charge, open doors or a damaged skid. A furnace energy balance answers the question by quantifying heat in, heat out and every loss path, so the 8–15% quick wins can be found, sized and fixed in the right order. Book a 30-minute furnace balance review with your historian data.
Heat in, heat out and every loss quantified per furnace and per zone, so engineers fix the largest losses first.
At a Glance
Why an Energy Balance Beats a Fuel Meter
A fuel meter tells you how much a furnace burned. It cannot tell you why this week’s fuel per tonne is 4% higher than last month’s, or which of a dozen possible causes is responsible. An energy balance can. By accounting for heat into the furnace and every path heat takes out, whether into the stock, up the stack, into cooling water or through walls and open doors, it turns a single number into a map of losses with sizes attached.
For plant engineers, that map changes the conversation. Instead of generic advice to tune combustion, the balance shows that flue losses rose because excess oxygen drifted in the soaking zone, or that cooling water losses jumped after skid insulation was damaged. Each loss has a cause and a fix, and the fixes can be ranked by size.
Measuring Each Term of the Balance
| Balance term | How it is quantified | Data sources |
|---|---|---|
| Heat in | Fuel flow × calorific value, plus sensible heat of preheated air and fuel | Fuel meters, gas analysis, recuperator temperatures |
| Heat to stock | Mass × enthalpy rise from charge to discharge temperature, by steel grade | Tracking system, pyrometers, grade data |
| Flue gas loss | Flue gas flow (from fuel and air) × enthalpy at stack temperature; unburnt CO included | Flue temperature, O₂ and CO analyzers |
| Skid and cooling water | Water flow × specific heat × temperature rise | Cooling water flow meters, inlet and outlet temperatures |
| Walls and roof | Surface temperature to convection and radiation loss by area | Thermographic survey, shell thermocouples |
| Doors and openings | Radiation through openings × time open, plus infiltration effects | Door status signals, furnace pressure |
Every megawatt removed by cooling water must be replaced by fuel. Damaged skid insulation shows up here first, often long before anyone inspects the skids.
Where the 8–15% Quick Wins Usually Are
Quick wins are the measures that need little or no capital, only control, practice and maintenance. Across reheating furnaces, many plants find that together they fall in an 8–15% planning range for fuel per tonne. The balance shows which ones apply to your furnace and how big each is.
Excess air carries heat up the stack. Holding flue O₂ at the lowest safe level, zone by zone, is often the single largest quick win.
Negative pressure pulls in cold air; excessive positive pressure pushes flames out of openings. Both cost fuel.
Charging and discharge doors left open longer than needed radiate heat directly to the building.
Every degree of charge temperature is heat the furnace does not have to supply. Coordinating caster and furnace raises the hot-charge ratio.
Turning zones down during mill delays, instead of holding full temperature, cuts fuel burned for no output.
Repairing skid insulation and keeping recuperators clean restores losses that creep up between shutdowns.
Furnace Types and Their Dominant Losses
| Furnace | Typical dominant losses | First levers to check |
|---|---|---|
| Reheating (walking beam, pusher) | Flue gas, skid cooling, delays | Excess O₂ by zone, hot charging, delay turn-down, skid insulation |
| Hot blast stoves | Flue gas, shell losses, cycle timing | Combustion control, stove cycle optimization, waste gas heat recovery |
| Ladle and tundish preheaters | Open-flame losses, missing lids, long preheat times | Lid use, burner tuning, preheat scheduling |
| Annealing and heat treatment | Flue gas, protective gas, idle holding | Load planning, idle setbacks, burner maintenance |
| Coke oven battery heating | Flue gas, heating gas distribution, door leakage | Heating control, flue temperature balance, door sealing |
Reheating furnaces get most of the attention, but ladle and tundish preheaters are often among the least efficient fuel users in a plant, burning open flames for hours with lids off. A short balance on the preheater fleet frequently turns up savings out of proportion to its size.
From One-Off Study to Live Balance
A traditional energy balance is a two-week measurement campaign that produces a report and a snapshot. It is valuable, and it also starts ageing the day it is finished. A data-driven balance uses the same physics, calibrated against the campaign, then runs continuously on historian data: fuel, air, flue analysis, cooling water, door signals and tracking. Efficiency and each loss term are recalculated every hour, zone by zone.
Measure all balance terms once, including temporary instruments.
Fit the physics model to the campaign and historical data.
Recalculate losses hourly from historian signals.
Flag losses that rise beyond their normal band.
Confirm the fix brought the loss back down.
What iFactory Delivers
Physics-based heat balance per furnace and zone, calibrated to your measurements.
Flue, cooling water, wall and opening losses recalculated continuously.
Air-fuel ratio, pressure, door, hot charging and delay opportunities sized in GJ and dollars.
Loss terms that rise beyond their band flagged with the signals behind them.
Measurement plans and temporary instrumentation lists for the initial balance.
Fuel per tonne against a normalized baseline after every fix.
Share a few weeks of furnace historian data. We build a first-pass heat balance, size each loss and rank the quick wins for your furnace.
How Deployment Works
Server racked on site, historian, meter and production data connected, and metering gaps listed against the units that matter most.
Baselines and expected-energy models built per unit, then piloted with your energy and process engineers reviewing every finding.
Dashboards, alerts and reports rolled out plant-wide, teams trained, and 24×7 remote monitoring of the system in place.
Frequently Asked Questions
It is an accounting of all heat entering a furnace and every path by which heat leaves it, including the stock, flue gas, cooling water, walls and openings. It shows where fuel goes and how efficient the furnace is.
Yes. The ISO 13579 series sets out a method for measuring energy balances and calculating the efficiency of industrial furnaces.
After heat delivered to the stock, flue gas loss is usually the largest, driven by stack temperature and excess air. Skid cooling water, walls and openings follow.
It is a planning range for low-capex measures such as air-fuel ratio control, furnace pressure, door practice, hot charging and delay strategies. A furnace that is already well tuned will find less.
Yes. A physics model calibrated to a measurement campaign can run on historian data and recalculate losses hourly, zone by zone.
Fuel flow and calorific value, air flow or flue analysis, stack temperature, stock tracking and temperatures, cooling water flow and temperatures, door signals and shell temperatures.
iFactory builds calibrated heat balances for your furnaces and tracks every loss hourly, so quick wins are found, fixed and verified.