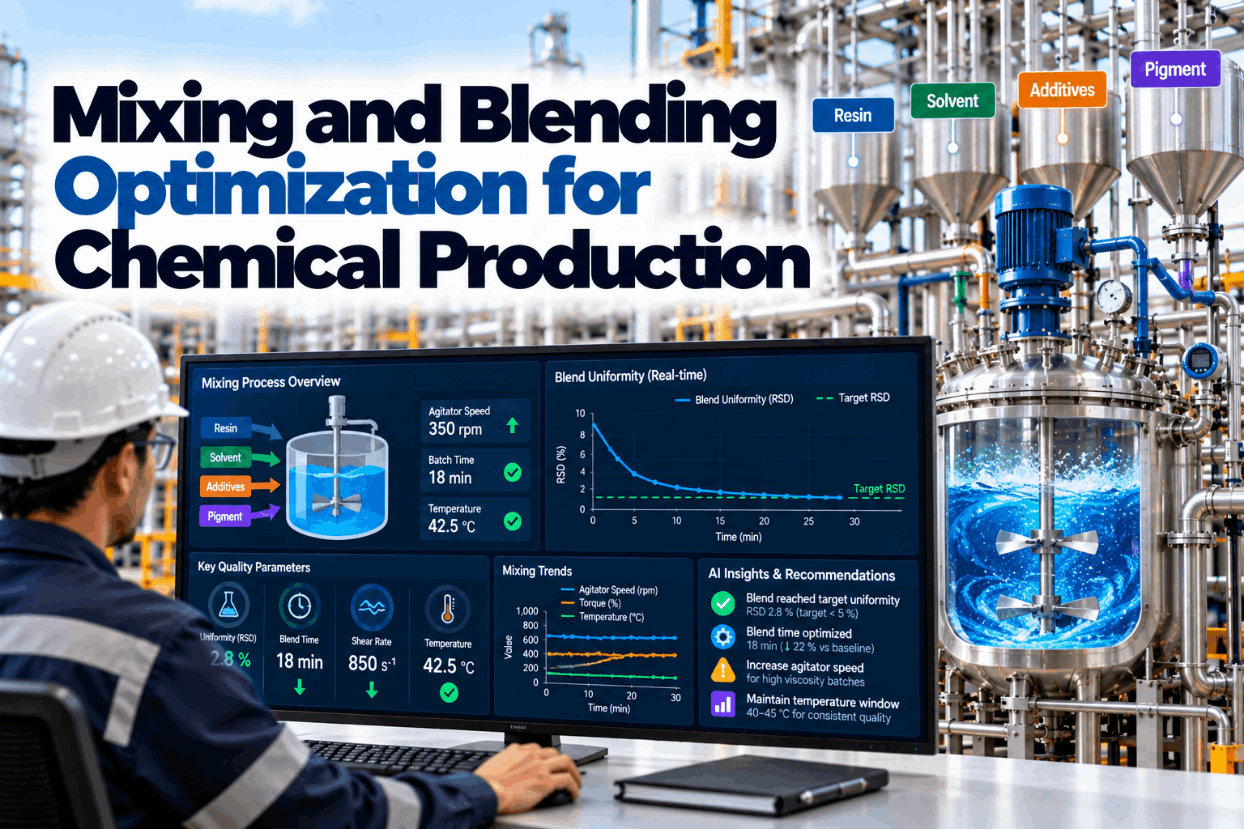
Mixing looks simple and is easy to get wrong. A blend that is not uniform gives off-spec paint color, uneven polymer properties or a specialty chemical that fails its assay. Most plants control mixing by recipe time and speed: mix for a fixed number of minutes, sample, and re-mix if the sample fails. That approach ignores how raw materials, batch size, temperature and viscosity change from batch to batch. Mixer power, torque, temperature and in-line measurements already show how a batch is progressing; used well, they tell operators when the blend is ready rather than when the clock says so. This guide covers mixing fundamentals, impeller choice, scale-up, blend uniformity, segregation, dispersion quality in coatings and how continuous monitoring improves first-time-right batches. To see your batch data analyzed, book a short walkthrough.
Mixing and Blending Optimization for Chemical Production: Uniform Batches, First Time
Blend endpoints set by the batch, not the clock, using power, torque, temperature and in-line signals, so paints, coatings, polymers and specialty chemicals pass first time with less re-mixing.
Why Mixing Problems Persist
Mixing is in almost every chemical process, which makes it easy to overlook. When the Handbook of Industrial Mixing was reviewed in AIChE’s Chemical Engineering Progress, the review recalled an estimate that poor mixing cost the US chemical industry between $1 billion and $10 billion in 1989. The number is old, but the causes it described, lost yield, off-spec product and scale-up failures, still apply.
In batch production, the usual control is a recipe: charge in order, mix at a set speed for a set time, take a sample and test. If the sample fails, mix longer and test again. Each retest adds time, and each batch that passes after too much mixing used energy and capacity it did not need.
The batch itself carries information about how mixing is going. Power draw and torque change as solids wet out and viscosity develops. Temperature shows reaction and shear heating. In-line measurements show composition. Reading these signals lets the plant judge each batch on its own progress.
That is the shift from recipe time to batch endpoint. We can review your batch data on a call.
Mixing Fundamentals in Plain Terms
A few quantities explain most mixing behavior.
Because power rises with the cube of speed and the fifth power of diameter, a modest speed change can double or halve mixing intensity. That is why power and torque readings are such useful signals: they show what the mixer is actually doing to the batch.
Most modern mixer drives already report power or torque. We use them as the core signal in every rollout.
Choosing Impellers for the Duty
Different impellers give different balances of flow and shear. Typical turbulent power numbers, from published impeller data, show how differently they behave.
| Impeller | Typical power number | Flow pattern | Good for |
|---|---|---|---|
| Six-blade Rushton turbine | About 5.0 | Radial, high shear | Gas dispersion, fast reactions |
| 45° pitched-blade turbine | About 1.3 | Mixed axial and radial | General blending, solids suspension |
| Hydrofoil | About 0.3–0.75 by design | Axial, high flow, low shear | Blending and suspension at low power |
| Marine propeller | About 0.35 | Axial | Low-viscosity blending |
| High-shear rotor-stator | Varies by design | Intense local shear | Dispersion, emulsions, deagglomeration |
| Ribbon, paddle and tumble blenders | Not comparable | Bulk movement of powders or pastes | Dry and paste blending |
At the same speed and diameter, a Rushton turbine draws roughly 14 times the power of a marine propeller. Choosing the wrong impeller either wastes energy on shear the process does not need or fails to deliver the shear it does need.
Powder blending uses different equipment altogether. Chemical Engineering lists V-type, tumble, ribbon or paddle, pneumatic and high-speed agitated blenders, each suited to particular particle sizes, cohesiveness and fragility.
Our engineers can review whether your impellers match the duty of each product.
Scale-Up: Why Lab Mixing Does Not Copy Directly
A blend that works in a 5-liter lab vessel often behaves differently in a 10-cubic-meter tank. Scale-up rules try to keep the important mixing quantity constant.
Keeps overall mixing intensity similar. Common for blending and suspension.
Keeps peak shear similar. Common for dispersion and shear-sensitive products.
Keeps the flow regime similar, but is rarely practical at large scale.
Gas transfer, solids suspension, dispersion and blending each favor different rules.
Blend time usually rises at larger scale even when intensity is held constant.
First plant batches confirm or correct the scale-up assumption.
No single rule keeps everything constant. Holding power per volume constant raises tip speed at larger scale; holding tip speed constant lowers power per volume. The right compromise depends on what matters most for the product.
Plant data closes the loop. Comparing power, torque and blend results at plant scale with lab results shows where the scale-up assumption held and where it did not, which improves the next product transfer.
Using plant data to verify scale-up shortens product transfers. See how in a demo.
Measuring Blend Uniformity Reliably
A blend is only as good as the test that proves it. Sampling errors can make a good blend fail or a poor blend pass.
Illustrative. Each plant sets its own uniformity limit by product; the method of calculation is the same.
Chemical Engineering’s guidance on sampling is simple: collect a full stream sample, and always sample while the material is moving, from the beginning to the end of discharge. Samples taken from the top of a resting batch can misrepresent the whole.
Segregation can undo good mixing after the mixer. The same article describes three mechanisms: sifting, where fine particles move through a pile of coarser ones; fluidization, where fine light particles rise to the top; and dusting, where fines carried by air settle near walls. A blend that is uniform in the mixer may not be uniform in the drum.
Linking uniformity results to batch signals shows which signals predict a pass. Ask our team how the model is trained.
Dispersion Quality in Paints and Coatings
In paints and coatings, mixing must break pigment agglomerates and wet every particle, not just distribute ingredients evenly.
The Hegman gauge, under ASTM D1210, rates dispersion on a 0–8 scale, from about 100 microns down to zero.
Too coarse a grind can reduce color uniformity, gloss and opacity.
High-speed dispersers depend on tip speed to deliver the shear that breaks agglomerates.
Dispersion works best within a viscosity range that transfers shear to the pigment.
Power falls and temperature rises as dispersion progresses.
Extra time costs energy and can damage some pigments or raise temperature too far.
Many coatings plants check fineness of grind by hand at fixed times. Combining those results with power and temperature curves shows when each batch reaches its target, so checks can be timed to the batch rather than the clock.
Color consistency between batches depends on dispersion as much as on formulation. Tracking dispersion endpoints alongside color measurements shows whether color variation comes from raw materials or from mixing.
Coatings plants often see fewer tinting corrections once dispersion endpoints are consistent. Discuss your process with our specialists.
Fixed Recipe Times Versus Batch Endpoints
The difference between recipe-based and endpoint-based mixing shows in retests, cycle time and energy.
- Same time for every batch
- Sample after the clock runs out
- Re-mix and retest if it fails
- Over-mixing hidden in passing batches
- Raw material variation ignored
- Scale-up checked only by test results
- Time set by the batch’s own signals
- Sample when the model predicts readiness
- Fewer retests and re-mixes
- Shorter cycles where batches finish early
- Raw material effects visible
- Scale-up verified with plant data
Endpoint-based mixing does not remove testing. Quality release still depends on the plant’s specification and test methods. What changes is that tests are taken when the batch is likely to pass, and batches that need more time get it before sampling.
See how endpoint predictions are shown to operators in a session.
Mixing and Blending Checklist
Use this checklist to move from recipe times to batch endpoints.
Most plants already have the signals in their batch system. Bringing them together is the first step of a mixing review.
What Better Mixing Is Worth
Value comes from fewer failures and shorter cycles.
The 1989 industry estimate of $1–10 billion shows how broad the cost of poor mixing can be. In a single plant the value shows up as capacity: every retest and re-mix occupies a vessel that could be making the next batch.
A review of a few months of batch records usually shows your retest rate and its causes. Book one with our advisors.
How iFactory Delivers Mix Uniformity Monitoring
Normal signal patterns learned per product.
Readiness predicted from the batch’s own signals.
Batches deviating from normal flagged early.
Lots and suppliers tied to mixing behavior.
Plant results compared with lab data.
Uniformity and fineness results tied to batch records.
It runs on premises beside your batch system and historian. Share a few months of batch records and we will show your golden-batch curves in a working session.
Find Out Why Batches Need a Second Mix
Share batch records with power, temperature and test results. We build golden-batch curves for each product and show which signals predict a first-time pass.
Power draw settled 9% lower than the golden-batch curve after the second addition. The model predicts a blend uniformity outside the plant limit if mixing stops at the recipe time.
A Batch Extended Before Sampling
This exchange shows how a formulation engineer might use iFactory.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the mixing and blend uniformity models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers data connections across mixers, dispersers, blenders and batch systems, DCS, PLC/SCADA, historian, LIMS and CMMS integration, cabling and network setup, operator and engineer training, and 24×7 remote monitoring. Recommendations run in advisory mode first, and nothing writes to your control system without your management of change approval.
Server installed, DCS and historian links live, historical process, lab and maintenance data loaded.
Models calibrated on your own unit data, then run in advisory mode on one unit with your process engineers reviewing every recommendation.
Rollout to the agreed units under your management of change, operator and engineer training, and 24×7 remote monitoring in place.
Software, server and integration come as one package. For pricing on your site, contact our sales team.
Frequently Asked Questions
Usually as the coefficient of variation of several samples taken across the batch or discharge: the standard deviation of results divided by their mean. Each plant sets its own limit by product.
A dimensionless measure of impeller power draw. In turbulent flow it is roughly constant: about 5.0 for a six-blade Rushton turbine, 1.3 for a 45° pitched-blade turbine and 0.3–0.75 for hydrofoils.
By holding the most important quantity constant, usually power per volume for blending and suspension or tip speed for dispersion, then verifying with plant data.
Through sifting, fluidization and dusting during discharge, transfer and storage, especially when particles differ in size or density.
With a Hegman gauge under ASTM D1210, which rates fineness of grind on a 0–8 scale. Coarse grind can reduce color uniformity, gloss and opacity.
A first mixing area can typically be monitored within a 6–12 week rollout, using existing batch signals. Plan it with our engineers.
Let Every Batch Tell You When It Is Ready
iFactory learns golden-batch curves, predicts blend and dispersion endpoints and flags drifting batches, raising first-time pass rates and freeing vessel capacity.
Illustrative. Fewer retests and re-mixes as blend endpoints follow the batch instead of a fixed clock.