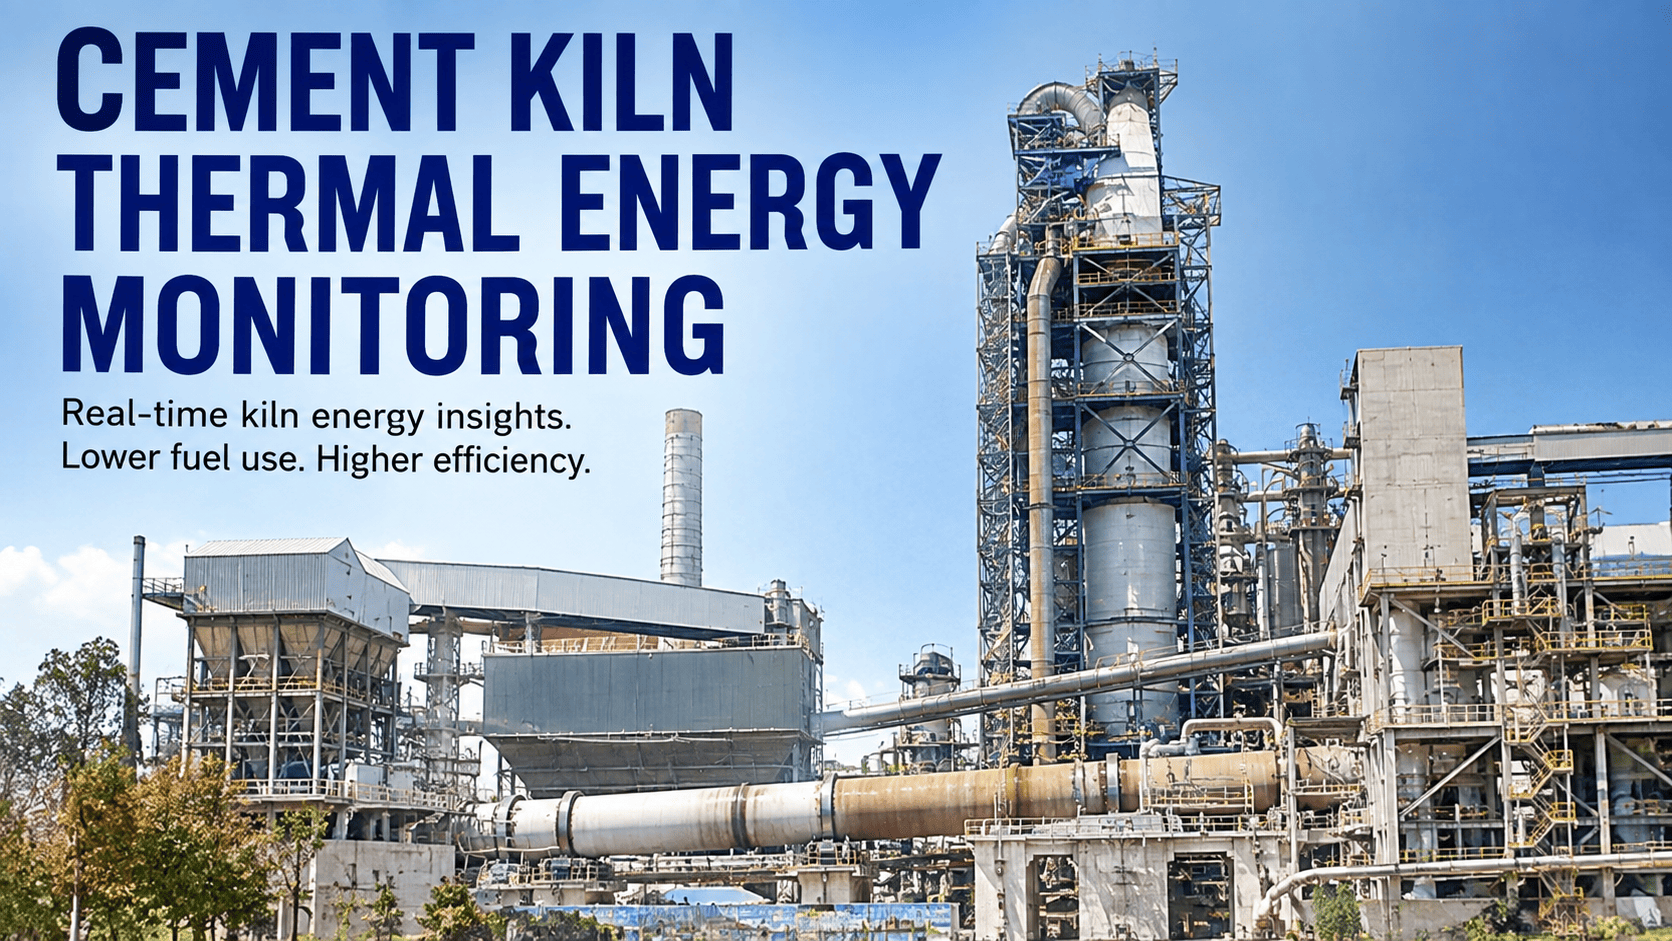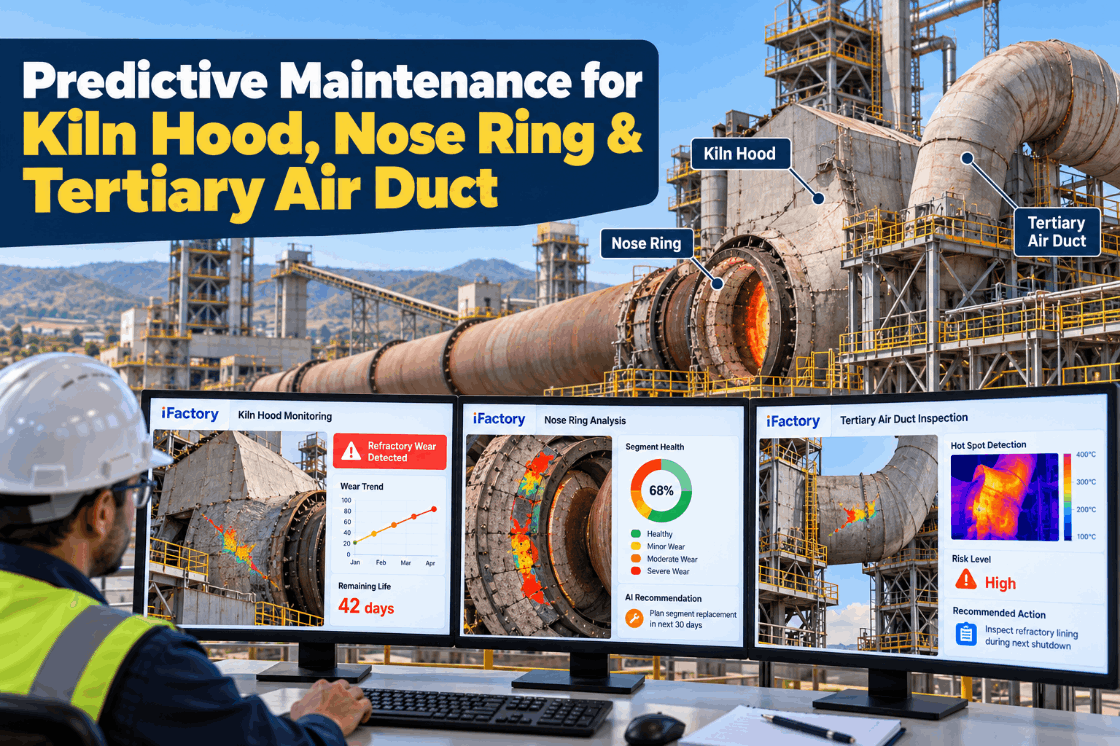
The kiln outlet is where a rotating shell at clinkering temperature meets a stationary hood, a cooling air system and the duct that carries hot air to the calciner. Each part of that junction wears in its own way, is checked by a different team and is usually only seen properly when the kiln is cold. Predictive maintenance puts their readings side by side, so the next kiln stop is planned around evidence instead of surprises. See how it looks for your own outlet end in a short kiln outlet walkthrough.
Read the Nose Ring, Kiln Hood and Tertiary Air Duct as One Hot Line
iFactory joins shell scanner data, casing IR surveys and the kiln outlet camera into one view of the interfaces where the kiln meets the cooler. When a segment warms or a casting starts to spall, the AI flags it weeks ahead, so the refractory crew reaches the planned stop with the right scope.
Four Junctions at the Hot End That Need Their Own Watch
The outlet end is harsh even by kiln standards. A US patent on kiln outlet segments describes temperatures of roughly 1,200 to 1,450°C in that region, and thermally driven abrasive wear on cast steel segments after about one year. The hood and the tertiary air duct sit right beside it, carrying the same hot, dusty air. These four interfaces are the focus of this page. Map your own outlet layout with our refractory support team.
How Each Interface Fails, and the First Sign to Look For
Nose ring castables have traditionally used calcium aluminate cement, and low, ultra-low and no-cement castables have been developed for the job because frequent air cooling causes cracking and thermal spalling. Damper suppliers point to a similar mismatch in the duct, where steel and castable expand at different rates. The matrix lists early signs and the data that shows them. Review your signals in a refractory data session.
Casing Surveys You Can Trend, Not Just Photograph
A single thermal image of a hood or duct casing tells you little. A series taken the same way tells you a lot. ISO 18434-1, the general thermography standard for condition monitoring, covers emissivity, reflected temperature and reporting, and FLIR describes repeat surveys showing earlier kiln hot spots that had greatly expanded. iFactory stores each survey point so the change is visible, not just the peak. Ask our thermography support team to review your route.
Monolithic linings hang on steel anchors. Plibrico notes that metallic anchors expand at about three times the rate of alumino-silicate refractories, which is why anchor tips are coated. Once a crack lets heat reach the anchors, they can oxidise and lose grip, and the hot area grows.
Ask the Hot End a Question, Get a Straight Answer
iFactory Predictive Maintenance answers spoken questions from the control room or the hood platform, using scanner, survey and camera data together, and confirms back before it adds anything to the stop list.
What the Outlet Camera Can Watch Between Stops
Many kilns already have a camera looking up the kiln from the hood, mainly for the flame and burning zone. The same view shows the nose ring tip. iFactory AI Vision learns what the tip profile looks like when it is sound and compares each frame against that baseline, accounting for dust and flame glare. See it run on outlet footage in a camera review call.
Rank Casing Points by How Fast They Are Warming
Refractory suppliers describe the tertiary air as carrying a high clinker dust load at times, with lining wear concentrated at bends and gas diversions and at the flaps and gates that control flow. That makes bends the first places to grid. The ranking below is illustrative, built from eight weekly surveys. Get help setting up your grid from our support engineers.
Found at the Stop, or Known Before It
Outlet refractory work is usually done in planned kiln stops, and the length of the stop is set by the slowest job. When the hood or nose ring is only opened up once the kiln is cold, the scope grows while the clock runs. FLIR makes the same point for planned shutdowns: custom parts take time, so damage spotted between stops lets materials be ordered in advance. Compare your last stop in a stop review call.
- Scope written after the hood door opens
- Segments and anchors ordered on the day
- Duct bends checked only if time allows
- Heat-up starts late because castable arrived late
- Scope drafted from trends and camera frames
- Parts and castable confirmed on site
- Worst duct bends already on the list
- Crew sized for the work actually expected
A Stop Scope Sheet Built From the Data
Refractory work at the outlet needs materials, anchors, formwork and people lined up before the kiln cools. Fuller notes that its precast outlet sectors need no drying and can save up to two days per replacement, which only helps if the parts are on site. One sheet per interface keeps the plan honest. Ask our support team for a blank sheet.
Three Illustrative Outlet Findings
These are illustrations of how the data usually comes together, not case studies. Your own procedures and refractory supplier decide the response. Talk through your own scenarios with our refractory specialists.
Outlet Camera Models, Survey Records and Edge Server, Delivered Ready
iFactory delivers Predictive Maintenance and AI Vision for the kiln outlet as one package. A pre-configured NVIDIA AI server ships racked and ready, with vision and anomaly models loaded, so camera video and scanner data are processed on site. You rack it, plug in power and Ethernet, and the AI is live. To size it for your kiln line, ask our support engineers.
- Pre-configured NVIDIA AI edge server, racked and ready
- Vision models for the nose ring and outlet view
- Links to the shell scanner and DCS signals
- Digital casing IR survey route and point records
- Damper, cooling fan and hood draft trending
- Voice queries and stop scope sheets per interface
- 24×7 remote monitoring of models and hardware
Scanner, camera and DCS signals linked, survey points numbered on the hood and duct.
Tip profile and casing baselines learned, flags checked by the refractory engineer.
Flags and voice queries switched on, stop scope sheets in daily use.
Predictive Maintenance and AI Vision for the Hot End
iFactory works with the scanner, camera and survey tools you already have and adds the link between them. We can outline a pilot on one kiln in a pilot planning call.
Questions Kiln and Refractory Teams Ask About the Outlet End
Reach the Next Kiln Stop With the Scope Already Written
Put the nose ring, hood and tertiary air duct on one hot-end view, rank every casing point by its rate of rise and turn flags into stop scope sheets. The system ships turnkey and goes live in 6 to 12 weeks.