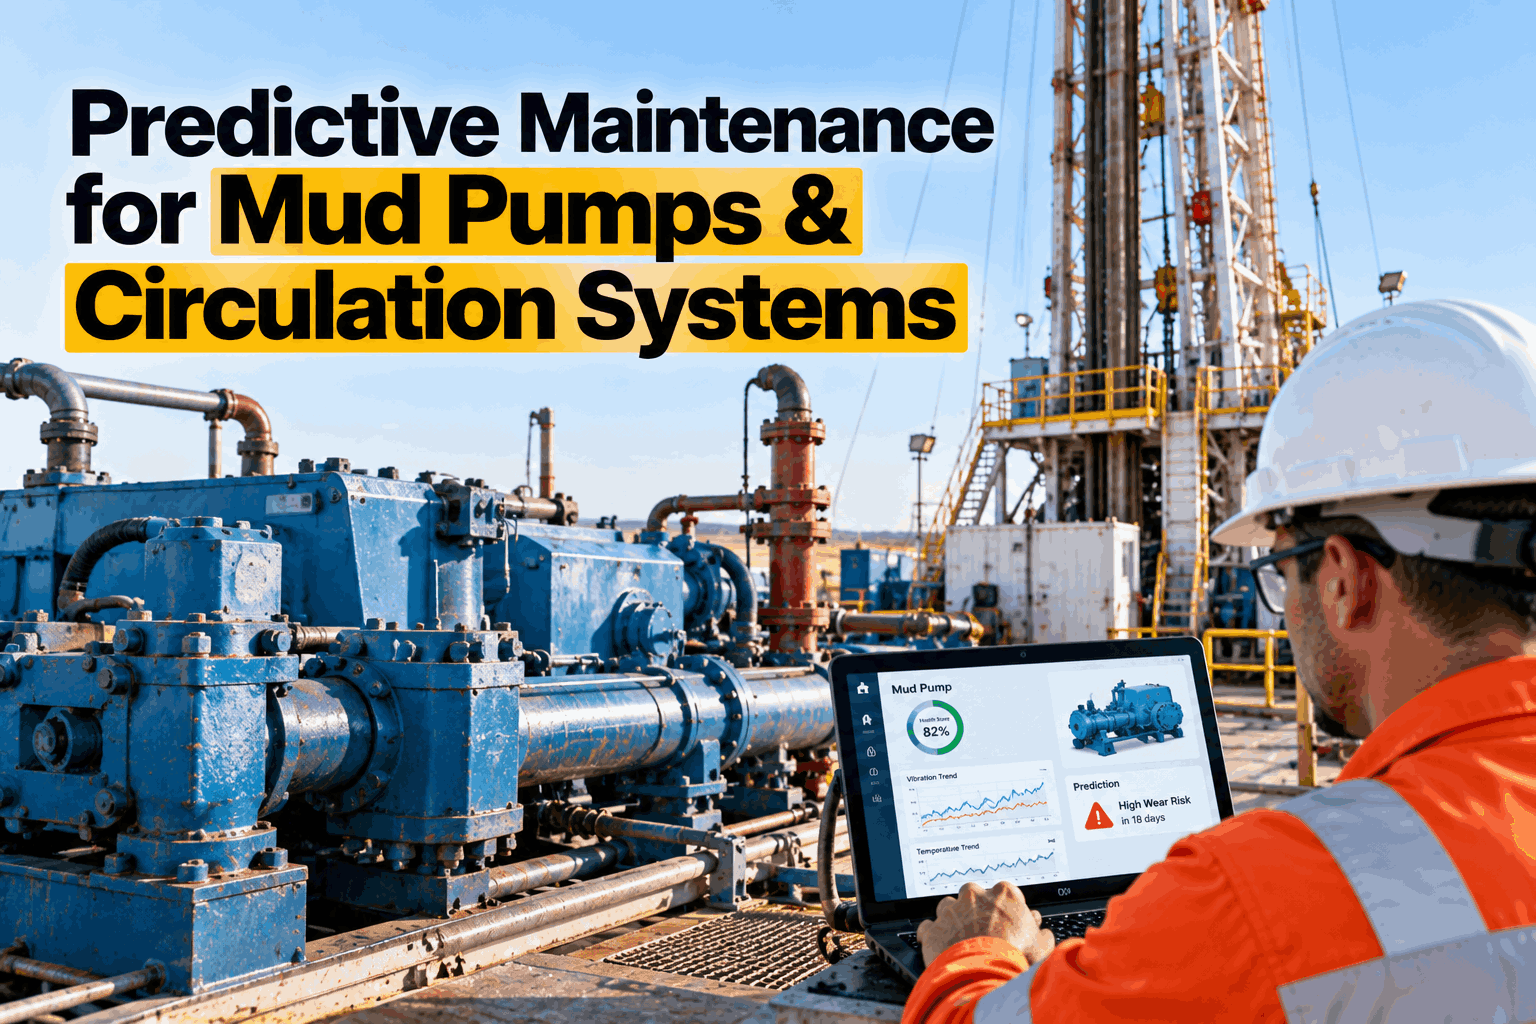
A mud pump rarely fails without notice. A valve begins to leak, a liner wears past its seal, a dampener loses its charge — and the pump says so in its vibration and pressure signature well before the driller sees standpipe pressure wander. The trouble is that nobody on the rig floor is listening at that frequency. iFactory's Predictive Maintenance Engine does: it tracks fluid-end wear cylinder by cylinder, estimates remaining life for liners, pistons and valves, and flags an active leak early enough to change the part at the next connection instead of after a washout. To see it on your own pump data, book a pump review.
Predictive Maintenance for Mud Pumps: Change the Valve Before It Cuts the Module
iFactory combines vibration on each fluid-end module with high-frequency pressure and the rig's own stroke, flow and pressure data. It names the pump, the cylinder and the part, projects how long it has left at the current duty, and tells the crew which window to use.
- Wear tracked per cylinder, per valve
- Remaining life estimated from actual duty
- Changes planned into connections and trips
Why Mud Pumps Fail at the Worst Time
The expendables in a fluid end — valves, seats, pistons and liners — are meant to wear. What turns wear into downtime is timing. A valve that starts to leak lets fluid and solids past the seat, and the erosion that follows can get much worse very quickly: left alone it cuts through the seat and into the module, turning a 40-minute valve change into a module replacement. It tends to happen under high pressure and high solids, which is to say in the hole section where losing a pump matters most. If pump failures are a regular entry in your daily drilling reports, our drilling specialists can review the pattern with you.
Changed on hours
Fixed-interval changes throw away good life on easy sections and are too late on hard ones. Duty varies too much for a calendar.
Run to failure
Waiting for the washout gets every hour from the part and gives the failure the choice of timing — and often takes the seat deck with it.
Seen late on the gauge
By the time standpipe pressure visibly fluctuates, the leak is well under way. The early signal is at frequencies the rig display does not show.
Which valve?
A triplex has six valves. Without knowing which one is leaking, the crew opens pots until they find it, with the pump off line throughout.
What Fails, and How Much Warning Each Gives
Honest lead times differ by failure mode, and a programme should be judged against the right one. Gradual wear of liners, pistons and valves can be trended and projected, which typically gives a planning horizon of 14 to 21 days for ordering parts and choosing a window. An active leak is different: once fluid is passing a seat, the useful warning is hours to a day or two — enough for the next connection, not for the next well. The figures for your pumps are confirmed during the pilot. To go through these against your own failure history, book a failure-mode session.
Bearings, crossheads, gears
Instrument One Rig's Pumps and Measure the Warning Time
Choose one rig. We fit sensors to its mud pumps, connect the rig data, and for six weeks record every alert against what the crew found when the part came out — so lead time and false alarms are measured on your pumps and your mud.
What iFactory Listens To
The idea is not new. Published work going back to 2002 showed that high-frequency pressure signatures and vibration on a triplex pump reveal wear earlier than conventional rig instruments do, and papers and patents since have refined leak detection valve by valve. What has changed is that the analysis can now run continuously on a server at the rig. Our instrumentation engineers can advise what your pumps already have and what would need adding.
From Alert to a Planned Change
An alert is worth only what the crew does with it. The value is in turning a signal into a decision the driller and the mechanic can act on without stopping to diagnose. To see this flow against your own rig routine, book a workflow session.
Detect
A change from the pump's own normal signature at the same pressure, stroke rate and mud weight.
Locate
Pump, cylinder and part: suction valve, discharge valve, or piston and liner.
Estimate
How fast it is progressing, and how long the part is likely to last at the current duty.
Plan
The best window: the next connection, a trip, a casing run. Parts and people lined up.
Confirm
The removed part is photographed and graded. The finding is fed back and the estimate improves.
Where a 40% Reduction in Pump Downtime Comes From
Predictive maintenance does not make parts last for ever. It moves changes out of drilling time and into windows that already exist, and it stops a small failure becoming a large one. The illustrative rig here loses 120 hours a year to its circulation system. Most of the saving is in valves and seats, because that is where an early call prevents the most collateral damage. At a rig rate near $400,000 a day, the 48 hours recovered are worth about $800,000 before spread costs; on a land rig the figure is far smaller and the arithmetic is the same. Our reliability engineers can run it with your own downtime log.
Beyond the Pumps: the Rest of the Circulation System
The mud pumps are the heart of the system, and the equipment around them decides how hard they work. Poor suction conditions shorten the life of everything in the fluid end; the Drilling Contractor case in which module washes fell by nearly 85% was a suction and cavitation fix, not a pump redesign. The same approach extends along the flow path.
Charge pumps and suction
Centrifugal charge pump wear, blocked strainers and aerated mud show up as low or uneven suction pressure before the mud pump begins to knock.
Dampeners and relief valves
Pulsation level tracks dampener precharge. Relief valves that lift early or weep are visible in the pressure record.
Standpipe and top drive
Washpipe packing and standpipe valves leak small before they leak large. Pressure decay tests and trends show the change.
Solids control
Shaker, centrifuge and agitator motors and bearings are monitored for the faults that let solids build up and wear the pumps faster.
What the AI Adds on the Rig
A fixed vibration alarm cannot work on a mud pump, because normal changes with every change of pressure, stroke rate and mud weight. iFactory's models learn each pump's signature across its operating range and judge the present against that. They run on a GPU server at the rig, so they keep working when the link to town is slow.
- Learns each pump. Normal is defined per pump and per operating point, not by a single threshold.
- Names the part. Signals are aligned to crank position, so an alert points to a cylinder and a valve.
- Projects remaining life. Wear rate is tied to actual duty: pressure, strokes and solids.
- Answers in plain language. The driller or mechanic asks what is wrong with a pump and gets the part, the evidence and the best window.
Delivered as a Turnkey AI System — Hardware and Software Together
iFactory ships as a complete bundle: a pre-configured NVIDIA AI server, racked and ready, with the Predictive Maintenance Engine and AI models pre-loaded, plus the sensors for your pumps. Rack it, plug in power and Ethernet, and the AI is live on the rig network — data stays on the rig and in your own systems. Our team handles sensor fitting, cabling, network setup, PLC and SCADA integration with the rig control and data systems, operator training and 24×7 remote monitoring. For a scoped proposal, book a deployment call.
Ship, network and data
Server delivered and racked. Sensors fitted to the mud pumps during a planned window. Rig data connected. Maintenance history loaded.
Model training and pilot
Models learn each pump across its operating range. Alerts begin in advisory mode, and every removed part is graded against its alert.
Go-live and training
Alerts go live for the drill crew and mechanics. Remaining-life estimates feed the parts plan. Other circulation equipment is added.
Frequently Asked Questions
How far ahead can a mud pump failure be predicted?
It depends on the failure. Wear of liners, pistons and valves can be projected as remaining life, typically giving a 14 to 21 day planning horizon. A valve that has begun to leak gives hours to a day or two. Sudden events, such as a burst dampener bladder, give none. The pilot measures the actual figures on your pumps.
What sensors are needed?
Accelerometers on each fluid-end module, fast pressure transducers on discharge and suction, and a crank position signal, together with the rig's existing pressure, flow and stroke data. Many rigs already have some of these; the first weeks show what must be added.
Can it tell which valve is leaking?
That is the aim of aligning vibration to crank position: a leak shows in the part of the stroke when a particular valve should be sealed. How reliably it separates suction from discharge valves on your pump model is confirmed against parts removed during the pilot.
Does it work across different pressures and mud weights?
Yes, and it has to. The models learn each pump's normal signature across pressure, stroke rate and mud weight, and compare like with like. A fixed alarm level would either miss faults at low duty or alarm constantly at high duty.
Is a 40% cut in downtime guaranteed?
No. It is the result of the worked example on this page, and it depends on how much of your present downtime comes from failures that give warning and on the crew acting on alerts. Your own downtime log shows what is achievable.
Does it need a connection to shore or town?
No. The analysis runs on the server at the rig. A connection is used for remote monitoring and support when it is available, and the system continues to work without it.
How long does deployment take, and what do we need to provide?
A typical rig is live in 6–12 weeks. You provide rack space, power, an Ethernet connection, access to the pumps for sensor fitting, the rig data feed, pump maintenance history and a mechanic or maintenance lead for the pilot. iFactory supplies the pre-configured NVIDIA AI server, sensors, software, integration and training. To scope your rig, contact our project team.
Hear the Leak Before the Driller Sees It
One turnkey system — NVIDIA AI server, sensors, Predictive Maintenance Engine, integration and training — delivered and live inside 12 weeks. Start with the rig that changed the most modules last year.
- 1Pump-related downtime hours, last 12 months
- 2Valves, seats, pistons and liners used
- 3Modules replaced, and why
- 4Hours achieved per part, by hole section
- 5Sensors already on the pumps