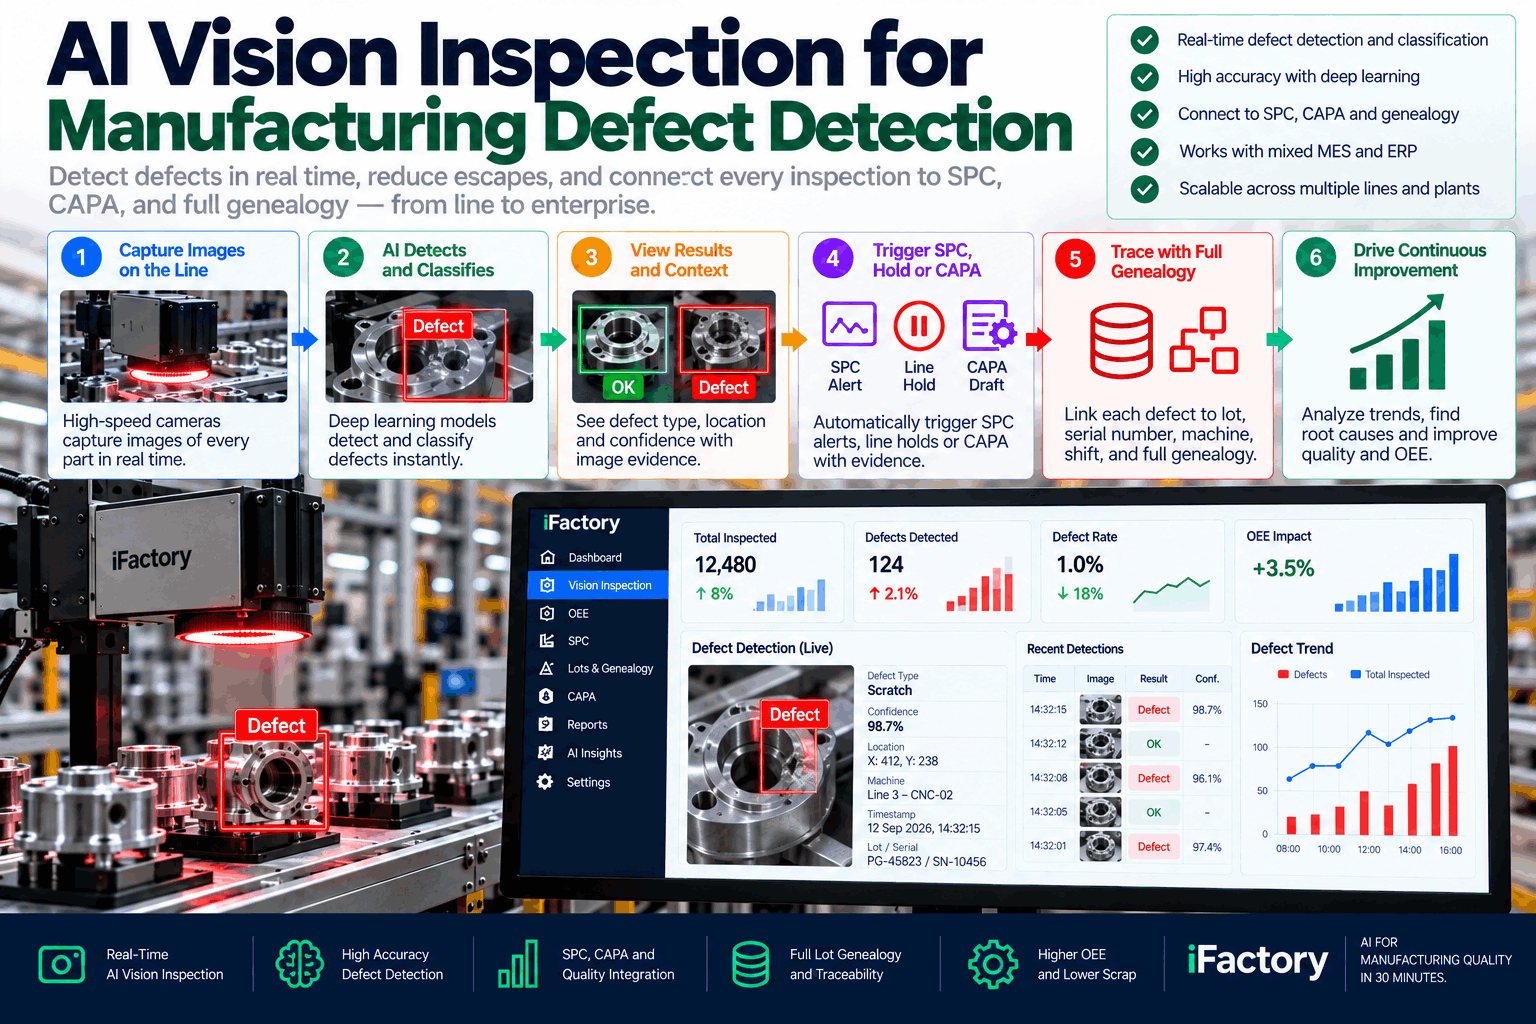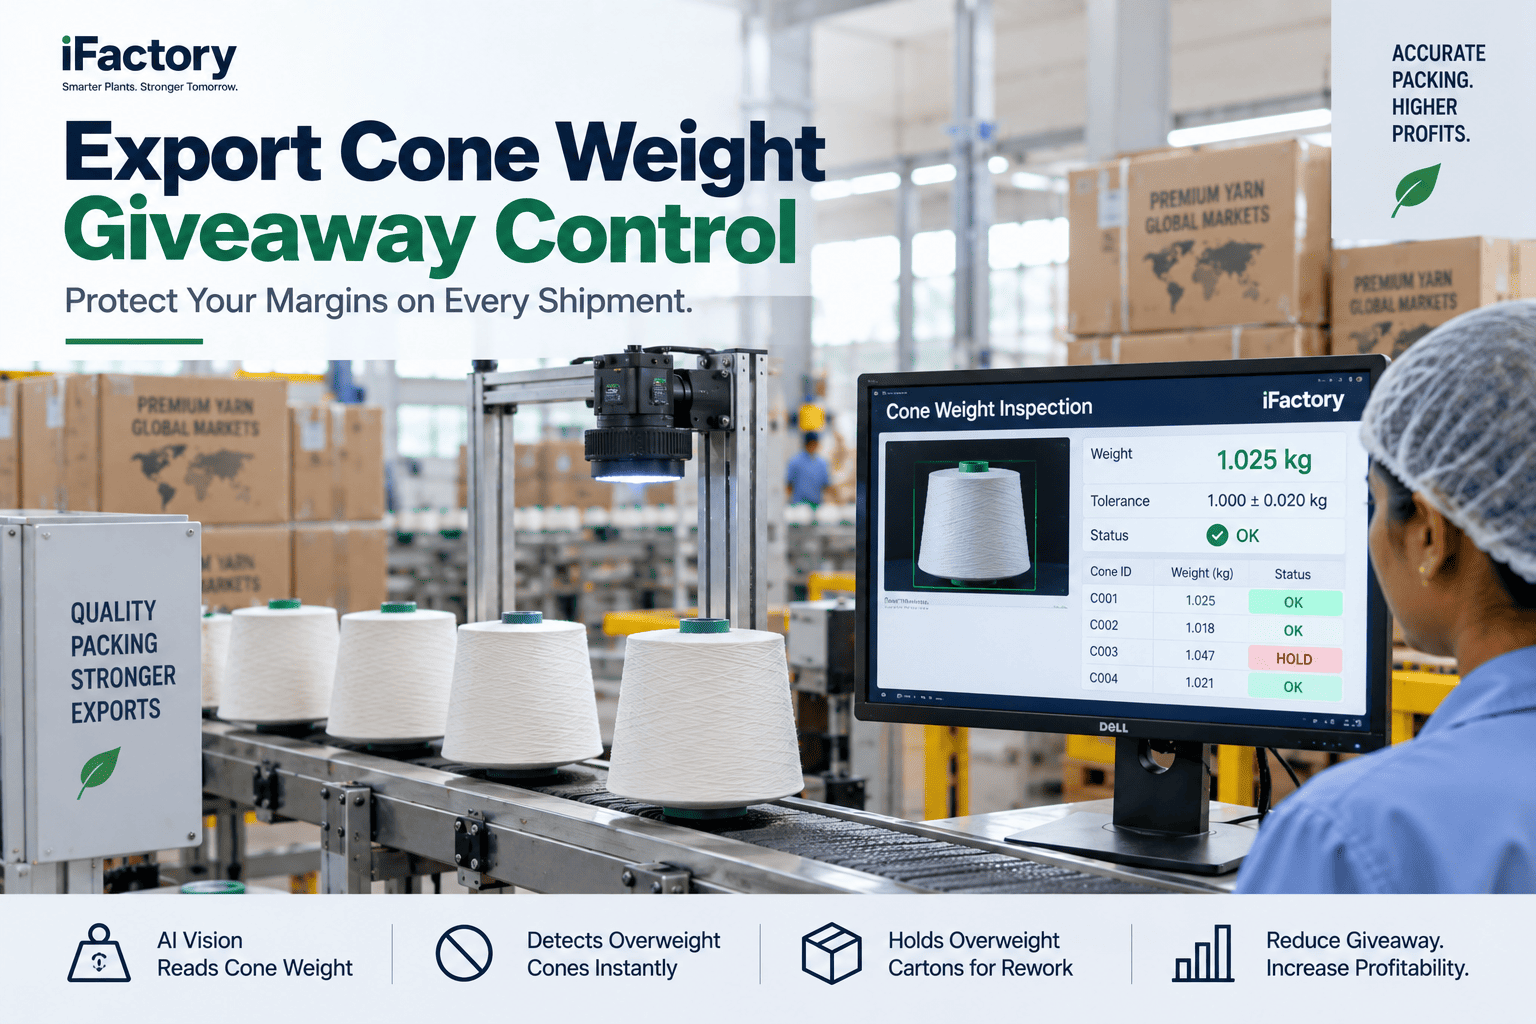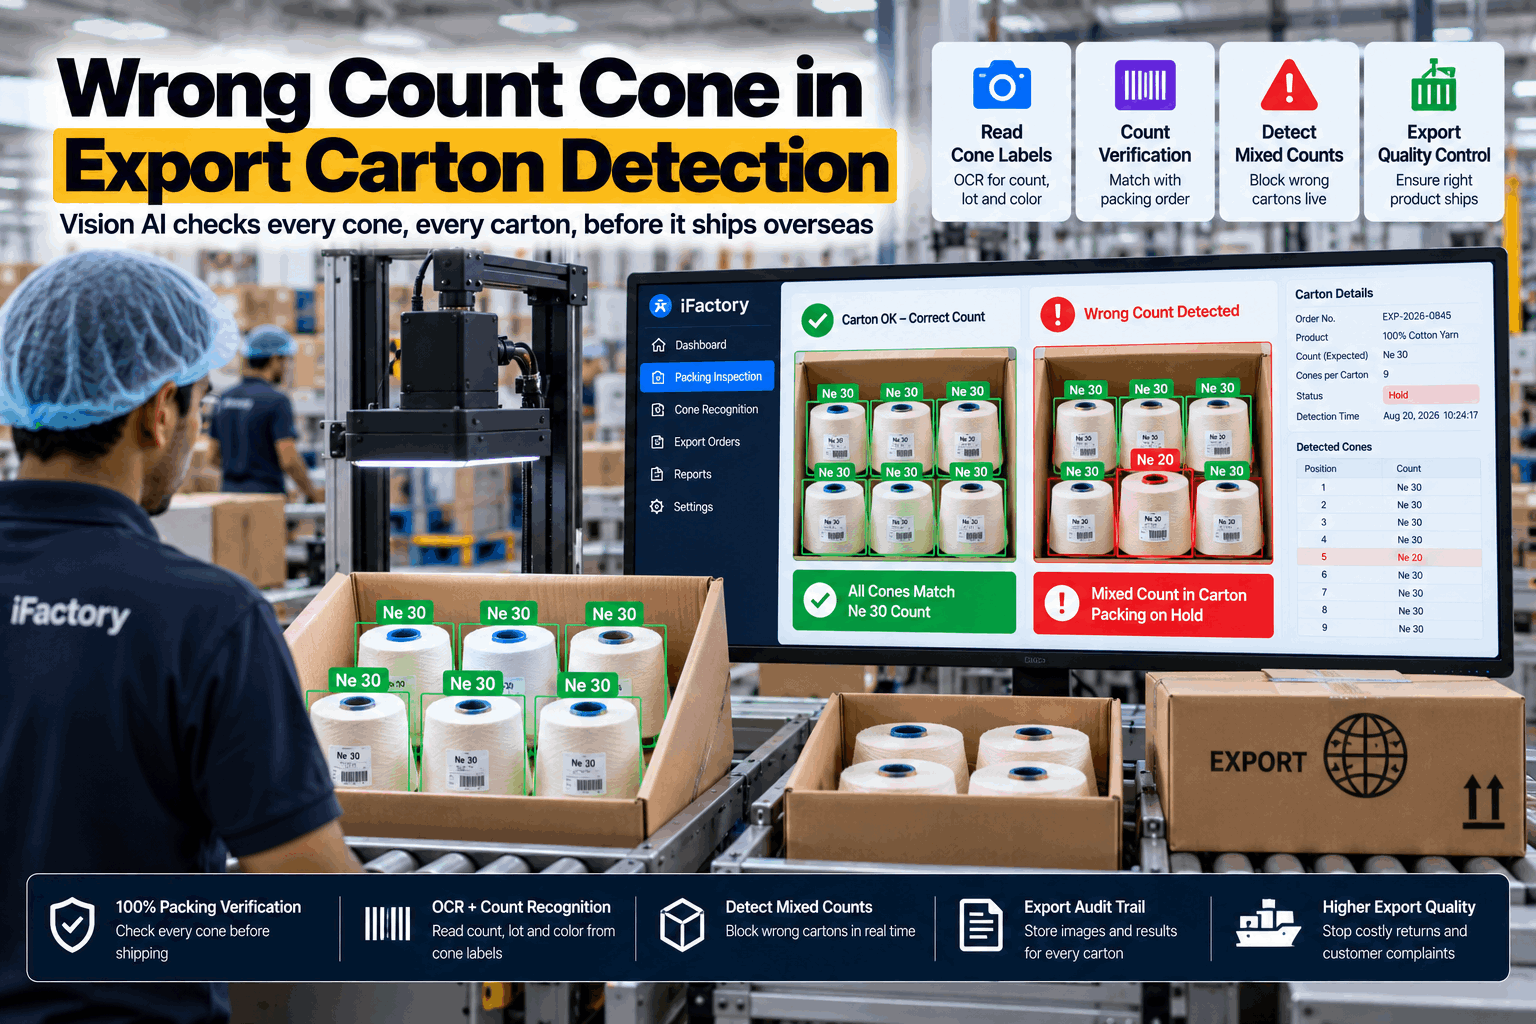
A wrong-count cone is one of the few packing errors that cannot be seen once the carton is sealed and cannot be fixed once the container has sailed. It weighs the same as its neighbours, looks the same from a metre away, and only shows itself weeks later as a stripe in a customer's dyed fabric. iFactory puts vision AI at the export packing station to read every cone's label and tip code, check a count proxy from the yarn surface, and hold the carton before it is sealed if anything disagrees with the order. To see it run on your own cones and labels, book a packing demo.
Read Every Cone Before the Carton Is Sealed — and Hold the One That Does Not Belong
Vision AI at the packing station reads the label and tip code on each cone, compares them with the export order, and checks the yarn surface against the rest of the carton. A mismatch stops the carton label from printing and shows the packer which cone to pull.
- Every cone read, not a sample of cartons
- Label, tip code and surface proxy checked together
- An image record for every carton shipped
Why One Wrong Cone Is an Export Problem, Not a Packing Problem
On a circular knitting machine each cone feeds one feeder until it runs out. A cone of the wrong count therefore knits a course of a different thickness again and again through every roll made from it — a horizontal stripe known as barré. ATIRA's guide to barré lists the mixing of yarn of different counts among its yarn-related causes. The stripe often becomes obvious only after dyeing, by which time the yarn is fabric and the fabric may be garments. For an exporter the customer is usually overseas: Bangladesh and China together took roughly 60% of India's cotton yarn exports in 2024-25. If mixed-count claims are part of your year, our textile team can review where they start.
Found late
The error is packed today and discovered after shipping, knitting and dyeing. The people and trolleys involved are long gone from memory.
Found far away
Nobody from the mill can open the remaining cartons. The customer decides how much of the lot to quarantine, and the mill pays for the caution.
Hard to bound
Was it one cone, one carton or one whole trolley? Without a per-carton record the honest answer is that the whole shipment is suspect.
Hard to answer
A claim arrives with photographs of fabric. The mill has a packing list and a test report for the lot, and nothing that shows what went into carton 187.
Six Routes a Wrong Count Takes Into the Carton
Mills already guard against count mix-ups with colour codes — training material from India's Textiles Committee describes ring bobbin colour and empty cone tip colour being displayed against the count on each machine. The codes work until the moment a person has to apply them at speed, at a changeover, at the end of a shift. These are six common routes, and what a camera at the packing station makes of each. To walk through your own packing flow, book a process review.
What "Count Proxy" Means — and What It Does Not
A camera cannot measure yarn count. Count is mass per unit length, and it is measured in the laboratory by reeling a known length and weighing it. What vision can do at packing speed is read the identifiers the mill has already put on the cone and look for physical signs that one cone is unlike the others. iFactory combines four layers of evidence, each with a known limit, and holds the carton when they disagree. Our vision engineers can explain how each layer would work with your labels and colour code.
How far the proxy goes: by the standard approximation for cotton yarn, Ne 30 is about 0.166 mm in diameter and Ne 40 about 0.143 mm, a difference a close-up camera can resolve. Ne 30 and Ne 32 differ by about 0.005 mm, which is a weak signal on its own. That is why the surface proxy is used to raise a doubt and the label and tip code are used to settle it. The same cone weight also hides a large difference in length: about 96 km of yarn at Ne 30 against about 128 km at Ne 40.
Prove It on One Export Packing Line in Six Weeks
Choose one line. We train the system on your running counts, tip codes and label formats, agree the hold action with your packing supervisor, and report every catch and every false hold each week.
At the Packing Station: Read, Match, Hold
The check sits where the cone passes anyway — over the bench, the feed chute or the conveyor — so a matching cone needs no extra action from the packer. Only a mismatch interrupts the work, and it interrupts it before the carton is closed, when pulling one cone takes seconds. To see the sequence at a station like yours, book a live session.
Order loaded
The export order is taken from your ERP or scanned from the packing slip: count, lot, tip code, cones per carton, net weight.
Each cone read
As a cone passes, cameras capture its label, its tip and a close-up of the yarn surface. Text and barcode are read from the label.
Matched to the order
Label and tip code are compared with the order, and the surface is compared with the other cones in the same carton.
Carton completed
The cone tally and the scale reading are checked against the packing specification before the carton is closed.
Release
The carton label prints with its carton number, the record is stored, and the carton moves to strapping. The packer has done nothing extra.
Hold
The carton label is withheld, a light and screen at the station show which cone and why, and the supervisor records the outcome: cone replaced, label corrected, or lot sent for a count test.
Why the Carton Audit Misses It
Most mills rely on two defences: the packer's eye and a pre-shipment audit of sample cartons. Both are reasonable and both have a ceiling. Take a 40 ft load of 450 cartons, 10,800 cones. Suppose five cartons each carry one wrong-count cone — five cones in 10,800, under 0.05%. An audit that opens 20 cartons and checks every cone in them has about a 20% chance of opening even one of the five. Four shipments in five, the audit passes and the cones sail. Our quality engineers can run the same sum for your audit plan.
The Packing Record: Evidence for Every Carton
Blocking the wrong cone is the first benefit. The second arrives months later, when a claim does come in. Every carton leaves with a record of what was read, so the conversation with the customer starts from evidence instead of memory.
- Answer a claim with facts. Pull the images and readings for the carton numbers the customer quotes, and show what was packed.
- Bound the problem. If a wrong cone is confirmed, find every carton packed from the same trolley, shift and changeover instead of recalling the whole lot.
- Trace it back. Holds are grouped by count, winder, shift and changeover, which points to the route the cones are taking.
- Show the buyer. A per-carton record is a stronger answer to a supplier audit than a signed checklist.
What the AI Adds at the Packing Line
Reading a clean barcode is not hard. Reading a small label on a curved cone, judging a tip colour under factory light and noticing that one cone's yarn looks different from the other twenty-three is where trained models earn their place. iFactory's models run on a GPU server in your mill and learn your counts, labels and colour codes from your own cones.
- Learns your codes. Each count's label layout and tip design is taught from sample cones, and a new count is added the same way.
- Reads imperfect labels. Skewed, creased or partly hidden labels are read where possible and reported as unread where not — never guessed.
- Explains each hold. The station screen shows the cone, the reading and the reason in plain words, in the packer's language.
- Answers questions. Supervisors ask about holds, cartons and orders in plain language and get the records behind the answer.
Fits Manual Benches and Conveyor Lines
Packing halls differ more than winding rooms do. The same check is fitted to the way your cones reach the carton, and the hold uses whatever your line already has — a printer, a light, a conveyor stop.
Delivered as a Turnkey AI System — Hardware and Software Together
iFactory ships as a complete bundle: a pre-configured NVIDIA AI server, racked and ready, with the vision software and AI models pre-loaded, plus the cameras and lighting for your packing stations. Rack it, plug in power and Ethernet, and the AI is live on your network — images of your cones stay in your mill. Our team handles camera mounting, cabling, network setup, PLC and SCADA integration, links to your ERP and label printers, operator training and 24×7 remote monitoring. For a scoped proposal, book a deployment call.
Ship, network and data
Server delivered and racked. Cameras and lighting fitted at the first station. Order data connected. Sample cones of each running count imaged.
Model training and pilot
Models trained on your labels, tip codes and yarn surfaces. One line runs live, first in alert-only mode, then with the hold switched on.
Go-live and training
Remaining export lines fitted. Packers, supervisors and quality staff trained. Hold rules and the carton record handed over to your team.
Frequently Asked Questions
Can a camera measure yarn count?
No. Count is measured in the laboratory by reeling and weighing. The system reads the count identifiers on each cone — label and tip code — and uses the look of the yarn surface as a supporting signal. When the signals disagree, the carton is held and the lab test decides.
What exactly is checked on each cone?
The printed text and barcode on the cone label, the colour and design of the cone tip against your colour code, and a close-up of the yarn surface compared with the rest of the carton. At carton level, the cone tally and net weight are checked against the packing specification.
What happens when a mismatch is found?
The carton label is not printed, the station shows which cone and which check failed, and a supervisor records the outcome. On conveyor lines the hold can stop or divert the cone through the PLC. Every hold is stored with its images.
Our labels are small stickers inside the cone. Can they be read?
Often, with a camera angled into the cone as it passes, but it depends on label position, print size and contrast. Camera positions are fixed during the pilot using your cones. A label that cannot be read is reported as unread, and you decide whether that holds the carton or asks the packer to confirm.
Will it slow the packing line?
A matching cone needs no action from the packer; the read happens as the cone passes. Time is spent only on holds. Throughput and the false-hold rate are measured on your line during the pilot, before the hold is switched on for every order.
Does it work for blended, dyed or synthetic yarn?
The label and tip code checks do not depend on fibre. The surface proxy is trained per yarn type, so blends and synthetics are added as their own classes. For dyed yarn, shade becomes an extra signal that helps separate lots.
How long does deployment take, and what do we need to provide?
A typical mill is live in 6–12 weeks. You provide rack space, power, an Ethernet connection, mounting points at the packing stations, your colour code and label formats, sample cones of each count and access to order data. iFactory supplies the pre-configured NVIDIA AI server, cameras, software, integration and training. To scope your packing hall, contact our deployment team.
Stop the Wrong Cone at the Bench, Not at the Customer's Dye House
One turnkey system — NVIDIA AI server, cameras, vision software, integration and training — delivered and live inside 12 weeks. Start with the export line that handles the most count changeovers.
- 1Was every cone in every carton read?
- 2Did every label match the order?
- 3Did every tip code match its label?
- 4Which cartons were held, and what was done?
- 5Can we show the customer the record?