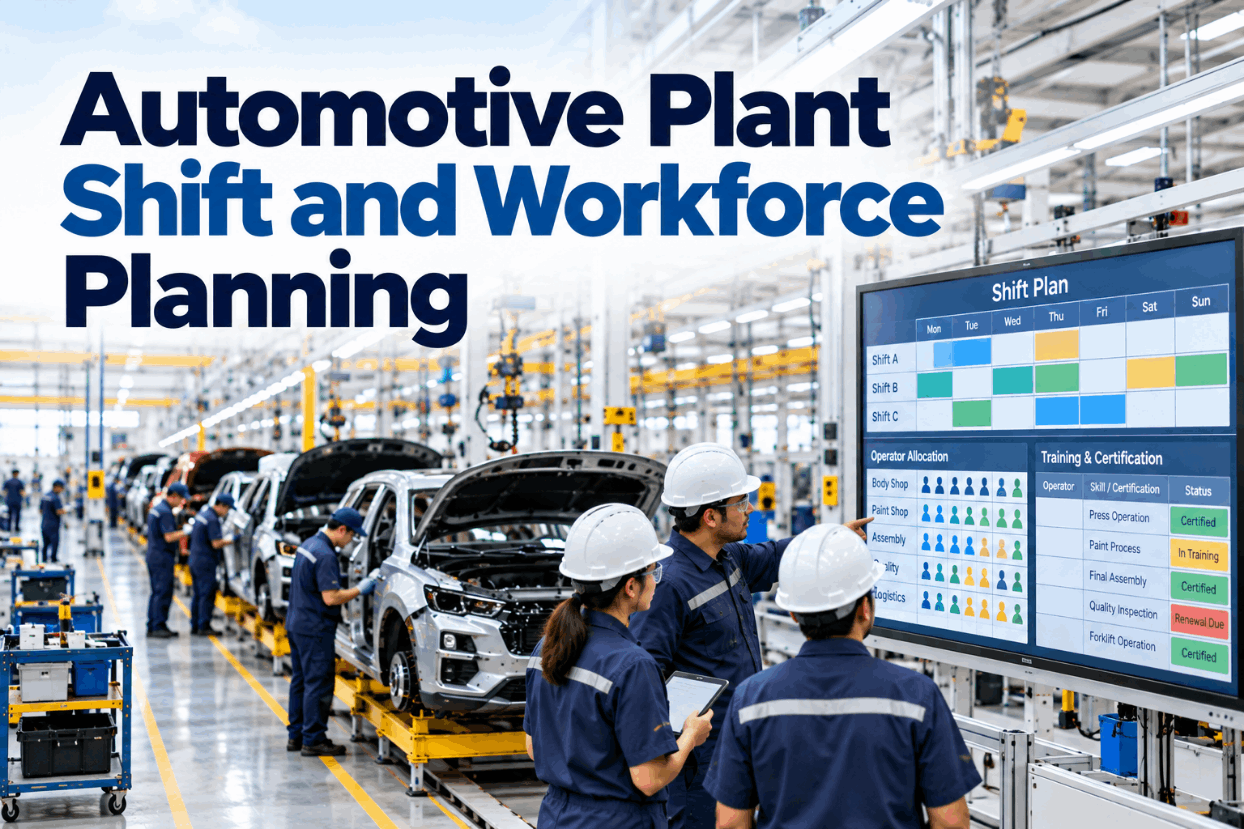
In an automotive plant, not every operator can work every station. Weld inspection, torque-critical joints, paint repair and quality gates need people who are trained, assessed and certified. Those people are a constrained resource, just like a robot or a press. When a roster puts an uncertified operator on a critical station, the plant takes a quality risk and an audit risk under IATF 16949. When it leaves a station without cover, the line slows or stops. This guide explains what IATF 16949 expects on competence, how to build and use a skill matrix, how to plan shifts around certifications, absence and training, and how to measure workforce readiness. To see skill-aware shift planning, book a short walkthrough.
Automotive Plant Shift and Workforce Planning: Roster Certified People Without IATF Risk
Shifts, training and certifications planned together, so every critical station has qualified cover, absence is absorbed and new models launch with trained crews.
Why Rosters Built on Headcount Fail
Many plants still roster by headcount: enough people per shift, allocated to lines by team leaders at the start of the shift. It works until someone is absent from a critical station, a new model needs different skills or a certification lapses. Then team leaders juggle, move people around and sometimes place operators on stations they are not qualified for, because the alternative is stopping the line.
Those moments carry real risk. A torque-critical joint done by an uncertified operator is a potential safety issue. A quality gate staffed by someone without the right training may miss defects. And an IATF 16949 auditor who finds operators on stations without evidence of competence will raise a finding. Meanwhile a stopped line is expensive: Siemens puts automotive downtime at about $2.3 million per hour in 2024.
The underlying issue is that headcount rostering treats people as interchangeable. They are not, and the roster should know it.
Planning by skills instead of headcount removes most of those moments before the shift starts. We can review your current rostering on a call.
What IATF 16949 Expects on Competence
IATF 16949 builds on ISO 9001’s competence requirements with automotive-specific additions. The main points relevant to rostering are these.
For rostering, the practical consequence is simple: the plant must be able to show that each person on a quality-relevant station was competent for it at that time. A roster linked to live qualification records provides that evidence automatically.
Auditors increasingly ask for that link between roster and qualification. We help set it up during implementation.
Building a Skill Matrix That Drives Rosters
A skill matrix records who can do what, at what level. To drive rosters, it must be current, specific to stations and tied to evidence.
| Station | Operator A | Operator B | Operator C | Operator D | Cover |
|---|---|---|---|---|---|
| Weld inspection, station 14 | Can train | Independent | Learning | Not trained | 2 qualified |
| Torque joint, station 22 | Independent | Independent | Independent | Learning | 3 qualified |
| Sealer application | Learning | Not trained | Independent | Can train | 2 qualified |
| Quality gate 3 | Independent | Not trained | Not trained | Learning | 1 qualified: risk |
Levels often follow the ILUO pattern: learning, able to work with support, fully independent and able to train others. Only independent and above count as qualified cover for rostering. The matrix should also hold expiry dates where certifications must be renewed.
The cover column is where planning starts. Any critical station with fewer than two qualified people is a single point of failure: one absence and the station is uncovered.
Agency and contract operators belong in the same matrix. IATF 16949 clause 7.2.2 explicitly includes contract or agency personnel in on-the-job training, so a temporary worker placed on a quality-relevant station needs the same evidence as a permanent one. Keeping them in a separate spreadsheet is where many audit findings start.
Linking each level to an assessment record gives auditors the evidence they need. Matrix set-up is shown in a demo.
Choosing Shift Patterns With Skills in Mind
Shift pattern choices affect not just capacity but how skills are spread across the week.
- Shifts sized by total people
- Skills spread unevenly across crews
- Night shift often thin on specialists
- Overtime used to cover skill gaps
- Rotations disrupt qualified cover
- Gaps found on the day
- Shifts sized by qualified cover per station
- Specialists spread across crews
- Every shift has cover for critical stations
- Training planned to fill thin shifts
- Rotations checked for cover before approval
- Gaps found days ahead
Balancing skills across crews often matters more than adding people. Two crews with the same headcount can have very different resilience if one holds most of the certified weld inspectors.
Working time rules shape every pattern: rest periods, maximum hours and local agreements with worker representatives. The planning system should check them automatically rather than relying on planners to remember.
Our planners can model your crews and show where skills are thin before any pattern change.
Planning Cover for Absence
Absence is predictable in aggregate even if not in detail. Plants can plan cover from their own history.
Illustrative. Floaters are only useful if they hold qualifications for the stations most likely to need cover.
The skill profile of floaters matters as much as their number. Eight floaters who can all work the same easy stations do not protect the quality gates. Floater training should target the stations with the thinnest cover.
Absence patterns also vary by day and season. Mondays, holiday periods and harvest seasons in some regions can raise absence well above average. Planning cover for those peaks avoids last-minute scrambles.
Using your own absence history by day and area makes the estimate reliable. We calculate it from your attendance data.
Scheduling Training Without Losing Output
Training takes people off the line, but skipping it leaves future gaps. The schedule has to fit both.
Stations with thin cover, expiring certifications and upcoming model changes.
Operators with related skills and availability.
Training slots in low-demand periods or with backfill.
Competence assessed and recorded before independent work.
New qualifications enter the matrix and the roster.
Cover rechecked for the coming weeks.
New model launches deserve special planning. IATF 16949 expects on-the-job training for new or modified jobs, and a launch changes many jobs at once. Training has to start weeks before the launch so crews are qualified by the first production vehicle.
Linking the training plan to the production plan shows exactly when trainees can be released. Ask our team how the two are joined.
Workforce Planning Checklist
Use this checklist to move from headcount rosters to skill-aware planning.
The most common gap is quality gates with a single qualified person. Finding them is usually the first quick win in a workforce review.
What Skill-Aware Planning Is Worth
The value of skill-aware workforce planning comes from avoided problems as much as from efficiency.
For most plants, the first benefit is visibility. Seeing that a quality gate has one qualified operator, or that the night shift has no certified weld inspector next Thursday, lets team leaders act before the problem arrives.
A short review of your matrix and rosters usually finds several such gaps. Book one with our advisors.
How iFactory Delivers Skill-Aware Workforce Planning
Station-level qualifications with evidence and expiry.
Qualified cover calculated for every station and shift.
Assignments that respect skills and working time rules.
Floater pools sized and trained from your history.
Sessions timed to launches, expiries and demand.
Who worked where, and their qualification at the time.
It works with your HR, time and attendance, MES and training systems. Share a skill matrix and roster and we will show the gaps in a session.
Find the Stations Running on One Qualified Person
Share your skill matrix, rosters and absence history. We map qualified cover for every critical station and shift and show where gaps and training needs sit.
Station 14 weld inspection has only one certified operator on the roster, and she is on leave. Two operators are one assessment away from certification.
A Cover Gap Found Before the Shift
This exchange shows how a shift manager might use iFactory.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the workforce planning and skill analytics models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensors and data connections across body, paint, assembly and quality areas, PLC/SCADA, MES, CMMS and ERP integration, cabling and network setup, operator and quality team training, and 24×7 remote monitoring.
Server installed, PLC, MES and ERP links live, historical production, quality and maintenance data loaded.
Models calibrated on your own lines, then run in advisory mode on one line or area with your planners and engineers reviewing every output.
Rollout to the agreed lines under your change management, planner, supervisor and engineer training, and 24×7 remote monitoring in place.
Software, server and integration come as one package. For pricing on your plant, contact our sales team.
Frequently Asked Questions
It requires the organization to determine and ensure competence for work affecting quality, maintain a process for training needs, provide on-the-job training for new or modified jobs, and keep evidence of competence.
A record of which operators can work which stations and at what level, often using ILUO-style levels from learning to able to train others, with evidence and expiry dates.
Common practice is at least two qualified people per critical station per shift, so one absence does not leave the station uncovered.
Estimate expected absence from your own history, size a floater pool accordingly and train floaters on the stations most likely to need cover.
Plan training into low-demand periods or with backfill, start launch training weeks ahead and record assessments before independent work.
A first area can usually be running within a 6–12 week rollout, starting with the skill matrix and cover checks. Plan it with our planners.
Put a Qualified Person on Every Critical Station, Every Shift
iFactory plans rosters from skills, certifications and absence history, flags gaps days ahead and keeps the evidence auditors ask for, so quality and output stay protected.
Illustrative. Share of shifts where every critical station has at least two certified operators.