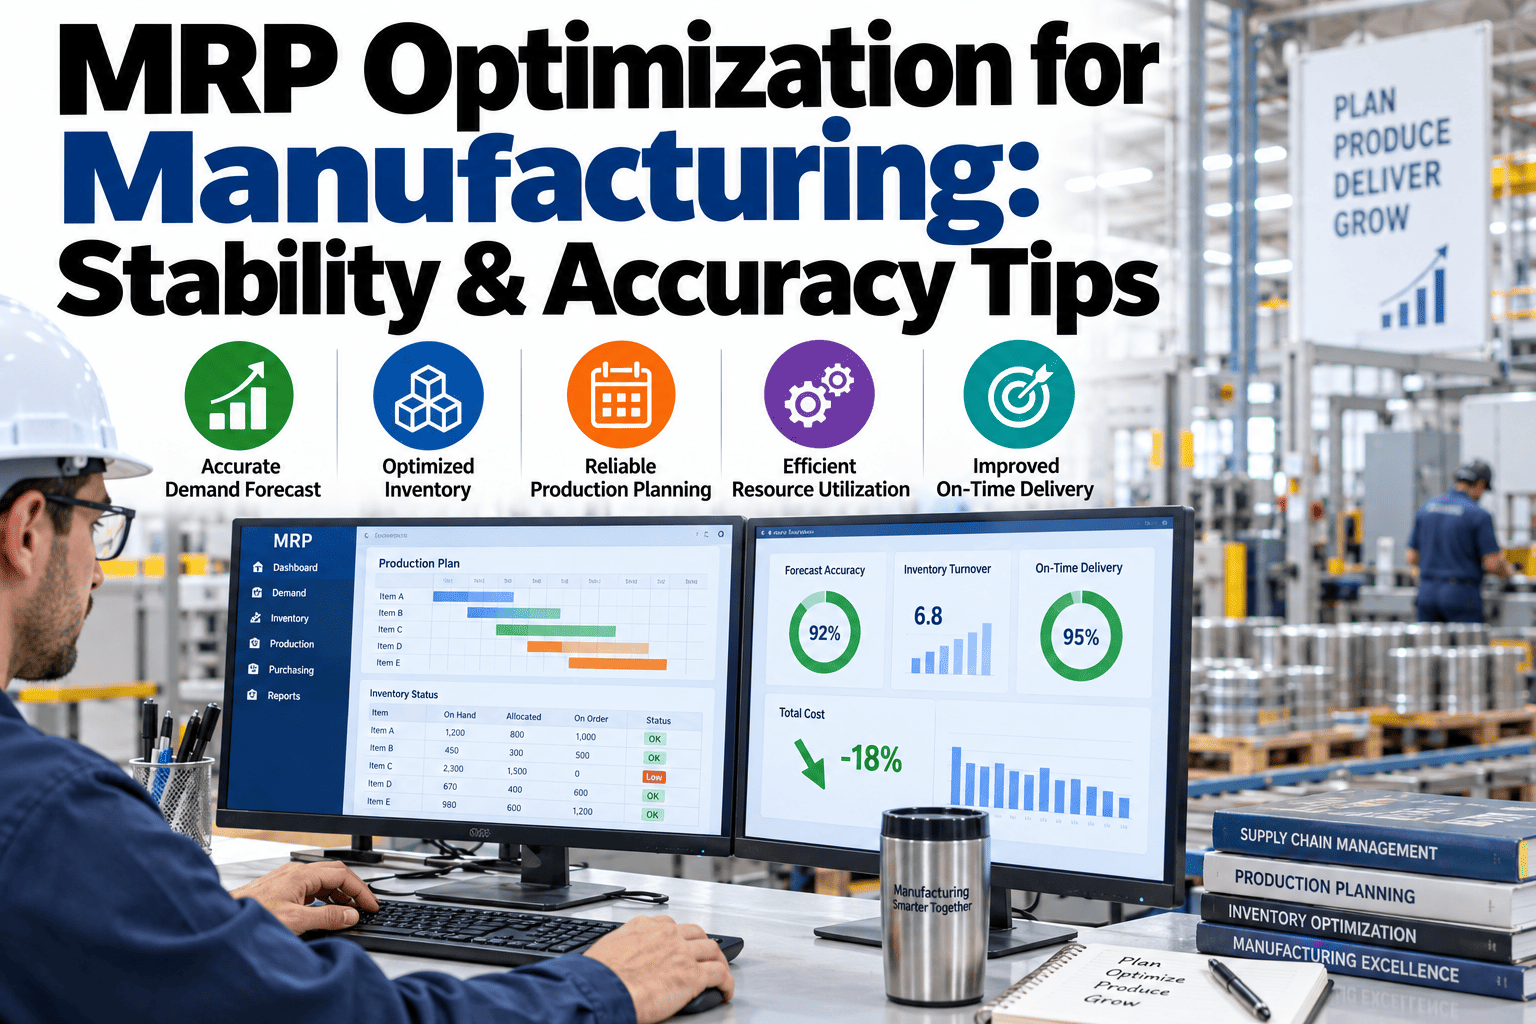
An MRP run that produces a different set of purchase orders every week isn't giving planners more accuracy, it's giving them more noise to chase. Nervousness — the tendency for small input changes to trigger large, repeated swings in planned order quantities and dates — is one of the most common reasons purchasing teams stop trusting their MRP output and start managing supply by spreadsheet instead. The fix rarely requires new software, it requires tuning the lot sizing rules, safety stock levels, and time fences that were often left at default values when the system was first implemented. This guide covers what actually drives planning stability and where accuracy gets lost between the calculation and the purchase order, and you can book a demo to see how iFactory tracks planning parameter performance against real order history.
Stop Re-Planning the Same Order Five Times Before It Ever Ships
iFactory connects lot sizing rules, safety stock levels, and actual order history in one view, so planners can see exactly which parameters are generating nervous, unreliable output before suppliers ever see the changes.
MRP Nervousness Isn't a Software Bug, It's a Parameter Problem
Most MRP engines recalculate net requirements every time the system runs, and by design, even a small change in forecast, on-hand inventory, or an open order status can ripple through the bill of materials and shift dozens of downstream planned orders. That behavior is expected. What turns it into a real problem is planning parameters that amplify the ripple instead of absorbing it, so a minor demand adjustment on a finished good turns into repeated date and quantity changes on purchase orders several levels down the structure.
A lot sizing method chosen for a stable, high-volume item but applied to an intermittent, low-volume one will generate erratic order quantities every time demand shifts even slightly.
Safety stock levels copied from a similar part number or left at a system default rarely reflect the actual demand and supply variability of the specific item.
Without a frozen or firm planning zone close to the current date, the system will happily rewrite orders that are already committed to a supplier or already in production.
A planning lead time that's shorter or longer than what a supplier or work center actually delivers throws off the timing of every downstream planned order calculated from it.
The Lot Sizing Rule You Pick Shapes Every Order the System Generates
Lot sizing determines how MRP converts net requirements into actual order quantities, and the method that works well for one item can create unnecessary volatility for another. Matching the rule to the item's demand pattern, cost structure, and supplier constraints is one of the highest-leverage adjustments a planning team can make.
| Method | How It Works | Best Fit | Trade-Off |
|---|---|---|---|
| Lot-for-Lot | Orders exactly what's needed for each period, no more | Expensive, low-volume, or highly variable items | Generates frequent small orders and higher ordering frequency |
| Fixed Order Quantity | Always orders the same predetermined quantity | Items with a fixed supplier minimum or container size | Can leave excess or shortfall if demand doesn't match the fixed amount |
| Economic Order Quantity | Calculates the quantity that minimizes combined ordering and carrying cost | Stable, high-volume items with predictable demand | Less responsive to sudden demand shifts than lot-for-lot |
| Period Order Quantity | Groups net requirements to cover a fixed number of future periods | Items with moderate, somewhat lumpy demand | Order size still swings with whatever demand falls in that period |
| Min-Max | Triggers a replenishment order once inventory falls below a set minimum | Low-value, high-frequency items where simplicity matters more than optimization | Tends to carry more average inventory than demand-driven methods |
Safety Stock Is a Balance, Not a Default Number
Safety stock exists to absorb the variability that MRP's own math can't predict, whether that's a supplier running late or a forecast that misses actual demand. The problem is that safety stock gets treated as a one-time setup value far more often than it gets revisited, even as demand patterns, supplier reliability, and lead times change underneath it.
Every minor supplier delay or demand spike turns into an expedite request, since there's no buffer to absorb normal variability before it becomes a shortage.
Planners lose confidence in the system and start manually padding quantities, which defeats the purpose of having a calculated safety stock value in the first place.
Production schedules become vulnerable to a single missed delivery, increasing the risk of a line stoppage over a routine supply fluctuation.
Carrying costs rise across the item's entire life, and for components with a shelf life or engineering revision risk, excess buffer can turn into scrap.
Warehouse space and cash get tied up in inventory that exists to cover a variability level that may no longer reflect current supplier performance.
Inflated buffers can mask a genuinely unreliable supplier, since the safety stock absorbs the lateness instead of surfacing it as a performance issue to address.
Time Fences Stop the System From Rewriting Orders Already in Motion
A time fence is a boundary in the planning horizon that limits how freely MRP can change orders as they get closer to their due date. Without one, the system treats an order due next week exactly the same as one due six months out, which means a forecast tweak today can rewrite a purchase order a supplier is already building against.
Covers the immediate near-term horizon, typically matching the supplier or shop floor lead time, where no automatic changes are allowed regardless of new demand signals.
Allows changes, but only with a planner reviewing and approving them manually rather than letting the system push updates straight to a supplier automatically.
Changes flow through with a lighter review step, useful for items where moderate flexibility is acceptable without full manual sign-off on every adjustment.
The far end of the planning horizon where full automatic replanning is appropriate, since orders here aren't yet committed to a supplier or a production slot.
Parameter Mistakes That Quietly Erode Trust in MRP Output
Lot sizing and safety stock settings entered during a system go-live years ago rarely get revisited even as demand volume, mix, and supplier lead times shift substantially.
Using the same lot sizing method and safety stock logic for both high-volume runners and low-volume specials ignores how differently those items actually behave in demand.
Planning lead times that no longer match actual supplier or work center performance throw off every downstream date calculation, even when lot sizing and safety stock are well tuned.
Items with short lead times and frequent demand changes are exactly the ones most likely to need a frozen zone, yet they're often the ones left fully open to replanning.
Cutting Purchase Order Reissues on a High-Mix Component Family
A fabricated metal parts supplier to a mid-size manufacturer was receiving revised purchase order dates and quantities on the same line item multiple times before the order ever shipped. The buying team had inherited the MRP parameters from a prior planner and had never reviewed lot sizing or safety stock settings against current demand volatility for that component family.
Switching the affected items from a fixed order quantity to a period order quantity method, adding a firm time fence matching the supplier's actual lead time, and recalculating safety stock based on the last twelve months of demand variability cut order reissues on that family by more than half within two planning cycles, and the supplier began holding tighter delivery windows once the orders stopped changing.
Building an MRP Program That Planners and Suppliers Both Trust
Review lot sizing rules by item family rather than assuming one method fits your entire item master, starting with your highest-volume and most volatile parts first.
Recalculate safety stock against recent demand and supplier lead time variability instead of leaving it at a value set during initial implementation.
Set a frozen or firm time fence on items close to their lead time so committed orders stop getting rewritten by minor upstream forecast changes.
Audit planning lead times against actual supplier and work center performance on a regular cycle, since drift here undermines every other parameter.