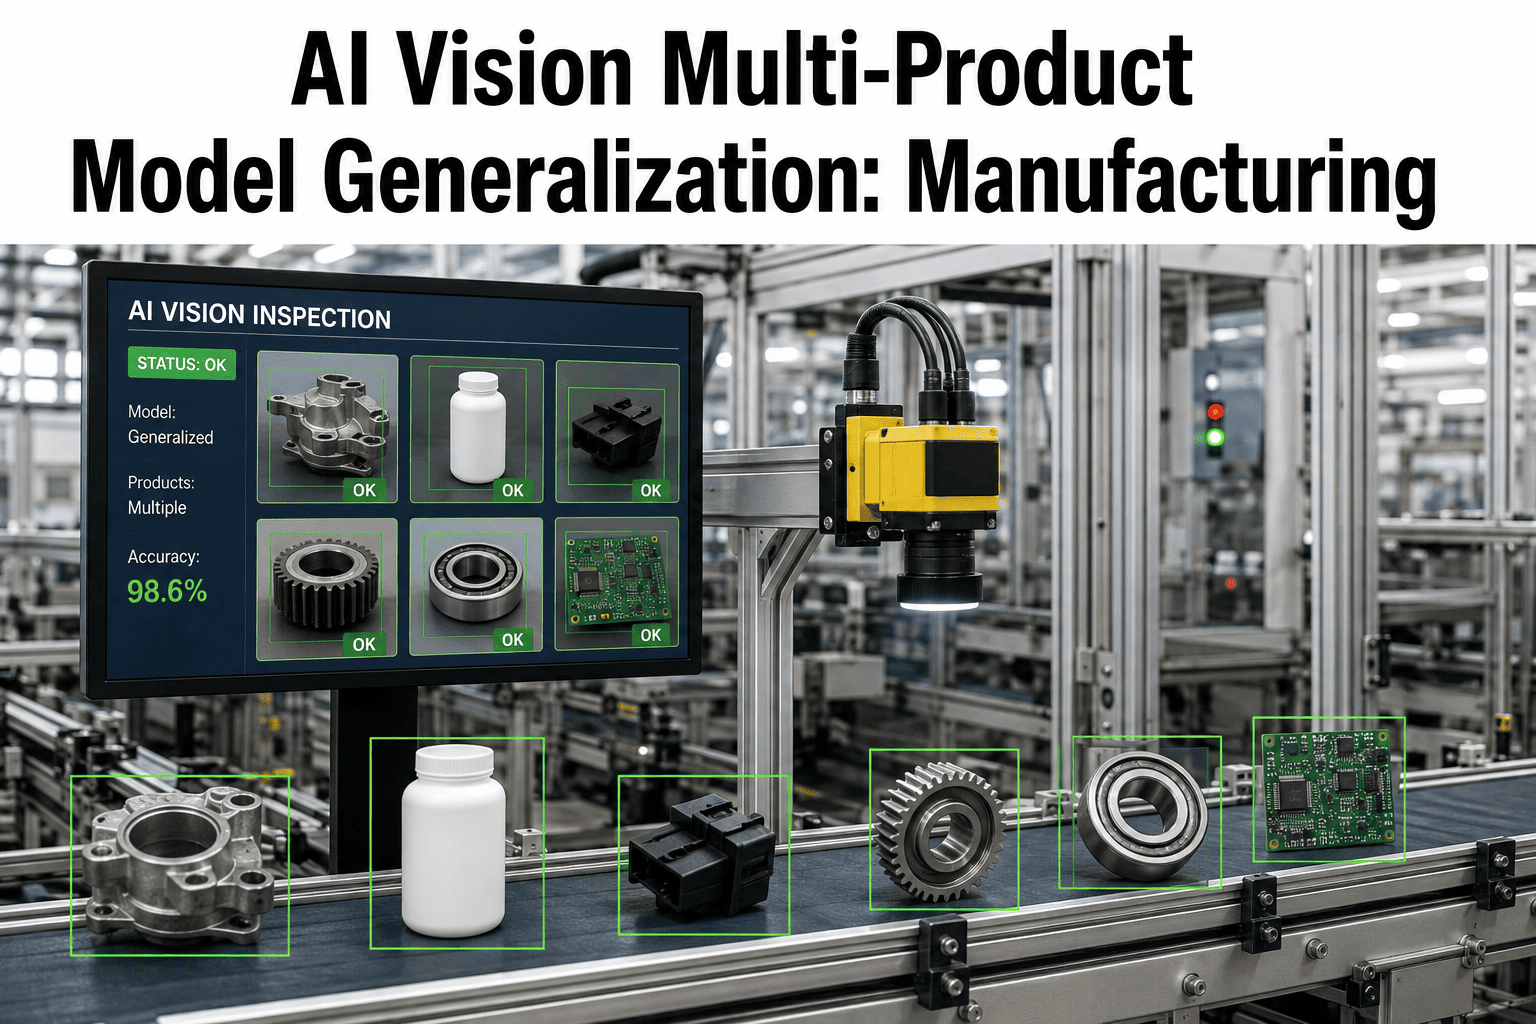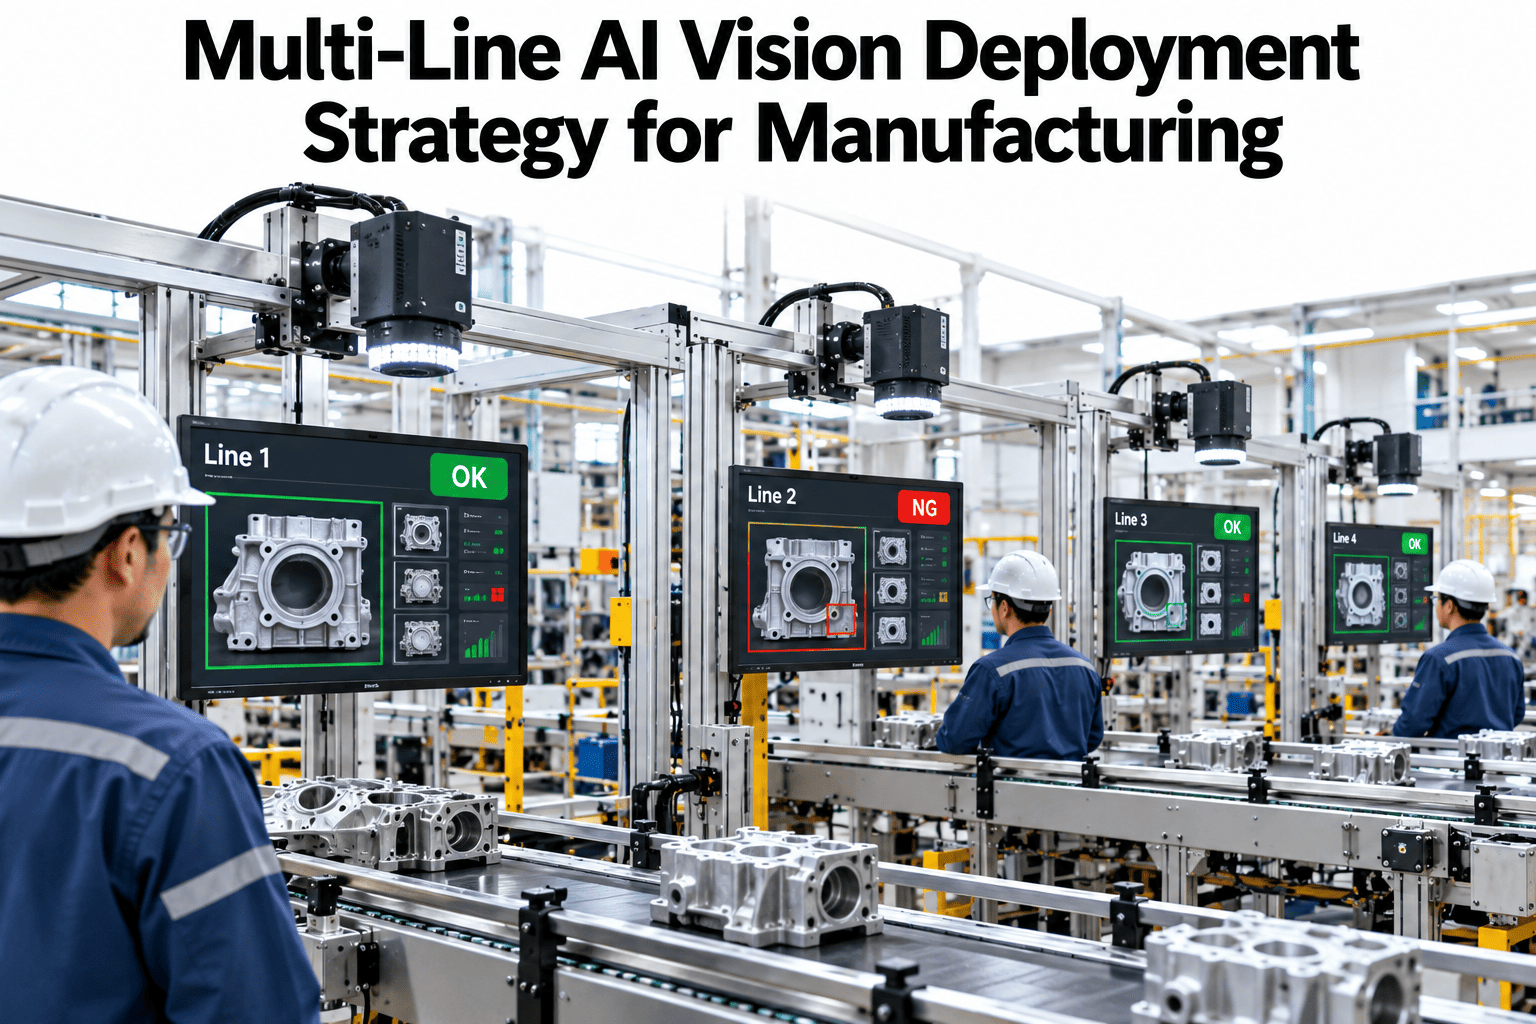
The first AI vision line is a project, but the second is a test of whether the first one can be copied. Plants that pick lines at random and rebuild each setup end up with a pile of one-off systems. A clear order and a shared kit keep the rollout moving. See how iFactory AI plans a multi-line vision rollout for your plant.
Pick the Right Lines, Then Copy What Works
iFactory AI helps manufacturers score every line, sequence the rollout in waves and reuse one proven kit, so each new line goes live faster than the last.
Why the Second Line Is Harder Than the First
A pilot proves that something can work under set conditions. A rollout has to work under many conditions at once, and the gap between the two is the point at which most programs slow down.
A strong pilot
One line, one product, one team that wants it to work.
A quick copy
The same model goes onto line two, with a different light and angle.
Results slip
False alarms rise and the new team starts to distrust the system.
One-off fixes
Each line is tuned by hand, so no two behave the same way.
Another common finding is that knowledge stays local. Gains reached in one plant seldom travel, so the aim is a process in which every successful deployment makes the next one easier.
Score Every Line Before You Commit
A short scorecard stops the loudest request deciding the order. Rate each line on a scale of one to five on the six questions below, then rank them.
| Criterion | The question | A high score looks like | A low score looks like |
|---|---|---|---|
| Defect value | How costly is a miss on this line? | Frequent, costly defects with clear rules | Rare issues with unclear standards |
| Product match | Does it look like a line already done? | Same product family and surface | New materials and finishes |
| Camera access | Can we mount a camera at the right spot? | Clear view, power and network nearby | Tight space, vibration or heat |
| Line steadiness | Does the process run in a steady way? | Few changeovers and steady speed | Constant changes and manual rework |
| Data on hand | Do we have images and labelled defects? | Saved images and agreed defect names | No history and no shared names |
| Team readiness | Will the line team own it? | A named lead and a quality partner | Nobody has time or interest |
Run the scoring as a group exercise. Put quality, maintenance, production and IT in one room, and ask each to score the same lines. Differences in scores often reveal facts that nobody had shared, such as a camera view blocked by a new guard, or a line that is about to be rebuilt.
Three Waves, Not One Big Launch
Sequence the lines by how much they teach you, not only by how much they pay. Each wave has a different job.
One or two lines
Pick high-value lines with a willing team. Build the kit, the defect list and the review habit here.
Twin lines first
Take lines with the same product and similar layout. Measure how little tuning each one needs.
Different lines
Add new products, speeds and materials, using the template and a tuning checklist.
Rank Your Lines With Us
Book a 30-minute session and iFactory AI will walk through a line scorecard, a wave map and a shared camera kit for your plant.
What You Copy and What You Tune
The biggest saving in a rollout is knowing which parts never change. Copy those exactly, and spend your effort on the few that do.
Keep a short change log for every line. When someone moves a light, swaps a lens or edits a threshold, write it down with a date and a reason. The log turns a mystery slump in results into a quick check, and it shows which local tweaks deserve to become part of the standard kit for every line.
One Camera Kit for Every Line
A kit sheet turns a one-off install into one you can run again and again. Write it once, test it on Wave 1 and then hold every new line to it.
Camera and lens
One approved model per job type, with a spare held on site.
Light and shield
Fixed light type and a shield against ambient glare and shift changes.
Mount and angle
A drawing with distance, tilt and a marker so any fitter gets the same view.
Compute and network
Edge inference at the line, with clear rules for power and cabling.
Data Needs, Line by Line
Every line needs its own images, even when the model is shared. The difference is how many, and how fast you can gather them.
Good parts
Normal product under normal light, across shifts and operators.
Known defects
Real examples of each named defect, labelled by one trusted reviewer.
Edge cases
Glare, dust, new batches and odd orientations that cause false alarms.
Line context
Speed, product code, shift and batch, stored beside every image.
Lighting and Position: The Two Biggest Differences
Most failed copies trace back to two things, how the part is lit and the spot the camera sits in. Check these before blaming the model.
Ambient light
Windows, skylights and neighbouring lines change the picture across the day.
Surface glare
Shiny film, metal or wet product reflects light and hides real defects.
Camera angle
A few degrees of tilt change what the model sees and what it ignores.
Line speed
Faster lines need tighter trigger timing and a shorter exposure.
Build Trust in Three Steps
A new line should earn the right to act. Start with the system watching, then alerting with a person in the loop, and only then acting on its own. Operators who can see the system be right are far more willing to rely on it.
Video evidence helps at each step. A short clip of a caught defect, or a missed one, settles an argument faster than a chart, and it shows operators that the system and the quality team are working on the same side.
Model Strategy: Share a Base, Tune the Edges
There are three ways to handle models across lines. The middle path usually wins, because it saves retraining without ignoring local differences.
Six Traps That Slow a Rollout
Model as the deliverable
A model with no home for its output is a demo. Plan a destination for results.
Vision data in a silo
Keep results beside quality, production and ERP data so teams can use them.
Waiting for perfect data
Ship with what you have and improve it as the line runs.
IT-only ownership
If plants cannot shape their own use cases, each one turns into a custom build.
Cloud round trips
Time-critical calls belong at the edge, close to the line.
Skipping the people side
Training and open communication decide whether operators accept the system.
Taking It Across Plants
When the rollout crosses plant boundaries, new questions appear. Decide them early, because they are far harder to change after several sites are live.
The Cost of Each New Line Should Fall
If line five costs as much effort as line one, the kit is not working. A healthy rollout shows a falling curve, because the camera kit, the defect list and the review habit are reused.
A Worked Ranking Example
Here is how a scorecard might rank six lines in one plant. The top two form Wave 1, the next two follow as twins, and the rest wait until the kit is proven.
Six Questions to Ask Any Vendor
Who Owns What
Programs stall when the platform sits only in IT, or only in one plant. Share the work, and name an owner for each piece.
Before Each New Line Goes Live
Run the same readiness check every time. The boxes are clickable.
Measures That Show the Rollout Is Healthy
Pick a small set and review it at the same time every week. A rollout that is measured by line, not only by plant average, shows problems while they are still small.
| Measure | What it shows | Review rhythm |
|---|---|---|
| Time to go live | Whether each line is faster than the last | Each line |
| False alarm rate | Whether operators can trust the alerts | Weekly |
| Escape rate | Defects the system missed and people caught | Weekly |
| Tuning hours | How far a line departs off the standard kit | Each line |
| Model version match | Whether lines run the release they should | Monthly |
| Operator override rate | How often people overrule the system | Weekly |
How iFactory AI Supports a Multi-Line Rollout
iFactory AI brings the scorecard, the kit and the model releases into one place, so line ten looks like line two and not like a new project.
Multi-camera vision
Several camera views per line feed one inspection result and one record.
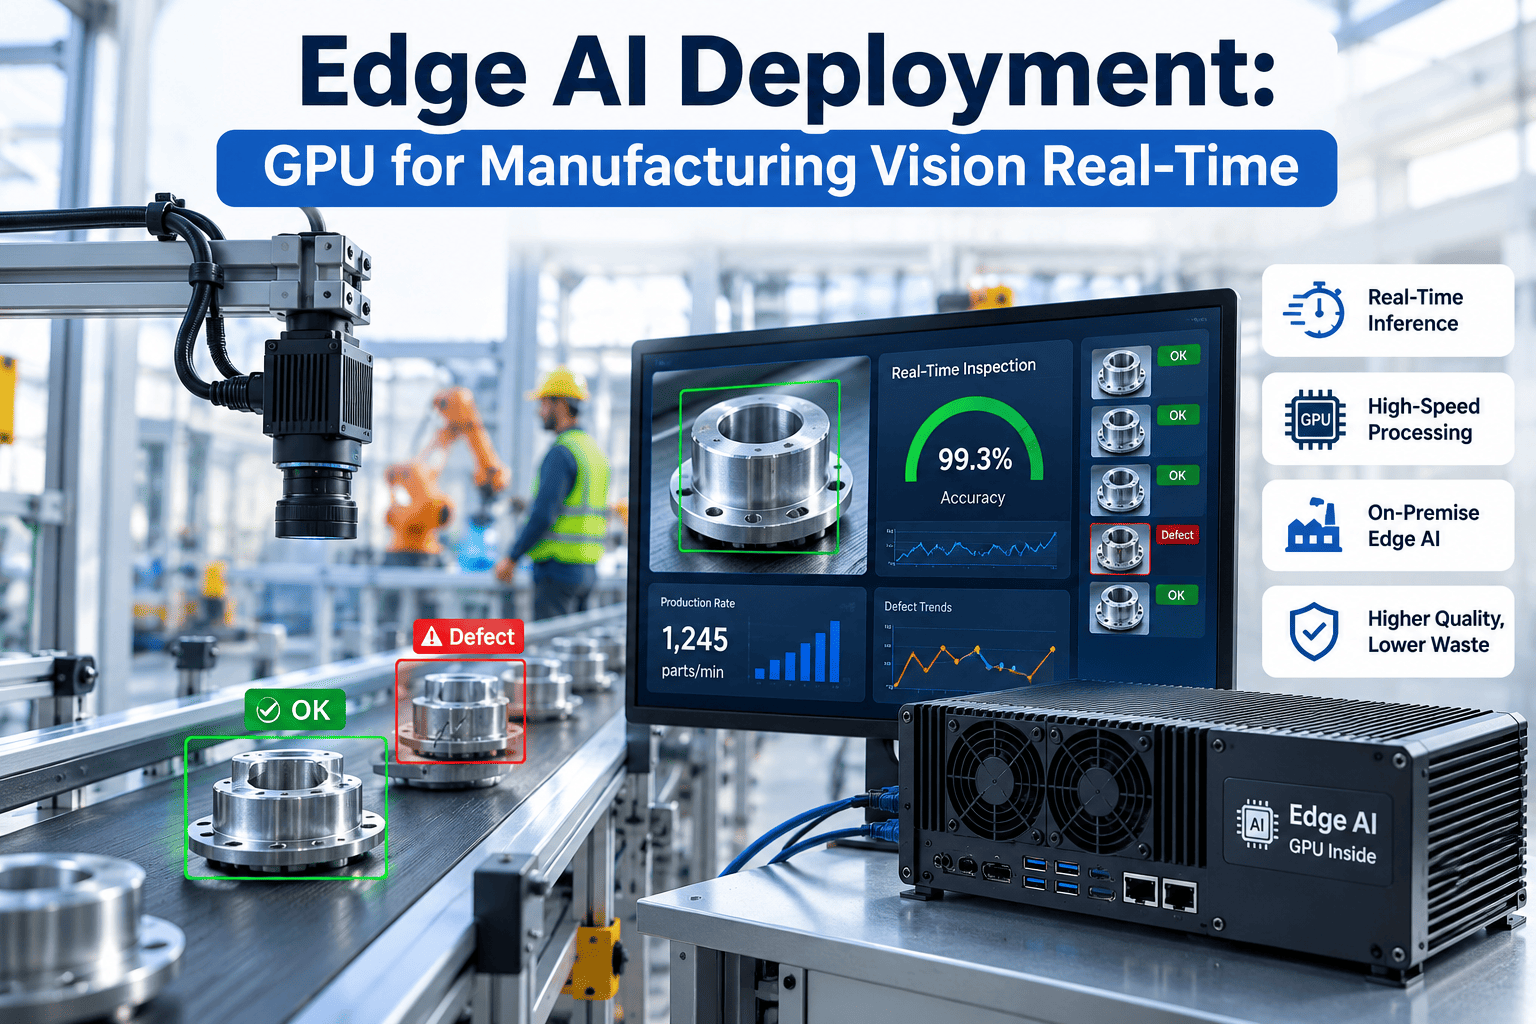
Edge inference
Models run at the line on an NVIDIA server, so decisions do not wait on the cloud.
Cross-line view
Compare false alarms, escapes and model versions across lines on one screen.
Operator feedback
People flag false alarms in one tap and the images feed later releases.
Plant system links
Results connect to PLC, SCADA, ERP and MES so action follows detection.
Reusable setup
Camera kit, defect list and alert rules copy to the next line as a template.
A 90-Day Starting Plan
The plan below covers the first wave. Later waves repeat the same four steps in less time, as the kit, the defect list and the review habit are reused.
Score the lines
Rate every line on the six questions and agree the wave order.
Build the kit
Fit Wave 1, write the kit sheet and name the defects.
Run in shadow
Compare the system with people, tune thresholds and log every change.
Go live and copy
Switch on alerts, review results and start Wave 2 with the template.
Frequently Asked Questions
How many lines should the first wave include?
Usually one or two, chosen for value and a willing team. The goal is to prove the kit and the review habit, not to cover the plant. Book a demo to size your first wave with the team.
Can one model run on every line?
Sometimes, for near-identical lines. Most plants do better with a shared base and a small local tune for light, speed and product. Book a demo to see shared and tuned models, or ask support a technical question.
What if our lines make very different products?
Group lines by similarity and start with the closest pairs. Different products can still share the camera kit, defect rules and review habit. Book a demo and bring your line mix so we can map the groups.
How do we keep results consistent across lines?
Hold every line to the same kit sheet, defect names and alert rules, and watch false alarms and escapes by line. A cross-line view makes drift easy to spot. Book a demo of the cross-line view on sample data.
How long does a full rollout take?
The turnkey build for the first lines runs 6–12 weeks. Later waves move faster when the kit is reused, but the total depends on how many lines you have. Book a demo to build a timeline for your plant.
Roll Out Vision Once, Then Repeat
iFactory AI gives manufacturers a scored line order, a reusable kit and a clear view across every line. Book a walkthrough for your plant.