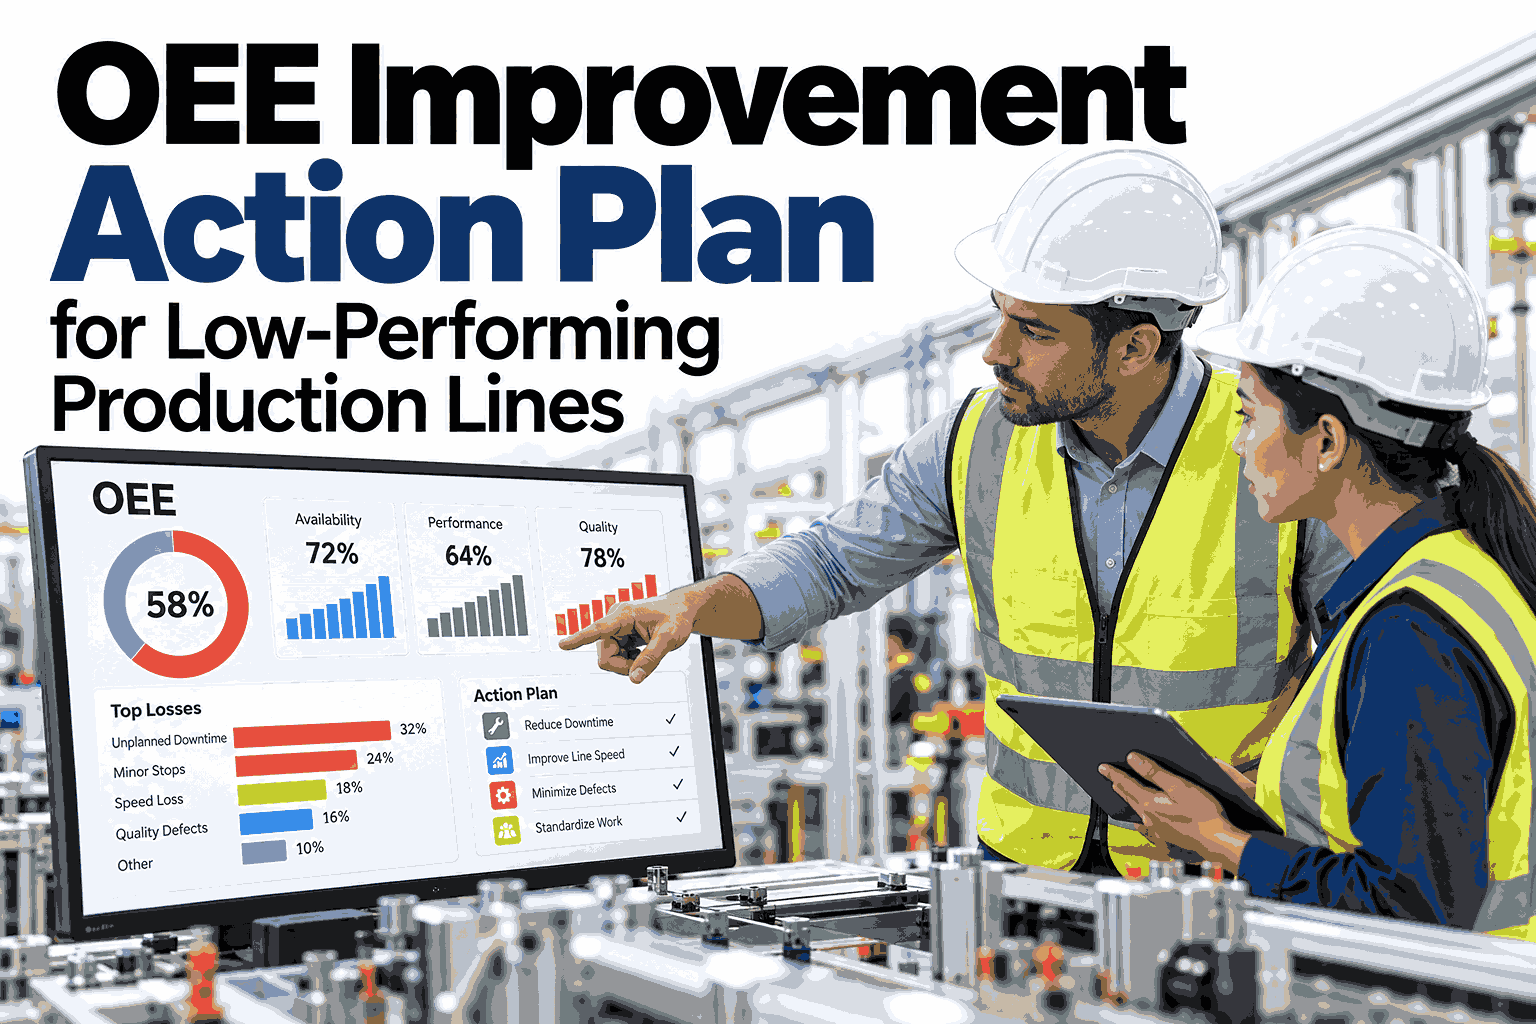
A line running at 60 percent OEE is not a failing line. It is a line quietly giving away four hours of every ten to stops, slow cycles and scrap. Most plants know which lines look weak, but few can say which loss is responsible or what to fix first. An action plan turns that guess into a ranked list with owners, dates and a target. This guide lays out a practical plan for low-performing lines, from baseline to sustained gains. Teams that want to check their own numbers can see how iFactory AI ranks OEE losses on live line data before they commit to a plan.
OEE Improvement Action Plan for Low-Performing Production Lines
A step-by-step plan to find the biggest loss, fix it first and hold the gain on every shift.
Why a Low OEE Score Hides the Real Problem
A single percentage tells you a line is weak. It does not tell you why. Three habits keep plants stuck at the same score for years.
A weekly average smooths away the one bad shift that caused most of the lost output.
Stop reasons typed in by hand at the end of a shift are often vague, late or missing.
Teams fix many small things at once, so no single fix is large enough to move the score.
The cure is the same for all three: measure each loss separately, rank them, and put the whole team behind the top one.
Where Your Score Really Sits
World-class OEE is usually quoted at 85 percent. Many lines run far below it, and the gap is where the money is.
The Six Big Losses to Hunt
Every minute of lost OEE falls into one of six buckets. Name the bucket first, then pick the tool.
See Your Six Big Losses Ranked by Cost
Book a 30-minute session and iFactory AI will show how each loss is captured, tagged and ranked for your own lines.
A Worked Example: One Line at 61 Percent
The numbers below are illustrative. They show why fixing the weakest factor beats polishing the strongest one.
Quality was already at 96 percent, so the gain came from stops and slow cycles. A team that chased scrap would have spent months on the smallest prize.
The Five-Step Action Plan
Work the steps in order. Each one produces something the next step needs.
Baseline the line
Record A, P and Q for four weeks using machine data, with ideal cycle time agreed by engineering and operations.
Rank the losses
Build a Pareto of lost minutes by cause. The top two or three bars usually hold most of the gap.
Find the root cause
Use five whys on the top loss and confirm with data from the shifts where it was worst.
Fix and standardise
Apply the countermeasure, update the work instruction and train every shift on the new method.
Monitor and repeat
Track the loss daily, set an alert band and move to the next bar of the Pareto once it holds.
Match the Loss to the Right Countermeasure
Use this table to move from a loss category to a first action your team can start this week.
| Loss | First Action | Proof It Worked |
|---|---|---|
| Breakdowns | Criticality ranking and planned lubrication routes | Fewer unplanned stops per week |
| Changeover | Split internal and external setup tasks | Shorter average changeover time |
| Minor stops | Log every stop under five minutes by cause | Stop count falls on the top cause |
| Reduced speed | Test rated speed with controlled quality checks | Actual cycle approaches ideal cycle |
| Startup rejects | Standard warm-up recipe and first-piece check | Lower scrap in the first hour |
| Production rejects | Control charts on key process settings | First-pass yield rises and holds |
A 30-60-90 Day Roadmap
Short cycles keep momentum and let the team see results before attention drifts.
Habits That Make the Gain Stick
Scores slip back when the work stops being visible. Four routines keep it in front of the team.
Daily five-minute huddle
Review yesterday's top loss at the line, with the operator who saw it.
One owner per loss
Every ranked loss has a named person and a date for the next update.
Operator-led checks
Cleaning, inspection and lubrication belong to the people who run the machine.
Weekly loss review
Managers check whether the Pareto is shrinking, not whether the meeting happened.
Where iFactory AI Fits
iFactory AI reads machine, quality and maintenance data together, so every loss is captured, ranked and explained without manual logs.
Automatic loss capture
Stops, slow cycles and rejects are timestamped from machine signals and tagged by cause.
Live OEE by line and shift
A, P and Q update continuously, so a bad hour is seen while it can still be fixed.
Ranked loss Pareto
Lost minutes are ordered by cost, so the team knows which fix is worth the most.
Ask in plain language
Managers can ask why OEE fell on Line 3 and receive the ranked causes.
Frequently Asked Questions
What is a good OEE target for a low-performing line?
Do not jump straight to 85 percent. A realistic first goal is a gain of 10 to 15 points over the baseline within 90 days. Set the target from your own loss data, then raise it as the top losses are removed. You can review target setting on your own line data in a live session.
Which factor should we fix first, A, P or Q?
Fix the one with the largest gap to its realistic level, which is usually availability or performance. Quality is often already high, so the gain per hour of effort is smaller. A ranked Pareto settles the question with data. To see how, request a loss ranking walkthrough with the iFactory AI team, or ask support about line setup.
How do we measure OEE without manual logs?
Pull run state, counts and reject signals directly from machines or controllers, then tag stops by cause on a short list. This removes end-of-shift guesswork and keeps data consistent across lines. Starting with one pilot line is usually enough. A short product tour of automatic capture shows the setup.
How long before we see results?
Quick wins on minor stops and changeovers often show within the first 30 to 45 days. Larger gains from breakdown and quality work take a full quarter. Daily tracking makes progress visible early so the team stays engaged. See a typical 90-day tracking view in a guided session.
Can the plan be repeated across other lines?
Yes. Once the method and loss categories are standard, a second line can follow the same five steps in less time. Comparing lines on the same basis also shows where best practice already exists. Schedule a multi-line comparison walkthrough to see how it works.
Turn Your Weakest Line into Your Best Case Study
iFactory AI captures every loss, ranks it by cost and tracks the fix shift by shift. Book a walkthrough to see it on your own lines.