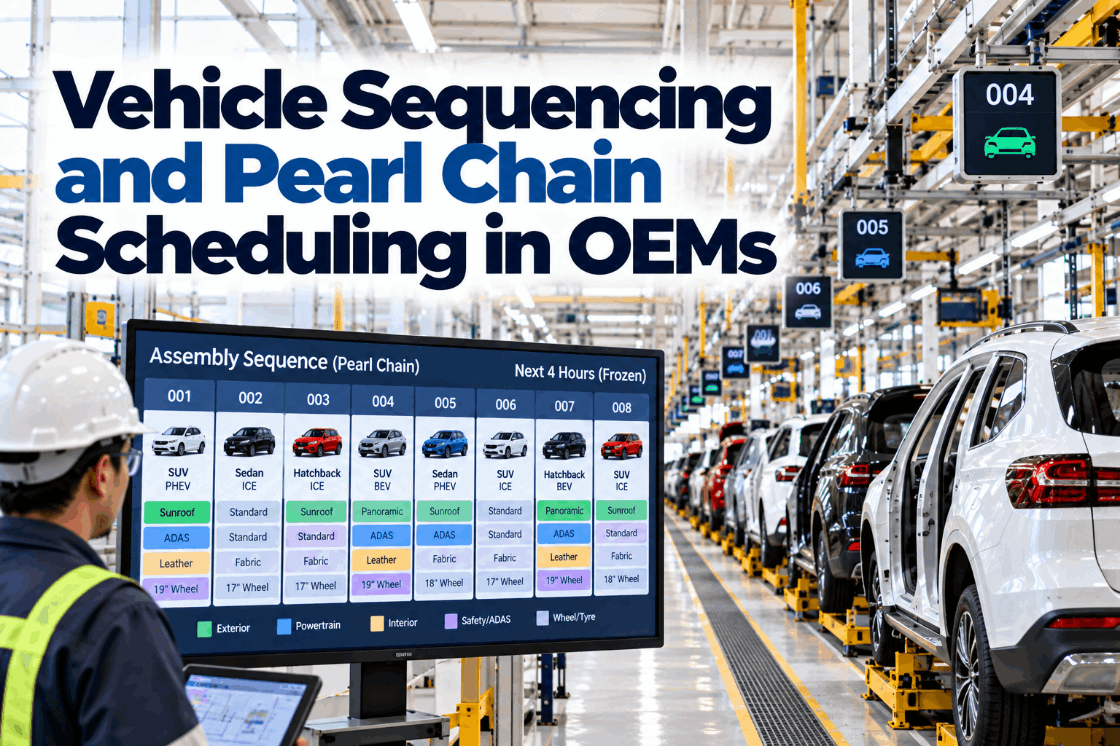
The pearl chain, known in German as the Perlenkette, is the fixed order in which vehicles are planned to move through body, paint and final assembly. Once it is fixed, suppliers build and deliver seats, cockpits and other modules in the same order, and the plant commits to keeping it. In practice, bodies fail inspections, parts go missing and trucks arrive late, and every disruption threatens the chain. This guide explains how the pearl chain works, how it is built, what breaks it, how leading plants recover and how to measure stability. To see pearl chain stability tracked on your lines, book a short walkthrough.
Vehicle Sequencing and Pearl Chain Scheduling in OEMs: Build, Protect and Recover the Chain
A stable build sequence fixed days ahead, protected from disruption and recovered quickly with painted body storage, so suppliers deliver in order and final assembly runs as planned.
Why the Pearl Chain Matters
An automotive plant with just-in-sequence suppliers depends on a promise: vehicles will arrive at final assembly in the order planned. Seat, cockpit, bumper and door suppliers build to that order and deliver racks in sequence. If a vehicle arrives out of order, the part at the station is wrong, the line may stop or the vehicle is built with a workaround.
The pearl chain is how that promise is made. Supply chain sources describe the sequence as fixed several days before production, giving suppliers a stable view. The detailed JIS call-offs that tell suppliers exactly what to deliver are then sent hours before each vehicle reaches the station. Keeping the chain intact from body shop to final assembly is what makes both work.
A note on timing: some descriptions say the pearl chain freezes a few hours ahead. That is closer to the JIS call-off horizon than the chain itself. Exact horizons vary by OEM and plant, so each plant should document its own.
The German term Perlenkette, a string of pearls, captures the idea well: each vehicle has its place, and the chain only has value if the pearls stay in order. Pulling one out leaves a gap that someone has to fill.
Stability is measurable and improvable. We can review your sequencing performance on a call.
How the Pearl Chain Works
The pearl chain links planning, production and suppliers through one fixed sequence.
The chain is only as strong as its weakest shop. Body shop holds and paint repairs are the usual places where vehicles leave their positions, which is why paint and body data matter so much to sequencing.
ILVS depends on accurate tracking. Every body carries an identity, read at key points such as body shop exit, paint entry, paint exit and assembly entry. Those reads tell planners where each body is and whether it is still in position, which is the raw data for both recovery and stability reporting.
Each plant defines its own freeze horizon and recovery rules. We help document them during implementation.
Building a Stable Pearl Chain
Stability starts with a sequence that can actually be built.
Confirm parts, capacity and engineering for every order.
Ratio rules, spacing and work content balance.
Colour blocks balanced against assembly rules.
JIS suppliers can build to the sequence.
Sequence fixed and shared for the agreed horizon.
Bodies started in sequence in the body shop.
Building feasibility in from the start prevents many later disruptions. Orders that are not buildable because parts are short should not enter the frozen sequence, or they will leave it later and break the chain.
The Renault car sequencing problem, set as the ROADEF industrial challenge in 2005, shows why this is hard. Balancing ratio rules for assembly against colour batching for paint is a difficult optimization, and the sequence must be good on both counts to stay stable.
Good sequencing software makes those trade-offs visible. See it in a demo.
What Breaks the Pearl Chain
Most disruptions fall into a few categories.
Bodies failing paint audit leave sequence and rejoin later.
Dimensional or weld issues hold bodies back.
Missing parts make planned vehicles unbuildable at their slot.
JIS racks late or in the wrong order.
Stops in body or paint change the arrival pattern at assembly.
Customer changes inside the frozen horizon.
Paint is usually the largest source of sequence loss, because paint defects are common and repair loops take time. That is why painted body storage is the main buffer used to restore the chain.
Tracking the causes separately is the first step to improving stability. A plant that knows most of its sequence loss comes from one paint repair loop can target that loop directly, rather than adding buffer everywhere.
Linking each sequence break to its cause shows where to act first. Ask our team how causes are recorded.
How Leading Plants Recover the Chain
Recovery follows a clear order of options, from least to most disruptive.
Replace the missing body with a matching one from PBS so the sequence continues.
Swap vehicles nearby where ratio rules and JIS sequences allow.
Place the repaired body back in a slot that respects rules and supplier sequence.
Change JIS call-offs only where the supplier horizon allows.
Run an empty slot when no suitable body is available.
Involve planning and suppliers when disruption exceeds buffer capacity.
Painted body storage is the key. A PBS with enough bodies of the right mix can fill most gaps without affecting suppliers. Keeping its mix balanced is itself a planning task.
Speed matters as well. A gap discovered as the body arrives at assembly leaves few options. A gap detected when the body fails paint audit leaves time to find a replacement in storage and to warn suppliers if needed.
Recovery rules should be agreed and automated rather than improvised. Our planners help define them with your team.
Measuring Pearl Chain Stability
A simple stability measure shows how well the chain holds.
Illustrative. Plants often track stability at several points: body shop exit, paint exit and assembly entry.
Tracking stability by cause and by shop shows where to act. If paint accounts for most out-of-position vehicles, improving first-time-through quality in paint improves the whole chain.
Stability should be reviewed with suppliers too. JIS suppliers feel every sequence change, and sharing stability data helps them plan and builds trust in the plant’s commitments.
Reporting stability daily keeps it visible. We provide it in every rollout.
Pearl Chain Checklist
Use this checklist to strengthen your pearl chain.
Most plants find paint repair loops cause most breaks. A sequence review usually confirms it.
What a Stable Pearl Chain Is Worth
A stable pearl chain benefits the plant and its suppliers.
With automotive downtime around $2.3 million an hour on Siemens’ figures, even small improvements in stability that avoid line stops are valuable. The exact value depends on your current stability and how often breaks stop the line.
Suppliers gain too. A stable chain lets them run their own sequenced production efficiently, which over time can support better terms and fewer expedited deliveries.
A review of a month of stability data usually shows where the gains are. Book one with our advisors.
How iFactory Delivers Pearl Chain Scheduling
Ratio rules, colour blocks and buildability together.
Every body’s position through each shop.
Matching bodies chosen from PBS automatically.
JIS call-offs aligned with the actual sequence.
Daily stability by shop and cause.
Agreed options applied in the right order.
It works with your ERP, MES, body tracking and supplier systems. Share a month of sequence data and we will show your stability by cause in a session.
See Where Your Pearl Chain Breaks
Share a month of sequence and body tracking data. We measure stability at each shop, rank the causes of breaks and show how much painted body storage can recover.
Body 1182 failed paint audit and will rejoin 46 positions late. Painted body storage can fill the slot with a matching body, keeping JIS call-offs in order.
A Paint Repair Absorbed by the Chain
This exchange shows how a sequence planner might use iFactory.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the vehicle sequencing and body tracking analytics models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers sensors and data connections across body, paint, assembly and utility systems, PLC/SCADA, MES, CMMS and ERP integration, cabling and network setup, operator and quality team training, and 24×7 remote monitoring.
Server installed, PLC, MES and ERP links live, historical production, quality and maintenance data loaded.
Models calibrated on your own lines, then run in advisory mode on one line or area with your planners and engineers reviewing every output.
Rollout to the agreed lines under your change management, planner, supervisor and engineer training, and 24×7 remote monitoring in place.
Software, server and integration come as one package. For pricing on your plant, contact our sales team.
Frequently Asked Questions
The pearl chain, or Perlenkette, is the fixed sequence in which vehicles are planned to move through body, paint and final assembly, shared with suppliers so they can deliver parts in the same order.
Supply chain sources describe the sequence as commonly fixed several days before production. Detailed JIS call-offs are sent hours before each vehicle reaches the station. Exact horizons vary by OEM and plant.
Paint repairs, body shop holds, missing parts, late or wrong supplier racks, equipment stops and late order changes.
By filling gaps from painted body storage, swapping vehicles within rules, reinserting repaired bodies carefully, adjusting call-offs only where allowed and escalating when buffers are exhausted.
As the share of vehicles entering final assembly, or another key point, in their planned position, tracked daily by shop and cause.
A first line can typically have stability tracking and recovery support within a 6–12 week rollout. Plan it with our planners.
Keep Every Vehicle in Its Place in the Chain
iFactory builds a buildable sequence, tracks every body through each shop and fills gaps from painted body storage, so suppliers deliver in order and final assembly runs as planned.
Illustrative. Share of vehicles entering final assembly in their planned position.