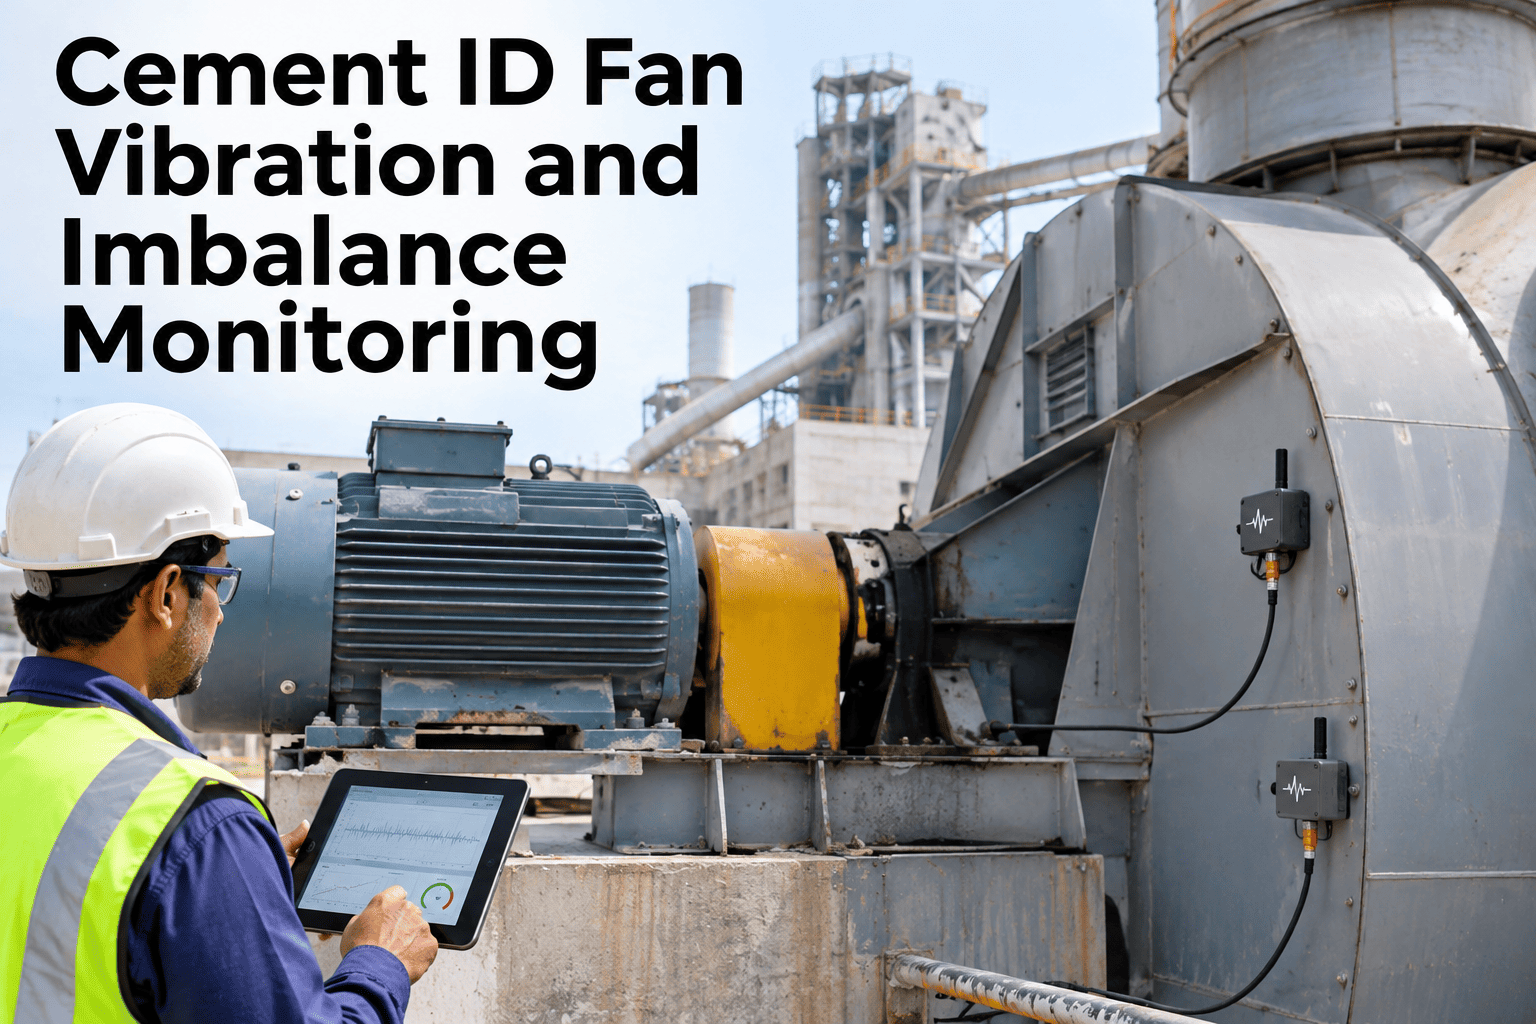
An induced draft fan pulls hot gas out of the kiln continuously, and when it fails the kiln can go cold within the hour, triggering a refractory cool-down cycle that takes far longer to reverse than the fan repair itself. Published research on kiln induced draft fans found horizontal-plane vibration readings rose by more than 120 percent in the window before bearing failure, far more than the vertical or axial planes moved. Cement ID fan vibration and imbalance monitoring reads that same signal continuously, so blade imbalance, bearing wear and misalignment are caught as a spectrum shift weeks before they become a trip. Reliability teams who want this mapped to their own ID or preheater fans can discuss their plant data and fan use case with iFactory.
Read the Spectrum Before the Fan Reads You a Kiln Trip
iFactory, an on-premise AI platform for predictive maintenance, trends ID and preheater fan vibration by frequency and by plane, so imbalance, bearing wear and misalignment are told apart weeks before a trip.
What Is ID Fan Vibration and Imbalance Monitoring?
ID fan vibration and imbalance monitoring is the continuous tracking of vibration amplitude, frequency content and measurement plane on an induced draft or preheater fan, so a developing imbalance, bearing fault or misalignment is identified before the fan's protection system trips the kiln. Unlike a single overall-vibration reading, spectrum-based monitoring tells failure modes apart, which decides whether the fix is a cleaning job or a bearing change. Because a cement kiln has no buffer between the preheater, the kiln and the cooler, an ID fan trip does not stay contained to the fan; it stops the whole pyroprocessing line and starts a refractory cool-down that a plant would much rather avoid scheduling on short notice.
Four Failure Modes Behind Most ID Fan Trips
Mass imbalance from deposit
Alkali and sulfate buildup on impeller blades is the most common ID fan failure mode in cement, creating uneven static and dynamic imbalance.
Bearing wear
Defect frequencies appear in the spectrum well before amplitude rises enough to trip a simple overall alarm.
Misalignment
Shows up as a dominant frequency at twice running speed, often with an axial phase shift.
Erosion-driven asymmetry
Dust erosion thins one side of the impeller unevenly, slowly shifting the fan's balance over months.
Reading the Vibration Spectrum
An overall vibration reading tells you something is wrong. The frequency spectrum tells you what. Matching the dominant frequency multiple to its fault family is the core skill of fan vibration analysis.
| Dominant Frequency | Likely Fault |
|---|---|
| 1× running speed | Mass imbalance, typically from blade deposit or erosion |
| 2× running speed, with axial phase shift | Misalignment between fan and motor |
| Bearing defect frequencies | Race or rolling element wear |
| Sub-synchronous, 0.4–0.6× | Looseness or aerodynamic instability |
Why the Measurement Plane Matters
Vibration does not move the same amount in every direction, and published research on kiln induced draft fans shows the horizontal plane is the most predictive axis for bearing failure on this equipment type.
See Your Own Fan Spectrum Read
Share a vibration history from one ID or preheater fan, and iFactory AI will show how the spectrum would have been classified.
Operating Conditions That Shift the Baseline
A fan's normal vibration signature is not fixed. Comparing today's reading against the wrong baseline produces both missed faults and false alarms.
Setting Alarm Thresholds by Severity Zone
Most cement plants set ID fan alarm zones with reference to ISO 10816 vibration severity bands, with the zone boundaries adjusted to the specific fan's mass, speed and mounting.
Inspection Checklist for ID and Preheater Fans
A Composite Scenario: Catching Blade Deposit Before It Became Imbalance
A preheater fan on a kiln line showed a slow 1× amplitude climb in the horizontal plane over three weeks, with no change recorded in gas temperature, load or damper position. The spectrum read ruled out bearing defect frequencies and misalignment, pointing instead to a developing mass imbalance consistent with blade deposit buildup. A borescope inspection confirmed uneven alkali deposit on three impeller blades, and the fan was cleaned and rebalanced during a short planned stop instead of being left to run until the imbalance tripped the fan's own protection system. This kind of scenario is illustrative of how spectrum classification narrows the likely cause before anyone opens the fan casing, which matters because a preheater fan inspection is not something a crew wants to schedule speculatively.
Why Maintenance History Belongs With the Trend
A vibration trend read without the fan's maintenance history is only half the picture. A balancing job, an impeller clean or a bearing change should reset the baseline, or the next comparison measures the fan against a state that no longer exists. iFactory, an on-premise AI platform for predictive maintenance, keeps the spectrum trend and the maintenance record against the same asset, so a re-baseline happens automatically after major work instead of being forgotten.
Overall Vibration Monitoring vs Spectrum Analysis
| Approach | Tells You | Limitation |
|---|---|---|
| Overall vibration | Something has changed | Does not identify the fault type |
| Spectrum analysis | Which fault family is developing | Needs a trained read or an automated classifier |
Where iFactory AI Fits
iFactory combines spectrum classification, plane comparison, baseline management and maintenance history for every ID and preheater fan in one on-premise system, so a confirmed fault reaches a work order automatically. Deployment runs on your own server, which keeps fan and kiln process data inside the plant network rather than a third-party cloud.
Spectrum Classification
Dominant frequencies are matched to likely fault families automatically.
Plane Comparison
Horizontal, vertical and axial readings are tracked and weighted by fan type.
Auto Re-Baseline
A balancing or repair job resets the trend reference automatically.
CMMS Work Orders
Confirmed faults open a scheduled job with the spectrum attached.
Frequently Asked Questions
How early does spectrum monitoring catch ID fan imbalance?
Reported lead times on cement ID fans typically range from a few weeks to about a month, depending on the fault and how aggressively the deposit or wear is progressing. See typical lead times on your own fans during a short walkthrough.
Is horizontal-plane vibration always the most important reading?
For kiln induced draft fans, published research found horizontal-plane vibration the most predictive axis for bearing failure, but all three planes should still be tracked together for a complete picture. Ask support how plane weighting is set for your fan type.
Do we need a vibration specialist on staff to read the spectrum?
Not necessarily. Automated classification can match the dominant frequency to a likely fault family, with a specialist reviewing confirmed alerts rather than every raw reading. See how the classification works on your own data.
How often should the alarm thresholds be reviewed?
Thresholds should be revisited after any balancing job, bearing change or significant process shift, since the fan's normal signature changes with the work done on it. Review your current threshold setup with the iFactory team.
Can this cover preheater and cooler fans as well as the main ID fan?
Yes, each fan is tracked in its own asset record with its own baseline and zone settings, so the full fan fleet can sit in one system. Ask support about covering your full fan list.
Give Every ID Fan a Spectrum Reading, Not Just an Alarm Light
Book a session with iFactory AI and see your own fan vibration data classified by fault family before it ever reaches a trip.