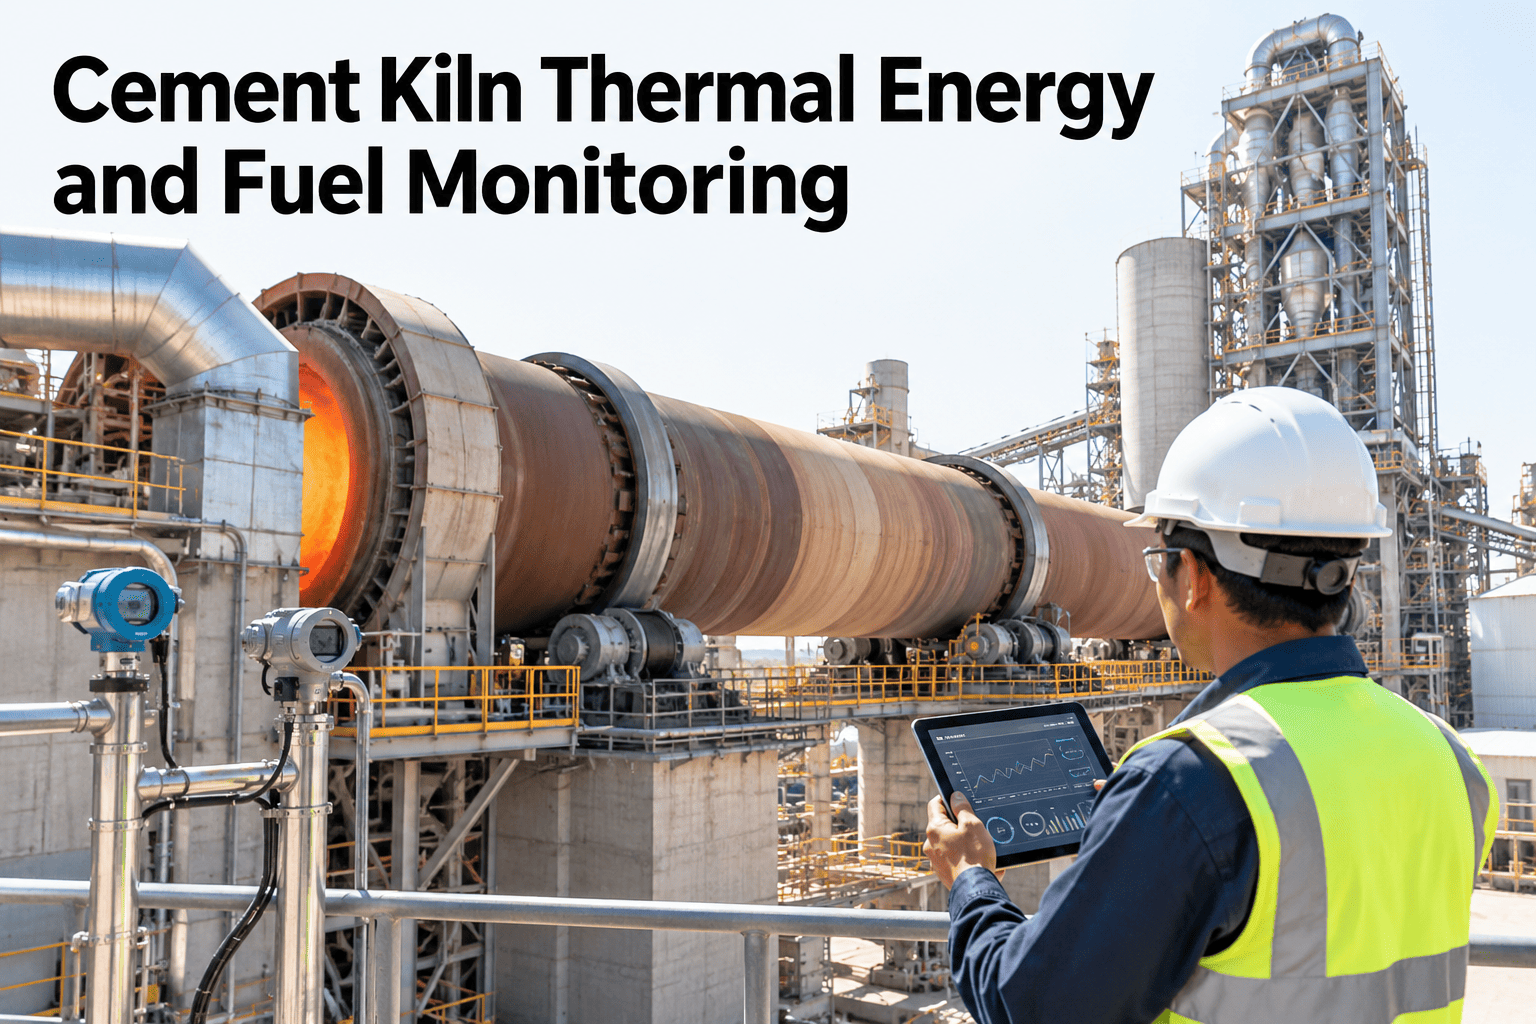
The kiln is where most of a cement plant's energy cost actually lives, yet thermal energy monitoring often gets far less attention than electrical monitoring, partly because fuel flow and heat consumption are genuinely harder to track precisely than a kWh meter reading. A kiln running a few percent above its normal thermal energy per tonne of clinker rarely triggers an alarm, since nothing fails outright, it just quietly costs more fuel every single day it continues. Monitoring fuel flow against clinker output consistently, not just reviewing it at month-end, is what catches that kind of drift while it is still a small and cheap problem to fix, and if you want to see this applied to a recent period of your own kiln data, you can review a thermal energy trend with our team.
Catch Thermal Energy Drift Before It Becomes a Permanent Cost
Continuous monitoring of fuel flow against clinker output, so a small rise in thermal energy per tonne gets caught and investigated while it is still cheap to fix.
The Fuel Flow Data Behind an Accurate Thermal Picture
Thermal energy monitoring starts with reliable fuel flow data, and the accuracy of everything downstream depends on getting this input right.
How Heat Consumption Metrics Get Calculated
Fuel quantity alone does not tell the full story, since different fuels and fuel mixes deliver different amounts of heat per unit consumed.
Calculating this consistently across the fuel mix, rather than just the primary fuel alone, is what keeps the figure accurate as alternative fuel ratios shift from period to period.
Why Clinker Output Context Matters as Much as the Fuel Side
Thermal energy per tonne only means something when read alongside what the kiln was actually producing at the time, since output rate itself affects thermal efficiency.
| Operating context | Typical thermal energy effect | What to check first |
|---|---|---|
| Below-rated kiln output | Higher thermal energy per tonne | Feed rate against kiln design capacity |
| Startup or shutdown period | Significantly higher thermal energy per tonne | Whether the period should be excluded from steady-state trends |
| High alternative fuel ratio | Variable, depends on fuel calorific value | Calorific value testing frequency for that fuel batch |
| Stable, full-rate operation | Closest to the kiln's design efficiency | Comparison baseline for all other periods |
Separating startup, shutdown, and below-rate periods from stable operation is essential, otherwise a handful of unusual periods can distort the entire trend line.
Review Your Own Kiln's Thermal Trend
Share a recent period of fuel and output data and we will show where your kiln's thermal energy is trending.
What Trend Analysis Actually Catches
A single day's reading rarely tells you much, but a consistent trend across weeks is where genuine drift becomes visible against normal day-to-day variation.
A gradual creep like this, roughly a single-digit percentage increase over two months, is exactly the kind of drift that a month-end review alone often misses but a running trend view catches early.
Turning the Trend Into a Reporting Workflow
Catching drift is only useful if it leads to a consistent process for investigating and reporting on it.
What iFactory Cement and Energy Specialists See on Kiln Lines
iFactory cement and energy specialists who review kiln thermal data across multiple plants find that a gradual upward drift, rather than a sudden spike, is the more common and more costly pattern, since it tends to go unnoticed for weeks before anyone investigates.
They recommend reviewing thermal energy trends weekly rather than monthly specifically because of this pattern, since a weekly view catches the drift early enough that the eventual fix is usually small and operational rather than a larger maintenance intervention.
What Kiln Operators and Energy Managers Ask
Bring Thermal Energy and Fuel Monitoring to Your Kiln Line
Book a session with iFactory AI to review your kiln's thermal energy trend and set up ongoing drift detection against your own baseline.