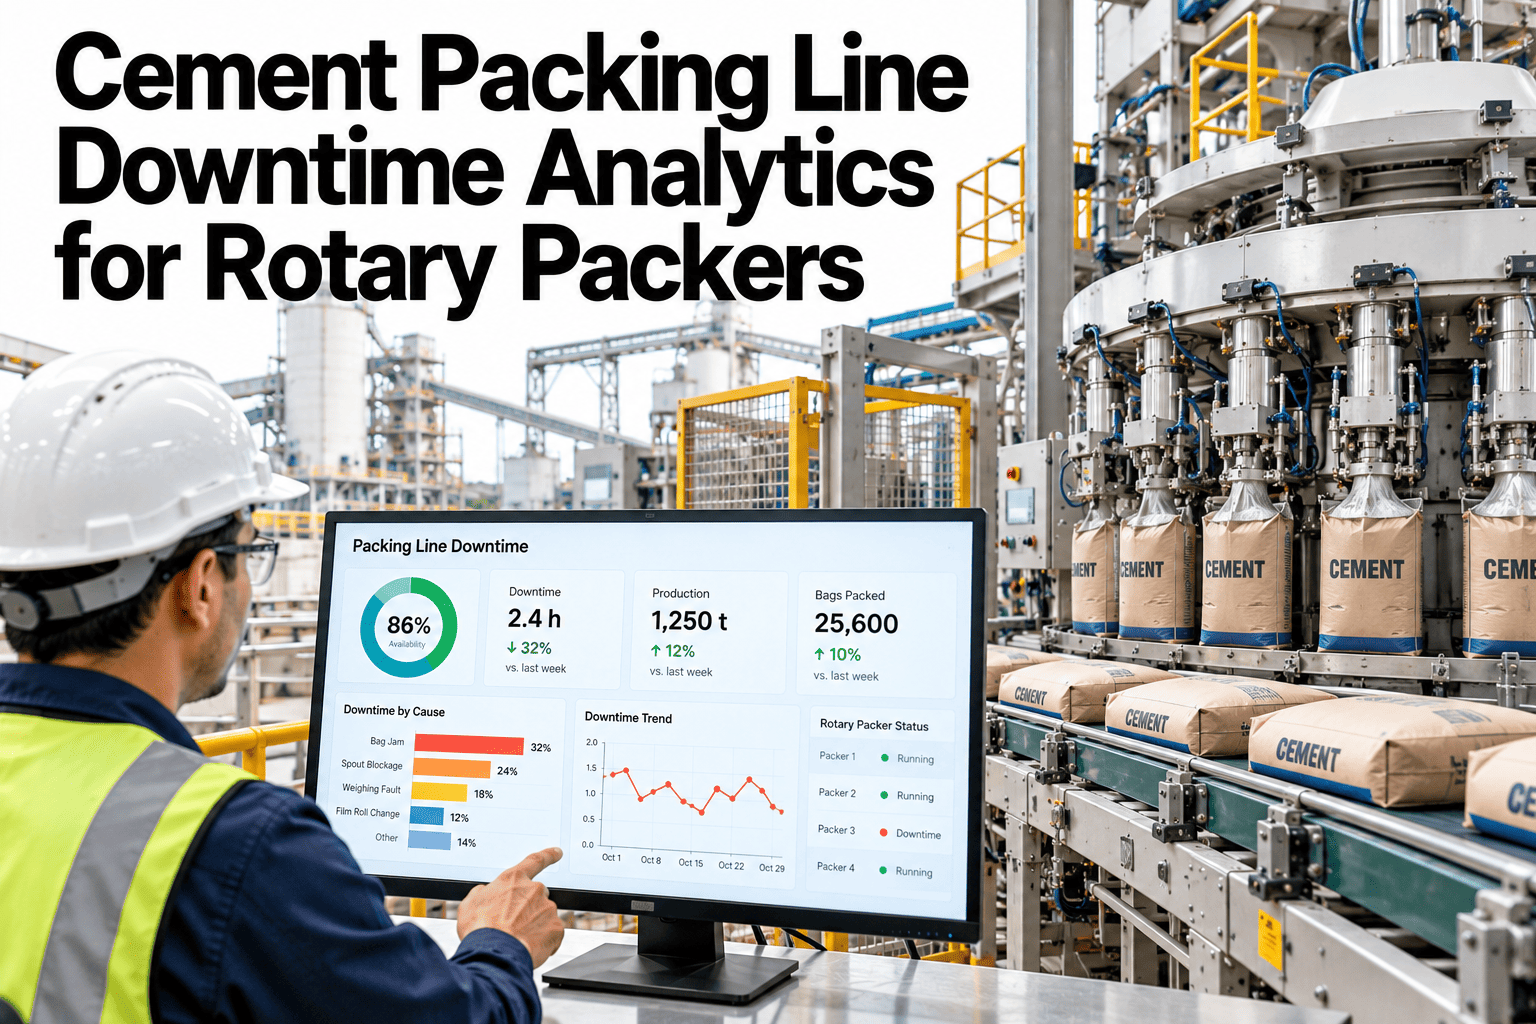
A rotary packer can stop for a dozen different reasons in a single shift, and most plants only find out which one cost the most time at the end of the month, if at all. Spout jams, bag misfeeds, weight rejects and belt stops all look the same on a basic uptime report. This guide covers how to break packing line downtime into causes that can actually be acted on, by packer and by shift. Teams ready to see their own packer data this way can book a demo with the iFactory AI team.
Cement Packing Line Downtime Analytics for Rotary Packers
A rotary packer's downtime causes fall into a short, repeatable list. Naming them consistently and tracking them by packer and shift turns a vague uptime percentage into a prioritized action list.
Building a Downtime Taxonomy for Packers
A packer stop needs a cause code before it is useful data, and the code list has to be specific enough to act on. "Mechanical stop" tells nobody anything. "Spout 6 seal failure" tells the maintenance team exactly where to look.
| Category | Example Causes | Typical Owner |
|---|---|---|
| Spout issues | Seal failure, clogged spout, misaligned bag clamp | Maintenance |
| Bag supply | Empty bag magazine, torn bag, wrong bag size loaded | Operations |
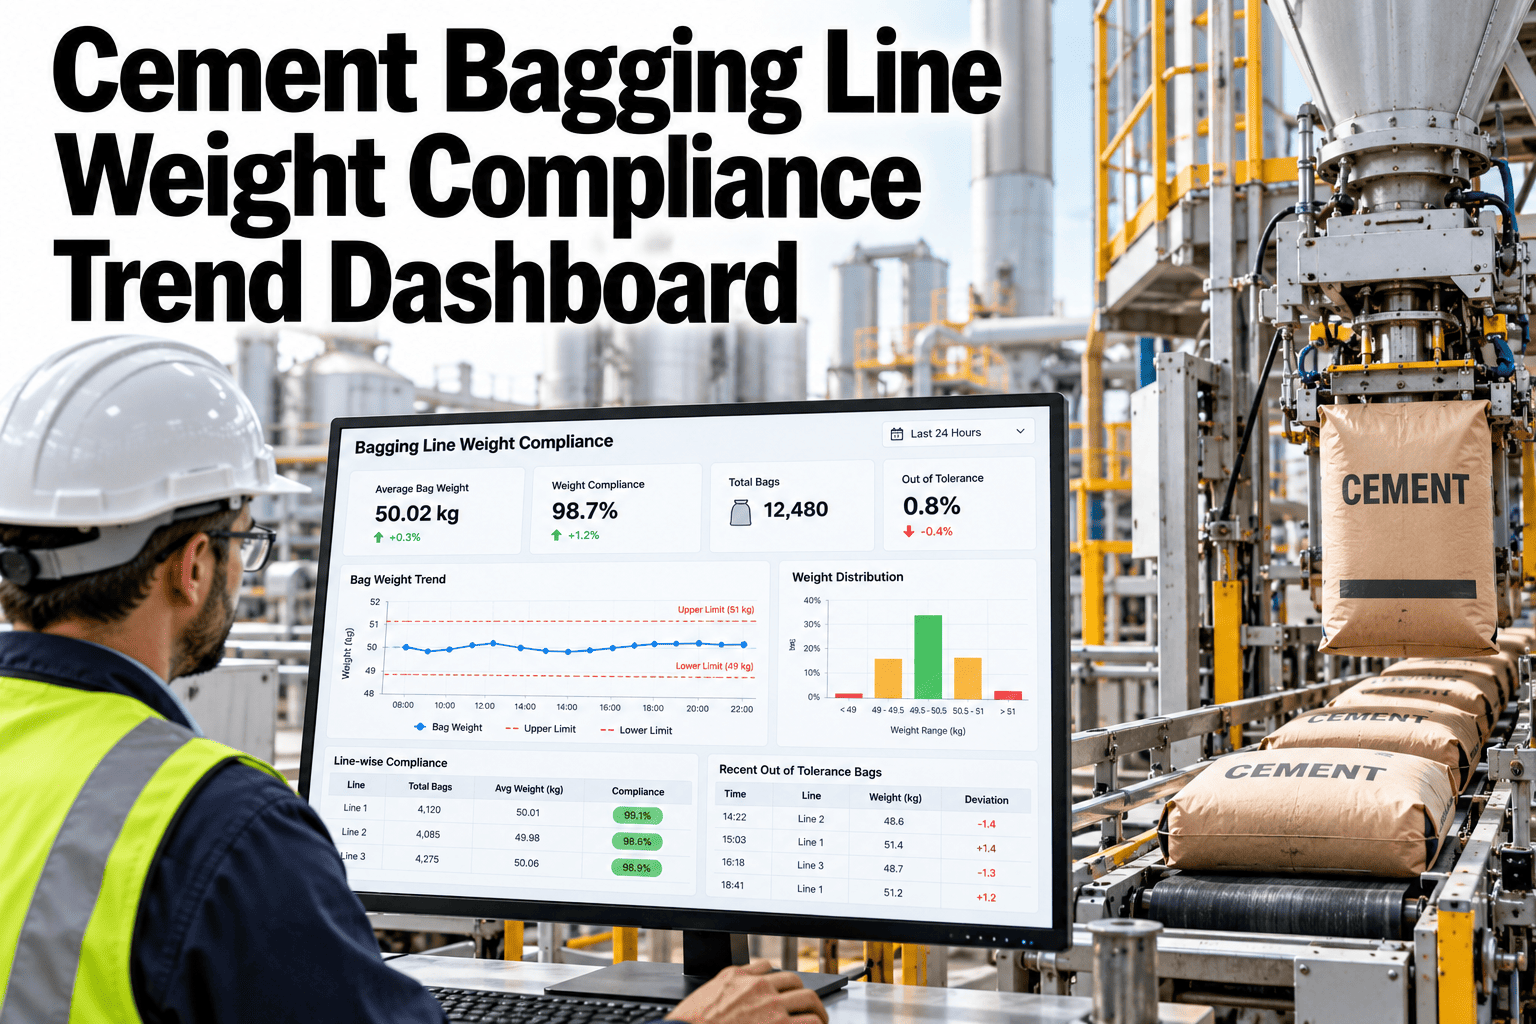
| Weight control | Rejected underweight or overweight bag, scale drift | Quality |
| Conveying | Belt jam, discharge chute blockage | Maintenance |
| Upstream supply | Cement silo low level, feed screw stoppage | Production |
Packer and Shift View
The same downtime total looks completely different once it is split by individual spout and by shift. A packer with one consistently underperforming spout points to a mechanical fix. A shift with consistently higher downtime points to a training or staffing gap.
In this illustrative view, Spout 3 stops roughly three times as often as Spout 8. Without the per-spout breakdown, that imbalance disappears into a single line-wide downtime number, and the seal or clamp issue on Spout 3 keeps costing time unnoticed.
Stop Duration, Not Just Stop Count
A high-frequency, short stop and a rare, long stop can cost the same total minutes but call for different fixes. Counting stops alone hides this difference.
Nuisance stops
Minor bag misfeeds or clamp resets, often fixable with a mechanical adjustment or operator retraining.
Breakdown stops
Seal failures, motor faults or jams needing a maintenance call, usually the bigger single-event time loss.
See Every Packer Stop Categorized Automatically
iFactory AI captures packer stops by spout, cause and duration, so your team acts on the biggest losses first. Book a 30-minute walkthrough.
Recurring Causes Worth a Standing Fix
Some causes never go away with a one-time repair. They need a standing countermeasure, whether that is a changed maintenance interval, a different bag spec, or an operator checklist added to shift handover.
Dispatch Impact
Packing downtime does not stay contained at the packer. Every stopped minute on the line shows up later as a longer queue at the weighbridge and a truck turnaround time that creeps up without an obvious cause at the gate.
Action Tracking
A downtime cause only stays fixed if the action taken against it is tracked to completion. Logging the cause without logging the fix just produces a longer history of the same problem.
| Field | Purpose |
|---|---|
| Cause code and spout | Links the action to the specific recurring issue |
| Action taken | What was actually done, not just planned |
| Owner and due date | Keeps the fix from stalling indefinitely |
| Recurrence check | Confirms whether the cause actually stopped appearing |
Plain-Language Glossary
A shared vocabulary keeps maintenance, operations and quality reading the same downtime data the same way.
Expert Review
Packing line reviews across cement plants keep returning to the same two notes.
Rank by minutes, not count
Splitting stop duration from stop count almost always reprioritizes the top fix. A spout with many short nuisance stops often ranks below a rarer, much longer breakdown stop once minutes are totaled.
Connect to dispatch
Plants that connect packer downtime to the dispatch queue find it far easier to explain truck turnaround spikes to customers, since the cause can be shown rather than guessed at.
Frequently Asked Questions
How many downtime cause codes should a packer have?
Somewhere between eight and fifteen specific codes usually covers a rotary packer well, broad enough to be manageable but specific enough to act on. Book a demo to see a starter code list.
Should every spout be tracked separately?
Yes, since averaging across spouts hides exactly the kind of imbalance that points to a specific mechanical fix. A per-spout view is where most of the actionable insight lives.
How does packing downtime connect to dispatch metrics?
Every minute the packer is down delays the next bag reaching a truck, which compounds into queue time at the weighbridge. Book a demo to see packing and dispatch data linked.
Can this work with a manual stop-logging process?
It can start there, though automated detection from packer PLC signals catches short stops a manual log tends to miss. Ask support which packer PLCs are commonly connected.
How often should the recurring cause list be reviewed?
A weekly review catches recurring causes quickly, with a monthly rollup to check whether prior fixes actually held.
Turn Packer Stops Into a Prioritized Fix List
iFactory AI captures and categorizes packer downtime by spout, cause and duration, connected through to dispatch impact. Book a walkthrough built around your line.