Coating is the single most underappreciated variable in a cement kiln's economics. It is not a material anyone buys, tracks in inventory, or lists on a monthly cost report, yet a stable coating in the burning zone is what keeps the refractory lining alive, keeps shell temperature inside a safe band, and keeps fuel consumption from creeping upward one degree at a time. When coating fails — either falling away in a chunk or building into an unstable ring — the operator is left compensating in real time, usually with a flame or feed change that fixes the symptom for an hour and reintroduces the problem the next shift. Raw mix chemistry sets the ceiling on how coatable a clinker is, and flame shape decides whether that potential coating actually forms and holds in place, which is a gap iFactory's process team spends most of its time closing with plants, and you can book a demo to see the same logic run against your own kiln's shell scanner history.
Coating Failure Costs More Than a Hot Spot — It Costs Weeks of Kiln Availability
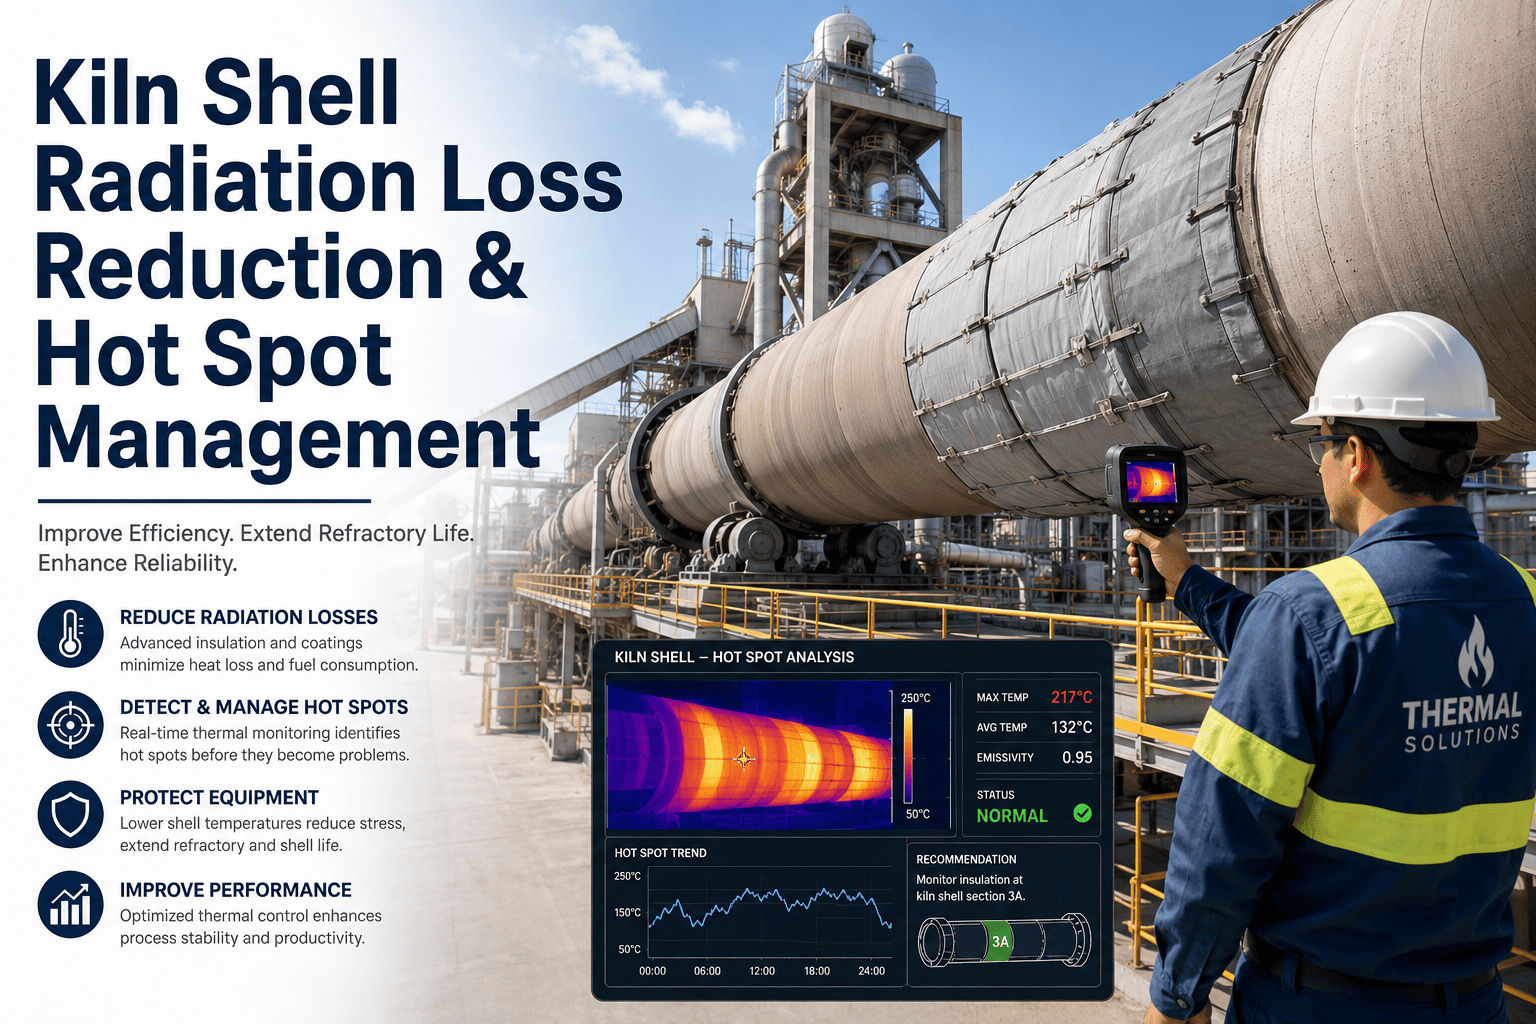
Every unplanned refractory replacement traces back to a coating that either never formed correctly because the raw mix chemistry was fighting it, or fell away because the flame drifted and nobody caught it before shell temperature confirmed the damage. iFactory fuses raw mix chemistry trends, shell temperature scans, and flame behavior into one continuous view of coating condition, so the burning zone operator adjusts before the coating is already gone.
Raw Mix Chemistry Sets the Ceiling — Flame Shape Decides If You Reach It
A kiln can be fed a raw mix with ideal liquid phase chemistry and still run bare refractory in the burning zone if the flame is too long, too hard, or misaligned. The reverse is also true: no amount of flame tuning fixes a raw mix that swings between low-liquid and high-liquid chemistry from one silo draw to the next. Coating management only works when both systems are read together, because a chemistry shift that would normally be harmless becomes destabilizing the moment it lands on top of an already-marginal flame, and a flame adjustment that would normally be safe becomes damaging the moment it lands on top of an already-thin coating.
Raw Mix Chemistry
Lime saturation factor, silica modulus, and minor-element content set how much liquid phase forms at burning zone temperature and how coatable the resulting clinker actually is. This is decided long before the material reaches the burner, often days earlier at the quarry face and the raw mill blending stage, which is why a coating problem traced back far enough almost always has a chemistry footprint somewhere upstream.
Flame Shape and Position
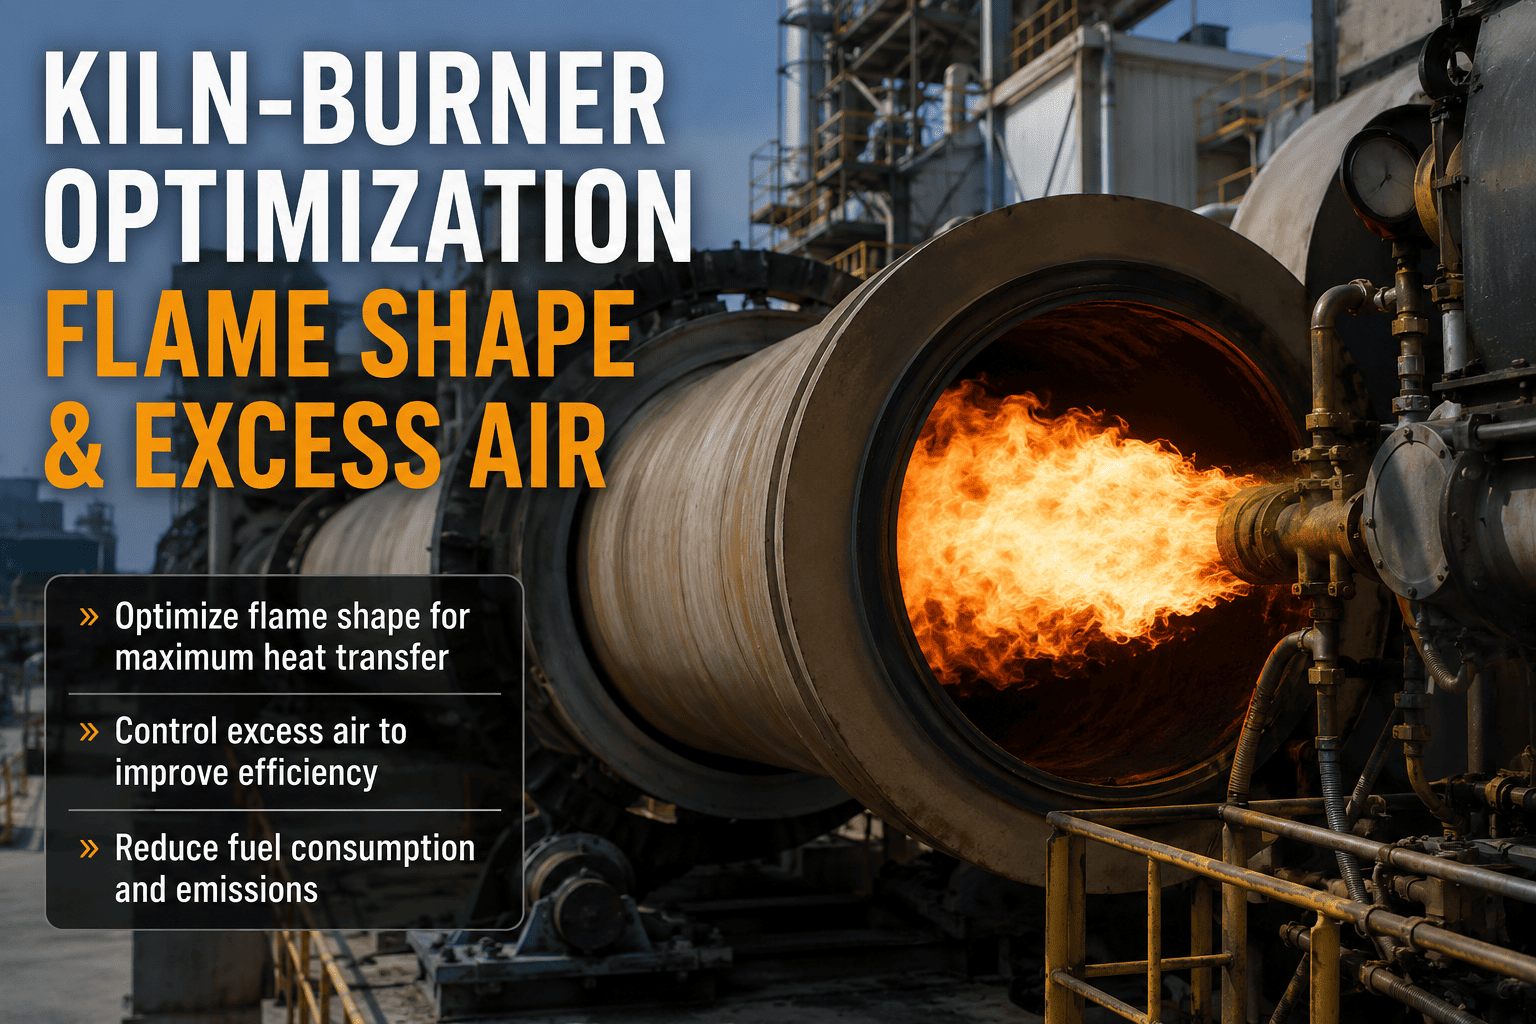
Burner angle, tilt, primary air momentum, and pull-in or push-out position decide where peak heat lands on the coating ring and whether the liquid phase the chemistry produced gets the chance to bond evenly to the brick. Flame is the only lever an operator can pull within minutes, which makes it the default tool reached for even when chemistry is the real root cause.
Treating the two as separate disciplines is where most coating programs stall. Process engineering owns raw mix design, operations owns the flame, and the two teams typically compare notes only after a coating event has already cost refractory or fuel. A kiln that tracks both together closes that gap by surfacing the correlation directly: a shift in silica modulus that lines up with a shell temperature drift two hours later becomes visible as one connected event instead of two unrelated reports filed by two different departments.
The Chemistry Levers That Set the Coating Ceiling
Coating formation depends on liquid phase, and liquid phase in the burning zone is driven almost entirely by four numbers your lab already calculates every shift. Most plants have this data sitting in a quality report and a coating problem happening two buildings away, with nobody connecting the two in real time. Coordinating raw mix adjustment with coating behavior, rather than treating them as separate reports, is where the fastest gains typically sit.
| Chemistry Parameter | Typical Target Range | Effect on Coating |
|---|---|---|
| Silica Modulus (SM) | 2.3 – 2.7 | Above 2.7 starves liquid phase and coating won't build; below 2.3 produces excess liquid that coats thick but unstable |
| Liquid Phase at 1450°C | 23% – 29% | Below range gives dusty, poorly coated burning zones; above range risks refractory infiltration and spalling |
| Alkalis (K₂O + Na₂O) | Below 1.0% | Above 1.0% condenses in the transition zone, disrupting coating adhesion upstream of the burning zone |
| Chlorine Content | Below 0.015% | Above threshold creates volatile cycling that destabilizes coating and accelerates buildup elsewhere in the system |
| Coal Ash Infiltration | Consistent, low-variance | Every 1% ash infiltration shift lowers effective clinker LSF by roughly 0.04 units, moving the coating ceiling without a raw mix change being logged |
The practical challenge is not knowing these targets — most kiln chemists can recite them from memory. It is catching the moment a quarry face shift, a homogenization silo drift, or a wet batch of coal quietly pushes one of these numbers out of range before it shows up as a coating event a shift later. Poor homogenization alone can force a kiln to constantly chase fuel and speed corrections, adding an estimated 50 to 100 kcal/kg to specific heat consumption while coating stability degrades in the background.
Silica modulus deserves particular attention because it behaves almost like a dial for coating character rather than coating quantity. Push it above roughly 2.7 and the mix becomes genuinely hard to burn, forcing higher sustained burning zone temperatures just to keep clinker moving, which in turn increases fuel consumption and pushes the kiln toward the thin, patchy end of the coating spectrum. Pull it below roughly 2.3 and the opposite problem appears: liquid phase becomes abundant enough that the mix burns easily, coating builds fast and looks impressive on a shell scan, but that same coating is often loosely bonded and prone to falling away in large sections the moment feed rate, fuel quality, or kiln speed shifts even slightly. Neither extreme is where a plant wants to operate for sustained periods, and the target range exists precisely because it is the band where coating forms thin enough to stay bonded and thick enough to actually protect the brick.
Coal ash and moisture deserve the same scrutiny raw mix chemistry gets, because fuel quality swings are one of the most common blind spots in coating troubleshooting. A wet coal delivery that pushes moisture above roughly 1% reduces combustion efficiency and flame temperature in a way that looks, from the burning zone's perspective, almost identical to a raw mix chemistry problem — yet the fix is entirely different. Without a system that tracks fuel quality alongside raw mix chemistry and flame behavior, plants frequently spend a shift adjusting burner position to correct a coating drift that a coal moisture reading would have explained in seconds.
Flame Adjustment for Coating Control, One Move at a Time
Flame adjustment is where coating management actually happens in real time, because raw mix chemistry can only be corrected on the timescale of a homogenization silo, while a burner move changes coating conditions within minutes. That speed is also the risk: a large, uncoordinated flame adjustment made to fix one symptom can just as easily strip coating somewhere else in the burning zone.
Confirm Burner Alignment Before Anything Else
The burner should sit on the nose ring pointed up the kiln axis. A tip misalignment of as little as 15mm can shift the flame roughly half a meter down the kiln, raise shell temperature locally, and shorten brick life by weeks — long before an operator would attribute the change to burner position.
Use Push-In or Pull-Out to Target a Specific Coating Zone
If coating is failing at the front end of the kiln, pushing the burner in by up to half a meter moves peak heat away from that section. If the flame is running too long and heat is landing too far down the kiln, pulling the burner out by a similar margin brings the peak back toward the nose ring.
Balance Primary Air Momentum Against the Burning Zone Load
Primary air volume and velocity control flame momentum and how well secondary air is entrained into the flame. Too little momentum produces a soft, long flame that builds thick but unstable coating; too much produces a hard, short flame that damages coating right at the burner tip.
Coordinate Every Move With Kiln Speed and Feed Rate
A flame adjustment made in isolation from feed rate and kiln speed is a guess. The same burner position that stabilizes coating at one feed rate can strip it at another, which is why flame moves should always be read against the current production rate, not applied as a fixed setting.
Each of these moves is well understood individually by an experienced kiln operator, and none of them is difficult to execute on its own. What is difficult is sequencing them correctly under time pressure, at 2am, when a shell temperature alarm has just fired and the instinct is to make a large correction quickly. A large angular change made without confirming refractory condition first, or a push-in made while chemistry is simultaneously drifting toward high liquid phase, can turn a manageable coating event into a multi-day recovery. The kilns that handle coating events best are usually not the ones with the most experienced single operator on shift — they are the ones where every operator, regardless of experience level, can see the same chemistry and flame data at the moment they need to make the call.
Your Lab Already Has the Chemistry Data — It Just Isn't Talking to the Burning Zone
iFactory connects raw mix chemistry trends directly to shell temperature and coating behavior, so a silica modulus drift is flagged before it becomes a bare-refractory hot spot.
Reading the Warning Signs Before They Become an Outage
Coating problems rarely announce themselves cleanly. Most plants only get a hard confirmation once shell temperature scanners show a hot band or a free lime result comes back out of specification, and by then the coating event that caused it has usually already passed. The signs below are the earlier tells, split by which direction the coating is failing.
Signs of Coating Loss
- Localized shell temperature rise on the scanner, even a few degrees, in a section that was previously stable
- Flame appearing to elongate or lose definition without a corresponding feed or fuel change
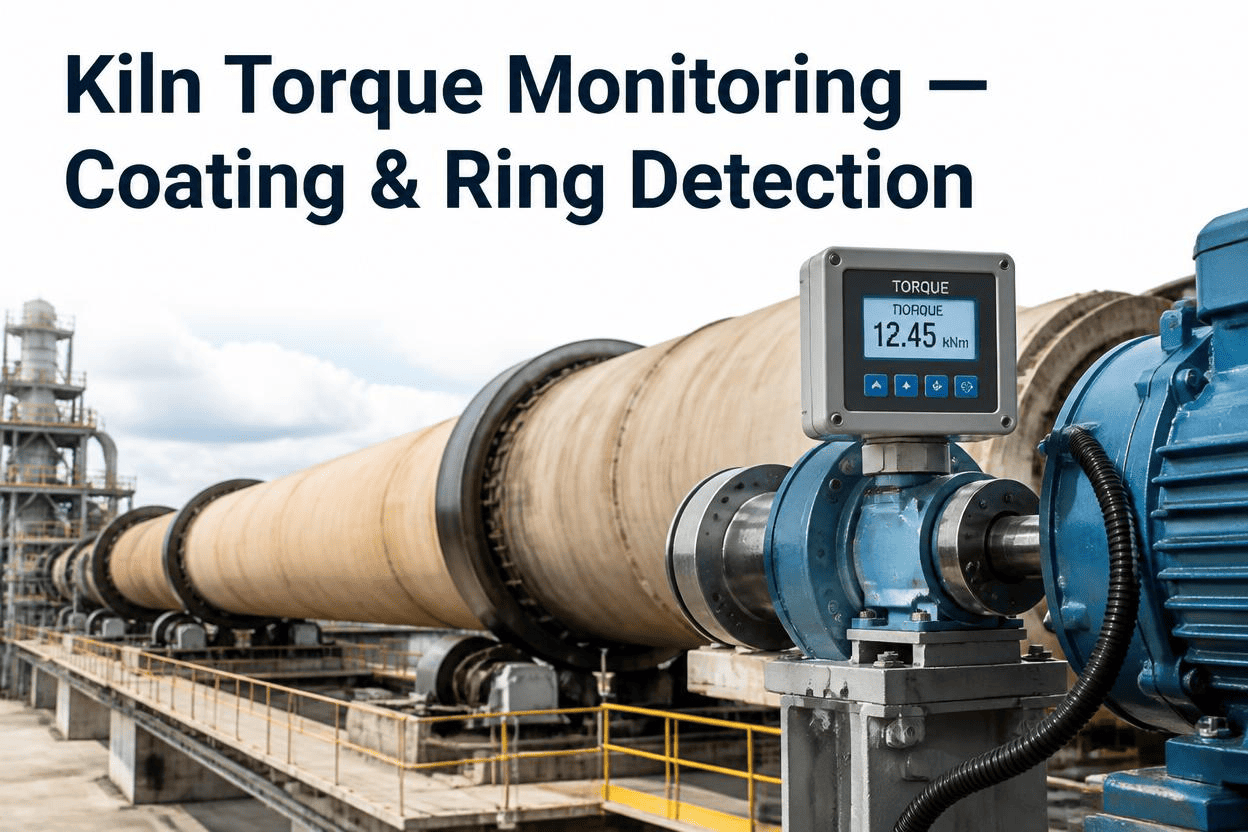
- Kiln torque trending down as the load on the drive reduces with less coating mass on the shell
- Free lime results creeping upward as burning zone heat transfer becomes less consistent
Signs of Coating Overbuild
- Kiln torque climbing steadily as thick, uneven coating adds rotating mass and drag
- Dusty or inconsistent clinker exiting the kiln as excess liquid phase disrupts nodulization
- Sudden torque spikes suggesting a large section of overbuilt coating is about to spall away on its own
- Recurring ring formation in the same kiln zone despite repeated flame corrections
Neither list is useful in isolation, and this is the part most coating troubleshooting misses. A rising shell temperature reading, taken alone, tells an operator that coating is thinning somewhere — it does not tell them whether the cause is a chemistry-driven drop in liquid phase or a flame that has drifted out of position over the last several hours. Reading the same signal against raw mix trend data and recent burner moves is what turns a warning into a diagnosis, and a diagnosis is what lets an operator choose the right correction instead of the fastest one.
What Plants Report After Moving to Condition-Based Coating Control
Plants that connect raw mix chemistry, shell temperature, and flame behavior into a single coating view consistently report the same categories of improvement, even though every kiln's specific numbers vary with its refractory design, raw material source, and fuel mix. The pattern that shows up most often is not a single dramatic fix but a steady reduction in how often the burning zone team is reacting to a surprise, which shows up downstream as fewer unplanned stops and a more predictable refractory replacement schedule.
Building a Repeatable Coating Management Routine
The plants that get the most consistent coating results tend to share a few habits that have nothing to do with expensive hardware and everything to do with how information moves between the lab, the control room, and the shift log. None of these habits require replacing existing instrumentation, and most can be layered onto a kiln's current DCS and quality reporting setup within a few weeks.
Log Coating Events, Not Just Coating Failures
A shift log that only records the day the shell scanner alarmed misses the slow drift that preceded it. Tracking coating condition on a regular cadence, not just during events, builds the history needed to recognize a developing problem the second time it happens instead of the fifth.
Review Chemistry and Flame Moves in the Same Meeting
When raw mix results and burner adjustment logs are reviewed by the same group at the same time, correlations surface that never appear when process engineering and operations review their own data separately on their own schedules.
The common thread across both habits is coordination — coating control is rarely lost because a plant lacks the underlying chemistry or combustion knowledge. It is lost because that knowledge lives in separate reports, reviewed by separate teams, on separate timelines, while the coating itself responds to both systems continuously and at once. Closing that gap is largely a data and workflow problem rather than an equipment problem, which is why it is often one of the faster wins available to a kiln operations team.
Questions Kiln Operations Teams Ask About Coating Management
Stop Trading Refractory Life for Coating Guesswork
iFactory reads raw mix chemistry and flame behavior together to keep coating in its stable working range, shift after shift.