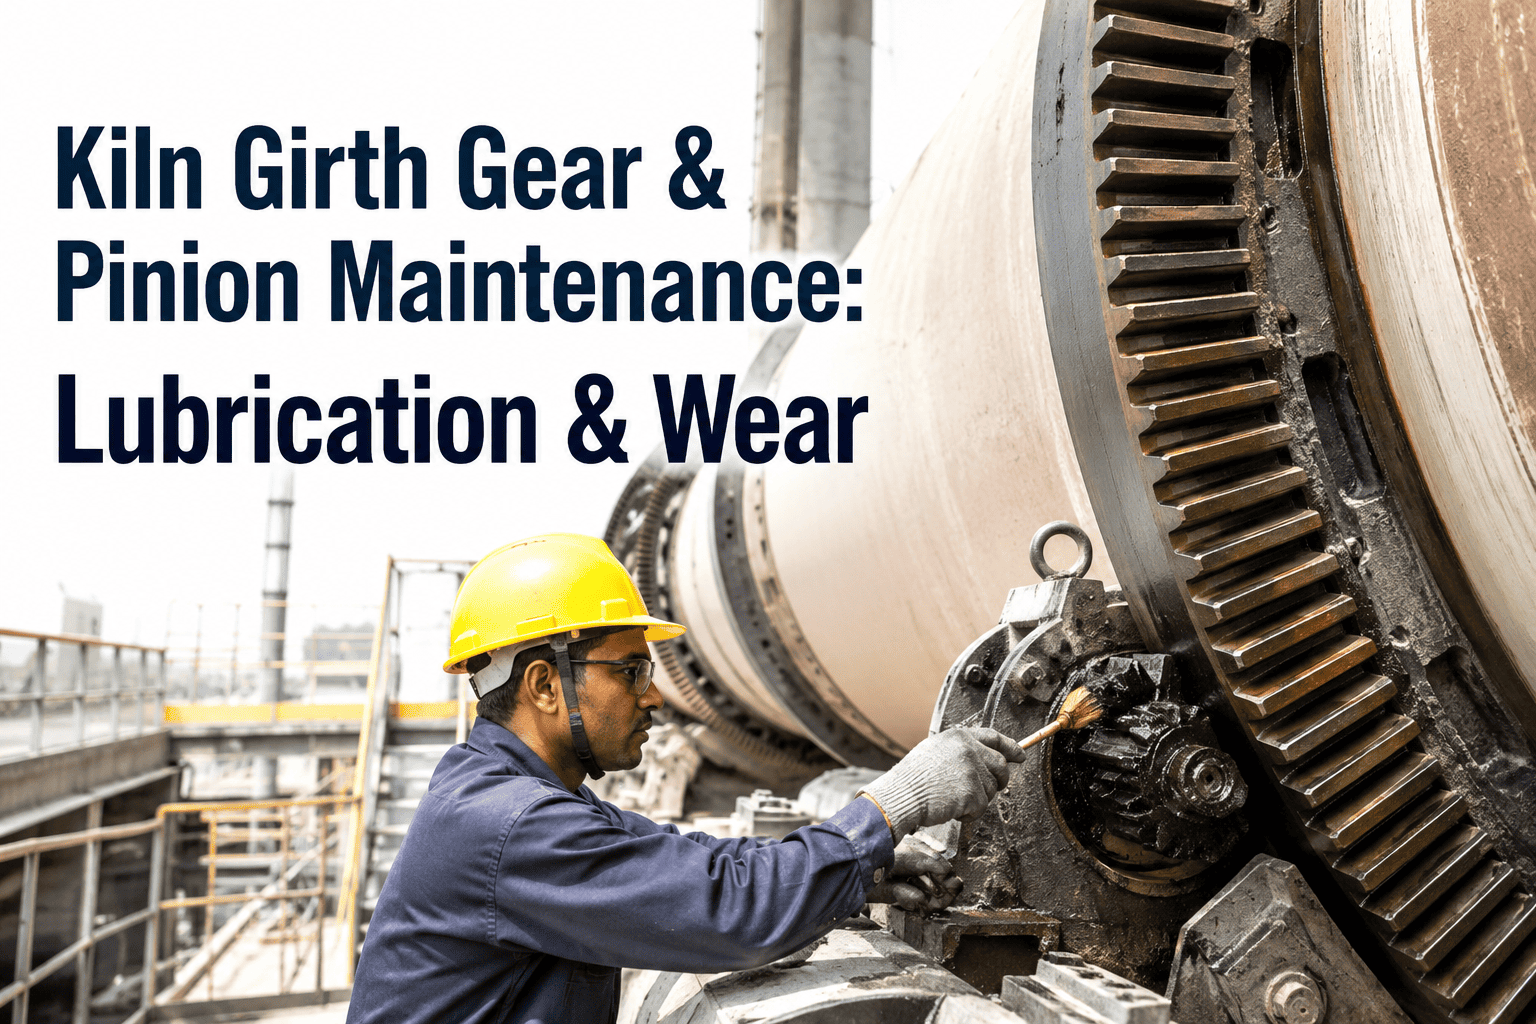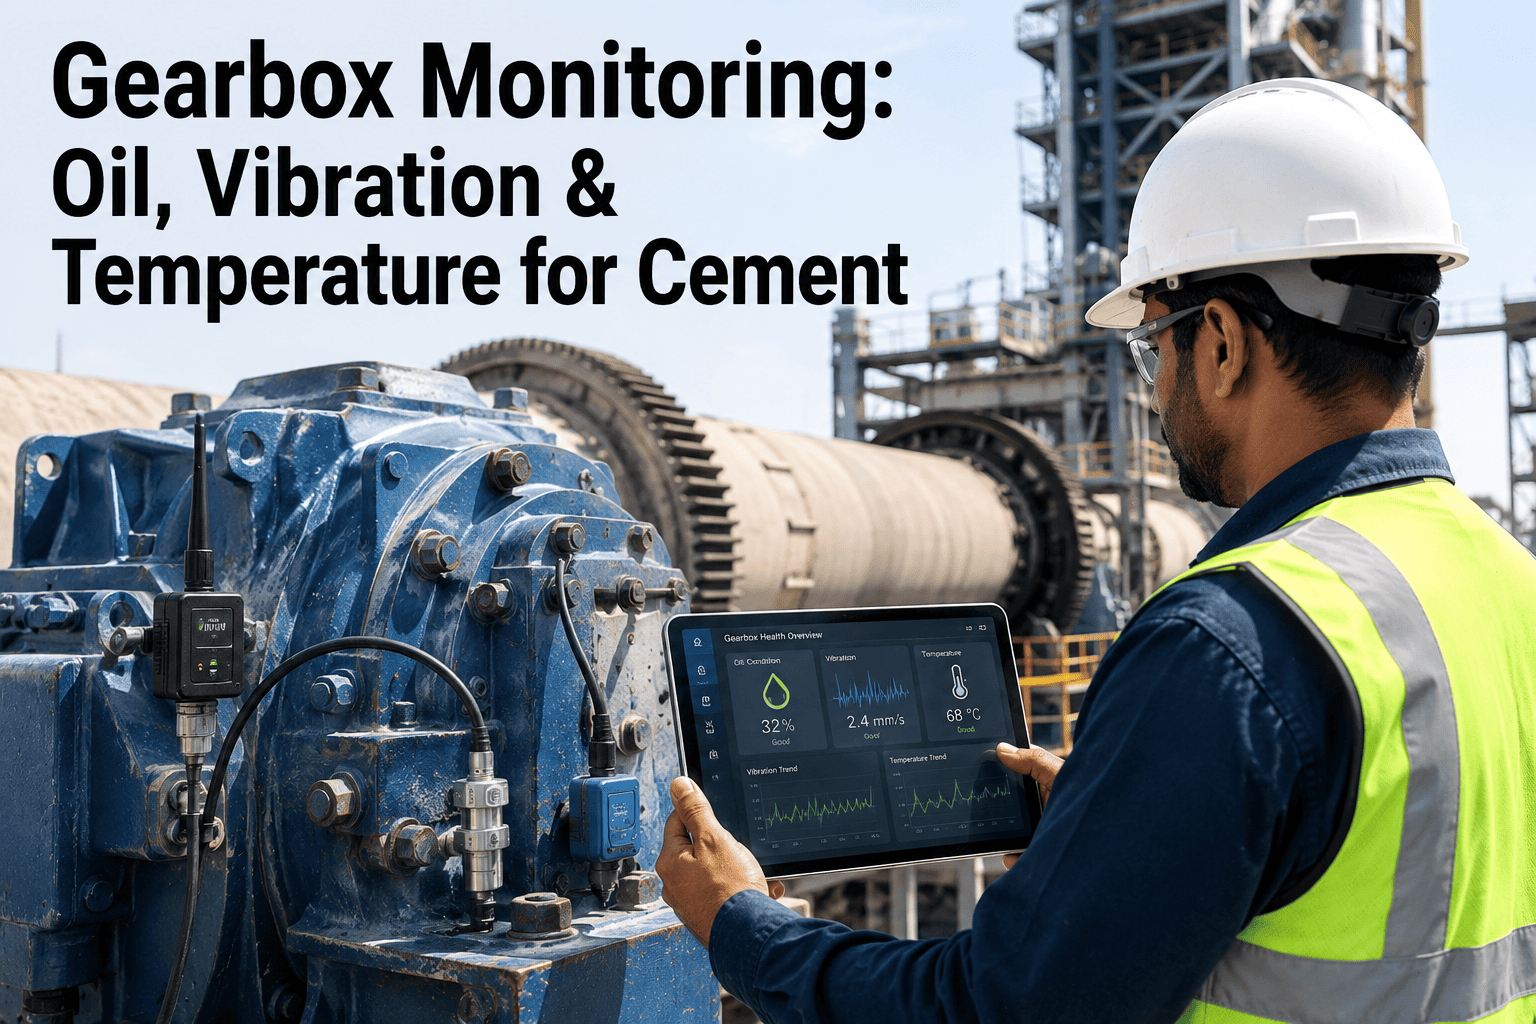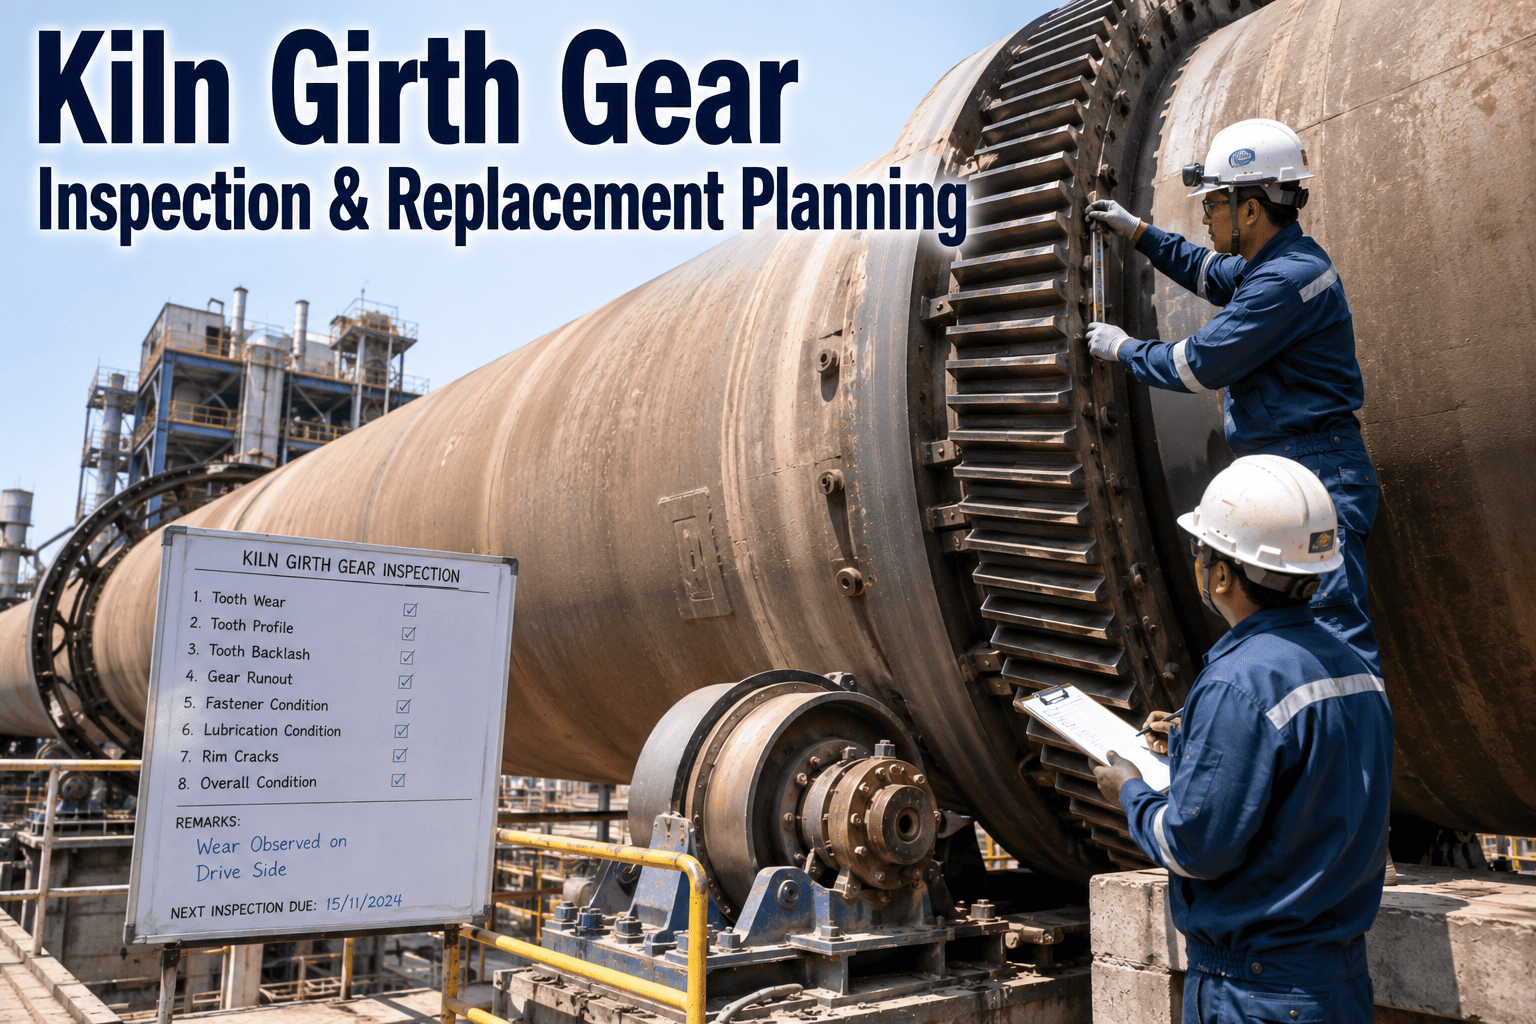
A girth gear rarely fails without warning — it fails after months of warnings nobody connected to each other. A faint click during a quiet shift gets written off as normal kiln noise. A vibration report comes back "within tolerance" because the gear mesh frequency component sits just under the alarm threshold. A pinion bearing runs a few degrees warmer than baseline and nobody logs it as a trend. Then a millwright puts a dial indicator on the housing during a planned outage and finds axial migration three or four times the correctable limit, and the only options left are an emergency shutdown or running a gear that is already grinding metal on metal. The pattern is common enough that iFactory's reliability team sees it on almost every kiln drive assessment it runs.
Girth Gear Failure Has a 6 to 12 Week Warning Window — If Anyone Is Watching
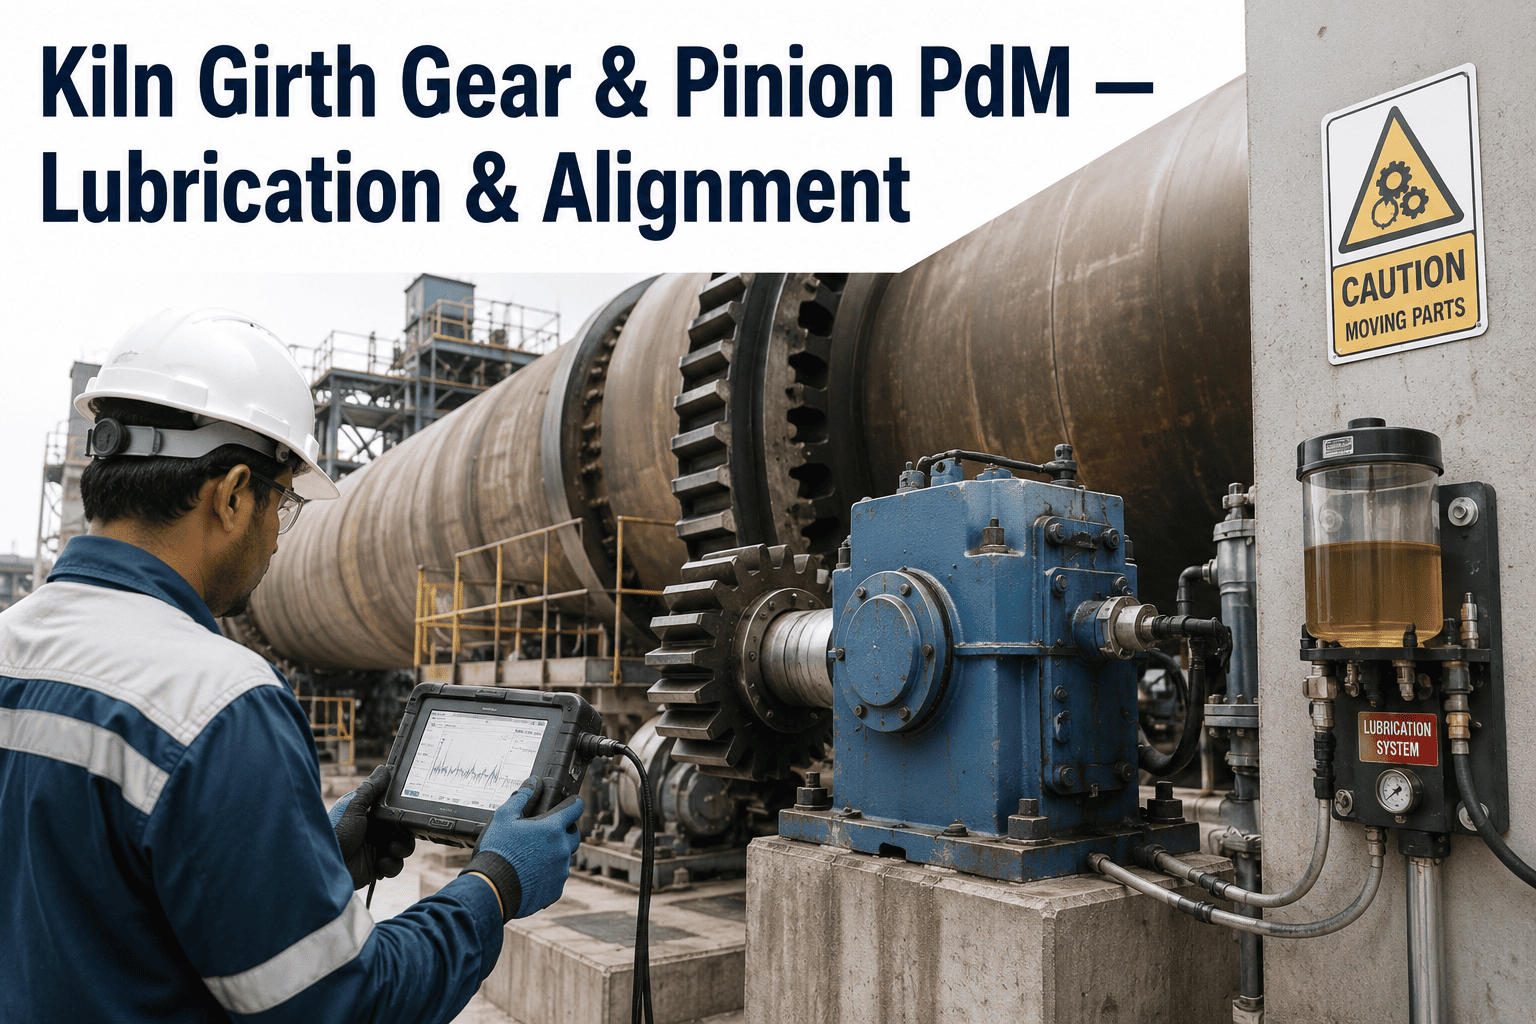
The kiln girth gear is one of the largest single machined components in the plant, meshing with the pinion under continuous heavy load, 24 hours a day, in a dusty, high-temperature environment. Replacement lead time runs three to six months. When it fails, the kiln stops, and every downstream operation stops with it. When it degrades slowly enough to catch, the warning signs show up in vibration, temperature, and lubrication data weeks before the mechanical failure does.
Three Ways a Girth Gear Drifts Out of Alignment
Pinion-to-girth-gear alignment determines how load distributes across the full width of the tooth face. Misalignment does not happen in one way — it develops along three distinct paths, and each one leaves a different signature in the data long before it becomes visible to the eye.
The Pinion Walks Along Its Shaft
Driven by thrust load and foundation movement, axial migration shifts the contact zone toward one edge of the tooth face. It progresses slowly over months, tracked by axial position monitoring on the pinion bearing housing, and is fully correctable if caught early.
The Shafts Stop Running Parallel
Foundation settlement, base bolt creep, or shell ovality tilt the pinion relative to the girth gear centerline. Even a deviation of roughly 0.1 mm per metre of face width concentrates load on one tooth edge, cutting fatigue life by up to 60%.
The Tooth Clearance Opens Up
Wear at the contact face gradually increases the gap between mating teeth, producing impact loading on every mesh cycle instead of smooth rolling contact. Left unchecked, it accelerates tooth pitting and eventually root cracking under cyclic fatigue.
Want to know which of these three is active on your kiln right now? Book a drive-train diagnostic and iFactory will walk your vibration and thermal history against all three drift signatures.
Which Monitoring Signal Catches the Problem First
No single sensor tells the whole story on a girth gear. The value comes from combining signals that each surface a different failure stage, so the earliest one to move gives the maintenance team the longest correction window instead of the shortest. A vibration reading alone might sit comfortably under an alarm threshold while a thermal scan of the same mesh zone already shows a hot spot forming, and neither one on its own tells the full story the way the two together do.
| Monitoring Method | What It Detects | Typical Lead Time | Signal Type |
|---|---|---|---|
| High-frequency vibration analysis | Early tooth pitting, surface fatigue, mesh irregularity via gear mesh frequency and sidebands | Up to 12 weeks ahead of failure | Contact sensor |
| Thermal imaging of the mesh zone | Lubrication film breakdown, localized hot spots, misalignment at the contact interface | 6 to 8 weeks ahead of failure | Non-contact, infrared |
| Motor current signature analysis | Mechanical load variation transmitted through the drive train from the gear mesh itself | Weeks, without any rotating-gear contact | Non-contact, electrical |
| Axial and radial position tracking | Pinion migration and angular drift relative to girth gear centerline | Months, tracked as a slow trend | Dial indicator or laser |
| Blue paper lubrication test | Spray nozzle coverage gaps and edge concentration on the tooth face | Immediate, at time of test | Manual field check |
The Inspection and Lubrication Cadence That Prevents Premature Replacement
Girth gears manufactured from high-strength alloy steel are built for decades of service, but the difference between a gear that lasts 15 to 20 years and one that fails at 6 to 10 years is almost entirely maintenance discipline rather than material quality. The cadence below is not a theoretical ideal — it is the minimum rhythm that plants with long-lived girth gears tend to have in common, regardless of tonnage or kiln size.
Reliability Perspective
We had the vibration data. We had the temperature data. What we didn't have was one screen that put them next to each other with a trend line, so three separate teams each saw a reading that looked fine in isolation. Once we started correlating axial position, mesh frequency, and bearing temperature against the same timeline, we caught a drift that would have gone unnoticed for another two months.
— Maintenance Superintendent, 4+ MTPA cement plant kiln drive assessment
girth gear service life achievable with consistent lubrication, alignment, and backlash monitoring
typical service life where lubrication PM is deferred or misalignment persists uncorrected
fatigue life reduction from angular misalignment as small as 0.1 mm per metre of face width
What an Unplanned Girth Gear Failure Actually Costs
The gear itself is rarely the largest number in an unplanned failure. Production loss, emergency logistics, expedited fabrication fees, and the ripple effect through every downstream operation — clinker cooler, cement mill, packing — dominate the total cost, which is exactly why a 6 to 12 week warning window is worth acting on well before the first emergency call goes out.
typical fabrication and delivery lead time for a replacement girth gear, far longer than any planned outage window
production loss per day of unplanned kiln stoppage, compounding for every day parts and crews are mobilized
of premature girth gear replacements traceable to lubrication, alignment, or backlash issues that were monitorable in advance
Not sure how your kiln's current inspection cadence stacks up? Book a drive-train reliability review and bring your last twelve months of vibration and lubrication records.
Catch Girth Gear Drift While It's Still a Millimetre, Not a Replacement
iFactory correlates vibration, thermal, motor current, and alignment data on a single trend line, so a developing failure surfaces as a pattern across signals weeks before any one reading crosses its alarm threshold. Start with your highest-risk kiln drive. Prove the lead time. Then extend it plant-wide.
Frequently Asked Questions
How often should girth gear and pinion alignment actually be checked?
A full dial indicator or laser alignment check is generally recommended every 6 to 12 months, and always immediately after any major maintenance event such as a gear replacement, shell repair, or foundation work that could shift the relative position of the pinion and girth gear. Between full checks, monthly review of vibration trend data and pinion bearing temperature against an established baseline can surface a developing drift long before the next scheduled alignment window, which matters because correction gets harder and more expensive the longer misalignment is allowed to progress.
What does the blue paper lubrication test actually tell a maintenance team?
The blue paper test is a simple, immediate field check: a sheet of blue paper is held against the gear teeth right after a spray lubrication cycle, and the resulting pattern shows exactly how the lubricant is distributed across the tooth face. A uniform pattern from root to pitch line confirms the spray nozzles are correctly aimed and unobstructed, while edge concentration or visible gaps point to nozzle misalignment, blockage, or a coverage zone that has shifted because the gear itself has moved. Photographing the result and logging it against the work order turns a one-time check into a trend that shows whether coverage is improving or degrading over successive cycles.
Can vibration analysis catch girth gear problems before they're audible?
Yes, and this is where the largest correction window comes from. High-frequency vibration analysis isolates the gear mesh frequency and its sidebands, which can reveal early tooth pitting or surface fatigue up to roughly 12 weeks before the problem becomes audible or before overall vibration levels rise enough to trip a conventional threshold alarm. The key is analyzing the specific frequency components tied to the gear mesh rather than relying on a single overall vibration reading, since a developing fault can hide inside an aggregate number that still looks normal.
Why does girth gear failure risk keep getting missed even when data is being collected?
The most common reason is that vibration, thermal, lubrication, and alignment data get collected by different teams on different schedules and reviewed in isolation, so each individual reading looks acceptable even while the combined pattern points to a developing failure. A vibration reading that sits just under an alarm threshold, a bearing temperature a few degrees above baseline, and a lubrication coverage gap can each be dismissed separately, but together they describe the same drift. iFactory's platform brings these signals onto one timeline specifically to close that gap.
How much does proper alignment and lubrication actually extend girth gear life?
The difference is substantial and well documented: girth gears with consistent spray lubrication, correct alignment, and regular backlash monitoring commonly reach 15 to 20 years of service life, while gears with deferred lubrication maintenance or persistent uncorrected misalignment often fail within 6 to 10 years. Since the gear material and manufacturing quality are typically the same in both cases, the gap is almost entirely attributable to maintenance discipline. Book a reliability review to see where your current program sits against that range.